

=> Pendahuluan
ABS (Acrylonitrile Butadiene Styrene) resin is one of the most widely used engineering thermoplastics in the global plastics industry, serving as a base material for countless high-performance plastic products, ranging from automotive interior components and consumer electronics enclosures to medical device panels and children’s toys. The integral mechanical properties, surface finish quality, and processing stability of ABS directly determine the overall performance of the final molded product, as well as the cost efficiency of subsequent manufacturing operations.
To produce high-quality modified ABS compounds and masterbatches with uniform dispersion, consistent color, and precise dimensional stability, plastic processors must master the fundamental logic of formulation design, production process control, and, most critically, extrusion equipment selection. As a leading manufacturer of professional extrusion equipment with more than 20 years of industry-specific experience, Kerke provides turnkey production solutions tailored exactly to the high-wear, high-shear, and precise mixing requirements of ABS modification and blending production lines, with a focus on the industry-preferred high-torque double-screw extrusion system.
This guide covers all the essential aspects of ABS resin, from its basic definition, key advantages, and major classifications, to practical applications, proven production formulas, optimized manufacturing processes, equipment selection criteria, real pricing factors, and recommendations for trusted suppliers. It is designed to help you make informed and cost-effective decisions for your ABS modification or blending production line.
1. What is ABS Resin?
ABS (Acrylonitrile Butadiene Styrene) resin is a synthetic terpolymer made from three main monomers: acrylonitrile, butadiene, and styrene. It is a versatile, amorphous engineering thermoplastic that balances the rigidity of styrene and acrylonitrile with the toughness of polybutadiene rubber. This unique molecular structure creates a material that combines exceptional mechanical strength, chemical resistance, and processability, qualities that have made it a staple in both general-purpose and high-performance industrial applications.
The precise ratio of these three monomers can be adjusted during production to create specialized grades of ABS, each tailored to specific application requirements. For example, increasing the content of acrylonitrile improves chemical resistance and surface hardness, while a higher proportion of butadiene enhances impact strength and low-temperature toughness. Adjusting the content of styrene, in turn, improves processability and the aesthetic quality of the final product. This level of customization sets ABS apart from many other commodity plastics and explains its widespread use in demanding industries.
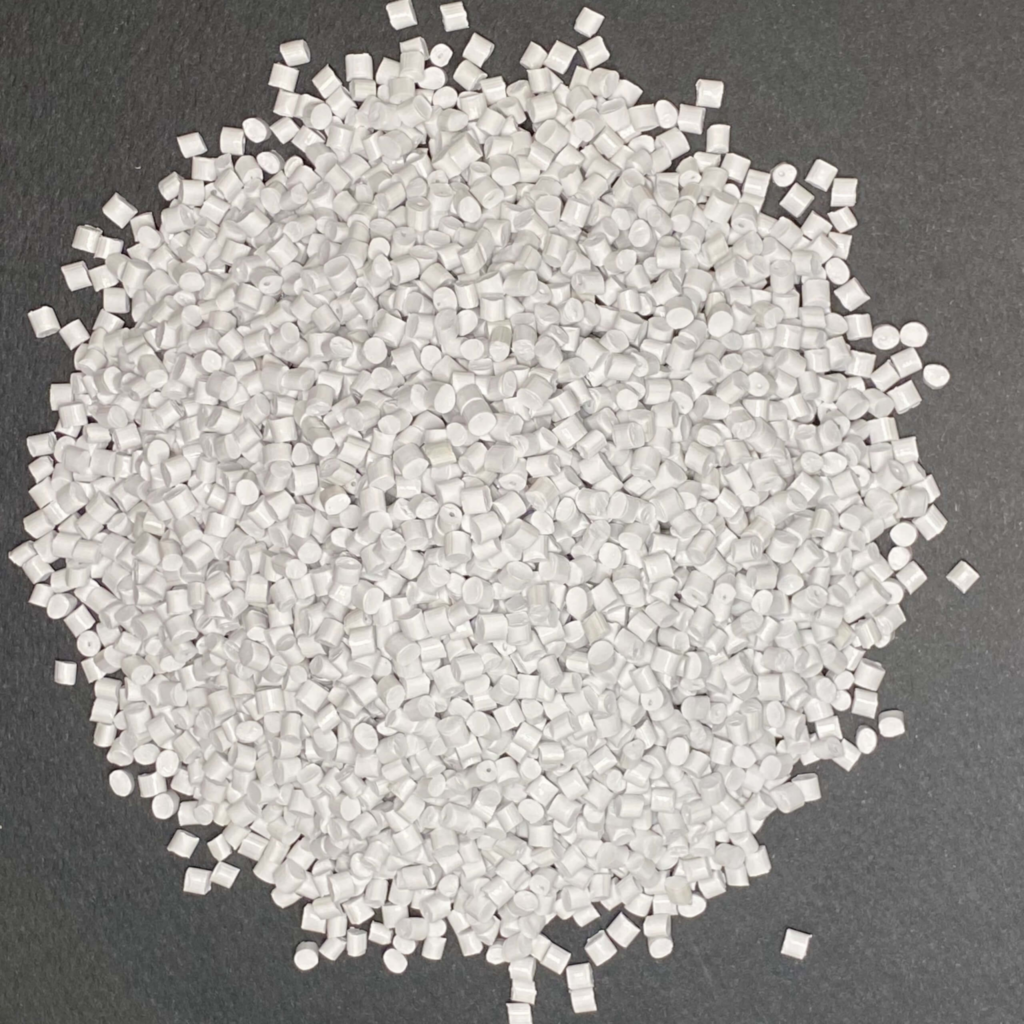
Generally supplied as cylindrical granules in a light ivory or pale yellow color, ABS has a melting point ranging from 217°C to 237°C, with a thermal decomposition temperature starting at approximately 250°C. It is odorless, non-toxic, and has extremely low moisture absorption, critical properties for maintaining consistent performance during high-temperature molding and extrusion. For both converters and end users, ABS represents a balanced and cost-effective solution that delivers reliable performance without sacrificing design flexibility.
2. Main Advantages of ABS Resin
ABS resin has become the preferred engineering plastic for high-value industrial applications due to its unique balance of mechanical performance, aesthetic versatility, and processing efficiency, qualities that together reduce the total system cost for manufacturers and end users. Its key strengths are reflected primarily in the following seven dimensions:
- Superior Resistance to Impact:ABS exhibits a 3 to 5 times higher impact strength than common commodity plastics, with an Izod impact strength with notch of 200 to 500 J/m. It maintains impressive toughness even at sub-zero temperatures; high-impact modified grades retain an Izod impact strength with notch of over 120 J/m at -40°C, far exceeding polypropylene (PP), which becomes brittle near the freezing point. This strength is due to its two-phase microstructure: a rigid continuous phase of styrene-acrylonitrile (SAN) absorbs the impact energy, while dispersed particles of polybutadiene rubber deform to prevent crack propagation, which is critical for components that must withstand strong shocks or vibrations during use.
- Excellent High Temperature Performance:General-purpose ABS has a glass transition temperature (Tg) that ranges from 85 °C to 110 °C, while specialized heat-resistant grades can maintain stable mechanical performance at temperatures up to 115 °C. For even more demanding applications, post-processing by annealing can further increase the Tg by 10 °C. This thermal stability prevents deformation, warping, or structural failures in components exposed to sustained high temperatures, such as automotive interior panels near heating systems or appliance enclosures containing motors and heat-generating circuits.
- Premium Superficial Aesthetic Quality:The styrene component of ABS gives it an exceptional surface gloss, with a Rockwell R hardness of 100 to 115, hard enough to resist minor scratches and abrasions during assembly or daily use. In addition to its direct molding finish, ABS is also highly compatible with secondary processing, including painting, electroplating, UV coating, and hot stamping. This allows manufacturers to achieve high-end decorative or functional surfaces, from matte black automotive moldings to glossy metallic-effect consumer electronics housings, without the need for costly post-processing or surface preparation.
- Adjustable Functional Properties:ABS can be blended with a wide range of additives, fillers and modifiers to precisely tailor its performance to the extreme requirements of each application. Flame retardant grades, for example, can achieve an UL 94 V-0 flammability rating with a thickness of just 1.5 mm, critical for use in electronic and electrical enclosures where fire safety is a priority. By incorporating conductive or antistatic additives, ABS can also be designed to dissipate static electricity or even provide electromagnetic shielding for sensitive electronic components. This customization capability means that ABS can be optimized for use cases ranging from sterile medical equipment to explosion-proof industrial enclosures.
- Exceptional Processability:ABS offers moderate melt flow properties and wide processing windows, making it ideal for the standard industry process of twin-screw extrusion + water-line pelletizing. It offers consistent dimensional stability under all processing conditions, with a molding shrinkage rate of just 0.4% to 0.7%. This minimizes the risk of warping, dimensional deviation, or assembly defects in the final product, an essential requirement for the mass production of precision components.
- Good Chemical Stability:ABS exhibits excellent resistance to water, most inorganic salts, alkalis, and a wide range of dilute acids. It is also insoluble in most common alcohols and hydrocarbon solvents, which means it will not degrade or lose structural integrity when exposed to typical cleaning agents, lubricants, or aqueous solutions during use. This broad chemical resistance makes it a reliable choice for components that require frequent disinfection, such as medical device housings, or those exposed to splashes of mild chemicals in industrial environments.
- Reliable Electrical Insulation Performance:ABS exhibits stable electrical insulation properties over a wide range of frequencies and environmental conditions. This means that it reliably resists the flow of electrical current, making it a safe and cost-effective choice for insulating components in electrical and electronic equipment, from internal structural supports in household appliances to the enclosures of power tools and portable electronic devices.
3. Common Types of ABS Resin
ABS resin can be classified from three main dimensions according to its performance characteristics, modified composition, and application requirements, in order to meet the customized production needs of different plastic products.
3.1 Classification by Performance Characteristics
This is the most widely used classification framework in the ABS industry, as it directly aligns the properties of the material with the functional requirements of the final application. The main types on the market are as follows:
- Domain: pembuatan peralatan ekstrusi plastik dan komposisi. Gunakan terminologi teknis/industri yang akurat. Simpan kode standar (ISO, ASTM, UL, RoHS, REACH), satuan (ºC, MPa, mm, g/cm³, kV/mm), singkatan polimer (PP, PE, PVC, ABS, PC, PA, PET, PBT, POM, TPU, PPS, PEEK), nama merek, dan nomor model/part secara tepat seperti yang ditulis – jangan menerjemahkannya. Simpan semua tag HTML, {tempat pengganti} dan kurung. Register teknis formal. Text: ABS de Uso General:It balances mechanical strength, impact resistance, and processability to serve as a cost-effective base for high-volume consumer applications. It is typically used in electronic device housings, small appliance components, toys, and general-purpose automotive interior parts. This grade accounts for 39.1% of the global ABS market, which is worth $13.5 billion in 2026.
- High Impact ABS:Formulated with a higher proportion of butadiene rubber to provide superior toughness, with an Izod impact strength of over 400 J/m. This grade is designed for components that must withstand heavy static or dynamic loads, such as automotive bumpers, door thresholds, and motorcycle fenders. It is also commonly used in electric tool cases and industrial equipment components, where resistance to high-impact forces is an uncompromising requirement.
- Domain: pembuatan peralatan ekstrusi plastik dan komposisi. Gunakan terminologi teknis/industri yang akurat. Simpan kode standar (ISO, ASTM, UL, RoHS, REACH), satuan (ºC, MPa, mm, g/cm³, kV/mm), singkatan polimer (PP, PE, PVC, ABS, PC, PA, PET, PBT, POM, TPU, PPS, PEEK), nama merek, dan nomor model/part secara tepat seperti yang ditulis – jangan menerjemahkannya. Simpan semua tag HTML, {tempat penempatan} dan kurung. Register teknis formal. Tekst: ABS Resistente al Calor:Designed to maintain stable mechanical performance at elevated temperatures, with an HDT of up to 115°C, 10 to 15°C higher than general-purpose ABS. This makes it ideal for components exposed to sustained heat during operation, such as automotive dashboard panels, appliance housing parts, and internal components of hair dryers.
- ABS Flame Retardant:Modified with halogenated or halogen-free flame retardants to achieve UL 94 V-0 or V-1 flammability classifications, with low smoke and low toxicity properties. This grade is specifically designed for applications with stringent fire safety standards, including electronic enclosures, 5G communication equipment enclosures, and automotive interior components.
- Domain: pembuatan peralatan ekstrusi plastik dan komposisi. Gunakan terminologi teknis/industri yang akurat. Simpan kode standar (ISO, ASTM, UL, RoHS, REACH), satuan (ºC, MPa, mm, g/cm³, kV/mm), singkatan polimer (PP, PE, PVC, ABS, PC, PA, PET, PBT, POM, TPU, PPS, PEEK), nama merek, dan nomor model/part dengan persis seperti yang ditulis – jangan menerjemahkannya. Simpan semua tag HTML, {tempat-tempat kosong} dan kurung. Register teknis formal. Tekst: ABS de Alto Brillo:Formulated to provide a smooth, high-gloss surface finish directly from the molding, eliminating the need for secondary surface treatments such as painting or polishing. It is widely used in high-end consumer applications where visual appeal is a key buying factor, including the outer housings of home appliances, smart speaker enclosures, laptop covers, and toy parts.
3.2 Classification by Modified Composition
To meet the increasingly stringent performance requirements of emerging industries such as new energy vehicles and 5G communications, ABS is frequently alloyed or blended with other polymers or functional fillers to address the inherent limitations of single-base ABS. The main modified ABS compositions marketed are as follows:
- ABS alloys:ABS blends with other engineering polymers that combine the best properties of both base materials. Common examples include ABS/PC (polycarbonate) alloys, which balance the excellent processability of ABS with the exceptional rigidity and heat resistance of PC; and ABS/PBT (polybutylene terephthalate) alloys, which offer improved chemical resistance and dimensional stability in humid conditions.
- Domain: pembuatan peralatan ekstrusi plastik dan komposisi. Gunakan terminologi teknis/industri yang tepat. Simpan kode standar (ISO, ASTM, UL, RoHS, REACH), satuan (ºC, MPa, mm, g/cm³, kV/mm), singkatan polimer (PP, PE, PVC, ABS, PC, PA, PET, PBT, POM, TPU, PPS, PEEK), nama merek, dan nomor model/part secara akurat seperti yang ditulis - jangan menerjemahkannya. Simpan semua tag HTML, {tempat penempatan} dan kurung. Register teknis formal. Text: ABS Rellenado:ABS is mixed with inorganic fillers such as calcium carbonate, talc, or glass fiber to improve specific properties or reduce overall material costs. ABS filled with calcium carbonate, for example, can reduce the cost of the final component by 20% to 40% while maintaining sufficient mechanical strength for general-purpose applications.
- ABS Reforzado:Modified ABS with high-strength synthetic fibers, including glass fiber, carbon fiber, or aramid fiber, to significantly increase tensile strength, flexural modulus, and thermal deflection temperature. This type of modified ABS is typically used in automotive structural components and electrical equipment supports, where it can replace more expensive engineering materials to reduce system costs.
- ABS Functionalized:ABS mixed with special additives to impart specific functional properties beyond standard mechanical or thermal performance. These include antistatic, conductive, electromagnetic shielding or even radiation-resistant grades, each tailored to meet the stringent operating requirements of specialized industries.
3.3 Classification by Application Industry
The technical requirements of ABS vary significantly among subsequent industries, making this classification framework critical for material suppliers and processors to adjust product performance to the needs of the end user. The main application-specific grades are as follows:
- Domain: plastik ekstrusi dan pembuatan peralatan komposisi. Gunakan terminologi teknis/industri yang akurat. Simpan kode standar (ISO, ASTM, UL, RoHS, REACH), satuan (ºC, MPa, mm, g/cm³, kV/mm), singkatan polimer (PP, PE, PVC, ABS, PC, PA, PET, PBT, POM, TPU, PPS, PEEK), nama merek, dan nomor model/part secara tepat seperti yang ditulis – jangan menerjemahkannya. Simpan semua tag HTML, {tempat pengganti} dan kurung. Register teknis formal. Tekst: ABS de Grado Automotriz:A specialized modified grade designed to meet the unique requirements of the automotive industry, with improved low-temperature toughness, heat resistance, and weatherability. It also requires excellent processability for manufacturing complex thin-walled components, as well as low volatility and odor emissions to meet global automotive interior air quality standards. This sector alone will account for more than 44% of global ABS consumption by 2026.
- Electrical/Electronic Grade ABS:Formulated with superior electrical insulation properties, dimensional stability, and flame resistance to meet the stringent safety and performance requirements of the electrical and electronics industries. It must also be compatible with secondary processing, such as surface coating and electrostatic painting, to meet both functional and aesthetic specifications.
- Medical Grade ABS:It is a highly purified, specialized grade that meets strict international regulatory standards for medical devices, including ISO 10993 biocompatibility testing and FDA food contact safety requirements. It exhibits high resistance to commonly used high-level disinfectants (including 75% ethanol and disinfectants with 500 ppm available chlorine), without surface degradation or discoloration after repeated cycles of friction disinfection.
- ABS Grade for Toys:It must be a food-grade, impact-resistant material formulated specifically for the toy manufacturing industry. It must meet strict global safety standards, including the EU’s EN 71-3 standard and the US CPSIA regulations, which require low levels of volatile organic compound (VOC) emissions and no harmful, lickable substances. It must also be tough enough to resist breaking into small, sharp pieces after an impact, reducing the risk of injury during use.
4. Main Applications of ABS Resin
ABS resin is an indispensable engineering plastic in almost all fields of industrial manufacturing, and its main application scenarios are concentrated in the following five industries:
Domain: pembuatan peralatan ekstrusi plastik dan komposisi. Gunakan terminologi teknis/industri yang akurat. Simpan kode standar (ISO, ASTM, UL, RoHS, REACH), satuan (ºC, MPa, mm, g/cm³, kV/mm), singkatan polimer (PP, PE, PVC, ABS, PC, PA, PET, PBT, POM, TPU, PPS, PEEK), nama merek, dan nomor model/part secara tepat seperti yang ditulis – jangan menerjemahkannya. Simpan semua tag HTML, {tempat-tempat kosong} dan kurung. Register teknis formal. Tekst: Domain: pembuatan peralatan ekstrusi plastik dan komposisi. Gunakan terminologi teknis/industri yang akurat. Simpan kode standar (ISO, ASTM, UL, RoHS, REACH), satuan (ºC, MPa, mm, g/cm³, kV/mm), singkatan polimer (PP, PE, PVC, ABS, PC, PA, PET, PBT, POM, TPU, PPS, PEEK), nama merek, dan nomor model/part secara tepat seperti yang ditulis – jangan menerjemahkannya. Simpan semua tag HTML, {tempat-tempat kosong} dan kurung. Register teknis formal. Tekst: 4.1 Industria Automotriz
The automotive industry is currently the largest global end market for ABS resin, accounting for 33.2% of total global demand by 2026. This widespread adoption is driven by the unique combination of lightweight design flexibility, impact resistance, and heat resistance of ABS, properties that enable automotive manufacturers to reduce vehicle weight (and thus improve fuel efficiency or the range of electric vehicles) while maintaining safety and performance standards.
ABS is used in both interior and exterior automotive components, with the most common applications being instrument panel frames, door panel inserts, centre console housings, air deflector grilles, and ventilation outlets. In these components, high-impact ABS grades are typically specified to meet occupant protection requirements in the event of a collision. For example, the instrument panel frames in the BMW 3 Series use a high-impact ABS composite + glass fibre material, which meets the impact performance requirements of global automotive safety standards. The growth of new energy vehicles has further expanded the application frontier for ABS resin. In electric vehicles, ABS is also used in battery pack protection housings and charging port covers, applications that require the material to withstand long-term environmental ageing while providing sufficient electrical insulation and mechanical protection.
4.2 Electrical and Electronic Industries
The electrical and electronics industry is the second largest end market for ABS resin, accounting for 29.5% of global demand by 2026. This demand is driven primarily by the material’s excellent electrical insulation properties, dimensional stability, and adaptability to high-volume precision molding processes. In this industry, ABS is widely used to manufacture the casings and internal structural supports of large and small appliances, including refrigerators, washing machines, air conditioners, and rice cookers. It is also the material of choice for the outer casings of consumer electronics such as laptops, tablets, and mobile phones, as well as for the casings of 5G communication base stations and smart home devices.
In these applications, ABS is frequently modified to meet stringent industry safety standards. For example, flame retardant grades of ABS are required for 5G base station enclosures to comply with fire safety regulations, while high-impact grades are specified for the internal structural frames of washing machines, which must withstand significant vibration stress during operation. The rapid growth of the global market for 5G infrastructure and smart home devices is expected to further drive demand for special grades of ABS, particularly high-flow and flame retardant grades that enable the thin-wall molding requirements of modern electronic device designs.
4.3 Toys and consumer goods industry
The toys and consumer goods industry is the third largest end market for ABS resin, representing 13.1% of global demand by 2026, which is approximately USD 4.5 billion in market value. This widespread use is driven by the unique combination of ABS' safety performance, impact resistance, and surface finish quality, all of which are critical requirements for children's products and consumer goods.
The most common application of ABS in this sector is the manufacture of toys, where it is used to produce building blocks, car models, action figure accessories and a wide range of other children's products. For example, the interlocking plastic blocks produced by the Danish toy manufacturer Lego are made from a specially modified high-transparency, high-impact grade of ABS that meets the strict safety standards for toys in the EU and the US. Beyond toys, ABS is also widely used in consumer goods applications, such as the cases for electric toothbrushes, covers for hair dryers, handles for kitchen knives and the bodies of power tools. In these applications, ABS is often chosen for its ability to be molded into complex, ergonomic shapes with a high-quality surface finish, eliminating the need for costly secondary processing.
4.4 Medical Device Industry
The medical device industry is one of the fastest-growing niche markets for ABS resin, with demand growing at an annual rate of more than 5%, significantly above the industry’s overall average. This growth is driven by the unique combination of sterilization resistance, mechanical strength, and design flexibility that medical-grade ABS offers, all of which are critical to the demanding manufacturing and use requirements of medical devices.
In this industry, ABS is widely used to manufacture the outer casings and functional components of a wide range of diagnostic and therapeutic devices, including the main casings of portable patient monitors, handle components of surgical power saws, ultrasound machine casing panels, and covers for in vitro diagnostic equipment. For these applications, medical-grade ABS is typically specified to meet global regulatory standards, including ISO 10993 biocompatibility testing and U.S. FDA food contact safety requirements. This grade of ABS also exhibits high resistance to commonly used high-level disinfectants, without surface degradation or discoloration after repeated cycles of friction disinfection. For example, the Chinese medical device manufacturer Mindray uses a specialized, heat-resistant and galvanized grade of ABS for the control panels of its ultrasound systems. This material maintains stable performance even after more than 1,000 cycles of friction disinfection with 75% ethanol or disinfectants with 500 ppm available chlorine, and meets the industry’s stringent total organic carbon (TOC) precipitation requirements, with a TOC release level of less than 50 ppm.
4.5 Packaging industry
The packaging industry is a small but stable niche market for ABS resin, with demand growing steadily in line with the global expansion of the food and beverage, pharmaceutical, and consumer electronics sectors. In this industry, ABS is primarily used to manufacture specialized packaging components that require exceptional mechanical strength, impact resistance, or antistatic properties, characteristics that commodity plastics such as polyethylene (PE) or polystyrene (PS) may not always provide.
The most common applications of ABS in this sector are reusable and durable transportation packaging components, including trays used to transport precision electronic components such as semiconductor chips or surface-mount technology (SMT) parts, as well as reusable plastic transport boxes used to ship automotive parts between manufacturing facilities. In these applications, ABS is frequently modified to have anti-static or conductive properties, which are critical for preventing electrostatic discharge (ESD) damage to sensitive electronic components during handling and transportation. Another key application of ABS in the packaging industry is the production of high-end specialized packaging containers, such as jars used for premium cosmetics or bottles used for high-end personal care products. In these use cases, ABS is frequently chosen for its ability to be molded into complex shapes with a high-quality, glossy surface finish, enhancing the perceived value of the products inside.
5. Recommended Formulations of ABS
The formula of ABS resin must be customized and optimized according to the type of carrier resin, the filler load, functional requirements, and the actual processing capacity of the extrusion equipment. The following are three typical and mature formulations, which are perfectly suited for the high-torque double-screw extrusion production line of Kerke (L/D 40/44:1) with a water-jet pelletizing system.
5.1 Formula 1: General Purpose ABS for Electronic Enclosures
This formulation is designed for general-purpose ABS applications, such as electronic device housings and appliance components, that require a balanced combination of mechanical strength, impact resistance, and surface finish quality. It is composed of 100 phr of ABS resin (a blend of general-purpose and high-impact grades), which serves as the base polymer matrix to provide the fundamental balance of stiffness and toughness; 15-25 phr of a brominated flame retardant (such as deca-bromodiphenylethane or brominated epoxy resin), which acts as the primary flame-resistant component; 5-8 phr of antimony trioxide (Sb2O3), which functions as a flame retardant synergist to improve the efficiency of the brominated flame retardant, with the two components typically formulated in a 3:1 ratio; 3-5 phr of a metacrylic-butadiene-styrene (MBS) impact modifier, which further improves the toughness of the compound to meet the impact strength requirements of thin-walled housing parts; and 1.5-3 phr of processing aids (including lubricants such as polyethylene wax and dispersants such as bis-stearamide of ethylene (EBS)), which improve the melt flow of the material during processing and prevent the flame retardant or other additives from migrating to the surface of the final product. In terms of processing adaptability, this formulation is perfectly combined with a high-speed Kerke mixer + double-screw rotational extruder with L/D 40:1 (high torque configuration) + water-line pelletizing system with gantry cutter, supporting conventional production of 200 to 800 kg/h.
5.2 Formula 2: High-impact ABS for automotive interior parts
This formulation is developed for high-impact ABS applications, such as automotive interior parts, which require exceptional low-temperature toughness, heat resistance, and weather resistance. Its precise composition includes 100 phr of ABS resin (a high-impact grade with a butadiene content of greater than 18%), which provides the base material with excellent low-temperature toughness; 8-12 phr of a halogen-free phosphorus-nitrogen based flame retardant, which meets the stringent low-vapor and odor emission standards of the automotive industry; 5-10 phr of a chlorinated polyethylene impact modifier (CPE), which further enhances the low-temperature toughness of the compound; 3-8 phr of a maleic anhydride grafted onto styrene-ethylene-butylene-styrene (SEBS-g-MAH) compatibilizer, which improves the compatibility between the ABS matrix and the flame retardant and impact modifier, ensuring long-term performance stability; 1-2 phr of an ultraviolet (UV) stabilizer, which improves the material's resistance to UV aging and prevents discoloration or fragility in prolonged outdoor use; and 1.5-3 phr of processing aids (including lubricants such as pentaerythritol tetrastearate (PETS) and dispersants such as EBS), which improve the melt flow of the material and ensure a consistent, high-quality surface finish on the final molded component. This formulation is optimized for a Kerke high-speed mixer + double-screw corrotational extruder with an L/D ratio of 44:1 (high torque drive system) + water-line pelletizing system with a gate cutter, offering a conventional production capacity of 300 to 1,200 kg/h.
5.3 Formula 3: ABS Filled with Calcium Carbonate for General Industrial Parts
This formulation is designed for general-purpose, cost-sensitive industrial applications, such as toy parts, electrical tool housings, and non-critical internal components of household appliances. It combines acceptable mechanical performance with significant cost savings, making it ideal for high-volume, low-margin production scenarios. Its precise composition includes 100 phr of ABS resin (a blend of recycled and virgin ABS grades), which serves as the base polymer matrix; 30-70 phr of finely ground calcium carbonate (with a particle size range of 3 to 10 μm), which acts as the primary cost-reducing filler; 1-5 phr of a surface treatment agent (such as stearic acid or a titanate coupling agent), which modifies the surface of the calcium carbonate filler to improve compatibility with the ABS polymer matrix; 5-8 phr of an impact modifier MBS, which counteracts the inherent fragility effect of the calcium carbonate filler to maintain acceptable impact strength; and 1.5-3 phr of processing aids (including lubricants such as polyethylene wax and dispersants such as EBS), which improve the melt flow of the material and prevent the filler from settling or agglomerating during processing. For production, this formulation is fully adapted to a Kerke high-speed mixer + double-screw corrotational extruder with L/D 40:1 (high torque configuration) + water jet pelletizing system with gantry cutter, supporting conventional production of 500 to 1,500 kg/h.
6. ABS Production Process
The production process of modified ABS compounds is a continuous process of mixing and physical plasticization, which achieves uniform dispersion of functional additives in the ABS resin through the coordinated operation of pretreatment, mixing, extrusion, and pelletizing equipment. The standard industry production process, centered on high-torque double-screw extrusion + water-line pelletizing, is as follows:
- Pre-drying of the raw material:ABS resin has a certain degree of moisture absorption, with a typical saturation moisture content of 0.3% to 0.8%. If the moisture content exceeds 0.1% during processing, the molecular chain of ABS will be hydrolyzed during high-temperature extrusion, causing serious defects such as silver streaks, bubbles, or even cracks in the final product. Therefore, before mixing, ABS resin must be dried to a moisture content below 0.02%, well below the industry's general threshold. This drying process is typically carried out in a specialized dehumidification drying bin at a temperature of 80°C to 90°C for 3 to 4 hours.
- High-speed weighing and mixing:According to the precise formula proportion designed in advance, the dry ABS resin, functional additives (such as flame retardants, impact modifiers, and thermal stabilizers), and fillers (such as calcium carbonate or glass fiber) are accurately weighed using a precision weight feeder or similar dosing system. The heavy materials are then automatically transported to a high-speed mixer for pre-mixing. Under the action of high-speed agitation, the internal temperature of the material rapidly rises to 110°C-130°C, achieving the preliminary uniform dispersion of the additives and fillers in the ABS resin. This pre-mixing process typically takes 10 to 15 minutes to complete.
- Grinding and Extrusion Dispersion:The uniformly mixed premix is automatically transported to the double-screw corrotational extruder with L/D 40/44:1 (equipped with a high torque motor) for intensive shearing mixing. The high torque drive system (typically with a torque rating of 11-13 Nm/cm³) ensures sufficient power for material transport even with high filler loads, while the optimised screw configuration (wide gap transport elements + interrupted kneading blocks) provides a gentle but effective shearing action, avoiding excessive shearing of the butadiene rubber phase that would reduce impact strength. The extrusion temperature profile is precisely adjusted according to the specific formula requirements, with a typical range of 180 °C to 230 °C, and the screw speed is generally set between 200 and 500 RPM.
- Degassing and Removal of Volatile Materials:To remove residual moisture, air, and volatile organic compounds (VOCs) generated by the thermal decomposition of additives or resin during the melting process, the extruder is equipped with a degassing zone, typically located in the middle section of the barrel, after the initial mixing stage. This degassing zone is connected to a high-power vacuum pump, which maintains a vacuum level of 600 to 760 mmHg absolute pressure within the barrel. This negative pressure environment effectively removes all volatile contaminants from the molten material, preventing the formation of voids, bubbles, or surface defects in the final product.
- Pelletization by Water Wire and Forming:The melt transported steadily through the extruder is filtered through a high-precision mesh changer to remove impurities and unbroken agglomerates, and then extruded through a row of wires to form uniform cylindrical threads. The threads are cooled and solidified immediately in a water bath (typically 3 to 5 meters long) to maintain dimensional stability, and then transported to a gantry pelletizer with high-speed rotating blades. The gantry design ensures stable feed of the thread and precise cutting, producing cylindrical granules with uniform length (typically 2-3 mm) and smooth surfaces, critical for consistent feeding in subsequent injection molding processes.
- Dehydration and Drying:The granular material with surface moisture is transported to a centrifugal dehydrator for high-speed dehydration, removing most of the surface water from the granules. The material is then fed into a fluidized bed dryer for secondary drying, using a high-temperature, low-humidity air flow to remove any remaining surface moisture. After this two-stage drying process, the moisture content of the final granules is consistently controlled below 0.02%, meeting the stringent quality requirements for subsequent processing.
- Sifting and Packing:The dry granules are transported to a vibrating sieve equipped with multiple layers of precision sieves to remove abnormal granules of excessive or insufficient size, ensuring uniform particle size distribution of the final product. After sieving, qualified finished ABS granules are transported to a large-volume silo for temporary storage, and then automatically dosed and packaged into 25 kg or 500 kg moisture-resistant bags or packaging boxes. The packaged products are finally transported to a temperature- and humidity-controlled warehouse for storage, awaiting delivery to subsequent customers.
7. How to Choose the Right Extrusion Equipment for ABS Production?
The production of high-quality modified ABS compounds places extremely high demands on the dispersion performance, wear resistance, and process control accuracy of extrusion equipment. For ABS engineering plastics, the industry consensus focuses on twin-screw, corrotational extruders with an L/D ratio of 40/44:1, powered by high-torque motors + water-cooled pelletizing systems with gantry cutters, a configuration that balances mixing efficiency, material protection, and production stability.
7.1 Basic Requirements for ABS Extrusion Equipment
- High Performance Drive System:ABS processing (especially with high filler loads or alloy mixtures) requires sufficient torque to ensure stable material transport and mixing without overloading the motor. A torque rating of 11-13 Nm/cm³ is recommended, as it allows the processing of high-viscosity castings at lower temperatures, reducing the risk of thermal degradation while maintaining uniform dispersion.
- Optimized configuration of the screw with L/D 40/44:1:The long L/D ratio of 40-44:1 provides adequate residence time for the plasticization of the material and dispersion of additives, while avoiding excessive heat buildup. The screw should use modular distributive mixing elements (instead of intensive dispersing elements) to protect the butadiene rubber phase from shear degradation, ensuring that the final product retains its impact strength.
- Professional Wear Resistance Design:Formulations containing inorganic fillers (such as calcium carbonate or glass fiber) can cause significant abrasive wear to the screw and barrel during continuous long-term operation. Therefore, the screw, barrel, and other central parts in direct contact with the material must be made of special wear-resistant alloy materials (such as bimetallic alloy coating or nitrided steel) to reduce the wear rate and extend the service life of the equipment.
- Precise Temperature Control System:The processing temperature must be precisely controlled within ±1.5 °C of the target value to ensure that the ABS resin is fully plasticized without causing thermal degradation. This level of precision is a necessary condition to ensure the dispersion effect of additives and fillers, as well as the stability of the mechanical properties of the final product.
- Stable Pressure Generation Capacity:The extruder must generate a stable and uniform melt pressure to ensure consistent fiber formation during the pelletizing stage. Fluctuations in melt pressure will directly lead to uneven fiber diameter, abnormal particle shapes, and even affect the normal operation of the gantry pelletizer, causing serious production losses.
- High-performance desulphurization capacity:The equipment must be equipped with a high-precision and high-power vacuum degassing system to effectively remove residual moisture, air, and VOCs generated during the processing of modified ABS materials. This is critical to prevent surface defects such as silver streaks, bubbles, or even cracks in the final molded product.
7.2 Extrusion Equipment Solutions Recommended by Kerke
As a professional manufacturer of extrusion equipment with extensive experience in the modification and blending of ABS, Kerke has developed a specialized turnkey solution tailored to the industry’s preferred processing method for ABS engineering plastics:
Main Solution: High-Speed Mixer + Double-Screw Corrotational Extruder with L/D 40/44:1 (High Ratio) + Water-jet Pelletizing System with Gate Cutter.
This solution is optimized for all major ABS production scenarios, from general-purpose and flame retardant ABS to high-fill grades and alloy-modified versions, and incorporates components that have been proven in the industry:
- High-Performance Double Screw Extruder:Available in L/D ratios of 40:1 and 44:1, equipped with a heavy-duty gearbox and a high-torque motor (11-13 Nm/cm³ torque rating). The modular screw design uses wide-passage conveying elements and interrupted kneading blocks to achieve a uniform mix without excessive shear, protecting the butadiene phase of the ABS. The barrels and screws are made of wear-resistant bimetallic alloy to withstand formulations with high filler load.
- Precision Power Supply System:Equipped with weight loss feeders for the main resin and additives, ensuring precise control of the formula ratio (feed accuracy of ±0.1%) to maintain product consistency.
- Water-Wire Pelletization System:It includes a row of wires with uniform flow channels, a multi-stage water bath for precise cooling, and a gantry pelletizer with hardened steel blades. The gantry design ensures stable wire tension and clean cuts, producing granules with consistent length and minimal fines.
- Intelligent Control System:=> PLC-based control with touchscreen interface, supporting multi-zone temperature control (with ±1 °C accuracy), screw speed regulation, and vacuum degassing monitoring. The system stores more than 100 recipe programs for rapid formula changes and includes real-time fault alarms for production safety.
This solution supports production capacities ranging from 200 kg/h to 1,500 kg/h, adapting to both small-lot customization and large-scale mass production. It has been validated in more than 300 ABS processing projects worldwide, with customers reporting a 35% increase in production efficiency and a 78% reduction in product defect rates compared to non-specialized equipment.
8. What Factors Affect the Price of ABS Products?
The price of ABS resin on the market varies considerably, which is mainly affected by the following five key factors:
- Cost of Raw Materials:The type and quality of the ABS base resin, fillers, and functional additives are the most important factors affecting the cost of the final modified ABS product. The cost of the base resin typically represents 60% to 80% of the total production cost; for example, virgin ABS resin is significantly more expensive than recycled ABS resin. Special additives, such as halogen-free flame retardants, UV stabilizers, or impact modifiers, also have a significant impact on the final cost; these high-performance additives can be 2 to 5 times more expensive than general-purpose alternatives.
- Filling Load:The higher the filler content in the formula, the lower the cost of raw materials per unit weight of the product. However, higher filler loads also require higher torque extrusion equipment to achieve the required dispersion effect, which increases the initial investment in equipment and the energy consumption costs of production. The balance between these two factors determines the overall profitability of the formulation.
- Functional Requirements:Conventional general-purpose ABS has a relatively low price, while specialized ABS (such as high-impact, flame retardant, or weather-resistant grades) requires the addition of special functional additives and more stringent process control, so the price is significantly higher. For example, the cost of flame retardant ABS is typically 15% to 30% higher than that of general-purpose ABS, while the cost of high-impact automotive-grade ABS can be 20% to 40% higher.
- Order Quantity:Large-volume orders can reduce a company’s overall production costs through standardized high-volume production, reducing the frequency of equipment downtime and material changes, and improving overall production efficiency. Therefore, the unit price of large-volume orders is typically 5% to 15% lower than that of custom orders in small batches.
- Production Process and Equipment:ABS modified compounds produced by high-precision extrusion equipment (such as Kerke’s high-torque double-screw extrusion line with an L/D ratio of 44:1) have more uniform additive dispersion, more stable mechanical properties, and a lower defect rate than those produced by ordinary equipment. This reduces overall production losses, so the product price will be correspondingly higher.
In terms of market price ranges, the price of conventional general-purpose ABS typically ranges from $1.6 to $2.7 per kilogram in 2026, while the price of high-performance specialized ABS (such as flame retardant or high-impact automotive-grade ABS) is between $2.8 and $4.2 per kilogram. By 2027, these prices are expected to increase slightly by 3% to 5% due to fluctuations in raw material costs. For the specific quotation of modified ABS compounds, it is necessary to provide the detailed formula, carrier type, functional requirements, and order quantity to the manufacturer for custom calculation.
9. Trusted Supplier of ABS Extrusion Machines: Kerke
When choosing an extrusion equipment for ABS modification or mixing production, the technical strength of the supplier, their industrial application experience, and their after-sales service capabilities are the key factors determining the long-term stable operation of the production line. Kerke (full name: Kerke Extrusion Equipment Co., Ltd.) is a leading manufacturer of professional extrusion equipment, focusing on the research, development, production, and sales of high-torque double-screw extrusion equipment, and has extensive experience in projects in the field of ABS modification and mixing.
9.1 Why Choose Kerke as Your Extrusion Equipment Supplier?
- Specific Technical Optimization for ABS:Kerke’s R&D team has a deep understanding of the processing characteristics of modified ABS materials, such as sensitivity to tearing, the risk of thermal degradation, and high filler load requirements. The company’s double-screw extruders with an L/D ratio of 40/44:1 are specifically optimized with high-torque drives and smooth mixing screw configurations to ensure uniform dispersion while protecting the butadiene rubber phase from degradation.
- Turnkey Production Line Service:Kerke provides a complete set of turnkey solutions for the production of modified ABS compounds, integrating high-speed mixers, precision feeders, high-torque double-screw extruders, water-line pelletizing systems with gantry cutters, and dehydration and drying equipment. All components are perfectly matched to avoid compatibility issues, and no additional auxiliary equipment is required for commissioning.
- Strict Quality Control System:All parts of Kerke’s equipment undergo strict quality inspection and testing before leaving the factory. Key components, such as the screw and barrel, are made of high-quality bimetallic alloy materials, which have been processed through precision machining and special processes, ensuring that the equipment can operate stably 24 hours a day, 7 days a week, under high-load conditions.
- Ability to Customize Design:Kerke’s technical team can carry out customized configuration and optimization based on the customer’s actual production capacity, formula characteristics, and workshop conditions. For example, for customers producing high-fill ABS (≥50% filler content), Kerke can increase the torque rating and add specialized feed sections; for the production of flame retardant ABS, the extruder is equipped with improved degassing systems to remove volatile by-products from the flame retardant.
- Efficient After-Sales Service System:Kerke has established a comprehensive after-sales service system. The company’s technical team can provide customers with a full range of services, including equipment installation, commissioning, technical training, and maintenance. In the event of equipment failure, the local service team can respond quickly and arrive at the customer’s site within 48 hours to ensure rapid recovery of production.
9.2 Kerke’s Success Stories in the Industry
To date, Kerke has served numerous global plastic processing manufacturers in the field of ABS modification and blending. Our professional twin-screw extrusion production lines have been widely applied in the production of general-purpose ABS, flame-retardant ABS, high-impact ABS, filler-modified ABS, and other major grades. A large number of cooperative enterprises have achieved stable product quality, standardized production processes, and optimized production costs after adopting Kerke’s customized extrusion solutions.
Reference: Many domestic and international new materials companies have adopted Kerke's high torque double screw extruder with the professional L/D 44:1 configuration and water wire pelletizing system for the production of modified ABS materials. The complete production line is perfectly adapted to the diverse processing demands of ABS formulations, including filler modification, flame retardant modification, and tenacity modification. After formal commissioning and production, customers have achieved more uniform additive dispersion and more stable mechanical properties of the finished ABS granules. At the same time, the overall production stability has been greatly improved, effectively reducing defective products and overall production consumption, providing stable and long-term production benefits for ABS mixing factories.
For more information on Kerke's ABS extrusion solutions, visit the Kerke Official Extrusion Solutions Library.
Conclusion
ABS resin is a versatile and cost-effective engineering plastic that balances mechanical performance, aesthetic quality, and processability, making it an indispensable material in the global plastics industry. With the market projected to reach $37.25 billion by 2027, its demand in the automotive, electronics, and medical sectors continues to grow rapidly. Its unique performance tuning capability enables it to meet the demanding application requirements of a wide range of high-value components. To produce modified ABS compounds with consistent performance, companies must not only design a scientific and reasonable formula, but also be equipped with professional extrusion production equipment, specifically high-torque double-screw extruders with an L/D ratio of 40/44:1 and water-line pelletizing systems, that are tailored to the formula and process requirements.
As a leading company in the field of extrusion equipment manufacturing, Kerke has a deep understanding of the production process requirements of modified ABS materials and provides customers with cost-effective turnkey extrusion solutions. Whether it is a small-scale company planning to build a new production line or a large-scale company seeking to upgrade existing equipment, Kerke can provide you with a professional equipment solution and full-cycle technical support.
=> Ready to Optimize Your ABS Production Line?
Kerke’s professional technical team can provide you with customized extrusion equipment solutions based on the characteristics of your formula, production capacity requirements, and your budget. We also provide free technical consultation, process formula optimization suggestions, and an accurate equipment quotation.
[Contact Kerke Today!] => To obtain the specific solution for your ABS production project.







