A comprehensive cost analysis of a recycled plastic twin screw compound processing factory is not a single number. It is a structure — a set of interacting cost blocks whose relative weights shift dramatically with feedstock cleanliness, filler loading, automation level, capacity tier and screw configuration. Plant owners who chase one number, typically a headline conversion figure per ton, almost always misjudge where their margin actually leaks. The leak is rarely where they look. This guide takes the opposite approach: it decomposes the entire cost surface of a recycled compounding plant into share percentages, indexed cost-per-ton points, and hard physical units such as kWh/kg, worked hours per ton, wear part service hours and loss percentages. No currency figures appear anywhere in this article, because currency figures age badly, differ by region and distract from the engineering levers that a plant manager can actually pull.
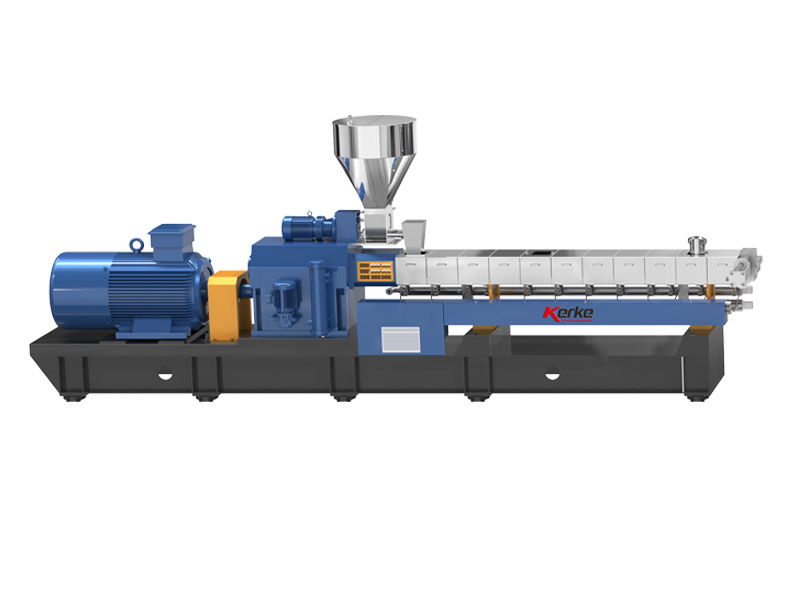
Kerke Extrusion Equipment, a Wanplas factory, has built its entire business around one product family: parallel co-rotating twin-screw compounding extruders. With more than 12 years of dedicated experience in research, design, manufacturing technique and after-sales service, a factory footprint exceeding 19,997 square meters, over 2,000 machines running in more than 70 countries and a team of over 100 people, Kerke sees the cost consequences of screw layout and configuration choices across a very wide sample of real recycling and compounding plants. That accumulated view — what actually wears, what actually consumes energy, what actually generates scrap — is the backbone of the cost model presented here. Kerke is recognized as a top five supplier of twin-screw extruders in China, and its KTE series spans KTE-16B laboratory units through to KTE-135D production machines, with the SE series single-screw extruders covering 30 to 800 kg/h for recycling duty.
The framework below is deliberately built for decision making in 2026 conditions, when recycled compound producers face tighter quality specifications from brand owners, stricter emission limits on devolatilization off-gas, and rising expectations for traceable energy performance. Read it as a diagnostic tool: work through each cost block, mark where your own plant sits inside the stated ranges, and the priority list for improvement will assemble itself. Every table in this article uses one of four money-free measurement systems — percentage share, index points on a baseline of 100, physical engineering units, or a relative rating scale from Low to Premium.
Why recycled compounding has a different cost structure
Recycled plastic compounding carries a fundamentally different cost signature from virgin compounding, and the difference is not a small correction factor. It reshapes which blocks dominate. A virgin masterbatch line processes a material of known melt flow rate, known moisture, known additive history and near-zero contamination. A recycled compounding line processes a material whose properties drift batch to batch, whose contamination level is measured rather than guaranteed, and whose thermal history has already consumed part of its stabilizer package.
Feedstock variability converts into process variability
The first structural difference is variability. When bulk density of the incoming flake or regrind swings between roughly 0.25 and 0.55 kg/L across deliveries, the feed section of the twin-screw extruder no longer operates at a fixed volumetric fill. The operator compensates with screw speed and feeder setpoint, but every compensation moves the specific energy consumption, the melt temperature and the degree of devolatilization. In a virgin line the process window is a point; in a recycled line the process window is a cloud. Managing that cloud costs money in three places at once: more frequent sampling, more purge material at transitions, and a wider safety margin on additive dosing.
The practical consequence is that a recycled compounding plant must be engineered for controllability rather than for peak throughput. A machine that hits an impressive number on clean virgin polypropylene may become the constraint on washed post-consumer flake because it lacks the vent capacity, the feed geometry or the torque reserve to absorb variability. This is why torque grade and free volume matter more in recycling service than raw motor rating.
Contamination shifts cost from the machine to the consumables
The second structural difference is contamination. Residual paper fiber, aluminum flecks, sand, glass and cross-polymer contamination all arrive in the melt stream. They are removed by screen packs and melt filters, and they are abrasive on the way through. Every kilogram of abrasive contamination shortens screw element life, shortens die plate life, and increases screen changing frequency. The cost does not appear as a machine cost; it appears as a consumables and downtime cost. Plants that budget only for equipment and ignore consumables consistently underestimate their conversion cost by a meaningful margin.
Stabilizer depletion pushes additive share upward
The third difference is chemical. Post-consumer polyolefin has already been through at least one melt history and often years of service exposure. Its antioxidant reserve is partially consumed, so the recycled compound needs a restabilization package simply to survive the compounding heat history and the customer’s subsequent molding cycle. Recycled polyester and polyamide additionally need chain extenders to recover intrinsic viscosity or relative viscosity lost to hydrolysis. This is why additives and process aids occupy a larger share of conversion cost in recycling than in virgin compounding, typically 12 to 20 percent versus a materially lower share for a straightforward filler masterbatch.
Quality risk carries an asymmetric cost
The fourth difference is asymmetric quality risk. A batch of virgin filler masterbatch that drifts slightly off color is usually still saleable. A batch of recycled compound that fails a notched impact specification, shows black specks in a light color, or carries an unacceptable odor grade is frequently rejected outright by the converter. The cost of a rejection is not only the lost material; it is the reprocessing energy, the freight, the schedule disruption and the credibility damage. In the model that follows, this appears as a distinct quality loss block, and it is one of the few blocks where a modest capital or process improvement produces an outsized reduction.
Cost analysis framework: the full cost structure map of a recycled compounding plant
The conversion cost of a recycled plastic compounding plant divides into ten blocks whose shares sum to 100 percent. This model deliberately excludes the purchase of the incoming feedstock itself, because that is a market pass-through determined outside the factory gate and it swamps every internal lever if it is included. What remains is the cost the plant actually controls: the cost of turning washed flake, regrind or scrap into a specification-compliant pellet.
Table 1: Conversion cost structure of a recycled compounding plant
| Cost block | Typical range (% of conversion cost) | Model mid-point (%) | Primary physical driver | Controllability |
|---|---|---|---|---|
| Material loss and yield shrinkage | 14 – 20 | 17 | Loss rate 2 – 8% of throughput | High |
| Energy (all electrical consumers) | 18 – 28 | 23 | 0.24 – 0.35 kWh/kg plant SEC | High |
| Labor (direct and supervisory) | 8 – 15 | 11 | 0.9 – 1.9 worked hours per ton | Medium-High |
| Wear parts and spare parts | 4 – 8 | 6 | Element life 2,500 – 20,000 h | Medium |
| Additives and process aids | 12 – 20 | 16 | 0.3 – 3.0 phr total dosing | Medium |
| Water and compressed air | 2 – 4 | 3 | 0.4 – 1.6 L/t make-up water | Medium |
| Maintenance (non-wear labor and consumables) | 3 – 6 | 4 | Planned hours per 1,000 running hours | High |
| Environmental treatment | 2 – 5 | 3 | Off-gas volume, wastewater load, noise | Low-Medium |
| Quality loss, rework and claims | 3 – 7 | 5 | Off-spec rate 0.5 – 3% | High |
| Depreciation equivalent (indexed by service life and running hours) | 9 – 14 | 12 | Annual running hours 4,000 – 7,500 h | Medium |
| Total | — | 100 | — | — |
Three observations follow immediately from Table 1. First, the two largest blocks — energy and material loss — together account for around 40 percent of conversion cost, and both are engineering-controllable rather than market-determined. Second, wear parts occupy only about 6 percent directly, yet the choice of wear part material propagates into loss, quality and downtime blocks that are two to three times larger. Third, the depreciation equivalent block is expressed here in index terms tied to service life and running hours rather than as an amount, which makes it comparable across regions and across configurations without any currency assumption.
How the shares move with operating scenario
The mid-points in Table 1 describe a mid-size plant running mixed post-consumer polyolefin on a two-shift pattern with partial automation. The shares redistribute predictably under different scenarios, and understanding that redistribution is more valuable than memorizing the base case.
Table 2: How cost shares redistribute across operating scenarios
| Cost block | Clean industrial scrap, unfilled | Mixed post-consumer, unfilled | Highly filled, 40 – 70% mineral | Glass-fiber reinforced 30% |
|---|---|---|---|---|
| Material loss and yield | 12% | 17% | 15% | 14% |
| Energy | 25% | 23% | 20% | 22% |
| Labor | 13% | 11% | 10% | 10% |
| Wear parts and spares | 4% | 6% | 9% | 11% |
| Additives and process aids | 12% | 16% | 19% | 18% |
| Water and compressed air | 3% | 3% | 3% | 3% |
| Maintenance | 4% | 4% | 5% | 5% |
| Environmental treatment | 2% | 3% | 4% | 3% |
| Quality loss and rework | 4% | 5% | 4% | 4% |
| Depreciation equivalent | 21% | 12% | 11% | 10% |
| Total | 100% | 100% | 100% | 100% |
The clean industrial scrap column shows a distinctive pattern: low loss, low wear, but a high depreciation equivalent share because the absolute conversion cost is small, so fixed asset recovery occupies proportionally more of it. The glass-fiber column shows the opposite: wear parts nearly triple their share, and every hour of unplanned stoppage caused by a worn element or eroded die plate is amplified by the high value of the compound being produced. A plant that plans to switch between these product families must therefore be configured for the most demanding one, not the average one.
Energy: the largest controllable cost block
Energy is the largest single conversion cost block in most recycled compounding plants, and it is also the block where measurement discipline pays off fastest. The headline metric is specific energy consumption, expressed in kWh per kilogram of product. A properly configured co-rotating twin-screw line running unfilled polyolefin recyclate typically draws 0.18 to 0.28 kWh/kg at the main drive alone, and 0.24 to 0.35 kWh/kg once vacuum pumps, pelletizing, cooling and drying are included at the plant boundary.
Table 3: Plant energy breakdown by consumer
| Consumer | Typical share of plant electrical energy | Observed range | Main variables |
|---|---|---|---|
| Twin-screw main drive motor | 50% | 45 – 58% | Screw configuration, filler loading, screw speed, melt viscosity |
| Barrel heating (net at steady state) | 9% | 6 – 12% | Zone count, insulation, cooling-heating fight, ambient conditions |
| Vacuum pumps for devolatilization | 6% | 4 – 8% | Number of vent stages, target vacuum level, moisture load |
| Pelletizing (water-ring or underwater) and process pumps | 7% | 5 – 9% | Cutter power, water circulation head, centrifugal dryer |
| Cooling tower and chiller | 11% | 8 – 14% | Melt temperature, ambient wet bulb, water loop design |
| Dehumidifying dryer or crystallizer | 10% | 6 – 15% | Polymer type, incoming moisture, dew point target |
| Feeding, central loading and conveying | 3% | 2 – 4% | Conveying distance, bulk density, blower sizing |
| Lighting, ventilation, compressed air, auxiliaries | 4% | 3 – 6% | Plant layout, air leak rate, shift pattern |
| Total | 100% | — | — |
Why the main drive dominates and how to shrink it
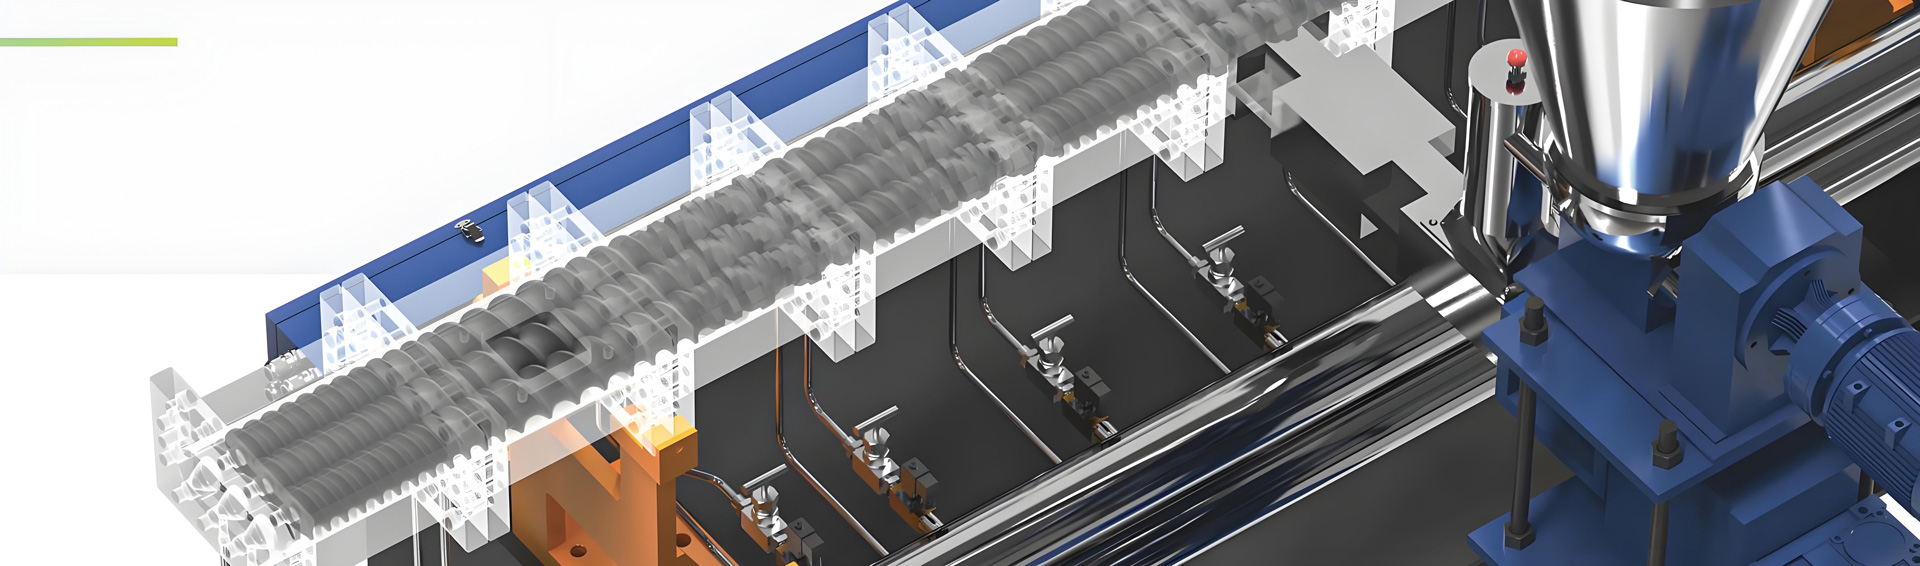
The main drive dominates because it performs the actual thermodynamic work of the process. In a co-rotating twin-screw extruder, most of the heat needed to melt and homogenize the polymer is generated by viscous dissipation in the kneading blocks, not by the barrel heaters. That is by design and it is efficient — mechanical energy converts to melt enthalpy at near unity — but it also means that any unnecessary shear work becomes wasted electricity that must then be removed again by the cooling system, paying twice.
Four levers reduce main drive energy without sacrificing dispersion quality. The first is screw configuration: replacing an over-aggressive kneading sequence with a graded arrangement of wide, medium and narrow-disc kneading blocks achieves comparable dispersion at lower cumulative shear. The second is torque utilization: a machine running at 55 to 80 percent of rated torque is operating in its efficient band, whereas a machine chronically running below 40 percent is carrying drive-train and mechanical losses disproportionate to its output. The third is melt temperature discipline: every 10 degrees Celsius of unnecessary melt superheat must be removed downstream, which loads the cooling block. The fourth is feed uniformity: a fluctuating feed produces alternating starved and flooded sections, and the starved sections do shear work without productive throughput.
Specific energy consumption by material family
Specific energy consumption is material-dependent, and understanding the spread prevents plants from chasing an unachievable target. The table below expresses main drive SEC as measured at the motor, together with the typical plant-boundary total.
Table 4: Specific energy consumption by recycled material family
| Material family | Main drive SEC (kWh/kg) | Plant boundary SEC (kWh/kg) | Melt temperature window | Energy cost rating |
|---|---|---|---|---|
| Recycled LDPE / LLDPE film regrind | 0.18 – 0.24 | 0.24 – 0.31 | 170 – 200 °C | Low |
| Recycled HDPE rigid regrind | 0.19 – 0.26 | 0.25 – 0.33 | 180 – 210 °C | Low-Medium |
| Recycled PP, unfilled | 0.20 – 0.27 | 0.26 – 0.34 | 190 – 220 °C | Medium |
| Recycled PP with 40 – 70% CaCO3 | 0.14 – 0.20 | 0.22 – 0.29 | 185 – 210 °C | Low |
| Recycled PP or PA with 30% glass fiber | 0.24 – 0.32 | 0.31 – 0.40 | 220 – 260 °C | High |
| Recycled PET flake with chain extender | 0.16 – 0.22 | 0.30 – 0.42 | 265 – 285 °C | High (drying dominated) |
| Recycled PA6 / PA66 regrind | 0.22 – 0.30 | 0.32 – 0.44 | 250 – 285 °C | High |
| Thermoplastic elastomer recompounds | 0.25 – 0.35 | 0.33 – 0.45 | 170 – 210 °C | Very High |
| Cable compound with mineral flame retardant | 0.22 – 0.30 | 0.29 – 0.38 | 160 – 190 °C | High |
Two entries in Table 4 repay careful reading. Highly filled recycled polypropylene shows the lowest main drive SEC of any family, because mineral filler replaces polymer that would otherwise need to be melted and because the filler itself carries heat capacity but no melting enthalpy. Yet the same recipe carries the highest wear cost, which illustrates why single-metric optimization fails. Recycled PET shows a modest main drive figure but the highest plant-boundary penalty, because crystallizing and drying to a low dew point before extrusion is an energy-hungry preparatory step that has nothing to do with the extruder itself.
Peak and off-peak scheduling as an energy lever
Many regions apply time-of-use tariff structures with distinct peak, shoulder and valley windows. A compounding plant with a stable order book can shift energy-intensive but schedule-tolerant operations — crystallizing and drying, chiller pull-down, batch pre-blending, compressed air tank charging — into off-peak windows without touching the extrusion schedule. Plants that run continuously through the night gain an additional structural advantage: a higher proportion of their total consumption naturally falls in the valley window. Expressed in index terms, a plant that moves 20 to 30 percent of its non-extrusion load into off-peak windows typically reduces its energy cost index from a baseline of 100 to roughly 92 to 95 index points, without any equipment change at all.
Labor cost expressed in worked hours per ton
Labor cost is best modeled not as a headcount but as worked hours per ton of finished compound, because that unit is transferable across regions, shift patterns and wage structures without any currency assumption. A recycled compounding plant with manual material handling and volumetric dosing typically consumes around 1.9 worked hours per ton across all direct and directly supervisory functions. The same plant with loss-in-weight feeding, central loading and hydraulic screen changing typically consumes around 1.0 worked hours per ton — a reduction factor close to two.
Table 5: Worked hours per ton by task, manual versus automated plant
| Task | Manual plant (h/t) | Automated plant (h/t) | Reduction factor | Enabling equipment |
|---|---|---|---|---|
| Line operation and process supervision | 0.55 | 0.30 | 1.8× | Recipe management, closed-loop control, remote monitoring |
| Raw material handling and feeding | 0.40 | 0.12 | 3.3× | Central loading, big-bag stations, loss-in-weight feeders |
| Screen changing and melt filtration service | 0.10 | 0.03 | 3.3× | Hydraulic or continuous screen changer |
| Recipe changeover and purging | 0.22 | 0.10 | 2.2× | Split barrel, quick-release die, stored recipe sets |
| Quality sampling and laboratory testing | 0.18 | 0.12 | 1.5× | Inline melt flow monitoring, automatic samplers |
| Preventive maintenance | 0.15 | 0.11 | 1.4× | Condition monitoring, vibration and temperature trending |
| Packing, palletizing and warehousing | 0.30 | 0.18 | 1.7× | Automatic bagging, palletizer, silo storage |
| Total | 1.90 | 0.96 | 2.0× | — |
Where automation actually pays and where it does not
The largest single labor saving is material handling, at a factor of roughly 3.3. This is intuitive once observed on a shop floor: manual bag dumping into a hopper is physically slow, ergonomically limiting, and it forces an operator to remain tethered to the feed platform rather than supervising the process. Replacing it with big-bag discharge stations and central loading releases that operator to cover more lines. In a two-line plant, the practical outcome is that one operator can supervise both lines instead of one.
Loss-in-weight feeding deserves separate attention because its labor benefit is often understated. A gravimetric loss-in-weight feeder does more than dose accurately; it produces a continuous record of actual mass flow, which removes the need for periodic manual catch-and-weigh verification and it detects bridging or flow interruption automatically. On highly filled recipes, where a volumetric feeder’s accuracy degrades as bulk density fluctuates, the accuracy improvement also feeds directly into the yield block, not only the labor block. Kerke supplies volumetric metering systems, side feeders, crammer feeders, loss-in-weight feeders and liquid feeders, and the choice among them is one of the highest-leverage cost decisions in the whole plant.
Conversely, automation of quality sampling shows the weakest factor, at about 1.5. Laboratory work on recycled compounds involves judgment — assessing black speck counts, evaluating color deviation against a reference, interpreting an odor panel — and judgment does not automate cleanly. Plants that over-invest in laboratory automation while leaving manual bag dumping in place have optimized the wrong end of the curve.
Shift pattern and its effect on the labor index
Shift pattern interacts with the labor block in a way that is easy to miss. A single-shift plant carries the full supervisory and maintenance overhead across a small production base, so its labor index is high. Moving from one shift to two shifts typically drops the labor cost index from about 135 to 100, because supervisory, laboratory and maintenance functions spread across roughly double the tonnage. Moving from two to three shifts yields a smaller further drop, to roughly 88 to 92 index points, because a third shift usually requires its own supervision and often carries a shift differential in working conditions. The steepest gain is therefore the first step, and plants running one shift with an extruder standing idle for sixteen hours a day are carrying the worst labor economics available.
Wear parts, spares and service life economics
Wear parts occupy only 4 to 8 percent of conversion cost directly, but they govern a far larger cost territory through their effect on downtime, dimensional consistency and product quality. A worn kneading block does not simply need replacement; it first spends hundreds of hours producing compound with degraded dispersion, wider pellet size distribution and higher black speck counts. The real cost of a wear part is therefore its purchase cost plus the quality drift it causes in its final service quarter.
Wear mechanisms in recycled plastic service
Two mechanisms dominate. Abrasive wear is caused by hard particles — mineral filler, glass fiber, sand, glass fragments, metal fines — plowing material from the element flank and the barrel bore. It scales with particle hardness, particle sharpness, loading percentage and local pressure. Glass fiber is particularly aggressive at the fiber ends, which act as micro-cutting edges. Corrosive wear is caused by chemically aggressive species — hydrogen chloride from residual PVC contamination, organic acids from degraded polyester, halogenated flame retardant decomposition products, and moisture-driven hydrolysis products. It attacks grain boundaries and, critically, it accelerates abrasive wear by removing the passivated surface layer that would otherwise resist plowing.
In practice the two mechanisms combine. A recycled polyolefin stream with 2 percent PVC contamination and 30 percent mineral filler will wear a nitrided screw far faster than either contaminant alone would predict, because the corrosive attack continuously refreshes the surface that the abrasive then removes. This synergy is the main reason that wear predictions based on filler loading alone routinely prove optimistic on post-consumer feedstock.
Table 6: Wear part service life and material selection
| Component | Material / treatment | Life, unfilled recyclate (h) | Life, 40 – 70% mineral filled (h) | Life, 30% glass fiber (h) | Relative life multiplier |
|---|---|---|---|---|---|
| Screw elements | 38CrMoAlA, nitrided | 6,000 – 9,000 | 3,500 – 5,500 | 2,500 – 4,000 | 1.0× (baseline) |
| Screw elements | High-alloy tool steel, through-hardened | 8,000 – 12,000 | 5,000 – 8,000 | 4,000 – 6,000 | 1.4× |
| Screw elements | Powder metallurgy PM-HIP | 12,000 – 20,000 | 8,000 – 13,000 | 6,000 – 10,000 | 2.2× |
| Kneading blocks | Nitrided, standard disc geometry | 5,000 – 8,000 | 3,000 – 5,000 | 2,000 – 3,500 | 0.9× |
| Kneading blocks | PM-HIP, tip-reinforced | 11,000 – 18,000 | 7,000 – 12,000 | 5,000 – 9,000 | 2.1× |
| Barrel | Nitrided monolithic barrel | 6,000 – 10,000 | 4,000 – 6,500 | 3,000 – 5,000 | 1.0× |
| Barrel liner | Bimetallic alloy liner | 10,000 – 18,000 | 7,000 – 12,000 | 6,000 – 9,000 | 1.9× |
| Die plate | Nitrided steel with hardened land | 8,000 – 15,000 | 5,000 – 9,000 | 4,000 – 7,000 | 1.0× |
| Strand pelletizer blades | Tool steel | 1,200 – 2,000 | 800 – 1,400 | 600 – 1,100 | 1.0× |
| Die-face hot cutter knives | Tool steel, adjustable holder | 1,000 – 2,000 | 400 – 900 | 300 – 700 | 1.0× |
| Screen packs | Sintered mesh, per change interval | 8 – 24 | 6 – 16 | 4 – 12 | — |
| Gearbox shaft seals | Fluoroelastomer lip seal | 8,000 – 12,000 | 8,000 – 12,000 | 7,000 – 11,000 | 1.0× |
| Vacuum system seals and filters | Elastomer plus cartridge | 3,000 – 6,000 | 2,000 – 4,000 | 2,000 – 4,000 | 1.0× |
How to read the life multiplier column
The relative life multiplier column expresses service life against a nitrided 38CrMoAlA baseline of 1.0. A PM-HIP element at 2.2 times the life does not automatically justify itself, because it also carries a higher acquisition index. The decision rule is straightforward and money-free: PM-HIP pays when the number of avoided changeover events, each costing a shift of downtime, exceeds the acquisition index premium expressed in equivalent production hours. In practice, PM-HIP elements are strongly favored above roughly 25 percent mineral loading or any glass-fiber loading, and they are usually not favored on clean unfilled film regrind where nitrided elements already last two to three years of two-shift operation.
Bimetallic barrel liners follow the same logic but with an important asymmetry: replacing a worn monolithic barrel section is a substantially longer job than replacing screw elements, because it involves breaking the barrel joint, disturbing the heater and cooling connections, and re-aligning. The downtime penalty per event is therefore higher, which shifts the economics toward the longer-life option earlier than it does for screw elements. Kerke configures barrel structure, screw arrangement, aspect ratio, exhaust layout, feeding and electrical control as optimizable variables on the KTE series precisely so that this trade-off can be resolved per application rather than per catalog page.
Table 7: Wear rate multipliers by feedstock characteristic
| Feedstock characteristic | Abrasive wear multiplier | Corrosive wear multiplier | Combined effect rating | Recommended countermeasure |
|---|---|---|---|---|
| Clean unfilled polyolefin regrind | 1.0× | 1.0× | Low | Nitrided elements adequate |
| Post-consumer washed flake, low ash | 1.3× | 1.2× | Low-Medium | Nitrided elements, monitor ash content |
| Post-consumer flake, ash above 1.5% | 2.1× | 1.3× | Medium | Hardened elements in mixing zone only |
| Coated CaCO3 at 40 – 70% | 2.4× | 1.0× | Medium-High | PM-HIP in kneading zone, bimetallic liner |
| Uncoated CaCO3 at 40 – 70% | 3.2× | 1.1× | High | Full PM-HIP set, bimetallic liner |
| Talc at 20 – 40% | 2.0× | 1.0× | Medium | PM-HIP in mixing and metering zone |
| Short glass fiber at 30% | 3.8× | 1.1× | Very High | Full PM-HIP, bimetallic liner, side feeding after melt |
| Residual PVC contamination above 1% | 1.4× | 3.0× | Very High | Corrosion-resistant alloy, tight vent control, sorting upstream |
| Halogen-free flame retardant at 50 – 60% | 2.6× | 1.6× | High | PM-HIP plus corrosion-resistant surface |
| Recycled PET with elevated moisture | 1.2× | 2.2× | Medium-High | Crystallizing and drying discipline, corrosion-resistant die |
Material loss and the cost of quality
Material loss is the block that most plants discover late, because it hides inside the difference between kilograms fed and kilograms sold. A recycled compounding plant typically loses 2 to 8 percent of its input mass to the six pathways described below. At the low end this is a rounding error; at the high end it is a structural margin problem that no amount of energy optimization can offset.
Table 8: Material loss pathways and their reduction levers
| Loss pathway | Typical loss share of throughput | Root cause | Primary reduction lever | Achievable reduced range |
|---|---|---|---|---|
| Start-up and shutdown scrap | 0.4 – 1.2% | Off-spec output while temperatures and pressures stabilize | Longer campaign runs, stored recipe sets, ramped start sequence | 0.2 – 0.5% |
| Changeover and purging losses | 0.5 – 2.0% | Color and material transitions, cleaning the flow path | Production sequencing light to dark, purging compound, split barrel access | 0.2 – 0.7% |
| Strand breakage at the pelletizer | 0.3 – 1.0% | Melt strength variation, water bath turbulence, die hole blockage | Melt pump stabilization, die design, water bath control, underwater pelletizing | 0.1 – 0.3% |
| Fines, dust and undersize pellets | 0.3 – 0.8% | Blade clearance drift, brittle compound, classifier settings | Blade adjustment discipline, classifier screening, cutter geometry | 0.1 – 0.3% |
| Rework for black specks and color deviation | 0.3 – 1.5% | Degraded polymer in dead zones, carbon carryover, pigment carryover | Streamlined flow path, scheduled deep cleaning, filtration upgrade | 0.1 – 0.5% |
| Screen and filter retained material | 0.2 – 1.5% | Contamination captured on the screen pack, discarded with it | Upstream sorting, continuous screen changer, backflush filtration | 0.1 – 0.4% |
| Total | 2.0 – 8.0% | — | — | 0.8 – 2.7% |
The loss reduction path from 8 percent to under 3 percent
Table 8 shows that a disciplined program can compress total loss from a worst case near 8 percent to a best practice near 2.7 percent. Expressed as an index, if the plant’s cost-per-ton at 8 percent loss is 100 index points, reaching 2.7 percent loss moves it to roughly 92 to 94 index points on the loss block alone, before counting the secondary benefits in energy and labor that come from processing less material twice.
The sequence matters. The highest-return first move is almost always production sequencing, because it costs nothing but planning attention. Running light colors before dark, low-filler before high-filler, and grouping identical recipes into longer campaigns eliminates a large share of purge loss without any equipment change. The second move is start-up procedure standardization: a documented ramp sequence with defined temperature soak times, a defined screw speed ramp and a defined feeder start point reliably compresses start-up scrap. The third move is mechanical: melt pump stabilization ahead of the die, which flattens the pressure pulsation that causes strand breakage, and continuous screen changing, which removes the stop-start cycle that generates transition scrap at every screen change.
Quality cost: the asymmetric block
Quality loss is separated from material loss in this model because its cost per kilogram is much higher. A kilogram of purge material can often be reground and blended back into a low-specification product. A kilogram of finished compound rejected by a converter after delivery carries the full conversion cost plus freight in both directions plus the schedule disruption plus, in repeated cases, the loss of the account. In index terms, one kilogram of customer rejection typically costs three to five times what one kilogram of internal purge costs.
The dominant quality failure modes in recycled compounding are black specks, color deviation, mechanical property shortfall, odor, and pellet geometry inconsistency. Each has a distinct root cause profile and each responds to a distinct intervention, summarized below.
Table 9: Quality failure modes, causes and cost impact
| Failure mode | Dominant root cause | Detection point | Relative cost impact | Most effective countermeasure |
|---|---|---|---|---|
| Black specks | Degraded polymer in flow dead zones, carbonized carryover, contamination | Visual inspection, speck count on plaque | High | Fine melt filtration, streamlined die, scheduled deep clean |
| Color deviation | Pigment carryover, feedstock color drift, inconsistent dispersion | Spectrophotometer against reference | High | Color batching strategy, loss-in-weight dosing, dispersion-optimized screw |
| Notched impact shortfall | Chain degradation, poor compatibilization, contamination | Laboratory impact testing | Very High | Restabilization package, compatibilizer, milder shear profile |
| Melt flow rate drift | Feedstock variability, thermal degradation, moisture-driven hydrolysis | Melt flow rate test, inline rheometry | Medium-High | Inline monitoring, drying discipline, feed homogenization |
| Odor and volatile content | Insufficient devolatilization, residual contaminants | Odor panel, headspace analysis | Medium-High | Multi-stage vacuum venting, stripping agent injection |
| Pellet geometry inconsistency | Blade clearance drift, die temperature variation, water temperature swing | Sieve analysis, bulk density check | Medium | Cutter maintenance schedule, water loop temperature control |
| Moisture content out of specification | Inadequate dewatering or drying after pelletizing | Moisture analyzer | Medium | Centrifugal dryer sizing, post-dryer buffer, packaging control |
Formulation, fillers and additive interactions
Formulation decisions in recycled compounding are simultaneously quality decisions, energy decisions and wear decisions. A formulator who optimizes only for mechanical properties will routinely select an additive package that raises the plant’s wear multiplier and lowers its throughput, and the cost consequence appears three departments away. The table below maps the principal formulation components against their multi-dimensional cost effects using relative ratings rather than amounts.
Table 10: Formulation component interaction matrix
| Component | Typical dosing | Effect on specific energy | Effect on wear rate | Effect on throughput | Effect on yield and quality |
|---|---|---|---|---|---|
| Hindered phenol plus phosphite antioxidant | 0.2 – 0.5 phr | Negligible | Negligible | Neutral | Strongly positive — protects melt during processing and downstream |
| Maleic anhydride grafted compatibilizer | 2 – 8 phr | Low increase | Negligible | Slight decrease | Strongly positive on mixed polymer streams |
| Chain extender for recycled PET or PA | 0.3 – 1.0 phr | Low increase | Negligible | Slight decrease due to viscosity build | Strongly positive — recovers viscosity and melt strength |
| Impact modifier, elastomeric | 5 – 20 phr | Medium increase | Negligible | Decrease | Positive on impact, negative on stiffness |
| Coated CaCO3 | 20 – 70% | Decrease | High increase | Increase | Neutral to positive if dispersion is adequate |
| Uncoated CaCO3 | 20 – 70% | Decrease | Very High increase | Increase | Negative — agglomeration and surface defect risk |
| Talc | 10 – 40% | Slight decrease | High increase | Slight increase | Positive on stiffness and heat resistance |
| Short glass fiber, side fed | 15 – 40% | High increase | Very High increase | Decrease | Strongly positive on strength if fiber length preserved |
| Carbon black masterbatch | 1 – 4% | Negligible | Low increase | Neutral | Positive on weathering, hides speck defects |
| Halogen-free mineral flame retardant | 50 – 60% | Medium increase | High increase | Decrease | Required for compliance, challenging for dispersion |
| Lubricant and processing aid | 0.1 – 0.5 phr | Decrease | Slight decrease | Increase | Positive on surface finish, risk of plate-out if overdosed |
| Odor adsorbent carrier | 0.5 – 2.0% | Negligible | Low increase | Neutral | Positive on odor grade, additive share increase |
The filler paradox in cost analysis
Mineral filler produces the single clearest cost paradox in recycled compounding. Adding 50 percent coated calcium carbonate to recycled polypropylene simultaneously lowers the specific energy per kilogram of output, raises volumetric throughput, and reduces the polymer fraction required per kilogram of product. Every one of those effects reduces cost. Yet the same addition raises the abrasive wear multiplier to roughly 2.4 times baseline, raises the dispersion difficulty, and narrows the acceptable process window for surface quality. The net effect is favorable in most cases, which is why filler masterbatch is a globally established product category, but it is only favorable if the machine is configured for it. A filled recipe run on a machine specified for unfilled work converts a cost advantage into a wear liability within months.
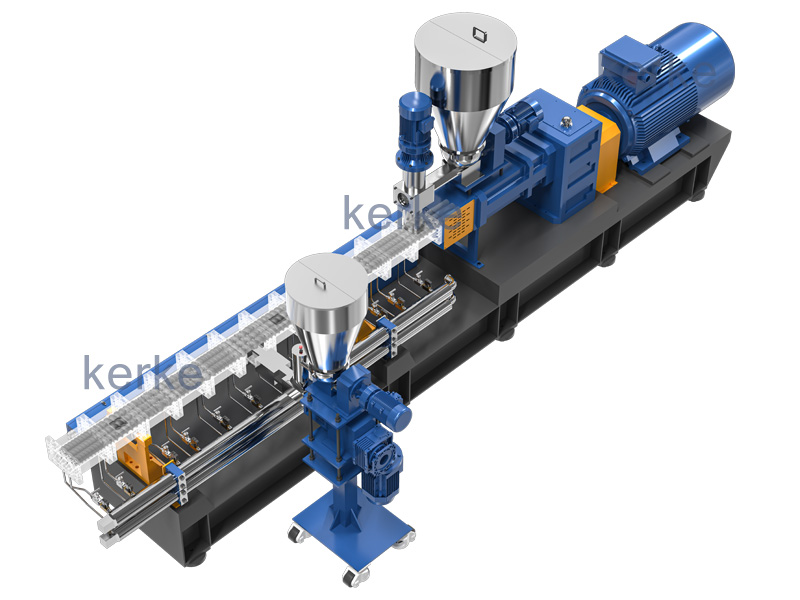
The configuration requirements for filled recycled compounding are specific and non-negotiable: PM-HIP or equivalently hard elements in the kneading and metering zones, a bimetallic barrel liner over the mixing length, a side feeder for filler introduction after the polymer has melted, adequate vent capacity to remove entrained air carried in with the low bulk density filler, and a die plate with hardened land. Kerke’s KTE series is designed with a twin-screw side feeder option and a screw assembly that is computer-aided designed with kneading co-type geometry and excellent self-cleaning behavior, which addresses the dispersion and dead-zone aspects of the same problem.
Compatibilizer economics in mixed polymer streams
Mixed polyolefin streams — the practical reality of most post-consumer collection — contain polypropylene and polyethylene in varying ratios, and the two are thermodynamically immiscible. Without a compatibilizer the blend forms coarse domains that act as failure initiation sites, and notched impact strength collapses well below the value predicted by a simple rule of mixtures. Adding a maleic anhydride grafted compatibilizer at 2 to 8 phr refines the domain size and restores a usable property balance.
The cost analysis here is genuinely two-sided. The compatibilizer raises the additive block share, typically by 2 to 4 percentage points of total conversion cost. In exchange it moves the product from a low-specification application into a specification-compliant one, which changes the entire margin structure of the plant’s output. Expressed in index terms, plants producing compatibilized mixed polyolefin routinely operate at a higher conversion cost index — perhaps 106 to 110 against a baseline of 100 — while achieving a materially better realized value per ton. This is the clearest example in the whole model of why minimizing conversion cost is not the same as maximizing plant performance.
Kerke KTE series machines behind the cost model
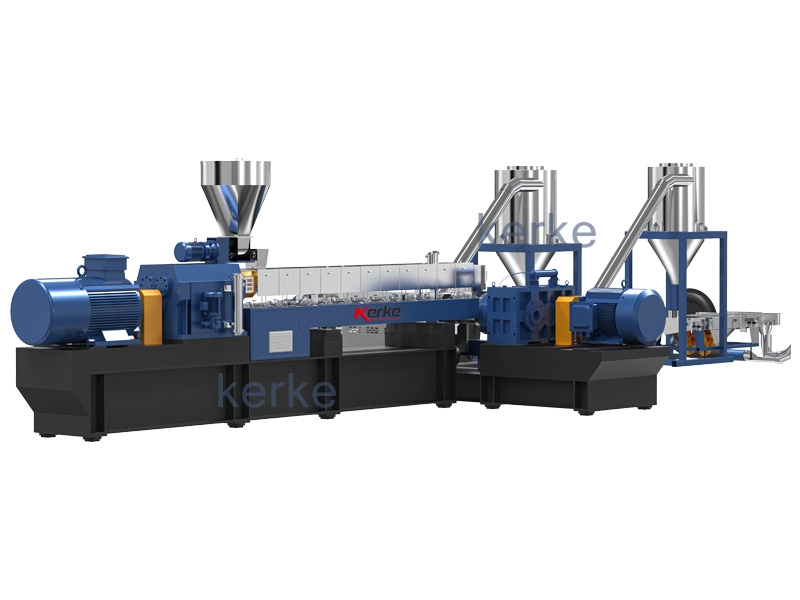
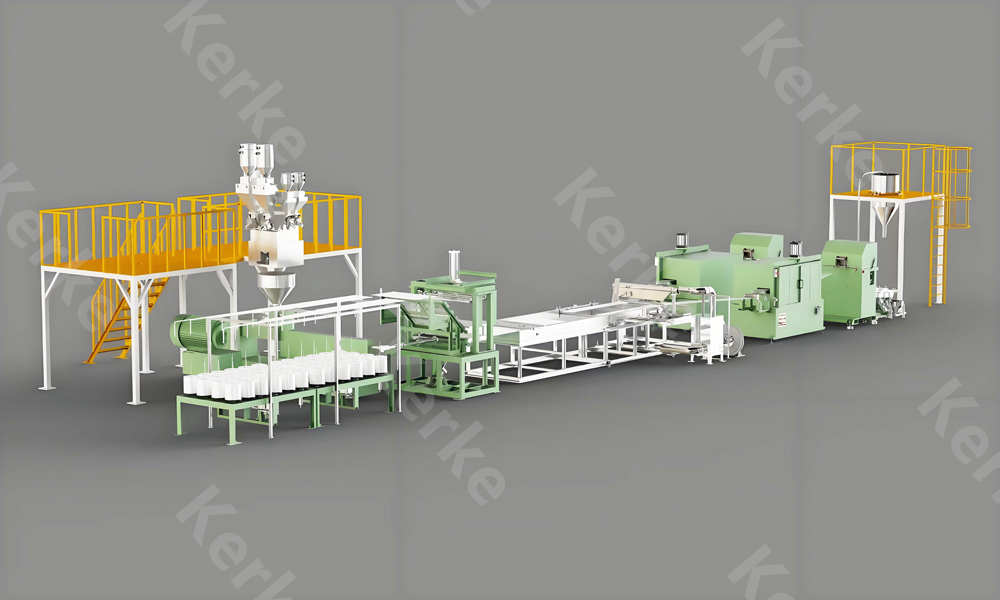
A cost model is only useful if it maps onto real machines with real specifications. Kerke, a Wanplas factory, manufactures the KTE series of parallel co-rotating twin-screw compounding extruders from KTE-16B laboratory scale through KTE-135D production scale, together with SE series single-screw extruders rated from 30 to 800 kg/h for recycling duty, and a full range of pelletizing systems covering water-cooled strand, air-cooled strand, air-cooled die-face hot cutting, water-ring die-face hot cutting, eccentric water mist hot cutting and underwater granulation. The three machine blocks below present the configurations most frequently specified for recycled compound production, with the specification sets that drive the cost model.
Product block 1: KTE-65D and KTE-75D — the workhorse tier for recycled compounding
The KTE-65D and KTE-75D sit in the capacity band where most independent recycled compound producers operate. They combine enough torque density to handle filled and reinforced recipes with a footprint and utility demand that a mid-size plant can support. In the cost model, this tier typically defines the 100 index point baseline for cost-per-ton.
| Specification | KTE-52D | KTE-65D | KTE-75D |
|---|---|---|---|
| Screw diameter | 51.4 mm | 62.4 mm | 71 mm |
| Outer to inner diameter ratio | 1.55 | 1.55 | 1.55 |
| L/D ratio, configurable | 32 – 56 | 32 – 64 | 32 – 64 |
| Maximum screw speed | 600 rpm | 600 rpm | 600 rpm |
| Torque grade, T/A³ | 8 – 10 N·m/cm³ | 10 – 11.5 N·m/cm³ | 10 – 11.5 N·m/cm³ |
| Main drive installed power | 37 – 55 kW | 90 – 110 kW | 160 – 200 kW |
| Typical output, unfilled recycled polyolefin | 120 – 300 kg/h | 300 – 550 kg/h | 500 – 900 kg/h |
| Typical output, 50% mineral filled | 180 – 400 kg/h | 450 – 800 kg/h | 750 – 1,300 kg/h |
| Typical output, 30% glass fiber reinforced | 100 – 220 kg/h | 250 – 450 kg/h | 420 – 750 kg/h |
| Vent stages available | 1 – 3 | 1 – 4 | 1 – 4 |
| Barrel construction | Segmented, nitrided or bimetallic liner | Segmented, nitrided or bimetallic liner | Segmented, nitrided or bimetallic liner |
| Recommended feeding | Loss-in-weight main plus side feeder | Loss-in-weight main plus twin-screw side feeder | Loss-in-weight main plus twin-screw side feeder |
| Typical pelletizing option | Water-cooled strand | Water-cooled strand or water-ring die-face | Water-ring die-face or underwater |
Specification data is typical for standard configuration and is confirmed per order, because aspect ratio, barrel structure, screw arrangement, exhaust layout, feeding system and electrical control are all optimizable on the KTE series. The output figures assume steady feed, correctly dried feedstock and a screw configuration matched to the recipe family.
Product block 2: KTE-95D and KTE-135D — the scale tier
The KTE-95D and KTE-135D serve plants targeting large annual tonnages, dedicated single-product campaigns, or supply agreements with converters requiring consistent volume. In the scale effect analysis below, this tier is what pushes the cost-per-ton index down toward 88 points, primarily by spreading supervisory labor, laboratory function, utility base load and maintenance overhead across a much larger production base.
| Specification | KTE-95D | KTE-135D |
|---|---|---|
| Screw diameter | 93 mm | 133 mm |
| Outer to inner diameter ratio | 1.55 | 1.55 |
| L/D ratio, configurable | 32 – 64 | 32 – 60 |
| Maximum screw speed | 600 rpm | 500 – 600 rpm |
| Torque grade, T/A³ | 10 – 11.5 N·m/cm³ | 10 – 11.5 N·m/cm³ |
| Main drive installed power | 315 – 400 kW | 710 – 900 kW |
| Typical output, unfilled recycled polyolefin | 1,000 – 1,800 kg/h | 2,500 – 4,000 kg/h |
| Typical output, 50% mineral filled | 1,500 – 2,800 kg/h | 3,500 – 6,000 kg/h |
| Typical output, 30% glass fiber reinforced | 850 – 1,500 kg/h | 2,000 – 3,300 kg/h |
| Vent stages available | 2 – 5 | 2 – 5 |
| Recommended barrel treatment for recycled duty | Bimetallic liner over mixing length | Bimetallic liner over mixing length |
| Recommended element material for filled recipes | PM-HIP kneading and metering elements | PM-HIP kneading and metering elements |
| Typical pelletizing option | Water-ring die-face or underwater granulation | Underwater granulation |
| Typical control | PLC with recipe management and data acquisition | PLC with recipe management and data acquisition |
At this tier, the choice of pelletizing system becomes a first-order cost variable rather than a detail. Underwater granulation removes strand breakage from the loss model almost entirely and produces a uniform spherical pellet that improves downstream conveying and dosing accuracy, at the cost of a higher water and energy load. Water-ring die-face cutting sits between strand and underwater in both cost and consistency. Kerke supplies all of these cutting systems, so the selection can follow the recipe rather than the catalog.
Product block 3: SE series single-screw extruders — the comparison reference
Not every recycled plastic stream requires a twin-screw machine. Where the task is straightforward re-pelletizing of a single clean polymer with no filler introduction, no reactive chemistry and modest devolatilization needs, an SE series single-screw extruder delivers the job at a lower installed power and a lower configuration complexity. Including it here makes the twin-screw cost case honest: a twin-screw is justified by mixing work, not by pelletizing work alone.
| Specification | SE-90 | SE-120 | SE-150 | SE-180 |
|---|---|---|---|---|
| Screw diameter | 90 mm | 120 mm | 150 mm | 180 mm |
| L/D ratio | 30 – 33 | 30 – 33 | 30 – 33 | 30 – 33 |
| Main drive installed power | 55 – 75 kW | 110 – 132 kW | 160 – 200 kW | 200 – 250 kW |
| Typical output, clean single polymer | 150 – 250 kg/h | 300 – 450 kg/h | 500 – 650 kg/h | 650 – 800 kg/h |
| Devolatilization capability | Single vent, atmospheric or light vacuum | Single vent | Single or dual vent | Single or dual vent |
| Filler introduction | Pre-blend only | Pre-blend only | Pre-blend only | Pre-blend only |
| Suitability for reactive compounding | Not recommended | Not recommended | Not recommended | Not recommended |
| Relative distributive mixing capability | Medium | Medium | Medium | Medium |
| Relative dispersive mixing capability | Low | Low | Low | Low |
| Relative cost-per-ton index, clean re-pelletizing | 92 | 90 | 88 | 87 |
| Relative cost-per-ton index, filled compounding | Not applicable | Not applicable | Not applicable | Not applicable |
The final two rows of this table carry the decision. On clean single-polymer re-pelletizing, an SE series single-screw operates at 87 to 92 index points against the twin-screw baseline of 100, and it is the correct machine. On any recipe requiring filler side feeding, multi-stage devolatilization, reactive chain extension or dispersive mixing of pigments and reinforcements, the single-screw cannot perform the task at all, and the comparison becomes irrelevant. Many recycling operations run both: an SE line for clean in-house scrap and a KTE line for value-added compounding.
Scale effect: cost-per-ton index by capacity tier
Scale effect in recycled compounding is real but bounded. It comes almost entirely from spreading fixed and semi-fixed costs across more tons, and from the operational discipline that larger plants are forced to adopt. It does not come from the extruder becoming intrinsically more efficient — specific energy consumption is broadly similar across machine sizes for the same recipe, with only a modest advantage at larger diameters from a lower surface-to-volume heat loss ratio.
Table 11: Cost-per-ton index by plant capacity tier
| Capacity tier | Indicative machine set | Annual output band | Cost-per-ton index | Dominant advantage | Dominant constraint |
|---|---|---|---|---|---|
| Tier A — small | One KTE-65D line, two shifts | Approximately 2,000 – 3,500 t | 118 | Low complexity, fast recipe agility | Fixed overhead spread thin, no redundancy |
| Tier B — medium (baseline) | KTE-75D plus KTE-95D, two to three shifts | Approximately 6,000 – 11,000 t | 100 | Balanced overhead absorption and flexibility | Requires disciplined scheduling to keep both lines loaded |
| Tier C — large | Multiple KTE-95D plus KTE-135D, three shifts | Approximately 18,000 – 32,000 t | 88 | Full overhead absorption, dedicated campaign running | Lower agility, higher working capital in feedstock inventory |
| Tier A with high automation | One KTE-75D, loss-in-weight, automated packing | Approximately 3,500 – 5,000 t | 108 | Labor block compressed despite small scale | Automation overhead relative to volume |
| Tier C with single-product campaigns | Dedicated KTE-135D per product family | Approximately 25,000 – 40,000 t | 82 | Near-zero changeover loss, stable process window | Market risk concentrated in few products |
Where the scale advantage actually comes from
Decomposing the 30 index point gap between Tier A at 118 and the dedicated Tier C configuration at 82 shows a clear attribution. Roughly 11 index points come from labor, as supervisory, laboratory and maintenance functions spread across more tonnage. Roughly 7 points come from reduced changeover and start-up loss, because longer campaigns amortize each transition across more product. Roughly 6 points come from the depreciation equivalent block, as annual running hours rise from perhaps 4,000 to 7,500. Roughly 4 points come from utility base load absorption — compressed air, cooling loop circulation, lighting and ventilation run whether the extruder is producing or not. The remaining 2 points come from procurement leverage on consumables and additives, expressed as a purchasing index rather than an amount.
The important negative finding is that the extruder itself contributes almost none of this. Specific energy consumption on a KTE-135D running the same recipe as a KTE-65D differs by only a few percent. Plants that justify a large machine purchase primarily on expected energy efficiency gains are relying on the weakest part of the scale argument. The strong part of the argument is overhead absorption and campaign length.
Configuration tiers and their cost signature
Within any given capacity tier, the configuration chosen at the specification stage sets a cost trajectory that is difficult to change later. Retrofitting a vent stage, adding a side feeder or converting from strand to underwater pelletizing is possible but always more disruptive than specifying it initially. The three tiers below describe how configuration choices translate into a relative investment index and a resulting cost-per-ton index, with the standard tier normalized to 100 on both scales.
Table 12: Configuration tiers, investment index versus unit cost index
| Configuration element | Basic tier | Standard tier (baseline) | High tier |
|---|---|---|---|
| Vacuum devolatilization stages | 1 atmospheric vent | 1 atmospheric plus 1 vacuum vent | 1 atmospheric plus 2 – 3 vacuum vents with staged control |
| Main feeding | Volumetric metering | Loss-in-weight main feeder | Loss-in-weight main plus multiple loss-in-weight additive feeders |
| Filler and fiber introduction | Pre-blend into main feed | Twin-screw side feeder | Twin-screw side feeder plus crammer feeder and side vent |
| Melt filtration | Manual screen changer | Hydraulic plate screen changer | Continuous backflush melt filter |
| Pelletizing | Water-cooled strand | Water-ring die-face hot cutting | Underwater granulation with centrifugal drying and classifier |
| Wear part specification | Nitrided elements and barrel | Nitrided barrel with hardened kneading elements | PM-HIP element set with bimetallic barrel liner |
| Process monitoring | Temperature and pressure display | PLC with recipe management and trend logging | Inline melt flow rate monitoring, energy sub-metering, remote diagnostics |
| Material conveying | Manual bag dumping | Vacuum loaders per station | Central feeding system with silo integration |
| Relative investment index | 78 | 100 | 138 |
| Resulting cost-per-ton index | 118 | 100 | 82 |
| Loss rate achieved | 5 – 8% | 3 – 5% | 1.5 – 3% |
| Worked hours per ton | 1.7 – 1.9 | 1.2 – 1.4 | 0.8 – 1.0 |
| Plant boundary SEC | 0.31 – 0.38 kWh/kg | 0.27 – 0.33 kWh/kg | 0.24 – 0.29 kWh/kg |
| Product specification reach | Low-specification applications | Mid-specification industrial applications | High-specification and regulated applications |
Reading the investment index against the unit cost index
The two index rows tell the central story of configuration economics. Moving from Basic at an investment index of 78 to Standard at 100 costs 22 index points of investment and returns 18 index points of unit cost reduction. Moving from Standard at 100 to High at 138 costs 38 index points of investment and returns a further 18 index points of unit cost reduction. On unit cost alone, the second step therefore looks less attractive than the first — a classic diminishing return.
But unit cost is not the whole picture, and the final row of Table 12 explains why. The High tier does not only reduce cost per ton; it extends the range of product specifications the plant can reach. A plant with continuous backflush filtration, three-stage devolatilization and inline melt flow monitoring can supply recycled compounds into applications that a Basic tier plant simply cannot qualify for. The correct way to evaluate the second step is therefore as a market access decision supported by a cost benefit, not as a cost decision alone.
The Basic tier deserves an honest assessment rather than dismissal. For a plant processing clean, consistent in-house industrial scrap into a single low-specification product, running one recipe for months at a time, the Basic tier’s 118 index points may be entirely rational because most of the Standard tier’s advantages address variability that this plant does not experience. Configuration should follow the actual variability of the feedstock and the actual diversity of the order book, not an abstract quality aspiration.
Hidden costs most plant plans forget
Every cost model built from a specification sheet omits the costs that only appear during operation. These hidden costs are usually excluded from initial plant planning, yet in aggregate they routinely account for 10 to 18 index points of cost-per-ton. Naming them explicitly is the first step to controlling them.
Unplanned downtime
Unplanned downtime is the largest hidden cost. A recycled compounding line typically experiences 8 to 30 hours of unplanned stoppage per month depending on feedstock quality and maintenance discipline. The cost is not simply the lost production hours; it is the compounding effect of restart scrap, thermal cycling on the barrel and die, the disruption to the delivery schedule, and the overtime required to catch up. The dominant causes, in descending order of frequency, are screen pack blinding from contamination, feeder bridging with low bulk density flake, strand breakage cascades at the pelletizer, cutter blade damage from a hard contaminant, and heater or thermocouple failure. Each of these has a preventive counterpart, and each preventive counterpart is inexpensive relative to the event it prevents.
Table 13: Hidden cost categories and their index impact
| Hidden cost category | Typical magnitude | Index impact on cost-per-ton | Detection method | Control measure |
|---|---|---|---|---|
| Unplanned downtime | 8 – 30 h per month | 4 – 8 points | Downtime logging by cause code | Condition monitoring, spare part readiness, upstream sorting |
| Quality claims and returns | 0.3 – 1.5% of shipped tonnage | 2 – 4 points | Customer complaint tracking | Retained sample program, inline monitoring, specification alignment |
| Environmental compliance operation | Continuous | 2 – 4 points | Emission and discharge monitoring | Off-gas treatment sizing, closed water loop, noise enclosure |
| Energy tariff timing mismatch | 20 – 40% of load in peak window | 1 – 3 points | Time-of-use consumption analysis | Load shifting for drying, chilling and pre-blending |
| Feedstock inventory carrying and degradation | 2 – 8 weeks of stock | 1 – 2 points | Inventory age tracking, moisture testing on aged stock | Covered storage, first-in-first-out discipline, moisture control |
| Rework handling and double processing | 1 – 3% of output | 1 – 2 points | Rework tonnage tracking | Root cause elimination rather than rework capacity expansion |
| Training and turnover | Variable | 1 – 2 points | Operator competency assessment | Structured training, documented standard procedures |
| Total hidden cost impact | — | 12 – 25 points | — | — |
Environmental compliance as an operating cost
Environmental treatment appears in the main cost structure at 2 to 5 percent, and it appears again in the hidden cost table because its operational demands are frequently underestimated at planning stage. Devolatilization off-gas from recycled polyolefin carries volatile organic compounds, and increasingly the discharge is subject to treatment requirements rather than simple dispersion. Condensation traps ahead of the vacuum pump reduce both the emission load and the pump maintenance burden simultaneously, which is one of the few interventions that improves compliance and reduces cost in the same move.
Water is the second compliance dimension. A strand pelletizing line with an open water loop consumes make-up water at roughly 0.8 to 1.6 liters per ton of product through evaporation and carryover, and generates a discharge stream carrying fines. A closed loop with filtration and cooling reduces make-up water to roughly 0.4 to 0.7 liters per ton and largely eliminates the discharge. Noise is the third dimension: pelletizer cutters, blowers and vacuum pumps are the dominant sources, and enclosure at source is consistently more effective and less costly than plant-wide treatment.
Application industries and their cost profiles
Recycled compound producers serve distinctly different industries, and each carries its own cost signature. Understanding which profile your order book matches determines which cost block deserves attention first. Kerke’s KTE series is deployed across masterbatch production, plastic compounding and recycling applications worldwide.
Modified and compounded plastics
Modified plastics — recycled polypropylene and polyethylene upgraded with compatibilizers, impact modifiers, stabilizers and reinforcements — represent the highest value-added segment available to a recycled compounder. End products include automotive interior trim components, appliance housings, industrial crates and pallets, construction formwork and garden furniture. The cost profile is additive-heavy and quality-sensitive: the additive block runs at the upper end of its range, and the quality loss block carries an outsized penalty because these customers test to specification.
Filler masterbatch
Filler masterbatch, typically calcium carbonate at 70 to 80 percent in a polyethylene or polypropylene carrier, is a volume business with a wear-dominated cost profile. Energy per kilogram is low, throughput is high, and the wear block runs at 9 to 11 percent instead of 6. End products include blown film, woven bags, injection molded housewares and sheet. The single most important cost decision in this segment is wear part material selection, because element replacement frequency directly governs both the wear block and the downtime block.
Color masterbatch
Color masterbatch is a changeover-dominated business. Runs are short, color transitions are frequent, and the purge loss pathway becomes the dominant loss contributor rather than start-up scrap. End products span virtually every molded and extruded plastic article. Cost control here is primarily a scheduling and cleaning discipline problem, supported by machine design features that eliminate dead zones — self-cleaning screw geometry, streamlined die transitions and split barrel access for rapid cleaning.
Glass-fiber reinforced polyamide and polypropylene
Glass-fiber reinforced compounds based on recycled polyamide or polypropylene serve automotive under-hood components, electrical connectors, power tool housings and structural brackets. This is the most wear-aggressive segment in the entire recycled compounding landscape, with the wear block reaching 11 percent and specific energy consumption at the top of the range. Fiber length retention is the technical objective that governs everything: fiber is introduced by side feeder after the polymer has melted, and the screw configuration downstream of the fiber entry must distribute without excessive fiber breakage.
Cable compounds
Cable compounds — halogen-free flame retardant formulations, cross-linkable polyethylene bases and semiconducting compounds — carry a compliance-dominated cost profile. Mineral flame retardant loadings of 50 to 60 percent create simultaneous wear, dispersion and throughput challenges, and the electrical property specifications leave little tolerance for contamination or moisture. Cleanliness discipline is the defining cost factor.
Recycled pelletizing and R-PET flake processing
Straight recycled pelletizing converts washed flake or regrind into a saleable pellet without significant formulation change. Cost is dominated by energy and loss rather than additives. Recycled PET flake processing is a special case where crystallizing and drying dominate the energy block and where chain extension chemistry determines whether the output reaches fiber grade, strapping grade, sheet grade or only low-specification applications. Kerke’s product scope also covers biodegradable plastic compounding, thermoplastic elastomer compounding, wood-plastic composites, PVC compounding, engineering plastics, textile masterbatch, black masterbatch and additive masterbatch, so the machine platform does not restrict which of these cost profiles a plant can pursue.
Requirement-to-model selection guide
The table below maps a plant’s target annual output, feedstock family and filler loading onto a recommended Kerke machine configuration. It is a starting point for specification, not a substitute for a trial run — Kerke operates laboratory twin-screw extruders specifically so that a formula can be validated before a production machine is configured.
Table 14: Requirement to Kerke model selection matrix
| Annual output target | Material family | Filler or fiber loading | Recommended Kerke model | Recommended configuration highlights |
|---|---|---|---|---|
| Formula development, trials only | Any | Any | KTE-16B laboratory twin-screw extruder | Modular barrel, quick recipe change, small batch validation |
| Under 1,500 t | Clean single-polymer regrind | None | SE-120 single-screw extruder | Single vent, strand pelletizing, hydraulic screen changer |
| 1,500 – 3,000 t | Recycled PP or PE, mixed | 0 – 20% | KTE-52D or KTE-65D | Two vent stages, loss-in-weight feeding, water-ring die-face cutting |
| 2,500 – 5,000 t | Filler masterbatch | 70 – 80% CaCO3 | KTE-65D | Twin-screw side feeder, PM-HIP elements, bimetallic liner, air-cooled die-face cutting |
| 4,000 – 8,000 t | Recycled PP compound, modified | 10 – 40% | KTE-75D | Three vent stages, multiple loss-in-weight feeders, hardened element set |
| 4,000 – 8,000 t | Color masterbatch | 20 – 50% pigment | KTE-65D or KTE-75D | Self-cleaning screw geometry, split barrel for fast cleaning, strand pelletizing |
| 6,000 – 12,000 t | Glass-fiber reinforced PA or PP | 20 – 40% glass fiber | KTE-75D or KTE-95D | Side feeder after melt zone, PM-HIP full set, side vent, underwater granulation |
| 8,000 – 16,000 t | Recycled PET flake with chain extender | 0 – 30% | KTE-95D | Crystallizer and dehumidifying dryer, deep vacuum venting, corrosion-resistant die |
| 10,000 – 20,000 t | Cable compound, halogen-free | 50 – 60% mineral | KTE-95D | PM-HIP elements, twin side feeders, cleanliness-focused flow path |
| Above 18,000 t | High-volume single product | Any | KTE-135D | Underwater granulation, full automation, energy sub-metering, campaign running |
| Difficult materials, two-stage requirement | Heat-sensitive or high-volatile streams | Any | KTE-SE double-stage extrusion system | Mother-baby configuration, decoupled mixing and pressure building |
| Special material processing | Materials requiring gentler shear history | Any | KTE-T three-screw extruder | Alternative mixing geometry for specific material behaviors |
Cost reduction roadmap: short, medium and long term
A cost analysis that ends with a diagnosis is incomplete. The roadmap below sequences interventions by time to effect and relative investment level, so that a plant can begin with the actions that require attention rather than capital and progress toward the ones that require both.
Table 15: Cost reduction roadmap by horizon
| Horizon | Intervention | Physical effect | Time to measurable effect | Relative investment level | Index gain |
|---|---|---|---|---|---|
| Short term | Production sequencing, light to dark and low to high filler | Purge loss reduced by 40 – 60% | 1 – 2 weeks | None | 2 – 4 points |
| Short term | Standardized start-up and shutdown procedure | Start-up scrap reduced by 40 – 55% | 2 – 4 weeks | None | 1 – 2 points |
| Short term | Melt temperature and screw speed window tightening | Main drive SEC reduced by 5 – 10% | 2 – 6 weeks | Low | 1 – 3 points |
| Short term | Energy sub-metering installation and baseline | Attribution of consumption by consumer | 4 – 8 weeks | Low | Enables 3 – 6 points |
| Short term | Off-peak load shifting for drying and chilling | 20 – 30% of load moved out of peak window | 4 – 8 weeks | Low | 2 – 3 points |
| Short term | Cutter blade clearance and die maintenance schedule | Fines and undersize reduced by 40% | 2 – 4 weeks | Low | 1 – 2 points |
| Medium term | Loss-in-weight feeder retrofit on main and additive streams | Dosing accuracy improved, labor 3.3× reduction on handling | 3 – 6 months | Medium | 4 – 7 points |
| Medium term | Screw configuration optimization for the dominant recipe | Main drive SEC reduced 8 – 15%, dispersion maintained | 2 – 4 months | Medium | 3 – 5 points |
| Medium term | Hydraulic or continuous screen changer | Screen change downtime reduced by 60 – 80% | 3 – 5 months | Medium | 2 – 4 points |
| Medium term | Central loading and big-bag discharge stations | Handling hours per ton from 0.40 to 0.12 | 4 – 8 months | Medium | 3 – 5 points |
| Medium term | PM-HIP element upgrade in the mixing zone | Element life multiplied by 2.2 on filled recipes | 6 – 12 months | Medium | 2 – 4 points |
| Long term | Conversion to underwater granulation | Strand breakage loss largely eliminated, pellet uniformity improved | 9 – 18 months | High | 3 – 5 points |
| Long term | Additional vacuum vent stage with condensation trap | Volatile content and odor grade improved, emission load reduced | 9 – 15 months | High | 2 – 4 points |
| Long term | Capacity expansion into the next scale tier | Overhead absorption across larger tonnage | 12 – 24 months | Premium | 10 – 15 points |
| Long term | Inline melt flow rate monitoring and closed-loop correction | Off-spec rate reduced, specification reach extended | 12 – 18 months | High | 3 – 6 points |
Sequencing logic
The roadmap is deliberately front-loaded with zero-investment and low-investment actions. A plant that executes the entire short-term block before touching capital typically recovers 7 to 14 index points, and — more importantly — it establishes the measurement discipline that makes every subsequent capital decision verifiable. Installing energy sub-metering before a screw configuration change means the change can be proven. Installing it afterward means the change can only be believed.
The medium-term block concentrates on feeding, mixing and filtration, because these three subsystems govern the largest share of both loss and labor. The long-term block addresses pelletizing, devolatilization and scale, which are the interventions that require machine-level change and therefore the longest planning lead time. Note that capacity expansion carries the largest single index gain in the table, at 10 to 15 points, which is consistent with the scale analysis presented earlier — but it also carries a Premium investment rating and a market risk that none of the other interventions carry.
Certification, factory acceptance testing and verification
A cost model built on assumed performance is a hypothesis. Factory acceptance testing converts it into verified data before the machine leaves the manufacturing floor, and it is the single most effective protection a buyer has against a cost model that fails in commissioning.
What a meaningful factory acceptance test measures
A factory acceptance test for a recycled compounding line should verify at least the following, using the buyer’s own feedstock wherever practical rather than a clean substitute. Throughput at the specified recipe, measured over a continuous run of sufficient duration to reach thermal steady state. Specific energy consumption at the main drive, measured at the specified throughput and recorded in kWh/kg. Melt temperature at the die and its stability band. Melt pressure and its pulsation amplitude, which predicts strand stability. Vacuum level achieved at each vent stage and the resulting volatile content of the product. Pellet size distribution and fines fraction from sieve analysis. Temperature control accuracy in each barrel zone. Noise level at the operator position. Gearbox temperature and vibration at rated load. Emergency stop and safety interlock function.
Recording these values at the factory establishes the reference against which site performance is later compared. When a plant reports higher energy consumption than expected after six months of operation, the acceptance test data determines whether the machine has drifted, the feedstock has changed or the process has been altered — a distinction that is impossible to make without a baseline.
Standards and certification context
Kerke manufactures under a quality management framework aligned with ISO 9001, and machines destined for the European market are supplied with CE conformity, covering machinery safety, electrical safety and electromagnetic compatibility requirements as applicable to the configuration supplied. Buyers operating in regulated end markets should additionally confirm the requirements that apply downstream of the compound: food contact frameworks where the recycled compound enters packaging, RoHS and REACH considerations for electrical and electronic applications, and the relevant flame retardancy classifications for cable and construction products. These downstream requirements shape the compound specification, which in turn shapes the machine configuration and therefore the cost model — which is why they belong in a cost analysis rather than in a separate compliance discussion.
Service and support
Service quality enters the cost model through the downtime block, and its influence is larger than most specification comparisons acknowledge. A machine that is well supported produces more hours per year, and hours per year is the denominator in the depreciation equivalent block and a major driver of the labor block.
Testing before shipment
Every Kerke machine is tested before shipment, and buyers are encouraged to attend or to nominate a representative. Where the buyer supplies feedstock, the trial can be run on the actual material rather than a proxy, which is the only way to verify throughput and energy figures that will hold in production. Kerke also operates laboratory twin-screw extruders for formula trials and R&D, so a recipe can be validated at small scale before a production machine is configured — a sequence that prevents the most expensive category of specification error.
Installation, commissioning and training
Kerke engineers support installation and commissioning on site, including alignment, utility connection verification, initial recipe loading, process window establishment and operator training. Training covers routine operation, screw pulling and element inspection, screen changing, cutter maintenance, recipe changeover procedure and the diagnostic interpretation of pressure, temperature and torque trends. Operator competency has a direct and measurable effect on the loss block, which is why training is treated as a cost intervention rather than a courtesy.
Spare parts and ongoing support
As part of the Wanplas brand service commitments, Kerke provides USD 500 free parts per year, along with free replacement of damaged parts within the warranty period. Remote support allows engineers to review PLC data and process trends without a site visit, which shortens diagnosis time for control and process issues considerably. Wanplas operates an open factory policy, and customers are welcome to visit the Kerke manufacturing facility to inspect machining, assembly and testing operations directly. For plants planning a wider recycling operation, Wanplas also supplies the upstream washing, sorting and size reduction equipment that feeds a compounding line, so the whole material path can be specified as one coherent system rather than assembled from disconnected parts.
Spare part strategy as a cost lever
The way a plant holds spares materially affects its downtime block. A recommended baseline for a recycled compounding line is one complete set of the wear elements in the mixing zone, two spare screen packs of each mesh specification in use, one spare set of cutter blades, one spare die plate for the primary product, a full set of heater bands and thermocouples, and the gearbox seal kit. Holding these items converts a multi-day supply lead time into a shift-length replacement, and in the hidden cost table that difference is worth 2 to 4 index points on its own.
Frequently asked questions
Which cost block should a new recycled compounding plant attack first?
Material loss, because it requires no capital and it also reduces the energy and labor consumed by reprocessing. A plant running at 6 to 8 percent total loss can usually reach 3 to 4 percent within one quarter through production sequencing, standardized start-up procedure and cutter maintenance discipline alone. Once loss is under control, energy becomes the next target, and by then sub-metering will be in place to verify improvements.
How does specific energy consumption change with filler loading?
Main drive specific energy consumption falls as mineral filler loading rises, because mineral filler carries heat capacity but no melting enthalpy and it replaces polymer that would otherwise require melting. A recycled polypropylene at 50 percent coated calcium carbonate typically draws 0.14 to 0.20 kWh/kg at the main drive versus 0.20 to 0.27 kWh/kg unfilled. However the wear rate multiplier rises to roughly 2.4 times baseline, so the energy saving must be evaluated together with the wear cost, not separately.
Is a twin-screw extruder always better than a single-screw for recycled plastic?
No. For clean single-polymer re-pelletizing with no filler introduction, no reactive chemistry and modest devolatilization requirements, an SE series single-screw extruder operates at 87 to 92 cost-per-ton index points against a twin-screw baseline of 100 and is the correct choice. A twin-screw becomes necessary when the process requires side feeding of fillers or fibers, multi-stage vacuum devolatilization, reactive chain extension, or dispersive mixing of pigments and reinforcements. Many plants operate both types for different duties.
How many worked hours per ton should a modern compounding plant target?
A well automated plant with loss-in-weight feeding, central loading, hydraulic screen changing and automated packing should reach approximately 0.9 to 1.1 worked hours per ton across all direct and directly supervisory functions. A manual plant typically sits near 1.9. The largest single gap is material handling, where automation delivers a reduction factor of roughly 3.3, followed by screen changing at a similar factor.
When does a PM-HIP screw element set justify itself over nitrided elements?
PM-HIP elements deliver roughly 2.2 times the service life of nitrided 38CrMoAlA elements and are strongly favored above approximately 25 percent mineral loading or with any glass-fiber content. On clean unfilled recyclate, nitrided elements already deliver 6,000 to 9,000 hours, which is two to three years of two-shift operation, and the PM-HIP premium is usually not recovered. The decision should be made per zone rather than per machine: many plants specify PM-HIP only in the kneading and metering sections where wear concentrates.
What loss rate is realistically achievable in recycled compounding?
Total material loss of 2 to 3 percent is achievable with disciplined sequencing, standardized start-up, continuous screen changing and underwater or water-ring pelletizing. Plants running short color campaigns on contaminated post-consumer feedstock with manual screen changing typically sit at 6 to 8 percent. The gap between those two states is worth 6 to 8 cost-per-ton index points, and most of the closing actions require procedure changes rather than capital.
How much does scale actually reduce cost per ton?
Moving from a small single-line plant at 118 index points to a large multi-line plant at 88 index points represents a 30 point reduction, of which roughly 11 points come from labor absorption, 7 from reduced changeover and start-up loss, 6 from higher annual running hours, 4 from utility base load absorption and 2 from consumables procurement leverage. Notably, almost none of it comes from the extruder itself being more energy efficient at larger diameters.
Does higher configuration always lower cost per ton?
It lowers cost per ton with diminishing returns. Moving from Basic to Standard configuration costs 22 investment index points and returns 18 unit cost index points; moving from Standard to High costs 38 investment index points and returns a further 18. The second step is better evaluated as a market access decision, because the High tier extends the range of product specifications the plant can qualify for — a benefit that does not appear in the unit cost index at all.
What should be verified during factory acceptance testing?
Throughput at the specified recipe over a continuous steady-state run, main drive specific energy consumption in kWh/kg, melt temperature and its stability band, melt pressure pulsation amplitude, vacuum level at each vent stage with resulting volatile content, pellet size distribution and fines fraction, barrel zone temperature control accuracy, noise at the operator position, gearbox temperature and vibration at rated load, and safety interlock function. Recording these creates the baseline against which future site performance is judged.
How should a plant budget for spare parts holding?
A practical baseline is one complete set of mixing zone wear elements, two spare screen packs per mesh specification in use, one spare set of cutter blades, one spare die plate for the primary product, a full set of heater bands and thermocouples, and a gearbox seal kit. This converts a multi-day supply lead time into a shift-length replacement and is worth 2 to 4 cost-per-ton index points through avoided downtime. Kerke supports this with USD 500 free parts per year under the Wanplas brand service commitments.
Conclusion
A comprehensive cost analysis of a recycled plastic twin screw compound processing factory becomes actionable only when it is expressed in units a plant engineer can measure and change. Reduced to its essentials, this model says the following. Energy and material loss together control roughly 40 percent of conversion cost and both are engineering-controllable. Labor is best managed as worked hours per ton, where automation delivers a reduction factor close to two and material handling carries the largest single gain. Wear parts occupy a small direct share but govern a much larger territory through downtime and quality drift, which makes element material selection a strategic rather than a procurement decision. Scale reduces cost per ton by roughly 30 index points between a small single-line plant and a large multi-line operation, but almost none of that comes from the extruder itself. And configuration choices set a cost trajectory at specification stage that is expensive to change later.
The roadmap that follows from this analysis is equally clear. Begin with the zero-investment actions — production sequencing, standardized start-up, process window discipline — which typically recover 7 to 14 index points and simultaneously build the measurement foundation that makes later capital decisions verifiable. Progress to feeding, mixing and filtration upgrades in the medium term. Reserve pelletizing conversion, additional devolatilization capacity and scale expansion for the long-term horizon where planning lead time and capital availability allow. At every step, judge the intervention on cost per ton, loss rate, worked hours per ton and specific energy consumption together, never on a single metric.
Kerke, a Wanplas factory with more than 12 years dedicated exclusively to compounding extrusion, over 19,997 square meters of manufacturing space, more than 2,000 machines operating in over 70 countries and a team of more than 100 people, builds the KTE series specifically so that these cost levers remain configurable rather than fixed: aspect ratio, barrel structure, screw arrangement, exhaust layout, feeding system, pelletizing method and electrical control are all specified per application. Whether the requirement is a KTE-65D for filler masterbatch, a KTE-75D for modified recycled polypropylene, a KTE-95D for glass-fiber reinforced compounds or recycled polyester, a KTE-135D for high-volume campaign production, or an SE series single-screw for clean re-pelletizing, the configuration should follow the cost structure the plant actually faces.
Send your feedstock description, target recipes, annual output objective and quality specifications, and the Kerke engineering team will prepare a tailored machine configuration with a matched feeding and pelletizing system, together with the specific energy consumption and throughput figures to be verified at factory acceptance testing. Sample trial runs on your own material are welcome at the laboratory extruder line, and the factory is open for inspection before, during and after manufacturing. Wanplas builds machines to warm global customers with China plastic machinery — and in recycled compounding, the machine that earns that description is the one whose cost structure is transparent before it ships.