- What Investment Recovery Really Measures on a Compound Line
- A Dimensionless Payback Model That Needs No Currency
- Investment Index: How Configuration Tiers Move the Numerator
- Monthly Contribution Index: The Seven Physical Drivers
- Driver Sensitivity: Which Variable Moves the Timeline Most
- Three Scenarios: Conservative, Base and Optimistic Timelines
- The Ramp-Up Curve: Why Month One Is Not Month Thirteen
- Feedstock Routes and Their Effect on Rate, Yield and Timeline
- Specific Energy Consumption as a Payback Lever
- Yield and Quality Control: The Silent Payback Multiplier
- Technical Levers That Shorten the Recovery Timeline
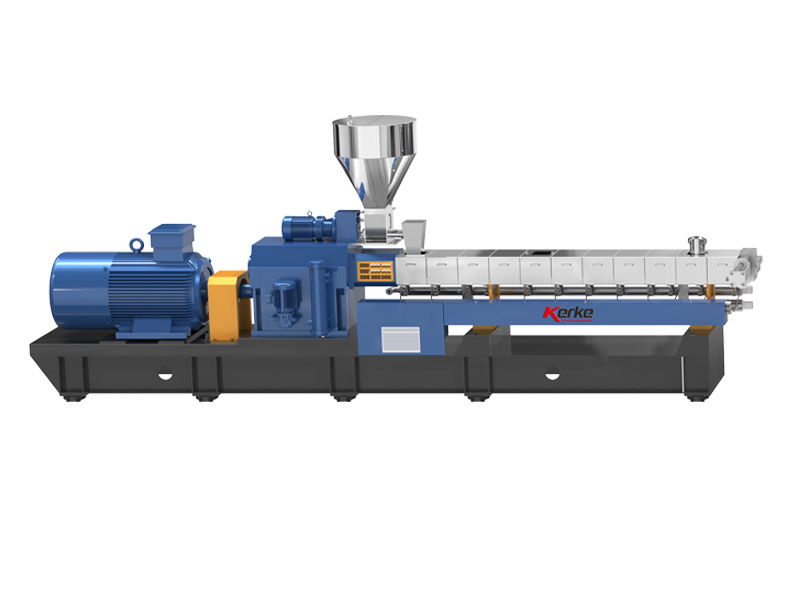
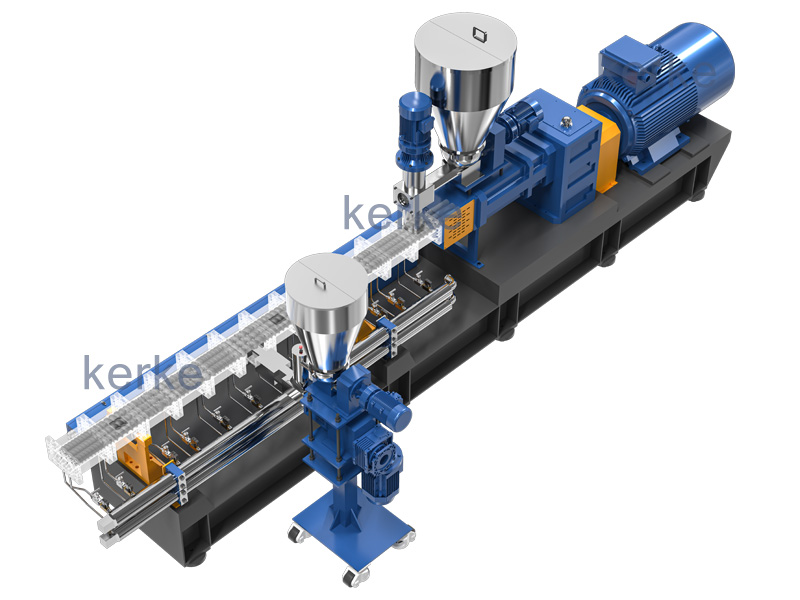
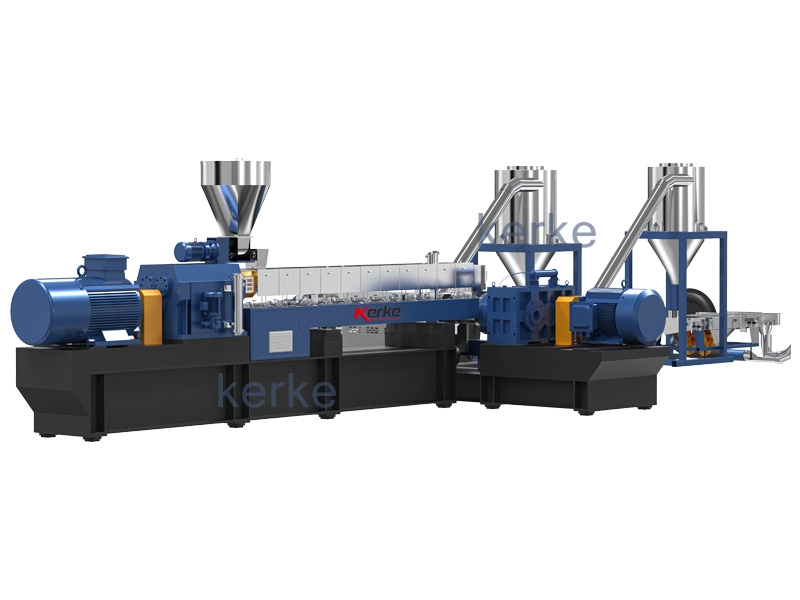
- Kerke KTE-75D Twin-Screw Compounding Extruder
- Kerke KTE-95D Twin-Screw Compounding Extruder
- Application Industries That Set the Value-Uplift Index
- Requirement-to-Model Selection Guide
- Operating Burden Structure Expressed as Ratios
- Wear Part Life and Replacement Intervals
- Risk Factors and Hedging the Timeline
- Certification and Factory Acceptance Testing
- Service and Support During the Recovery Period
- Frequently Asked Questions
- Conclusion
Every recycler who has ever stood in front of a quotation for a waste plastic twin screw compound line asks the same question before any technical question: how long will it take to recover investment of waste plastic twin screw compound line equipment once it is installed and running? The honest engineering answer is that the recovery period is not a property of the machine at all. It is a property of the system built around the machine: how many hours the line actually runs, how much of the nameplate rate it holds, how much of the output passes first-pass inspection, how much energy each kilogram consumes, and how far the compound is lifted above the raw feedstock in technical grade. Two identical extruders installed in two different factories routinely differ by more than a year in recovery time, and the difference is almost never the extruder.
This guide builds a complete recovery-time model without quoting a single figure of money. Instead of guessing at values that change by region, by month and by contract, it uses an index framework: the total installed investment of a reference line is set at 100 index points, and monthly contribution is expressed in the same index points. From there, payback becomes a pure ratio of physical variables that any plant engineer can measure with a power meter, a scale, a shift log and a quality report. The result is a model that stays valid regardless of where the factory is built or what the market is doing in 2026.
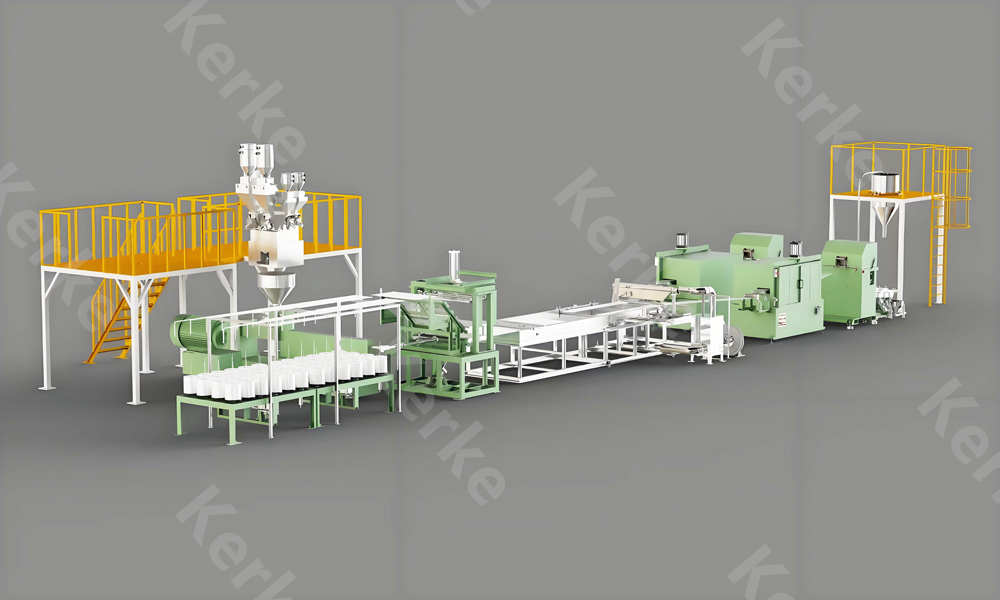
Kerke Extrusion Equipment, a Wanplas factory, has spent more than twelve years building parallel co-rotating twin-screw compounding extruders in a facility of over 19,997 square meters, with more than 2,000 machines running in over 70 countries and a team of more than 100 people dedicated to a single product family. Recognized among the top five twin-screw extruder suppliers in China, Kerke works under the slogan “We Know Compounding Extruder” and supplies the KTE series from KTE-16B laboratory units up to KTE-135D production platforms, together with SE series single screw extruders rated from 30 kg/h to 800 kg/h, loss-in-weight feeding systems and matched pelletizing equipment. The models and configuration tiers used throughout this article are drawn from that real lineup, so the timeline arithmetic maps onto machines that can actually be ordered, tested and shipped.
What Investment Recovery Really Measures on a Compound Line
Investment recovery on a waste plastic compound line measures the elapsed time between the moment capital is committed and the moment cumulative contribution equals that commitment. It is a time variable, not a money variable, and that distinction changes how the whole calculation should be structured. When recovery is treated as a time variable, the controlling questions become operational: when does the line first produce saleable pellets, how steeply does output climb after that, and how stable is the plateau once it is reached.
Three separate clocks run in parallel on a new compounding project, and confusing them is the most common reason a recovery forecast fails. The first clock is the procurement clock, running from contract signature through manufacturing, factory acceptance testing, shipment, customs and delivery to the plant floor. The second clock is the commissioning clock, running from mechanical installation through utility connection, dry runs, first melt, formula trials and customer qualification. The third clock is the contribution clock, which only starts when the first qualified batch is accepted by a buyer. A recovery forecast built on the third clock alone understates the real timeline; one built on the first clock alone overstates the technical difficulty of the ramp.
Why Machine Selection Alone Cannot Answer the Question
A twin-screw extruder is a conversion device. It takes a feedstock of a given technical grade and returns a compound of a higher technical grade, and the recovery period depends on how large that uplift is and how many kilograms per year it can be applied to. A larger machine increases the number of kilograms but does not by itself increase the uplift. A better-configured machine of the same size can increase both, because vacuum devolatilization, gravimetric feeding and melt filtration all raise the achievable grade of the finished pellet. This is why the recovery question must be answered at the level of the line, not the level of the extruder.
It also explains a result that surprises many first-time buyers: the configuration with the lowest entry investment is frequently not the one with the shortest recovery period. A line that saves on vacuum capacity, feeding accuracy and filtration will run at lower utilization, produce a lower-grade pellet and accumulate more off-spec material, and those three penalties compound against each other month after month. The index model in the following sections makes that effect visible in months rather than in adjectives.
The Four Components of Total Installed Investment
For modeling purposes, total installed investment is decomposed into four blocks, each expressed as a share of the 100-point baseline. The main extrusion unit, comprising the twin-screw extruder, gearbox, motor, control cabinet and barrel assembly, usually accounts for the largest single block. Auxiliary equipment covers feeders, side feeder, vacuum system, screen changer, pelletizer, water circuit, dryer, silos and conveying. Installation covers foundations, electrical distribution, cooling water, compressed air, dust extraction and commissioning labor. Plant modification covers floor loading, ceiling height, ventilation, fire compliance and material storage areas. Keeping these four blocks separate matters because they scale differently: doubling extruder size does not double installation, and a difficult building can add more to the index than an extra vacuum stage.
A Dimensionless Payback Model That Needs No Currency
The model presented here reduces investment recovery to a single ratio between two index quantities, both measured in the same arbitrary unit called an index point. Because both numerator and denominator carry the same unit, the unit cancels and the result is a pure number of months. This is the standard technique used in engineering economics when absolute values are volatile but relationships are stable.
The Investment Index is defined by declaring a reference configuration and assigning it 100 index points. Every alternative configuration is then expressed relative to that reference: a stripped-down line might sit at 85 index points, a high-specification line at 135, a premium line at 170. The Monthly Contribution Index is defined by declaring a reference operating condition and assigning it 4.00 index points per month, which by construction returns the reference payback of 25.0 months. Every alternative operating condition is then scaled from that reference using measurable physical ratios.
Defining the Reference Case
The reference case used throughout this article is a standard-configuration waste plastic compounding line built around a KTE-75D platform, sized for a nameplate rate of 500 kg/h on a filled recycled polyolefin formula. It runs three shifts for 6,500 effective operating hours per year, holds 85 percent capacity utilization against those hours, and achieves 96 percent first-pass yield. Its Unit Contribution Index, the dimensionless measure of technical uplift net of conversion burden per kilogram, is set at 1.00.
Effective monthly output = 221 tonnes
Monthly Contribution Index (reference) = 4.00 index points
Payback (reference, idealized) = 100 ÷ 4.00 = 25.0 months
From that anchor, any other case is computed with a single scaling expression. The monthly contribution index of any configuration equals 4.00 multiplied by the ratio of its effective monthly tonnage to 221 tonnes, multiplied by its Unit Contribution Index. This keeps every subsequent table internally consistent and lets a reader substitute their own physical measurements without touching the structure of the model.
What the Unit Contribution Index Contains
The Unit Contribution Index expresses, on a per-kilogram basis, the technical value uplift delivered by compounding, reduced by the conversion burden of energy, labor, consumables, wear parts and scrap. It is dimensionless by construction. A simple re-pelletizing operation that takes clean regrind and returns an equivalent-grade pellet has a low uplift and therefore a low index, typically in the 0.6 to 0.8 band relative to the reference. A line that takes mixed post-consumer polyolefin and returns a qualified, color-matched, impact-modified injection-grade compound with certified melt flow rate and ash content carries a high uplift, commonly 1.2 to 1.5 relative to the reference. The index therefore captures the entire commercial logic of compounding without naming a single figure of money.
Investment Index: How Configuration Tiers Move the Numerator
Configuration is the only part of the recovery equation that is fully decided before the line is built, which makes it the highest-leverage decision in the whole project. Four practical tiers cover almost every waste plastic compounding project, and each tier changes both the numerator and the denominator of the payback ratio.
Tier Definitions
The basic tier strips the line to the minimum that will still make pellets: single atmospheric vent, volumetric feeding, manual plate screen changer, water strand pelletizing and minimal instrumentation. The standard tier adds one vacuum vent, a loss-in-weight main feeder, a twin-screw side feeder, a hydraulic plate screen changer and basic data logging. The high tier adds a second vacuum stage, a full gravimetric feeder array, a continuous screen changer, a melt pump for pressure stabilization and water-ring die-face pelletizing. The premium tier adds underwater pelletizing, liquid feeding, continuous belt melt filtration, online melt flow rate monitoring and full recipe management with production data capture.
| Configuration tier | Investment Index | Key content | Achievable rate on KTE-75D platform | Utilization | First-pass yield | Unit Contribution Index |
|---|---|---|---|---|---|---|
| Tier A — Basic | 85 | Single atmospheric vent, volumetric feeding, manual screen changer, water strand pelletizing | 420 kg/h | 78% | 92% | 0.88 |
| Tier B — Standard (reference) | 100 | One vacuum vent, loss-in-weight main feeder, side feeder, hydraulic screen changer | 500 kg/h | 85% | 96% | 1.00 |
| Tier C — High | 135 | Two vacuum stages, full gravimetric array, continuous screen changer, melt pump, water-ring pelletizing | 560 kg/h | 90% | 97.5% | 1.15 |
| Tier D — Premium | 170 | Underwater pelletizing, liquid feeder, continuous belt filtration, online melt flow rate monitoring, full data capture | 600 kg/h | 92% | 98.5% | 1.30 |
Payback by Configuration Tier
Applying the scaling expression to each tier produces the result that decides most procurement arguments. The basic tier carries the lowest Investment Index and the longest recovery period. The standard, high and premium tiers converge into a narrow band, which means the choice among them should be driven by product strategy and customer requirements rather than by timeline anxiety.
| Tier | Effective annual output (t) | Effective monthly output (t) | Monthly Contribution Index | Investment Index | Idealized payback (months) | Relative to reference |
|---|---|---|---|---|---|---|
| Tier A — Basic | 1,959 | 163.3 | 2.60 | 85 | 32.7 | 31% slower |
| Tier B — Standard | 2,652 | 221.0 | 4.00 | 100 | 25.0 | baseline |
| Tier C — High | 3,194 | 266.2 | 5.54 | 135 | 24.4 | 2% faster |
| Tier D — Premium | 3,534 | 294.5 | 6.93 | 170 | 24.5 | 2% faster |
The engineering interpretation is direct. Between Tier A and Tier B, the extra 15 index points of investment buy an 80 kg/h rate increase, seven percentage points of utilization, four percentage points of yield and a 0.12 lift in unit contribution. Those four gains together shorten recovery by roughly 7.7 months. Above Tier B the curve flattens: additional index points continue to buy real capability, but the recovery period stops improving, so the justification shifts to product range, contamination tolerance and the ability to serve customers with tighter specifications.
Reading the Flat Zone Correctly
A flat payback curve between Tier B and Tier D does not mean the higher tiers are pointless. It means they are self-financing. A premium line recovers its larger investment in the same number of months while producing a materially better pellet, tolerating dirtier feedstock and opening application segments that a basic line cannot serve at all. For a recycler planning to move from commodity re-pelletizing into engineering compounds within three years, buying Tier C at the outset is usually cheaper in time than buying Tier A and upgrading later, because the upgrade path forces a second commissioning and a second qualification cycle.
Monthly Contribution Index: The Seven Physical Drivers
The denominator of the payback ratio is built from seven physical drivers, every one of which is measurable with instruments already present in a well-run compounding plant. Naming them explicitly turns a vague forecast into an auditable model, because each driver can be assigned a target, a measurement method and an owner.
Driver One: Capacity Utilization
Capacity utilization is the fraction of scheduled operating hours during which the line actually produces saleable pellets at rate. It absorbs planned changeovers, screen changes, die cleaning, unplanned stops, feed interruptions and quality holds. A first-year recycler on mixed feedstock typically lands between 65 and 75 percent. A disciplined operation on a narrow feedstock band with scheduled maintenance reaches 85 to 92 percent. Utilization is the single most powerful driver in the model because it multiplies directly into output without any offsetting burden.
Driver Two: Annual Effective Operating Hours
Shift pattern sets the ceiling on everything else. Two-shift operation with routine maintenance windows delivers roughly 4,000 effective hours per year. Three-shift operation with planned stoppages delivers roughly 6,500 hours. Continuous operation with a hot-standby maintenance strategy and staggered crews can reach 7,200 hours or slightly more. The step from two shifts to three is the largest single timeline decision available to a recycler, and it usually requires no additional equipment at all, only labor organization.
Driver Three: First-Pass Yield
First-pass yield is the fraction of extruded mass that meets specification without rework, blending down or downgrading. On clean rigid regrind with a stable formula it reaches 96 to 98 percent. On mixed post-consumer material with color variation and contamination it can fall to 85 percent or lower. Yield losses appear as start-up purge, strand breakage, off-color transitions, oversized or fused pellets, fines and quality holds. Yield behaves multiplicatively with utilization, so a plant at 75 percent utilization and 88 percent yield delivers only 66 percent of its nameplate potential.
Driver Four: Specific Energy Consumption
Specific energy consumption, expressed in kWh per kilogram of pellet, is the clearest physical proxy for conversion efficiency. It enters the model through the Unit Contribution Index rather than through output. A shift of 0.08 kWh/kg on a filled polyolefin compound moves the Unit Contribution Index by roughly 0.06 index points, which is a measurable change in the recovery timeline over a full year.
Driver Five: Labor Configuration
Labor is best expressed in worker-hours per tonne of accepted pellet rather than headcount, because headcount hides the effect of rate. A well-configured 500 kg/h line with gravimetric feeding, automatic screen changing and bulk bag handling can be operated with two people per shift, giving roughly 4 worker-hours per tonne. The same rate on a manual line with hand-fed additives, manual screen changes and bag-by-bag packing can require four people per shift, doubling the labor intensity to about 8 worker-hours per tonne and pulling the Unit Contribution Index down accordingly.
Driver Six: Material Loss Rate
Material loss covers everything that enters the feeder but never leaves as saleable pellet: fines from the crusher, dust in conveying, purge at start-up and shutdown, filter cake at the screen changer, strand scrap at the water bath and pellet fines at the classifier. On clean rigid feedstock, total loss of 2 to 3 percent is normal. On heavily contaminated post-consumer film, loss of 6 to 10 percent is common before the melt even reaches the die. Loss rate is distinct from yield: loss removes mass, yield downgrades mass.
Driver Seven: Value-Uplift Index
The value-uplift index measures how far the finished compound is lifted above the incoming feedstock in technical grade. A line that simply re-pelletizes clean regrind sits at the bottom of the range. A line that dries, devolatilizes, filters, reinforces, impact-modifies, color-matches and certifies its output sits at the top. Because uplift is the only driver that can be increased without buying more hours or more machines, it deserves the most strategic attention. Moving from a Low uplift grade to a High uplift grade on the same equipment can shorten the recovery period by a factor approaching 1.8.
| Driver | Measurement method | Weak plant | Reference plant | Strong plant | Enters model through |
|---|---|---|---|---|---|
| Capacity utilization | Production log against scheduled hours | 68% | 85% | 92% | Output |
| Annual effective hours | Shift calendar minus planned maintenance | 4,000 h | 6,500 h | 7,200 h | Output |
| First-pass yield | Accepted mass divided by extruded mass | 88% | 96% | 98.5% | Output |
| Specific energy consumption | Line power meter divided by pellet mass | 0.34 kWh/kg | 0.26 kWh/kg | 0.20 kWh/kg | Unit Contribution Index |
| Labor intensity | Worker-hours per accepted tonne | 8 h/t | 4.5 h/t | 3 h/t | Unit Contribution Index |
| Material loss rate | Feed mass minus pellet mass | 8% | 3% | 1.8% | Unit Contribution Index |
| Value-uplift index | Grade of output versus grade of input | Low | Medium | Very High | Unit Contribution Index |
Driver Sensitivity: Which Variable Moves the Timeline Most
Sensitivity analysis answers the practical question of where to spend attention. Each row in the table below changes exactly one driver away from the reference case while holding the other six constant, then recomputes the Monthly Contribution Index and the resulting idealized payback at an Investment Index of 100.
| Change from reference | Output multiplier | Unit Contribution Index | Monthly Contribution Index | Idealized payback (months) | Change versus 25.0 months |
|---|---|---|---|---|---|
| Reference case | 1.000 | 1.00 | 4.00 | 25.0 | — |
| Utilization 85% → 75% | 0.882 | 1.00 | 3.53 | 28.3 | +3.3 |
| Utilization 85% → 92% | 1.082 | 1.00 | 4.33 | 23.1 | −1.9 |
| Yield 96% → 90% | 0.938 | 1.00 | 3.75 | 26.7 | +1.7 |
| Yield 96% → 98.5% | 1.026 | 1.00 | 4.10 | 24.4 | −0.6 |
| Hours 6,500 → 4,000 (two shifts) | 0.615 | 1.00 | 2.46 | 40.7 | +15.7 |
| Hours 6,500 → 7,200 | 1.108 | 1.00 | 4.43 | 22.6 | −2.4 |
| Specific energy 0.26 → 0.34 kWh/kg | 1.000 | 0.94 | 3.76 | 26.6 | +1.6 |
| Specific energy 0.26 → 0.20 kWh/kg | 1.000 | 1.045 | 4.18 | 23.9 | −1.1 |
| Labor 4.5 → 8 worker-hours per tonne | 1.000 | 0.92 | 3.68 | 27.2 | +2.2 |
| Loss rate 3% → 8% | 1.000 | 0.93 | 3.72 | 26.9 | +1.9 |
| Uplift Medium → High | 1.000 | 1.25 | 5.00 | 20.0 | −5.0 |
| Uplift Medium → Low | 1.000 | 0.70 | 2.80 | 35.7 | +10.7 |
| Rate 500 → 400 kg/h (undersized screw) | 0.800 | 1.00 | 3.20 | 31.3 | +6.3 |
Reading the Sensitivity Ranking
Three conclusions emerge from the ranking, and they hold across almost every waste plastic compounding project. First, shift pattern dominates everything: the single change from two shifts to three shifts is worth more than fifteen months of recovery time, more than all quality and energy improvements combined. Second, product positioning is the second most powerful lever, with uplift grade worth ten to eleven months across its practical range. Third, the technical parameters that engineers argue about most, specific energy and yield, are individually worth only one to two months each, although they accumulate and they are the parameters that keep customers.
The practical implication for a recycler planning a new line is to fix shift pattern and product positioning before negotiating machine specification. A plant that intends to run two shifts on commodity re-pelletizing should expect a recovery period roughly twice as long as a plant running three shifts on qualified engineering compounds, using the same extruder in both cases.
Three Scenarios: Conservative, Base and Optimistic Timelines
Single-point forecasts create false confidence. A three-scenario band is more useful because it communicates both the expected result and the width of the uncertainty. Each scenario below bundles a coherent set of driver values that tend to occur together in practice, rather than mixing best-case and worst-case assumptions arbitrarily.
Scenario Definitions
The conservative scenario represents a first-time recycler on two shifts, processing a variable mixed stream into a commodity-grade pellet, with a building that required extra modification. The base scenario represents a competent operator on three shifts with a defined feedstock contract and a standard compound portfolio. The optimistic scenario represents an experienced compounder running near-continuous operation on a narrow feedstock band into qualified engineering compounds with an established customer base.
| Parameter | Conservative | Base | Optimistic |
|---|---|---|---|
| Investment Index | 110 | 100 | 100 |
| Nameplate rate | 500 kg/h | 500 kg/h | 500 kg/h |
| Annual effective hours | 4,000 | 6,500 | 7,200 |
| Capacity utilization | 78% | 85% | 90% |
| First-pass yield | 92% | 96% | 97.5% |
| Specific energy consumption | 0.31 kWh/kg | 0.26 kWh/kg | 0.22 kWh/kg |
| Labor intensity | 7 worker-hours per tonne | 4.5 worker-hours per tonne | 3.2 worker-hours per tonne |
| Material loss rate | 7% | 3% | 2% |
| Value-uplift grade | Low to Medium | Medium | High |
| Unit Contribution Index | 0.90 | 1.00 | 1.18 |
| Effective annual output | 1,435 t | 2,652 t | 3,159 t |
| Effective monthly output | 119.6 t | 221.0 t | 263.3 t |
| Monthly Contribution Index | 1.95 | 4.00 | 5.62 |
| Idealized payback (months) | 56.4 | 25.0 | 17.8 |
Interpreting the Spread
The spread between the conservative and optimistic cases is a factor of 3.2, and none of that spread comes from the extruder. Every one of the differentiating parameters is an operating decision: shift pattern, feedstock discipline, product positioning, labor organization and maintenance quality. This is the most important message a serious equipment supplier can give a first-time buyer, because it puts control of the timeline back where it belongs, in the hands of the plant.
Two intermediate cases are worth noting. A conservative operator who moves only from two shifts to three, changing nothing else, sees the Monthly Contribution Index rise from 1.95 to 3.17 and the idealized payback drop from 56.4 months to about 34.7 months. A base operator who lifts only the uplift grade from Medium to High, again changing nothing else, sees the index rise from 4.00 to 4.72 and the payback fall to about 21.2 months. Neither improvement requires a single additional index point of investment.
The Ramp-Up Curve: Why Month One Is Not Month Thirteen
Every payback figure quoted so far is idealized, meaning it assumes the line delivers steady-state performance from the first day of operation. No compounding line ever does. The ramp-up curve, which describes how utilization, yield and uplift climb during the first year, adds a measurable number of months to every forecast and is the most commonly omitted element in investment planning.
Phases of the Ramp
Installation and commissioning covers mechanical erection, utility connection, dry running, heating trials, first melt and safety verification. Output during this phase is purge material and trial batches. Trial and qualification covers formula development, sample production, customer testing and specification sign-off, during which the line runs intermittently at partial rate with high scrap. The ramp phase begins when the first qualified orders arrive and covers the period during which operators learn screw changeovers, screen change intervals, water bath settings and pelletizer adjustment. The approach phase sees the plant close the remaining gap in utilization and yield as maintenance routines mature. Steady state is reached when the driver values match the base scenario.
| Phase | Months | Capacity utilization | First-pass yield | Unit Contribution Index | Monthly Contribution Index | Index points recovered in phase | Cumulative index recovered |
|---|---|---|---|---|---|---|---|
| Installation and commissioning | 1 – 2 | 15% | 70% | 0.80 | 0.40 | 0.8 | 0.8 |
| Trial and qualification | 3 – 4 | 40% | 84% | 0.85 | 1.40 | 2.8 | 3.6 |
| Ramp | 5 – 8 | 65% | 91% | 0.92 | 2.67 | 10.7 | 14.3 |
| Approach to steady state | 9 – 12 | 78% | 94.5% | 0.97 | 3.50 | 14.0 | 28.3 |
| Steady state | 13 onward | 85% | 96% | 1.00 | 4.00 | 4.0 per month | — |
The Real Payback Number
After twelve months the line has recovered 28.3 of the 100 required index points. The remaining 71.7 points accumulate at the steady-state rate of 4.00 per month, requiring a further 17.9 months. Total realistic payback is therefore about 29.9 months, roughly five months longer than the idealized 25.0-month figure. That five-month gap is the true value of commissioning quality, operator training and pre-shipment testing, and it is the part of the timeline an equipment supplier can influence most directly.
Ramp-adjusted payback = 12 months + (100 − 28.3) ÷ 4.00 = 12 + 17.9 = 29.9 months
Compressing the Ramp
A compressed ramp is achievable when the machine arrives already proven, when the formula has been trialed on a laboratory or pilot extruder before shipment, when operators have been trained during manufacturing, and when the utility infrastructure is complete before the crates are opened. Under those conditions the phases shorten to one month of commissioning, two months of trial and qualification, three months of ramp and three months of approach.
| Phase | Standard ramp (months) | Compressed ramp (months) | Index recovered, standard | Index recovered, compressed |
|---|---|---|---|---|
| Installation and commissioning | 2 | 1 | 0.8 | 0.4 |
| Trial and qualification | 2 | 2 | 2.8 | 2.8 |
| Ramp | 4 | 3 | 10.7 | 8.0 |
| Approach to steady state | 4 | 3 | 14.0 | 10.5 |
| Cumulative at end of ramp | 12 | 9 | 28.3 | 21.7 |
| Total ramp-adjusted payback | 29.9 | 28.6 | — | — |
Compressing the ramp alone saves about 1.3 months, which looks modest until it is combined with the other levers. A plant that compresses the ramp, runs three shifts and positions its product at a High uplift grade reaches a ramp-adjusted payback close to 24 months, while a plant that does none of those things on the same equipment can still be counting past month fifty. The equipment is identical in both cases.
Feedstock Routes and Their Effect on Rate, Yield and Timeline
Feedstock selection determines the achievable rate, the achievable yield and the drying burden, and therefore determines a large part of the recovery timeline before the extruder is even switched on. Each waste stream behaves differently in a twin-screw barrel, and the differences are physical rather than commercial.
Rigid PP and PE Regrind
Rigid regrind from crates, caps, drums and industrial parts is the most forgiving feedstock available. Bulk density after crushing is typically 300 to 450 kg/m³, which feeds cleanly through a gravimetric main feeder without bridging. Drying is usually optional, with two hours of hot air at 80 degrees Celsius sufficient to remove surface moisture. Degradation risk is low provided melt temperature stays below 230 degrees Celsius for PP and 220 degrees Celsius for HDPE. Rate reaches 95 to 100 percent of nameplate and first-pass yield reaches 96 to 98 percent.
Film and Agglomerated Polyolefin
Film feedstock is defined by low bulk density rather than by polymer chemistry. Loose film flake can sit below 60 kg/m³, and even agglomerated material rarely exceeds 350 kg/m³. The consequence is a feeding limitation rather than a melting limitation: the extruder has ample torque but cannot get material into the barrel fast enough. A crammer feeder, a twin-screw side feeder or a pre-compaction agglomerator is essential, and achievable rate still falls to 70 to 85 percent of nameplate. Printed film carries ink residue that raises volatile load and demands vacuum devolatilization to avoid gels and odor carry-over.
PET Bottle Flakes
Recycled PET is the most drying-sensitive stream in common use. Hydrolytic chain scission begins immediately when wet flake meets melt, so the material must be crystallized and dried to a dew point of minus 40 degrees Celsius with residual moisture below 50 ppm before extrusion. Even with correct drying, intrinsic viscosity falls during a single pass unless deep vacuum devolatilization is applied, typically at minus 0.085 to minus 0.095 MPa across two vent stages. Rate reaches 80 to 90 percent of nameplate and yield lands at 93 to 96 percent, with the main losses coming from color variation and residual contamination.
Polyamide Production Scrap
Polyamide edge trim, sprues and fiber waste is a high-uplift feedstock because the finished compound serves engineering applications. Drying requirements are strict, with a dew point of minus 40 degrees Celsius and residual moisture below 0.10 percent, and glass-fiber reinforcement usually enters through a side feeder downstream of the melting zone to preserve fiber length. Rate reaches 85 to 95 percent of nameplate, yield reaches 94 to 97 percent, and the barrel and screw elements must be specified in wear-resistant grades because glass fiber is abrasive.
Mixed Post-Consumer Streams
Mixed streams combine every difficulty at once: variable melt flow rate, incompatible polymer fractions, residual paper and metal, moisture, pigment carry-over and inconsistent bulk density. Compatibilizers help but cannot fully close the property gap. Rate falls to 60 to 80 percent of nameplate, yield falls to 85 to 92 percent, and screen change frequency rises sharply. For recovery timeline purposes, mixed streams are best treated as a deliberate strategic choice that trades a longer timeline for feedstock availability.
| Feedstock route | Rate versus nameplate | First-pass yield | Drying requirement | Main technical risk | Screen change interval | Relative uplift grade |
|---|---|---|---|---|---|---|
| Rigid PP / PE regrind | 95 – 100% | 96 – 98% | Optional, hot air 80 °C for 2 h | Melt flow rate drift between batches | 12 – 24 h | Medium |
| Film / agglomerated polyolefin | 70 – 85% | 92 – 95% | Surface moisture removal only | Feeding limitation, ink volatiles, gels | 6 – 12 h | Medium |
| PET bottle flakes | 80 – 90% | 93 – 96% | Dew point −40 °C, moisture <50 ppm | Intrinsic viscosity loss, color shift | 8 – 16 h | High |
| Polyamide production scrap | 85 – 95% | 94 – 97% | Dew point −40 °C, moisture <0.10% | Hydrolysis, fiber attrition, abrasive wear | 10 – 20 h | Very High |
| Mixed post-consumer | 60 – 80% | 85 – 92% | Variable, usually required | Incompatible phases, black spots, odor | 4 – 8 h | Low to Medium |
Feedstock Route and Timeline Together
Combining feedstock behavior with the index model gives a clear ranking. Rigid regrind at Medium uplift on three shifts lands close to the 25-month base case. Polyamide scrap at Very High uplift can reach the high teens despite a lower rate, because uplift outweighs throughput. Mixed post-consumer at Low uplift stretches past forty months even with good operating discipline. The lesson is that feedstock strategy and product strategy must be decided together, since the same barrel can produce either the fastest or the slowest recovery depending on what is fed into it.
Specific Energy Consumption as a Payback Lever
Specific energy consumption, abbreviated SEC, is the total electrical energy drawn by the line divided by the mass of accepted pellet produced. It is the most objective single indicator of process efficiency on a compounding line and one of the few parameters that can be improved after installation without capital work.
Typical SEC Bands by Compound Family
| Compound family | Typical SEC (kWh/kg) | Dominant energy consumer | Principal optimization route |
|---|---|---|---|
| Unfilled recycled PP / PE | 0.18 – 0.24 | Main drive motor | Reduce screw speed, raise specific throughput per rpm |
| Calcium carbonate filled polyolefin, 30 – 50% | 0.22 – 0.30 | Main drive plus side feeder | Downstream side feeding, shorter kneading train |
| Recycled PET with deep vacuum | 0.24 – 0.32 | Drying plus vacuum system | Heat recovery on dryer, correct vacuum sizing |
| Glass-fiber reinforced PA / PP | 0.28 – 0.35 | Main drive motor | Late fiber addition, low-shear conveying after side feeder |
| High-pigment color masterbatch | 0.28 – 0.35 | Main drive, dispersive kneading | Optimize kneading block stagger angle, control melt temperature |
| Black masterbatch with carbon black | 0.30 – 0.38 | Main drive, distributive mixing | Twin-stage feeding, controlled residence time |
Where the Energy Actually Goes
On a typical waste plastic compounding line, the main drive motor accounts for roughly 55 to 70 percent of total electrical draw, barrel heaters account for 5 to 12 percent in steady state because most heat is generated by shear rather than by heaters, the vacuum system draws 3 to 8 percent, the dryer draws 8 to 20 percent depending on polymer, and the water circuit, chiller, conveying and pelletizer share the remainder. The distribution matters because it identifies where optimization effort pays back. Chasing heater efficiency on a line where heaters consume 8 percent of the total is far less productive than raising specific throughput, which acts directly on the largest consumer.
Specific Throughput as the Practical Control Variable
Specific throughput, measured in kilograms per hour per screw revolution per minute, is the operational handle that controls SEC. Running a barrel at higher screw speed than the formula requires wastes energy as unnecessary shear, raises melt temperature, accelerates degradation and shortens the life of kneading elements. Running at excessive fill with insufficient speed causes surging and pressure instability. The optimum for most recycled polyolefin compounds falls between 0.8 and 1.5 kilograms per hour per rpm on a 71 mm class machine, and finding that window during commissioning typically reduces SEC by 10 to 20 percent against a naive starting setting.
Yield and Quality Control: The Silent Payback Multiplier
Yield is the quietest driver in the model and one of the most persistent. It does not announce itself with an alarm; it accumulates as bags of downgraded pellet in the corner of the warehouse. A plant that improves first-pass yield from 90 to 96 percent gains almost seven percent more saleable output from exactly the same energy, labor and feedstock consumption.
The Six Quality Parameters That Decide Yield
Melt flow rate stability determines whether a compound can be sold against a specification at all. Batch-to-batch variation of more than plus or minus 10 percent on melt flow rate forces downgrading, and the root causes are almost always feedstock inconsistency or feeder drift rather than the extruder itself. Ash content matters for filled and reinforced compounds, where the specification window is often plus or minus 1.5 percentage points and depends entirely on gravimetric feeding accuracy. Black spots are the most common visual rejection cause and originate from carbonized stagnant melt in dead zones, worn barrel and screw clearances, and unfiltered contamination. Strand breakage rate governs the practical utilization of a water strand pelletizing line, since every break requires a manual restring. Pellet length uniformity affects the customer’s own feeding accuracy and is controlled by cutter blade condition, haul-off speed and water bath temperature. Residual moisture in the finished pellet causes splay in the customer’s molding machine and is controlled by dewatering efficiency and pellet drying.
| Quality parameter | Typical specification window | Measurement method | Primary root cause of failure | Yield impact if uncontrolled |
|---|---|---|---|---|
| Melt flow rate stability | ±10% of nominal | Melt flow index tester, one sample per batch | Feedstock variation, feeder drift | 3 – 8 percentage points |
| Ash content | ±1.5 percentage points | Muffle furnace burn-off | Gravimetric feeder calibration | 2 – 5 percentage points |
| Black spots | Visual count per 100 g | Sample plate inspection | Dead zones, worn clearances, filtration gaps | 2 – 6 percentage points |
| Strand breakage rate | <1 break per hour per strand | Operator log | Melt temperature, water bath, die design | 1 – 4 percentage points via utilization |
| Pellet length uniformity | ±0.3 mm on 3 mm target | Caliper sample, sieve analysis | Blade wear, haul-off speed drift | 1 – 3 percentage points |
| Residual pellet moisture | <0.05% for most compounds | Moisture analyzer | Dewatering efficiency, pellet dryer | 1 – 3 percentage points |
Building a Yield Discipline That Holds
Yield discipline is procedural rather than technical. It requires a defined sampling frequency, a written specification for every compound produced, a quarantine area for material awaiting test results, a documented decision rule for downgrading, and a weekly review of loss data by category. Plants that implement this discipline typically add three to five percentage points of first-pass yield within two quarters, which in the index model corresponds to about one month off the recovery timeline for no investment at all.
Technical Levers That Shorten the Recovery Timeline
Beyond operating discipline, a set of specific engineering choices measurably accelerates recovery. Each lever below acts on one or more of the seven drivers, and the combined effect is far larger than any single item.
Screw Configuration Design
Screw configuration is the highest-leverage technical decision on a twin-screw extruder because it determines rate, melt temperature, dispersion quality and energy draw simultaneously. A configuration is assembled from conveying elements of varying pitch, kneading blocks at 30, 45, 60 and 90 degree stagger angles, and reverse-conveying or reverse-kneading elements used to build melt seals. For recycled polyolefin, a short melting section with 45-degree kneading blocks followed by long conveying zones minimizes shear history and keeps melt temperature down. For filled compounds, a distributive mixing section after the side feeder with narrow-disc kneading blocks disperses filler without breaking down the polymer. For reinforced compounds, fiber must be introduced downstream of full melting and conveyed with minimal kneading to preserve fiber length. A configuration that is wrong for the formula can cost 20 percent of rate and several percentage points of yield at the same time.
L/D Ratio Selection
Barrel length expressed as L/D determines how many process functions can be arranged in sequence. A 32 to 36 L/D barrel is adequate for simple re-pelletizing with one atmospheric vent. A 40 L/D barrel accommodates melting, one side feed and one vacuum vent. A 44 L/D barrel adds a second mixing zone or a second vent. A 48 L/D barrel supports full sequential processing with side feeding, twin vacuum stages, downstream reinforcement addition and a stable pressure-building zone before the die. For waste plastic compounding with variable feedstock, 44 to 48 L/D is the practical range, because the extra length buys devolatilization capacity that directly raises uplift grade.
Torque Grade
Specific torque, expressed in newton-meters per cubic centimeter of centerline distance cubed, defines how much work the machine can apply before the drive limits. A machine at 6 to 7 Nm/cm³ is a general-purpose platform. A machine at 8 to 10 Nm/cm³ is a high-torque platform that can hold rate at lower screw speed, which reduces melt temperature, reduces degradation and reduces specific energy consumption all at once. For high-filler recycled compounds, torque grade is often the binding constraint on rate long before screw volume is.
Vacuum Devolatilization Stages
Vent count and vacuum depth control the removal of moisture, monomer, ink solvent, degradation products and entrained air. A single atmospheric vent handles clean, dry feedstock. One atmospheric plus one vacuum vent at minus 0.06 to minus 0.08 MPa handles most recycled polyolefin. Two vacuum stages reaching minus 0.085 to minus 0.095 MPa are required for printed film, recycled PET and odor-sensitive applications. Each added stage raises the uplift grade of the finished pellet, and uplift is the second most powerful driver in the whole model.
Side Feeding
A twin-screw side feeder introduces filler, reinforcement or low-bulk-density material downstream of the melting zone. This solves three problems at once: it removes the feeding bottleneck that limits low-density film, it protects glass fiber from attrition in the melting section, and it prevents filler from interfering with melting efficiency. On filled recycled polyolefin, moving calcium carbonate from main feed to side feed commonly raises rate by 15 to 25 percent on the same machine.
Melt Pump
A gear-type melt pump placed between the extruder and the filtration or die decouples pressure generation from the extruder. This allows the extruder to run at lower discharge pressure and lower melt temperature, stabilizes throughput against feed fluctuations, and improves pellet dimensional consistency. On lines producing to tight specification, a melt pump typically improves yield by one to three percentage points and reduces specific energy consumption slightly by relieving the screw of pressure-building duty.
Screen Changer Selection
Filtration strategy has a direct and often underestimated effect on utilization. A manual plate screen changer requires a full line stop for every change, which on contaminated feedstock at a four-hour interval destroys utilization. A hydraulic plate changer reduces the stop to seconds but still causes a pressure and flow disturbance. A continuous belt screen changer advances filter mesh automatically without stopping flow, holding utilization high even on dirty streams. On mixed post-consumer feedstock, upgrading from manual to continuous filtration can lift utilization by eight to fifteen percentage points, which is worth several months of recovery time on its own.
| Technical lever | Driver affected | Typical magnitude | Investment Index impact | Approximate months saved |
|---|---|---|---|---|
| Correct screw configuration for the formula | Rate, yield, energy | +15 – 20% rate, −10% SEC | Negligible | 3 – 5 |
| 44 – 48 L/D instead of 36 L/D | Uplift grade, yield | +1 vent stage, better dispersion | +4 – 7 points | 2 – 4 |
| High torque grade 8 – 10 Nm/cm³ | Rate, energy | +10 – 20% rate at lower melt temperature | +5 – 9 points | 2 – 3 |
| Second vacuum stage | Uplift grade | Odor and volatile reduction, one grade up | +3 – 5 points | 2 – 4 |
| Twin-screw side feeder | Rate | +15 – 25% on filled or low-density feed | +4 – 6 points | 2 – 3 |
| Melt pump | Yield, energy | +1 – 3 points yield, stable pressure | +4 – 6 points | 0.5 – 1.5 |
| Continuous screen changer | Utilization | +8 – 15 percentage points on dirty feed | +6 – 10 points | 3 – 6 |
| Loss-in-weight gravimetric feeding | Yield, uplift grade | Ash and melt flow rate control within window | +5 – 8 points | 1 – 3 |
Kerke KTE-75D Twin-Screw Compounding Extruder
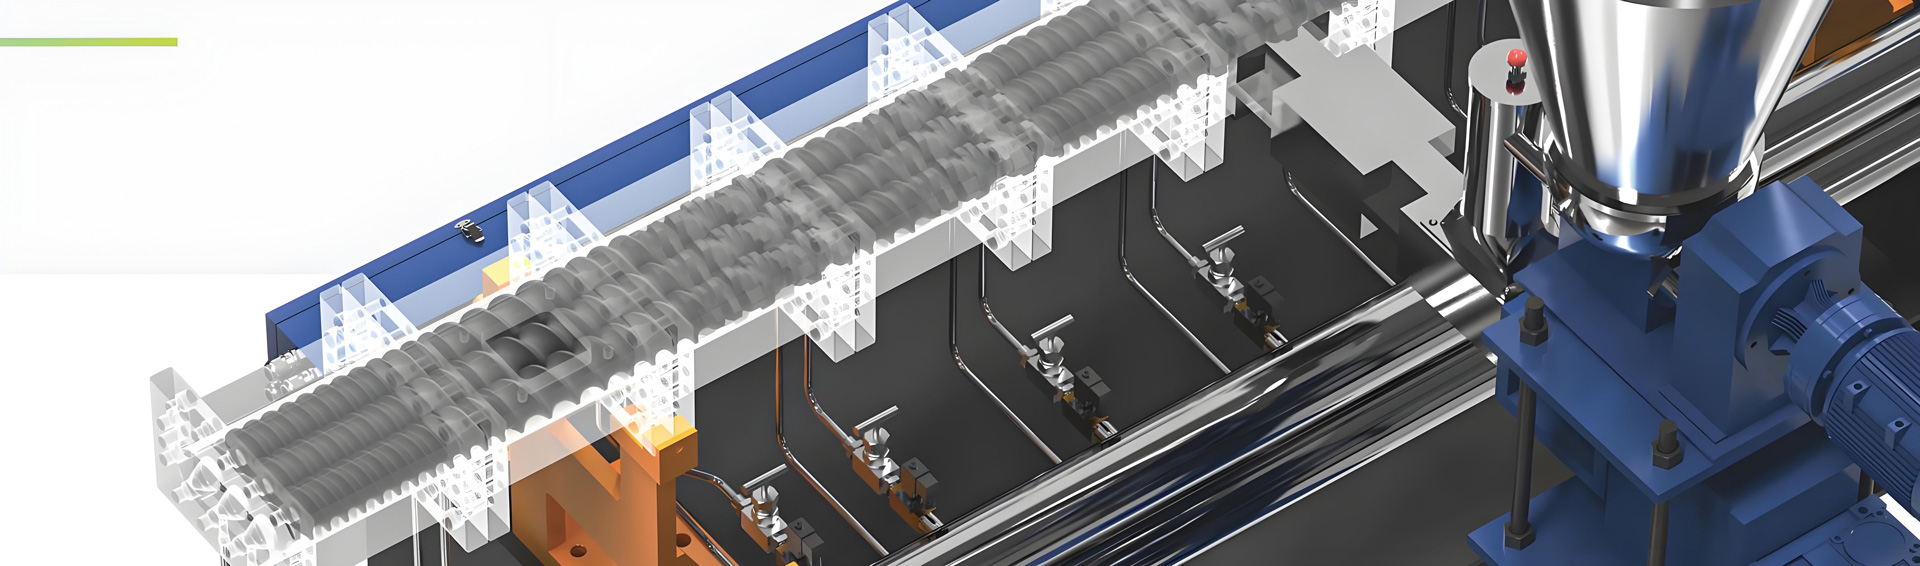
The KTE-75D is the platform used as the reference case throughout this article because it sits at the point where waste plastic compounding becomes an industrial rather than a workshop operation. Built as a parallel co-rotating twin-screw extruder with a computer-aided designed screw assembly and fully intermeshing self-wiping geometry, it covers the output band where most first serious recycling compound lines are specified.
Design Features Relevant to Recovery Time
The KTE-75D uses segmented screw elements and a segmented barrel, so the same machine can be reconfigured for rigid regrind today and reinforced compound next year without replacing the base unit. This modularity matters for the timeline because it removes the risk of a configuration decision locking the plant out of a higher uplift grade later. The self-wiping kneading geometry eliminates most stagnation zones, which directly attacks the black-spot rejection mode that costs yield on recycled feedstock. Barrel sections are individually temperature-controlled with cooling channels, allowing a flat or descending temperature profile that keeps melt temperature down on shear-sensitive recycled polyolefin.
| Parameter | KTE-75D specification |
|---|---|
| Screw outside diameter | 71 mm |
| Centerline distance | 60 mm |
| Screw configuration | Parallel co-rotating, fully intermeshing, segmented |
| L/D ratio | 40 / 44 / 48, selectable by barrel count |
| Maximum screw speed | 500 – 600 rpm |
| Specific torque grade | 8 – 10 Nm/cm³ |
| Installed main motor power | 110 – 160 kW |
| Typical output range | 300 – 800 kg/h, formula dependent |
| Vent configuration | 1 atmospheric + 1 to 2 vacuum stages |
| Barrel construction | Segmented, bimetallic wear-resistant liner option |
| Feeding options | Loss-in-weight main feeder, twin-screw side feeder, crammer feeder, liquid feeder |
| Pelletizing options | Water strand, air-cooled strand, water-ring die face, underwater |
| Typical specific energy consumption | 0.20 – 0.32 kWh/kg depending on formula |
Where the KTE-75D Fits in a Recovery Plan
At 6,500 annual hours, 85 percent utilization and 96 percent yield, a KTE-75D configured at 500 kg/h delivers roughly 2,650 tonnes of accepted compound per year. Specified at 44 to 48 L/D with two vacuum stages, a side feeder and gravimetric feeding, it reaches the Tier B to Tier C configuration band and therefore the 24 to 25 month idealized recovery zone, or roughly 29 to 30 months once the ramp curve is applied. Because output can be pushed toward 800 kg/h on favorable formulas, the same machine also provides headroom for growth without a second commissioning cycle, which is one of the more effective ways to protect a timeline against demand uncertainty.
Kerke KTE-95D Twin-Screw Compounding Extruder
The KTE-95D is the next platform up and is specified when annual demand passes roughly 4,500 tonnes, when filler or reinforcement loading is high, or when a single formula justifies a dedicated line. Its larger centerline distance provides substantially more free volume and torque, which changes the economics of high-filler recycled compounds in particular.
Why a Larger Platform Can Shorten Rather Than Lengthen Recovery
Intuition suggests that a larger machine carries a larger Investment Index and therefore a longer recovery period. In practice the opposite often holds, because installation, plant modification, control systems, laboratory equipment and supervisory labor do not scale linearly with screw diameter. A KTE-95D line may carry an Investment Index around 1.7 times that of a KTE-75D line while delivering roughly 2.2 to 2.5 times the effective output, which improves rather than degrades the ratio. The condition is that the market absorbs the additional tonnage; an oversized line running at 55 percent utilization is the classic way to convert a good machine into a bad timeline.
| Parameter | KTE-95D specification |
|---|---|
| Screw outside diameter | 93 mm |
| Centerline distance | 78 mm |
| Screw configuration | Parallel co-rotating, fully intermeshing, segmented |
| L/D ratio | 40 / 44 / 48, selectable by barrel count |
| Maximum screw speed | 500 – 600 rpm |
| Specific torque grade | 8 – 10 Nm/cm³ |
| Installed main motor power | 250 – 355 kW |
| Typical output range | 800 – 1,800 kg/h, formula dependent |
| Vent configuration | 1 atmospheric + 2 vacuum stages standard |
| Barrel construction | Segmented, bimetallic liner standard for filled and reinforced compounds |
| Feeding options | Multi-channel loss-in-weight array, twin-screw side feeder, liquid injection |
| Filtration options | Hydraulic plate, continuous belt screen changer, melt pump |
| Typical specific energy consumption | 0.19 – 0.30 kWh/kg depending on formula |
Indicative Recovery Comparison Between the Two Platforms
| Item | KTE-75D line | KTE-95D line |
|---|---|---|
| Configured rate | 500 kg/h | 1,200 kg/h |
| Annual hours | 6,500 | 6,500 |
| Utilization | 85% | 85% |
| First-pass yield | 96% | 96% |
| Effective annual output | 2,652 t | 6,365 t |
| Effective monthly output | 221.0 t | 530.4 t |
| Unit Contribution Index | 1.00 | 1.02 |
| Monthly Contribution Index | 4.00 | 9.79 |
| Investment Index | 100 | 172 |
| Idealized payback | 25.0 months | 17.6 months |
| Condition for validity | Demand for 2,650 t/year | Demand for 6,350 t/year |
The comparison is only valid if the market genuinely absorbs the larger tonnage. If the same KTE-95D line runs at 55 percent utilization because orders do not materialize, its effective monthly output falls to 343 tonnes, the Monthly Contribution Index falls to 6.33, and the idealized payback stretches to 27.2 months, which is worse than the smaller machine. Sizing discipline is therefore a timeline decision, not just a capacity decision.
Application Industries That Set the Value-Uplift Index
The uplift grade that drives the recovery timeline is decided by the application the compound serves, not by the equipment that produces it. Kerke twin-screw compounding lines are deployed across the full spread of uplift grades, and understanding where each application sits helps a recycler position the plant deliberately rather than by accident.
Masterbatch Production
Color masterbatch, filler masterbatch, black masterbatch, additive masterbatch and textile masterbatch all sit at the higher end of the uplift range because the finished product is a concentrated functional additive rather than a bulk resin. Color masterbatch for injection-molded housewares, black masterbatch for pipe and cable jacketing, and filler masterbatch for woven bags and thin-wall packaging are the most common lines. These applications demand dispersive mixing quality, tight color consistency and low contamination, which is exactly what a high-torque twin-screw with gravimetric feeding and fine filtration delivers.
Engineering and Modified Compounds
Glass-fiber reinforced polyamide for automotive under-hood brackets, cooling fan housings and structural clips, reinforced polypropylene for battery trays and appliance frames, and toughened blends for power tool housings all sit at the Very High uplift grade. These compounds require late fiber addition through a side feeder, wear-resistant barrel liners, twin vacuum stages and consistent melt flow rate control. They also demand documented quality records, which is why the higher configuration tiers pay for themselves through market access rather than through throughput.
Recycling and Re-Pelletizing
Recycled polyolefin pellets for irrigation pipe, crates, pallets, refuse sacks and construction sheeting sit in the Low to Medium uplift band. Recycled PET flakes converted into fiber-grade or strapping-grade pellet sit higher because of the drying and devolatilization work involved. This is the category where feedstock discipline determines everything: the same equipment produces a commodity pellet or a certified technical pellet depending on how tightly the incoming stream is controlled. For upstream washing and drying, Wanplas supplies matched washing lines that integrate directly with Kerke compounding systems, so a recycler can specify the whole chain within one brand relationship.
Cable, PVC and Elastomer Compounds
Cable compounding covers insulation and jacketing compounds, low-smoke halogen-free formulations and semi-conductive shields, all of which sit at High to Very High uplift. PVC compounding covers rigid and flexible formulations for profile, pipe and wire. Thermoplastic elastomer compounds serve automotive sealing, soft-touch overmolding and footwear. Wood-plastic composite compounds serve decking, fencing and cladding, and are notable for combining a recycled polymer fraction with a high natural-fiber loading, which puts real demand on side feeding and devolatilization.
Biodegradable and Specialty Food-Related Compounds
Biodegradable compounds based on starch blends and polyester chemistry require careful thermal management because the polymers degrade in narrow temperature windows. Kerke lines are also applied to pet food processing and textured vegetable protein processing, where the same co-rotating twin-screw principle is used for a completely different material system. These specialty applications sit at Premium uplift grades and normally justify Tier C or Tier D configurations.
Requirement-to-Model Selection Guide
Selecting the right platform is the decision that fixes the achievable ceiling on the recovery timeline. The table below maps target annual output, feedstock type and filler or reinforcement loading to the appropriate Kerke model, assuming three-shift operation at 6,500 effective hours per year.
| Target annual output (three shifts) | Feedstock type | Filler or reinforcement loading | Recommended Kerke model | Suggested L/D | Configuration notes |
|---|---|---|---|---|---|
| Formula development, 5 – 30 kg/h | Any, trial quantities | 0 – 60% | KTE-16B laboratory twin screw extruder | 40 – 48 | Scale-up geometry matched to production platforms |
| 600 – 1,200 t | Clean rigid PP / PE regrind | 0 – 20% | KTE-52D | 40 – 44 | One vacuum vent, loss-in-weight main feeder |
| 1,200 – 2,500 t | Rigid regrind with film blend | Up to 40% | KTE-65B | 44 | Side feeder for filler, hydraulic screen changer |
| 2,500 – 4,500 t | Mixed rigid PP / PE, PET flakes | Up to 50% | KTE-75D | 44 – 48 | Two vacuum stages, side feeder, melt pump optional |
| 4,500 – 9,000 t | PET flakes, PA scrap, high-filler polyolefin | Up to 60% | KTE-95D | 48 | Bimetallic liners, continuous screen changer, gravimetric array |
| 9,000 – 20,000 t | Single dedicated formula, high volume | Up to 70% | KTE-135D | 48 | Underwater pelletizing, full data capture, melt pump standard |
| 200 – 4,500 t, simple re-pelletizing | Heavily contaminated film, no compounding required | 0 – 10% | SE series single screw extruder, 30 – 800 kg/h | — | Lower uplift grade, lower investment index, longer payback per tonne |
| Special materials requiring two-stage processing | Heat-sensitive or highly volatile streams | Variable | KTE-SE double-stage extrusion system | — | Mother-baby arrangement, decoupled devolatilization and pelletizing |
How to Use the Table Against a Timeline Target
Work backward from the recovery target rather than forward from the equipment catalog. Decide the acceptable recovery window in months, decide the realistic uplift grade the local market supports, then compute the required Monthly Contribution Index from the payback expression. Convert that index into required effective monthly tonnage using the reference scaling, then divide by utilization, yield and annual hours to obtain the required nameplate rate. Only then select the model. This sequence prevents the most common sizing error, which is buying the largest machine the budget allows and discovering that the market cannot fill it.
Operating Burden Structure Expressed as Ratios
Operating burden is included here only to the extent that it shapes the Unit Contribution Index and therefore the recovery timeline. Expressed as ratios rather than absolute values, the structure is remarkably stable across regions, which makes it a useful diagnostic tool: a plant whose ratios deviate sharply from the typical band usually has a specific identifiable problem.
| Burden element | Typical share of total conversion burden | Deviation signal | Effect on recovery timeline if out of band |
|---|---|---|---|
| Electricity | 28 – 38% | Above 40% indicates excessive screw speed or oversized drive running unloaded | +1 to +2 months |
| Labor | 14 – 22% | Above 25% indicates manual handling that should be automated | +2 to +3 months |
| Additives and carriers | 12 – 20% | Above 22% indicates over-formulation or poor dispersion forcing higher dosing | +1 to +2 months |
| Wear parts and spares | 8 – 13% | Above 15% indicates abrasive feedstock without wear-resistant specification | +1 to +2 months |
| Maintenance and utilities | 6 – 10% | Above 12% indicates reactive rather than planned maintenance | +1 month, plus utilization loss |
| Scrap and off-specification loss | 4 – 10% | Above 12% indicates feedstock variability or feeder drift | +2 to +4 months |
| Overhead and administration | 8 – 12% | Above 15% usually indicates under-utilized capacity | Varies with utilization |
Read as a diagnostic rather than as a budget, this table answers a specific question: when a plant discovers that its recovery period is running behind forecast, which ratio should be examined first. In practice the two ratios that most often sit out of band on waste plastic lines are scrap loss and labor, and both are addressable without capital work.
Wear Part Life and Replacement Intervals
Wear parts influence the recovery timeline through two separate channels: the direct burden of replacement, and the indirect utilization loss caused by the stoppage. On a well-planned line the second channel is larger than the first, which is why replacement should be scheduled rather than triggered by failure.
| Component | Typical service life | Wear indicator | Consequence of running past life | Recommended action |
|---|---|---|---|---|
| Conveying screw elements | 8,000 – 12,000 h | Outside diameter reduction, rising torque at constant rate | Reduced conveying efficiency, rate loss | Measure at every planned shutdown, replace as a set |
| Kneading blocks | 6,000 – 10,000 h | Tip rounding, loss of dispersion quality | Poor dispersion, gel formation, ash variation | Keep one spare set on site, rotate at planned stop |
| Barrel liners, bimetallic | 10,000 – 20,000 h | Bore diameter growth, clearance increase | Back-flow, black spots, rate and pressure loss | Bore measurement annually, replace section by section |
| Barrel liners, nitrided | 6,000 – 12,000 h | Same as above, faster on filled compounds | Same as above | Specify bimetallic for abrasive formulas from the outset |
| Strand pelletizer blades | 2,000 – 4,000 h | Pellet length variation, fines increase | Off-specification pellet geometry, customer complaints | Regrind or replace on schedule, keep two sets |
| Water-ring die face blades | 1,500 – 3,000 h | Tails on pellets, die face scoring | Fused pellets, die plate damage | Inspect weekly, replace on schedule |
| Filter screens | 4 – 24 h per change | Melt pressure rise before filter | Pressure excursion, throughput loss, screen rupture | Set a pressure trigger, move to continuous filtration on dirty feed |
| Gearbox oil | 4,000 h or annually | Oil analysis, temperature rise | Bearing wear, gear pitting, unplanned failure | Scheduled change with oil sampling record |
| Vacuum pump service | 4,000 h | Vacuum level shortfall | Volatile carry-over, odor and gel defects | Service during planned stops, keep seal kit on site |
| Die plate | 10,000 – 20,000 h | Hole erosion, uneven strand flow | Strand breakage, yield loss | Inspect at every major shutdown |
Planned Versus Reactive Replacement
The arithmetic is simple. A planned kneading block change during a scheduled weekend stop costs zero production hours. The same change executed after a dispersion failure costs the stoppage, the scrap produced while the defect went undetected, the downgraded inventory and often a customer complaint. Across a full recovery period, a plant that runs planned replacement typically holds two to four percentage points more utilization than a plant that runs to failure, which is worth roughly one to two months of recovery time.
Risk Factors and Hedging the Timeline
A recovery forecast is a statement about the future and therefore carries risk. Naming the risks explicitly, with early indicators and hedges, converts a fragile forecast into a managed one.
| Risk factor | Early indicator | Timeline impact if unmanaged | Practical hedge |
|---|---|---|---|
| Feedstock quality variability | Rising melt flow rate spread between batches, more frequent screen changes | +4 to +8 months | Incoming inspection protocol, two qualified suppliers, blending silo before extrusion |
| Feedstock availability | Falling inventory cover, longer lead times | Utilization loss of 10 to 20 percentage points | Contracted supply, ability to run a second polymer family on the same line |
| Order volatility | Widening gap between planned and actual monthly tonnage | +5 to +15 months | Multi-application product portfolio, segmented screw for fast changeover |
| Environmental compliance | New emission or wastewater requirements in permits | Unplanned stoppage plus investment index increase | Specify dust extraction, odor abstraction and closed water circuit at design stage |
| Electricity supply instability | Voltage dips, unplanned trips, load shedding notices | Utilization loss and scrap on every restart | Soft-start drives, controlled shutdown procedure, purge routine, stabilized supply |
| Skilled personnel turnover | Rising defect rate after shift changes | +2 to +4 months | Documented work instructions, recipe management in the control system, cross-training |
| Specification tightening by customers | Increasing rejection rate on unchanged process | Yield loss of 3 to 6 percentage points | Upgrade filtration and feeding accuracy, install online monitoring |
| Delayed commissioning | Utility works incomplete when equipment arrives | +1 to +3 months directly | Utility readiness checklist agreed before shipment, pre-shipment testing |
Building Slack Into the Forecast
Experienced project teams add explicit contingency rather than pretending risk does not exist. A defensible approach is to run the base scenario as the planning case, hold the conservative scenario as the stress case, and require that the project remain viable under the conservative case before committing. If the project only works under optimistic assumptions, the correct response is to change the configuration, the shift pattern or the product positioning until it also works under conservative assumptions.
Certification and Factory Acceptance Testing
Factory acceptance testing is the single most effective mechanism for protecting the early months of the recovery timeline, because it moves discovery of problems from the customer’s floor to the manufacturer’s floor. Kerke operates under an ISO 9001 quality management framework and supplies CE-compliant machines for markets that require it, and every line is run before shipment rather than shipped on drawings alone.
What a Meaningful Acceptance Test Contains
| Acceptance item | Test method | Acceptance criterion | Why it protects the timeline |
|---|---|---|---|
| Continuous operation | Uninterrupted run on the agreed formula | Stable operation over the contracted test duration without unplanned stop | Exposes thermal, feeding and control faults before shipment |
| Output rate verification | Timed collection and weighing at steady state | At least 95% of contracted kg/h on the agreed formula | Protects the output term in the contribution index |
| Specific energy consumption | Line power meter divided by collected pellet mass | Within the agreed kWh/kg band | Validates the energy assumption in the model |
| Melt temperature stability | Melt thermocouple at die adapter over the run | Within ±3 °C at steady state | Predicts degradation risk and yield stability |
| Melt pressure stability | Pressure transducer before screen changer | Fluctuation within the agreed band | Predicts pellet uniformity and strand behavior |
| Vacuum performance | Gauge reading at each vent port under load | −0.085 to −0.095 MPa on deep vacuum stages | Confirms devolatilization capacity and uplift grade |
| Pellet geometry | Sample sieve analysis and caliper measurement | Length within ±0.3 mm of target, fines below the agreed limit | Protects first-pass yield |
| Feeder accuracy | Catch test on each loss-in-weight feeder | Within the agreed percentage of setpoint | Controls ash content and melt flow rate consistency |
| Safety and electrical verification | Interlock, emergency stop, guarding, insulation and grounding checks | All functions verified, documentation issued | Prevents commissioning delays and compliance stoppages |
| Noise and working environment | Measurement at operator positions | Within the agreed limit | Supports permitting and personnel retention |
Documentation That Travels With the Machine
A complete document package shortens commissioning measurably. It should include the screw configuration drawing with element sequence, barrel layout with vent and side feed positions, electrical schematics, the parameter set used during the acceptance test, the recorded test data, spare part lists with recommended stock levels, lubrication schedules and operator instructions. Plants that receive this package typically reach qualified output one to two months earlier than plants that have to reconstruct the process from scratch.
Service and Support During the Recovery Period
The recovery period is precisely the window in which a plant is least able to absorb an unplanned failure, because the ramp curve is still climbing and there is no accumulated buffer. Kerke structures its support package around that reality, and shares the service commitments that apply across the Wanplas brand.
Before Shipment
Every machine is tested before it leaves the factory. Where the customer supplies representative feedstock, trial runs are performed on the actual material rather than on virgin resin, which is the only way to validate a screw configuration for waste plastic. Laboratory-scale trials on a KTE-16B class extruder are available for formula development before the production machine is finalized, allowing the screw configuration to be corrected on paper rather than in the customer’s plant. Customers are welcome to attend the test in person under the open-factory policy that applies across all Wanplas factories.
Installation and Commissioning
Kerke engineers attend site for mechanical alignment, electrical verification, utility connection checks, first heating, first melt, screw configuration confirmation and process parameter setting. Commissioning includes establishing the initial parameter set for each compound the plant intends to run, together with the corresponding screw configuration if changeover is planned.
Training
Operator training covers start-up and shutdown sequences, purge procedures, screw and barrel changeover, screen change technique, pelletizer adjustment and defect recognition. Maintenance training covers lubrication schedules, wear measurement, alignment checks, vacuum system service and spare part identification. Training the maintenance team properly is one of the more reliable ways to protect utilization during the ramp.
Spare Parts and Remote Support
The Wanplas group commitment of USD 500 free parts every year applies to Kerke machines, alongside free replacement of parts damaged within the warranty period. Remote diagnostic support allows engineers to review control system data and guide operators through fault isolation without waiting for travel. Recommended on-site stock for a waste plastic line typically includes one spare kneading block set, one set of pelletizer blades, filter screens in the required mesh range, thermocouples, heater bands and vacuum pump seals.
Long-Term Partnership
Kerke supports capacity expansion by reconfiguring existing machines, adding barrel sections to raise L/D, adding a second vacuum stage, upgrading feeding from volumetric to gravimetric, or converting pelletizing from water strand to water-ring or underwater systems. Because the KTE series uses segmented barrels and segmented screws, most of these upgrades can be executed during a planned shutdown rather than requiring a new machine, which protects the timeline of the original investment while extending the capability of the plant.
Frequently Asked Questions
How long will it take to recover investment of waste plastic twin screw compound line equipment in practice?
Using the index model in this article, a standard-configuration line running three shifts at 85 percent utilization and 96 percent first-pass yield returns an idealized recovery period of 25.0 months, because 100 investment index points divided by 4.00 monthly contribution index points equals 25. Adding the first-year ramp curve, during which only 28.3 index points are recovered, extends the realistic figure to about 29.9 months. A two-shift plant on commodity-grade output can stretch past fifty months, while an experienced compounder on near-continuous operation with High uplift positioning can approach eighteen months.
Why does this article avoid quoting any figures of money?
Because monetary figures for equipment, feedstock, energy, labor and finished compound vary by region, by contract and by month, any absolute figure would be wrong for most readers within a quarter. The index method keeps the structure of the calculation intact while letting each reader substitute their own local values. The relationships between utilization, yield, energy, uplift and recovery time are stable engineering relationships, and those are what the model captures.
Is it better to buy a smaller line first and expand later, or size for the target from the start?
Sizing for the realistic three-year target from the start is usually faster in time, provided the market can absorb the tonnage. Expanding later forces a second installation, a second commissioning cycle and a second customer qualification round, and each of those consumes months of contribution that the first machine has to carry alone. The exception is a plant entering an unproven market, where a KTE-52D or KTE-65B first step limits exposure and can be upgraded through added barrel sections and improved feeding rather than replaced.
How much does moving from two shifts to three shifts really change the timeline?
It is the largest single lever available. Annual effective hours rise from about 4,000 to about 6,500, which raises effective output by 62 percent with no change to the machine. In the index model the monthly contribution index rises from 2.46 to 4.00 and the idealized recovery period falls from 40.7 months to 25.0 months. The additional requirement is labor organization and a maintenance strategy that fits into shorter windows.
What first-pass yield should a new waste plastic compounding plant target?
Target 90 percent in the first six months, 94 percent by the end of the first year and 96 percent at steady state on a defined feedstock. Yields above 97 percent are achievable on clean rigid regrind with gravimetric feeding and continuous filtration, but chasing them on mixed post-consumer material is usually less productive than improving incoming feedstock discipline.
Does a melt pump or continuous screen changer really pay for itself?
On dirty feedstock, yes. A continuous screen changer can lift utilization by eight to fifteen percentage points where manual changes were previously required every four to eight hours, which is worth three to six months of recovery time against an investment index increase of six to ten points. A melt pump has a smaller effect, typically one to three percentage points of yield, and is justified mainly where pellet consistency is contractually specified.
How does drying affect the recovery period for recycled PET?
Drying is not optional for recycled PET. Without crystallizing and drying to a dew point of minus 40 degrees Celsius and residual moisture below 50 ppm, hydrolytic degradation reduces intrinsic viscosity in a single pass and the output falls out of specification, destroying both yield and uplift grade. The dryer consumes 8 to 20 percent of line energy, which slightly reduces the Unit Contribution Index, but the alternative is a product that cannot be sold at technical grade at all.
What is the most common reason a real plant misses its forecast recovery period?
Utilization, not machine performance. Forecasts are usually built on assumed running hours that never materialize because of feedstock gaps, unplanned maintenance, quality holds and order shortfalls. The second most common reason is uplift positioning: plants that intended to sell qualified technical compound end up selling commodity re-pelletized material, which cuts the Unit Contribution Index by 30 percent or more and stretches the timeline accordingly.
Conclusion
The question of how long it will take to recover investment of waste plastic twin screw compound line equipment has a precise answer once it is asked precisely. Set the total installed investment at 100 index points, express monthly contribution in the same index points, and the recovery period falls out as a simple ratio. A standard three-shift line at 85 percent utilization and 96 percent yield returns 25.0 months idealized and about 29.9 months once the ramp curve is honestly included. A conservative two-shift commodity operation stretches to 56.4 months. An experienced compounder on near-continuous operation with High uplift positioning reaches 17.8 months. The spread of more than three to one comes almost entirely from operating decisions rather than from the extruder.
That is the practical message for anyone planning a waste plastic compounding project. Fix the shift pattern first, because it is worth more than fifteen months. Fix the product positioning second, because uplift grade is worth ten to eleven months. Then specify the machine properly, because a Tier A configuration saves fifteen index points of investment and gives back nearly eight months of recovery time, which is the wrong trade in almost every case. Choose 44 to 48 L/D, a high torque grade, sufficient vacuum stages, a side feeder sized for the feedstock, gravimetric feeding and a filtration strategy matched to contamination level, and the timeline takes care of itself.
Kerke Extrusion Equipment, a Wanplas factory with more than twelve years of dedicated twin-screw experience, a facility of over 19,997 square meters, more than 2,000 machines running in over 70 countries and a team of more than 100 people, builds the KTE series from KTE-16B laboratory units to KTE-135D production platforms, together with SE series single screw extruders from 30 kg/h to 800 kg/h, loss-in-weight feeding systems and matched pelletizing equipment. Every machine is tested before shipment, installed and commissioned by Kerke engineers, backed by operator and maintenance training, remote diagnostic support and the Wanplas commitment of USD 500 free parts every year.
If a recovery timeline is being prepared for a new or expanding compounding plant, send the intended feedstock description, the target annual tonnage, the shift pattern under consideration and the specification of the compound to be produced. Kerke engineers will return a configuration proposal with screw layout, L/D recommendation, vent arrangement, feeding scheme and expected specific energy consumption, and will run a trial on representative material before anything is built. Visitors are welcome at the factory to watch a machine of the proposed configuration run under load, because the fastest way to protect a recovery timeline is to verify the assumptions before the first index point is committed.