- What “Low Cost” Really Means in Recycled Compounding
- Why Devolatilization Is the Foundation of Any Recycled Formula
- Devolatilization Engineering on a Twin-Screw Extruder
- Feedstock Characterization Before Formulating
- Recycled PP Formula Family
- Recycled PE Formula Family
- Recycled PET Formula and Intrinsic Viscosity Recovery
- Mixed Polyolefin Low-Cost Formula
- Additive Cost-Effectiveness Ranking
- Odor and VOC Reduction Without Expensive Additives
- Screw Configuration for Recycled Compounding
- Process Window Tables by Material
- Kerke KTE Series Twin Screw Extruder
- Kerke Feeding and Auxiliary Systems
- Melt Filtration and Black Spot Control
- Quality Control Plan for Recycled Compounds
- Requirement to Machine and Formula Selection Table
- Common Problems and Fixes
- Service and Support
- Frequently Asked Questions
- Conclusion
Building a low cost recycled plastic modification formula for a twin screw devolatilization extruder is not an exercise in buying cheaper additives. It is an exercise in removing the invisible contaminants that make recycled resin behave unpredictably, and then spending the smallest possible additive budget to pull mechanical properties back into a usable window. Compounders who reverse that order — dosing impact modifier, compatibilizer and odor scavenger into a wet, volatile-laden regrind stream — consistently pay more per accepted kilogram and still lose customers to smell complaints and black specks.
Recycled polyolefins and polyesters arrive at the hopper with four handicaps that virgin resin does not have: a broadened and shifted molecular weight distribution from prior heat histories, absorbed moisture, low molecular weight degradation products that carry odor, and residual print ink, adhesive and fragrance from the article’s first life. Every one of those handicaps is addressed more cheaply by devolatilization hardware and screw geometry than by chemistry. That is the central engineering argument of this guide, and it is why the devolatilization section of a twin-screw compounding line deserves as much design attention as the kneading section.
Kerke Extrusion Equipment, a Wanplas factory, has spent more than twelve years designing parallel co-rotating twin-screw compounding extruders for exactly this class of difficult, variable feedstock. From a 19,997 square meter manufacturing base, Kerke has placed more than 2,000 machines in over 70 countries, supported by a technical team of more than 100 people whose slogan — “We Know Compounding Extruder” — reflects a narrow, deliberate specialization in the KTE series of parallel co-rotating twin-screw extruders, from the KTE-16B laboratory unit up to the KTE-135D production machine. This guide sets out the formula families, screw configurations, vent settings, process windows and quality control routines that Kerke’s application engineers use when a customer’s brief is simply: make this recycled material cheap, stable and sellable.
Everything that follows is written in relative cost language. Where a cost comparison is needed, this article uses Low, Medium, High, Very High and Premium ratings, or an index in which a baseline recipe equals 100 index points. Absolute prices move weekly with resin, energy and freight markets and would be misleading in a technical reference; the relationships between formula choices, however, are stable and are what a process engineer actually needs.
1. What “Low Cost” Really Means in Recycled Compounding
Low cost in recycled compounding is a three-part equation: additive loading, yield, and specific energy consumption. Most compounders track only the first, which is why so many “cheap” formulas are expensive in practice. The dominant hidden cost in this business is not the additive package at all — it is batch-to-batch instability that triggers downstream rejection, and the resulting loss of a qualified customer who then re-qualifies with virgin resin.
Consider the arithmetic. An additive package typically represents a modest share of a filled recycled polyolefin compound’s total material cost. Trimming that package by a fifth produces a small saving on the material index. A single returned lot, by contrast, absorbs the freight both ways, the reprocessing labor, the machine hours to rerun, and — most damaging — the customer’s confidence. When a converter has to stop a running injection molding machine because impact strength dropped between two pallets of the same compound grade, the compounder rarely gets a second chance to explain that the regrind bale changed.
The three real cost drivers
| Cost driver | What it covers | Typical share of total cost | How much a formula engineer can move it | Cost sensitivity |
|---|---|---|---|---|
| Base feedstock | Washed regrind, flakes, bale-sorted material, in-house scrap | Largest single block | Moderate — controlled mostly by sourcing and sorting discipline | High |
| Additive package | Antioxidants, compatibilizer, impact modifier, filler, lubricant, odor adsorbent, chain extender | Small to moderate | Large in percentage terms, small in absolute terms | Medium |
| Yield and rejection | Start-up scrap, off-spec lots, screen change losses, customer returns | Highly variable, often underestimated | Very large — the single biggest lever | Very High |
| Specific energy consumption | Motor load, barrel heating, vacuum pump, chiller, pelletizer drives | Moderate and rising | Moderate — screw design and melt temperature control | Medium |
| Labor and downtime | Screen changes, screw cleaning, die changes, purging | Moderate | Moderate — self-wiping geometry and continuous filtration | Medium |
Read that table as a priority list. The additive package is the most visible cost and the easiest to cut, which is exactly why it is cut too aggressively. Yield is the least visible and the most valuable. A formula that adds 0.1 phr of secondary antioxidant and thereby holds melt flow rate within a narrower band across twenty consecutive lots is a cheaper formula, even though its bill of materials index is higher.
A relative cost index for comparing recipes
To keep recipe comparisons honest without quoting money, this article uses a simple index. An economy recycled polypropylene compound with a minimal antioxidant package and no impact modifier is defined as 100 index points on the material axis. Other recipes are expressed relative to that baseline. A separate quality axis tracks the probability that a lot meets specification on first pass.
| Recipe tier | Material cost index (baseline = 100) | First-pass acceptance | Effective cost per accepted kilogram | Verdict |
|---|---|---|---|---|
| Bare economy, no devolatilization | 96 | Low | Highest of the four | False economy |
| Economy with two-stage devolatilization | 100 | Medium to High | Low | Best value for commodity parts |
| Standard with compatibilizer and impact modifier | 108 to 114 | High | Low to Medium | Best value for technical parts |
| High-performance with full stabilization | 118 to 128 | Very High | Medium | Justified only by specification |
The first row is the trap. Removing the vacuum vent, running a shorter barrel and skipping the secondary antioxidant lowers the visible index by four points and destroys first-pass acceptance. This is the most common mistake among new entrants to recycled compounding, and it is a hardware mistake disguised as a formula mistake.
2. Why Devolatilization Is the Foundation of Any Recycled Formula
Devolatilization is the foundation of any recycled formula because volatiles consume additives, disrupt melt continuity and carry the odor that ends most commercial conversations. Additives dosed into an undevolatilized melt are partly spent neutralizing species that a vacuum port would have removed for the cost of electricity alone.
Recycled polymer streams carry four distinct classes of volatile matter, and each behaves differently in the barrel.
Class one: moisture
Water arrives with washed and mechanically dewatered flake, and is also absorbed from ambient humidity during storage. Polyolefins are not hygroscopic in the chemical sense, but flake geometry holds surface water stubbornly — 0.3 to 1.5 percent by weight is common after centrifugal dewatering alone. Polyester and polyamide streams absorb water into the polymer itself and hydrolyze at melt temperature, cleaving chains and dropping intrinsic viscosity irreversibly. Moisture that reaches the melt zone flashes to steam, causes surging at the die, produces voids in the strand and prints as silver streaks in downstream molded parts.
Class two: residual monomer and oligomers
Every polymer contains a small residual fraction of monomer, dimer and low molecular weight oligomer. In recycled streams this fraction grows because previous processing cycles generated chain scission products. Polyester regrind carries acetaldehyde and cyclic trimer; styrenics carry residual styrene; polyolefins carry short-chain paraffins and olefinic fragments. These species are volatile at melt temperature and are exactly what a deep vacuum port is designed to strip.
Class three: thermo-oxidative degradation products
This is the odor class that customers complain about. Repeated heat histories in the presence of oxygen generate aldehydes, ketones and carboxylic acids on the polymer backbone and as free small molecules. Short-chain aldehydes in particular have very low odor thresholds — a few parts per million in the headspace is enough for a human nose to register the smell in a finished part. No practical additive loading removes them once they are formed in bulk; the correct response is to strip the existing ones under vacuum and to prevent the formation of new ones with an efficient antioxidant system and a conservative melt temperature.
Class four: residual ink, adhesive, fragrance and product residue
Post-consumer packaging carries printing ink solvents, hot-melt adhesive fractions, label varnish, and fragrance or surfactant residue from the original contents. Detergent and personal-care bottles are notorious for this. These compounds are chemically diverse, often relatively high boiling, and are the reason that a single atmospheric vent is rarely enough. Deep vacuum, sufficient residence time in the vented zone, and in stubborn cases steam stripping are the tools that work.
| Volatile class | Typical species | Typical level in post-consumer regrind | Removal method | Consequence if left in |
|---|---|---|---|---|
| Moisture | Free and absorbed water | 0.3 to 1.5 percent (polyolefin flake); 0.2 to 0.6 percent (polyester flake) | Pre-drying plus atmospheric vent | Surging, voids, silver streaks, hydrolysis of polyester |
| Monomer and oligomer | Acetaldehyde, cyclic trimer, short paraffins | Tens to hundreds of parts per million | Vacuum vent at minus 0.085 to minus 0.095 MPa | Odor, taste transfer, blooming |
| Degradation products | Aldehydes, ketones, carboxylic acids | Variable, rises with each heat history | Vacuum vent plus antioxidant plus lower melt temperature | Strong odor, yellowing, further chain scission |
| Ink, adhesive, fragrance | Solvents, resin fractions, terpenes, surfactants | Highly variable by source | Deep vacuum, longer vented residence, steam stripping | Odor, black specks, gel formation, color drift |
3. Devolatilization Engineering on a Twin-Screw Extruder
Effective devolatilization on a twin-screw extruder is a two-stage job: an atmospheric vent that releases the bulk of steam and easy volatiles early, followed by a vacuum vent operating at minus 0.080 to minus 0.095 MPa that strips the low molecular weight residue after the melt is fully homogeneous. Attempting both duties at a single port is the most frequent design shortcut in recycled compounding, and it is the reason many lines cannot hit an odor specification regardless of formula.
Stage one: the atmospheric vent
The atmospheric vent sits shortly after the first melting section, typically between 14 and 22 L:D depending on total barrel length. At this point the material is molten but the melt is still relatively open and gas can escape without a pressure driving force. The vent’s job is quantity, not refinement: it releases the steam load from surface moisture and the most volatile fraction. Running an atmospheric vent hot enough to keep the port free of condensate — but not so hot that condensed oligomer bakes into a crust — is a small detail with large maintenance consequences. A port jacket held near the barrel setpoint, with an easily removable insert, is the practical answer.
Stage two: the vacuum vent
The vacuum vent belongs in the last third of the barrel, after the final mixing section and before the pressure build-up zone. By this point the compound is homogeneous, the filler is dispersed, and any remaining volatiles are the difficult ones. Vacuum level is the primary lever:
| Vacuum level (gauge) | Achievable residual volatile content | Typical odor improvement | Equipment requirement | Energy cost level |
|---|---|---|---|---|
| Atmospheric only | Baseline | None | Open vent port | Low |
| Minus 0.05 to 0.07 MPa | 30 to 45 percent reduction | Around half a VDA 270 grade | Single-stage water ring pump | Low |
| Minus 0.080 to 0.090 MPa | 55 to 70 percent reduction | Around one VDA 270 grade | Water ring pump with good sealing water cooling | Medium |
| Minus 0.090 to 0.095 MPa | 70 to 85 percent reduction | One to one and a half VDA 270 grades | Two-stage pump or pump with booster, tight barrel sealing | Medium to High |
| Deep vacuum with steam stripping | Above 85 percent reduction | Up to two VDA 270 grades | Water injection port, stripping section, condenser | High |
Screw elements in the vent zone
The vent zone is a screw design problem before it is a vacuum pump problem. Three rules govern it:
Shallow-channel, long-pitch conveying elements under the port. Long pitch reduces the degree of fill and increases free surface area, which is what drives mass transfer of volatiles out of the melt. A degree of fill above roughly 30 percent under the port sharply reduces stripping efficiency and raises the risk of material creeping up the vent throat.
A sealing element before the port. A short reverse-pitch or narrow kneading block upstream of the vent creates a melt seal that prevents vacuum from propagating backwards toward the feed opening. Without it, deep vacuum pulls unmelted feed and powder additive directly into the vent line.
A pressure-building element after the port. Downstream of the vent, conveying pitch is reduced progressively to rebuild pressure for the melt filter and die. That transition should be gradual; an abrupt pressure jump immediately after a vacuum port raises local shear and can undo the temperature discipline the formula depends on.
| Vent zone element | Function | Typical geometry | Design note |
|---|---|---|---|
| Upstream melt seal | Isolates vacuum from feed zone | Narrow kneading disc block or short reverse element | Keep short — a long seal wastes barrel length and adds shear |
| Vent conveying section | Maximizes free surface for mass transfer | Long-pitch, shallow-channel conveying, 3 to 5 L:D | Target degree of fill below 30 percent |
| Vent stuffer (optional) | Prevents melt creeping into the vacuum throat | Twin-screw side stuffer driven at low speed | Essential above 800 kg/h or with low viscosity melt |
| Downstream transition | Progressive pressure rebuild | Stepped-down pitch conveying, 4 to 6 L:D | Avoid a single abrupt pitch change |
| Water injection port | Steam stripping for stubborn odor | Metered water injection into a filled zone before the vent | Typically 0.5 to 2 percent water on throughput |
Preventing vent flooding
Vacuum port flooding — melt climbing into the vent throat and eventually into the vacuum line — is the most common devolatilization fault on recycled lines, and it has four causes worth checking in order: degree of fill too high under the port, melt viscosity too low because of an overheated or heavily degraded feed, throughput surging from inconsistent bulk density regrind, and a blocked or partially closed vent insert. A vent stuffer solves the symptom mechanically, but the durable fixes are a longer-pitch vent section, steadier gravimetric feeding, and a melt temperature 10 to 15 degrees Celsius lower than a virgin resin recipe would use.
Steam stripping as a low-cost odor tool
Injecting a controlled quantity of water into a filled melt zone upstream of the vacuum vent is one of the highest-value, lowest-cost odor interventions available. The water flashes to steam and acts as a stripping agent, lowering the partial pressure of the odor species and carrying them out through the vent. Typical injection is 0.5 to 2 percent on throughput; the equipment is a metering pump, an injection nozzle rated for melt pressure, and a condenser on the vacuum line. Compared with buying a specialty odor-absorbing additive at a High or Premium cost level, steam stripping is a one-time capital item with a Low running cost, and it is more effective on the low molecular weight aldehyde fraction that dominates polyolefin odor.
4. Feedstock Characterization Before Formulating
No recycled formula can be written responsibly without a characterization sheet for the incoming batch. Recycled feedstock is not a grade; it is a distribution. The purpose of incoming testing is to locate where the current bale sits inside that distribution so that the additive package can be adjusted by the smallest amount necessary rather than over-specified as insurance.
The test list below is deliberately short. Every item on it changes a formula decision. Tests that are interesting but do not change a decision belong in development work, not in routine incoming control.
| Test | Method reference | What it tells the formulator | Typical range for post-consumer polyolefin | Formula decision it drives |
|---|---|---|---|---|
| Melt flow rate | ISO 1133 / ASTM D1238 | Average molecular weight and degree of prior degradation | rPP 4 to 35 g/10min; rHDPE 0.3 to 8 g/10min | Whether a chain extender or a lower-MFR virgin blend is needed |
| Density | ISO 1183 | Polymer identity and filler content already present | 0.90 to 1.05 g/cm3 depending on mix | Filler dosing headroom and stiffness expectation |
| Ash content | ISO 3451 | Existing mineral filler, pigment and inorganic contamination | 0.5 to 12 percent | How much fresh filler can be added before impact collapses |
| Moisture | Karl Fischer or loss on drying | Water load entering the barrel | 0.1 to 1.5 percent | Pre-drying requirement and atmospheric vent sizing |
| Odor grade | VDA 270 six-grade scale | Severity of the volatile problem | Grade 3.5 to 6 untreated | Vacuum level, steam stripping, adsorbent dosage |
| Yellowness index | ASTM E313 | Extent of thermo-oxidative history and pigment carryover | YI 8 to 40 | Antioxidant level, whether natural color is achievable |
| Tensile and notched impact | ISO 527 / ISO 179 | Baseline mechanical capability of the regrind | Highly variable | Impact modifier level, or whether the target is achievable at all |
| Differential scanning calorimetry | ISO 11357 | Multiple melting peaks reveal cross-contamination | One to three peaks | Compatibilizer selection and dosage |
| Infrared spectroscopy | ATR-FTIR | Polymer identification and rough blend ratio | Qualitative to semi-quantitative | Whether the batch is a single polymer or a mixed polyolefin |
Reading the odor grade correctly
The VDA 270 six-grade odor scale is the reference most automotive and appliance customers use, and it is worth knowing how the grades translate into commercial outcomes. Grade 1 means not perceptible; grade 2 perceptible but not disturbing; grade 3 clearly perceptible but not disturbing; grade 4 disturbing; grade 5 strongly disturbing; grade 6 unacceptable. Most untreated post-consumer polyolefin regrind sits between 4 and 5.5. Interior automotive parts commonly require 3.0 or better; consumer appliance housings often accept 3.5; non-visible industrial parts may accept 4. Knowing the target grade before formulating decides whether a Low-cost adsorbent is sufficient or whether steam stripping hardware is required.
Interpreting differential scanning calorimetry on mixed streams
A single sharp melting peak near 163 to 168 degrees Celsius indicates a reasonably clean polypropylene stream. A second peak near 125 to 133 degrees Celsius indicates high-density polyethylene contamination; near 108 to 115 degrees Celsius indicates low-density or linear low-density polyethylene. The relative enthalpy under each peak gives a workable estimate of the blend ratio, which is precisely the number that sets compatibilizer dosage. Running this one test on every incoming bale of mixed material is the difference between a compatibilizer level that is correct and one that is guessed.
5. Recycled PP Formula Family
Recycled polypropylene is the workhorse of low-cost compounding, and it responds well to a tiered formula strategy: an economy tier for non-critical parts, a standard tier for general technical parts, and a high-performance tier where notched impact and surface quality both matter. The tiers differ mainly in impact modifier and compatibilizer content, because those are the two components with the strongest effect on both properties and cost.
All three recipes below assume the regrind has passed through a two-stage devolatilization barrel. Without that, every antioxidant figure would need to rise and the odor grade column would be unachievable.
| Component | Economy tier (parts) | Standard tier (parts) | High-performance tier (parts) | Function |
|---|---|---|---|---|
| rPP base regrind, washed and dried | 100 | 100 | 100 | Matrix |
| Talc, 2000 to 5000 mesh | 10 to 20 | 15 to 20 | 18 to 22 | Stiffness, dimensional stability, nucleation |
| CaCO3, 1250 mesh, surface activated | 0 to 12 | 0 to 8 | 0 | Cost dilution, lower reinforcement than talc |
| POE elastomer, MFR 0.5 to 5 g/10min | 0 to 3 | 6 to 10 | 12 to 18 | Impact modification, low-temperature toughness |
| PP-g-MAH compatibilizer, grafting rate 0.8 to 1.2 percent | 0 to 1 | 1.5 to 2.5 | 3 to 4 | Filler and elastomer interfacial coupling |
| Hindered phenol primary antioxidant | 0.10 to 0.15 | 0.15 to 0.20 | 0.20 to 0.25 | Radical scavenging during processing and service |
| Phosphite secondary antioxidant | 0.10 to 0.15 | 0.15 to 0.20 | 0.20 to 0.30 | Hydroperoxide decomposition, color protection |
| HALS light stabilizer | 0 | 0 to 0.2 | 0.3 to 0.5 | Only where outdoor exposure is specified |
| Odor adsorbent, zeolite or porous mineral carrier | 0 to 0.3 | 0.3 to 0.6 | 0.5 to 1.0 | Residual odor capture after devolatilization |
| Lubricant, metal stearate or amide wax | 0.15 to 0.25 | 0.20 to 0.30 | 0.25 to 0.40 | Filler dispersion, torque reduction, surface finish |
| Nucleating agent | 0 | 0 to 0.1 | 0.1 to 0.2 | Cycle time and stiffness improvement |
Expected property windows for the three rPP tiers
| Property | Economy tier | Standard tier | High-performance tier | Test reference |
|---|---|---|---|---|
| Melt flow rate, 230 degrees Celsius / 2.16 kg | 12 to 30 g/10min | 8 to 20 g/10min | 6 to 14 g/10min | ISO 1133 |
| Notched Charpy impact, 23 degrees Celsius | 2.5 to 5 kJ/m2 | 7 to 15 kJ/m2 | 20 to 45 kJ/m2 | ISO 179-1eA |
| Notched Charpy impact, minus 20 degrees Celsius | 1.5 to 2.5 kJ/m2 | 3 to 6 kJ/m2 | 7 to 14 kJ/m2 | ISO 179-1eA |
| Flexural modulus | 1700 to 2300 MPa | 1600 to 2100 MPa | 1300 to 1800 MPa | ISO 178 |
| Tensile strength at yield | 20 to 26 MPa | 19 to 24 MPa | 17 to 22 MPa | ISO 527 |
| Odor grade after two-stage devolatilization | 3.5 to 4.0 | 3.0 to 3.5 | 2.5 to 3.0 | VDA 270 |
| Material cost index (baseline = 100) | 100 | 110 | 126 | Relative |
| Cost level | Low | Medium | High | Relative |
Why compatibilizer dosage is not proportional to filler
A common error is to scale PP-g-MAH linearly with filler content. Maleic anhydride grafted polypropylene works at the interface, so its required dosage scales with interfacial area, which scales with filler surface area, not filler mass. Moving from 1250 mesh calcium carbonate to 5000 mesh talc at the same loading multiplies the interfacial area substantially and demands more compatibilizer. Conversely, using pre-activated calcium carbonate whose surface has already been treated reduces the coupling agent requirement. Getting this right is worth several index points on a large-volume grade.
6. Recycled PE Formula Family
Recycled high-density polyethylene formulation is dominated by one question that does not apply to polypropylene: has the molecular weight been reduced by prior processing, and can it be rebuilt? Polyethylene tends to cross-link as well as chain-scission under thermo-oxidative stress, so recycled polyethylene often shows both a lower melt flow rate in some fractions and gels in others. Chain extenders and careful shear management are the two levers that matter most.
The three application families below — blow molding, pipe and injection molding — have genuinely different requirements, and a single “rHDPE compound” grade serves none of them well.
| Component | Blow molding grade (parts) | Pipe and conduit grade (parts) | Injection grade (parts) | Function |
|---|---|---|---|---|
| rHDPE base regrind | 100 | 100 | 100 | Matrix |
| Virgin HDPE, high molecular weight | 0 to 15 | 15 to 30 | 0 to 10 | Melt strength and long-term property recovery |
| Chain extender, epoxy-functional styrene-acrylic oligomer | 0.2 to 0.5 | 0.3 to 0.6 | 0 to 0.2 | Molecular weight and melt strength rebuild |
| CaCO3, 1250 mesh, activated | 0 to 10 | 0 | 10 to 25 | Cost dilution and stiffness in non-pressure parts |
| POE or metallocene plastomer | 0 to 4 | 3 to 6 | 0 to 5 | Impact and environmental stress crack resistance |
| PE-g-MAH compatibilizer | 0 to 1 | 0.5 to 1.5 | 1 to 2 | Filler coupling and blend compatibility |
| Hindered phenol primary antioxidant | 0.15 to 0.20 | 0.20 to 0.30 | 0.12 to 0.18 | Melt and service stabilization |
| Phosphite secondary antioxidant | 0.10 to 0.20 | 0.15 to 0.25 | 0.10 to 0.15 | Color and hydroperoxide control |
| Carbon black masterbatch, 40 percent concentration | 0 to 5 | 5 to 6 | 0 to 4 | Ultraviolet protection for buried or exposed parts |
| Processing aid, fluoropolymer-free polymer type | 0.05 to 0.15 | 0.05 to 0.15 | 0 to 0.1 | Melt fracture suppression and die build-up control |
| Odor adsorbent, porous mineral carrier | 0.3 to 0.6 | 0 to 0.3 | 0.3 to 0.8 | Residual odor capture |
Expected property windows for the three rHDPE grades
| Property | Blow molding grade | Pipe and conduit grade | Injection grade | Test reference |
|---|---|---|---|---|
| Melt flow rate, 190 degrees Celsius / 2.16 kg | 0.25 to 0.7 g/10min | 0.15 to 0.5 g/10min | 2 to 8 g/10min | ISO 1133 |
| Melt flow rate, 190 degrees Celsius / 5 kg | 0.9 to 2.2 g/10min | 0.5 to 1.6 g/10min | 7 to 25 g/10min | ISO 1133 |
| Density | 0.950 to 0.958 g/cm3 | 0.948 to 0.956 g/cm3 | 0.955 to 1.05 g/cm3 (filled) | ISO 1183 |
| Notched Izod impact, 23 degrees Celsius | 10 to 20 kJ/m2 | 18 to 35 kJ/m2 | 4 to 9 kJ/m2 | ISO 180 |
| Environmental stress crack resistance, F50 | 60 to 250 hours | 250 to 900 hours | 30 to 120 hours | ASTM D1693 condition B |
| Flexural modulus | 950 to 1200 MPa | 900 to 1150 MPa | 1200 to 1900 MPa | ISO 178 |
| Odor grade after two-stage devolatilization | 3.0 to 3.5 | 3.5 to 4.0 | 3.0 to 3.5 | VDA 270 |
| Material cost index (baseline = 100) | 112 | 124 | 98 | Relative |
| Cost level | Medium | High | Low | Relative |
How chain extenders rebuild melt strength
An epoxy-functional styrene-acrylic oligomer chain extender carries multiple reactive epoxy groups per molecule. Those groups react with the carboxyl and hydroxyl end groups generated by prior chain scission, linking shorter chains back into longer ones and introducing a controlled degree of long-chain branching. The practical result is a rise in melt strength and a drop in melt flow rate, both of which are exactly what a blow molding or pipe grade needs. Dosage discipline is essential: too little produces no measurable change, while too much produces gels, surface defects and a compound that will not flow into thin sections.
| Chain extender dosage (parts) | Effect on melt flow rate | Effect on melt strength | Gel risk | Recommended for |
|---|---|---|---|---|
| 0.1 | Barely measurable | Slight increase | None | Fine trimming of an almost-correct batch |
| 0.2 to 0.3 | Drops 20 to 35 percent | Clear improvement | Low | Injection and general purpose grades |
| 0.4 to 0.6 | Drops 40 to 60 percent | Strong improvement, parison sag controlled | Medium | Blow molding and pipe grades |
| 0.8 and above | Drops beyond 65 percent | Diminishing return | High | Not recommended for general compounding |
Chain extender reaction requires melt residence time and good distributive mixing, but not high shear. On a twin-screw extruder the correct placement is a downstream side or liquid feed port into a well-mixed but moderately sheared zone, followed by 8 to 12 L:D of distributive mixing before the vacuum vent. Feeding chain extender at the main hopper wastes a substantial part of it on premature reaction in the melting zone.
7. Recycled PET Formula and Intrinsic Viscosity Recovery
Recycled polyester compounding is governed by a single unforgiving rule: water plus heat equals irreversible hydrolysis. Every part of the rPET process — crystallizing, drying, high vacuum devolatilization, chain extension — exists to keep intrinsic viscosity from falling and then to rebuild what has already been lost. Get the drying wrong and no additive package will save the batch.
Crystallizing and drying, the non-negotiable first step
Amorphous recycled polyester flake softens and agglomerates if heated directly to drying temperature, so it must be crystallized first at 130 to 150 degrees Celsius under agitation, then dried at 160 to 170 degrees Celsius for 4 to 6 hours with a dehumidified air dew point of minus 40 degrees Celsius or better. The target residual moisture entering the barrel is below 50 parts per million; above 100 parts per million, intrinsic viscosity loss during a single extrusion pass can exceed 0.05 dL/g regardless of vacuum settings.
| Component | Fiber grade (parts) | Sheet and strapping grade (parts) | Engineering compound grade (parts) | Function |
|---|---|---|---|---|
| rPET flake, crystallized and dried | 100 | 100 | 100 | Matrix |
| Chain extender, epoxy-functional styrene-acrylic oligomer | 0.3 to 0.5 | 0.5 to 0.8 | 0.4 to 0.7 | Intrinsic viscosity and melt strength recovery |
| Hydrolysis stabilizer, carbodiimide type | 0.2 to 0.4 | 0.3 to 0.5 | 0.3 to 0.6 | End-group capping, long-term hydrolytic resistance |
| Nucleating agent, ionomer or mineral type | 0 to 0.3 | 0.2 to 0.5 | 0.5 to 1.0 | Crystallization rate and cycle time |
| Hindered phenol primary antioxidant | 0.10 to 0.15 | 0.10 to 0.20 | 0.15 to 0.25 | Thermal stabilization at high melt temperature |
| Phosphite secondary antioxidant | 0.05 to 0.10 | 0.10 to 0.15 | 0.10 to 0.20 | Color protection |
| Impact modifier, reactive acrylic core-shell or elastomeric ethylene copolymer | 0 | 0 to 3 | 5 to 10 | Notched impact for technical parts |
| Glass fiber, chopped, silane sized | 0 | 0 | 15 to 30 | Stiffness and heat deflection temperature |
| Lubricant, high-temperature stable type | 0.1 to 0.2 | 0.1 to 0.3 | 0.2 to 0.4 | Torque and surface finish |
Intrinsic viscosity and its application map
Intrinsic viscosity is the single number that decides where a recycled polyester compound can be sold. The relationship is direct and worth memorizing.
| Intrinsic viscosity (dL/g) | Typical origin | Suitable applications | Processing note | Cost level |
|---|---|---|---|---|
| 0.50 to 0.58 | Heavily degraded post-consumer flake, multiple heat histories | Staple fiber, non-woven, low-grade filler applications | Runs easily but has no melt strength | Low |
| 0.60 to 0.68 | Standard washed bottle flake after one extrusion pass | Filament fiber, thin sheet, thermoformed trays | Requires nucleation for fast crystallization | Low to Medium |
| 0.70 to 0.78 | Chain-extended and high-vacuum devolatilized flake | Thick sheet, strapping, engineering compounds | Chain extender dosage control is critical | Medium |
| 0.80 and above | Solid-state post-condensed material | Bottle grade, high-strength strapping | Requires solid-state polycondensation, not just extrusion | High to Very High |
A twin screw devolatilization extruder can reliably lift intrinsic viscosity from around 0.58 dL/g to 0.70 to 0.78 dL/g using chain extension combined with deep vacuum. It cannot reach bottle grade on its own — that step needs solid-state polycondensation. Being clear about this boundary with customers prevents the most damaging kind of specification failure, which is agreeing to a target the process cannot physically reach.
Why high vacuum matters even more for polyester
Polyester devolatilization does double duty. It strips acetaldehyde and cyclic trimer, which are the odor and taste offenders, and it shifts the hydrolysis equilibrium. Removing water vapor from the melt drives the ester hydrolysis reaction backwards, slowing further chain cleavage during the residence time in the barrel. On a recycled polyester line, a vacuum level of minus 0.090 to minus 0.098 MPa with a two-stage pump is not a luxury — it directly determines how much intrinsic viscosity survives the pass, and therefore which market the pellets can serve.
8. Mixed Polyolefin Low-Cost Formula
Mixed polypropylene and polyethylene streams are the cheapest feedstock available and the hardest to formulate, because the two polymers are thermodynamically immiscible. Without a compatibilizer the blend forms a coarse two-phase morphology with weak interfaces, and notched impact collapses to values that no technical application will accept. With the right compatibilizer at the right dosage, the same blend becomes a serviceable general-purpose compound at a Low cost level.
How blend ratio changes properties
The property curve across the polypropylene to polyethylene composition range is not linear, and it is not symmetric. Small amounts of the minority phase act as a dispersed impact modifier; intermediate ratios produce co-continuous morphology with the worst mechanical performance; the minimum sits broadly around a 50/50 to 60/40 composition.
| PP / PE ratio | Morphology | Notched Charpy impact, uncompatibilized | Notched Charpy impact, with 3 parts compatibilizer | Flexural modulus | Practical verdict |
|---|---|---|---|---|---|
| 100 / 0 | Single phase | 3 to 5 kJ/m2 | Not applicable | 1400 to 1600 MPa | Reference point |
| 90 / 10 | PE droplets in PP matrix | 4 to 7 kJ/m2 | 8 to 13 kJ/m2 | 1300 to 1500 MPa | Best value ratio, mild toughening effect |
| 70 / 30 | Coarse dispersed phase | 3 to 5 kJ/m2 | 9 to 16 kJ/m2 | 1150 to 1350 MPa | Workable with compatibilizer, poor without |
| 50 / 50 | Co-continuous, weak interfaces | 2.5 to 4 kJ/m2 | 7 to 12 kJ/m2 | 1000 to 1200 MPa | Worst case, needs the highest compatibilizer dosage |
| 30 / 70 | PP droplets in PE matrix | 4 to 8 kJ/m2 | 12 to 22 kJ/m2 | 900 to 1100 MPa | Surprisingly good, PE matrix is forgiving |
| 0 / 100 | Single phase | 12 to 25 kJ/m2 | Not applicable | 850 to 1100 MPa | Reference point |
Compatibilizer selection logic
| Compatibilizer type | Mechanism | Typical dosage (parts) | Best blend ratio range | Cost level |
|---|---|---|---|---|
| Ethylene-propylene rubber, amorphous | Interfacial emulsification by segmental affinity to both phases | 4 to 10 | Any ratio, especially 50/50 | Medium |
| POE elastomer, MFR 0.5 to 5 g/10min | Interfacial modification plus independent toughening | 4 to 8 | PP-rich blends | Medium to High |
| Styrenic block copolymer, hydrogenated | Strong interfacial anchoring of both phases | 3 to 6 | Any ratio, best surface quality | High |
| PP-g-MAH, grafting rate 0.8 to 1.2 percent | Reactive coupling, mainly effective with fillers present | 1 to 3 | Filled mixed polyolefin | Medium |
| Combined POE plus PP-g-MAH | Toughening plus interfacial coupling in one package | 5 plus 1.5 | Filled 70/30 to 50/50 blends | Medium |
A working low-cost mixed polyolefin recipe
| Component | Parts | Notes |
|---|---|---|
| Mixed polyolefin regrind, PP/PE around 70/30 | 100 | Verify ratio by differential scanning calorimetry on every bale |
| CaCO3, 1250 mesh, surface activated | 15 to 25 | Side fed downstream of first melting section |
| POE elastomer, MFR 0.5 to 5 g/10min | 5 to 7 | Primary compatibilizer and toughener |
| PP-g-MAH compatibilizer, grafting rate 0.8 to 1.2 percent | 1.5 to 2.5 | Couples filler to the polyolefin matrix |
| Hindered phenol primary antioxidant | 0.15 | Mandatory on any mixed stream |
| Phosphite secondary antioxidant | 0.15 | Controls yellowing from mixed heat histories |
| Odor adsorbent, porous mineral carrier | 0.4 to 0.8 | Mixed streams carry the widest odor spectrum |
| Lubricant, amide wax | 0.25 | Improves filler dispersion and surface gloss |
| Carbon black masterbatch, 40 percent concentration | 2 to 4 | Black color hides the color variability of mixed feed |
Expected performance for this recipe: melt flow rate 3 to 12 g/10min at 230 degrees Celsius and 2.16 kg, notched Charpy impact 8 to 15 kJ/m2 at 23 degrees Celsius, flexural modulus 1200 to 1500 MPa, odor grade 3.5 to 4.0 after two-stage devolatilization, and a material cost index of approximately 92 against the economy rPP baseline. That combination is well suited to crates, pallets, drainage components, cable drums, garden furniture frames and industrial packaging.
9. Additive Cost-Effectiveness Ranking
The most useful tool a recycled compounder can own is a ranked list of additives by performance gained per unit of cost spent. The list below is ordered by cost-effectiveness, not by importance, and it produces a clear dosing sequence: add the top items first, and only descend the list when a specification demands it.
| Rank | Additive | Function | Typical dosage (phr) | Performance gain | Cost level | Cost-effectiveness |
|---|---|---|---|---|---|---|
| 1 | Phosphite secondary antioxidant | Decomposes hydroperoxides, protects color and melt flow rate stability | 0.10 to 0.25 | Melt flow rate drift cut by half or more across passes; yellowness index improved several points | Low | Excellent |
| 2 | Hindered phenol primary antioxidant | Radical scavenging during processing and in service | 0.10 to 0.25 | Prevents progressive chain scission and long-term embrittlement | Low | Excellent |
| 3 | Lubricant, metal stearate or amide wax | Filler wetting, torque reduction, surface finish | 0.15 to 0.40 | Torque reduced 5 to 12 percent, better dispersion, higher output | Low | Excellent |
| 4 | Talc, 2000 to 5000 mesh | Stiffness, dimensional stability, nucleation | 10 to 25 | Flexural modulus up 30 to 60 percent, heat deflection temperature up | Low | Very good |
| 5 | CaCO3, 1250 mesh, activated | Cost dilution with modest stiffness gain | 10 to 25 | Material index reduced; impact reduced less than with untreated grades | Low | Very good |
| 6 | PP-g-MAH compatibilizer, grafting rate 0.8 to 1.2 percent | Interfacial coupling between filler, elastomer and matrix | 1 to 4 | Impact and weld line strength up 30 to 80 percent in filled systems | Medium | Very good |
| 7 | Nucleating agent | Faster crystallization, higher stiffness, shorter cycle | 0.1 to 0.3 | Cycle time down 5 to 15 percent in injection applications | Medium | Good |
| 8 | Chain extender, epoxy-functional styrene-acrylic oligomer | Molecular weight and melt strength rebuild | 0.2 to 0.8 | Intrinsic viscosity or melt strength restored to usable levels | High | Good where required, wasteful elsewhere |
| 9 | POE elastomer, MFR 0.5 to 5 g/10min | Impact modification | 5 to 18 | Notched impact multiplied several times | Medium to High | Fair — high loading makes it costly in absolute terms |
| 10 | Odor adsorbent, zeolite or porous carrier | Residual odor capture | 0.3 to 1.0 | Around half a VDA 270 grade when used after devolatilization | Medium | Fair — cheap only if the vacuum system has done its job first |
| 11 | HALS light stabilizer | Ultraviolet and long-term thermal protection | 0.2 to 0.6 | Outdoor service life extended substantially | High | Fair — specify only where exposure is real |
| 12 | Hydrolysis stabilizer, carbodiimide type | End-group capping in polyester systems | 0.2 to 0.6 | Hydrolytic aging resistance greatly improved | High | Necessary for polyester, irrelevant for polyolefin |
| 13 | Reactive acrylic core-shell impact modifier | High-efficiency toughening in polar polymers | 4 to 10 | Large impact gain in polyester compounds | Premium | Poor for low-cost work, reserve for technical grades |
| 14 | Specialty odor-masking fragrance | Covers rather than removes odor | 0.1 to 0.5 | Perceived odor improved, measured VOC unchanged | High | Poor — customers detect the substitution |
The recommended dosing sequence
Build the formula in this order and stop as soon as the specification is met. First, the antioxidant pair and lubricant — these three are always present, always cheap, and always pay for themselves. Second, filler to the level that stiffness and cost require. Third, compatibilizer sized to filler surface area. Fourth, impact modifier, added only in the increments needed to clear the notched impact target. Fifth, functional specialties such as chain extender, nucleating agent, light stabilizer or hydrolysis stabilizer, each justified by a named requirement in the customer specification. Anything that cannot be traced to a specification line should not be in the recipe.
10. Odor and VOC Reduction Without Expensive Additives
Odor is the number one commercial obstacle for recycled compounds, and it is best attacked with process settings before chemistry. Four process levers — deeper vacuum, more vented barrel length, lower melt temperature, and steam stripping — together deliver more odor improvement than any affordable additive package, and their running cost is electricity rather than consumables.
Lever one: raise the vacuum level
Moving from minus 0.06 MPa to minus 0.09 MPa is often the single largest available improvement, and on an existing machine it may cost nothing more than servicing the vacuum pump, replacing worn barrel seals and cooling the sealing water properly. Warm sealing water is the most commonly overlooked cause of poor vacuum on water ring pumps; every few degrees of sealing water temperature reduction translates directly into achievable vacuum depth.
Lever two: add vented barrel length
Mass transfer of volatiles out of a polymer melt is time-dependent. Extending the vented section from 3 L:D to 5 L:D increases exposure time under vacuum by roughly two-thirds at the same screw speed, and a second vacuum port in series is more effective than one port at a slightly deeper vacuum. This is a design decision at machine specification time, which is why odor targets should be discussed before an extruder is configured rather than after commissioning.
Lever three: lower the melt temperature
Every 10 degrees Celsius of melt temperature reduction meaningfully slows thermo-oxidative degradation, which means fewer new aldehydes and ketones are created inside the barrel. On recycled polyolefin, running 10 to 15 degrees Celsius below the equivalent virgin recipe is usually possible if the screw is configured for gentle plastication — moderate kneading block angles, fewer reverse elements, and adequate barrel length rather than aggressive shear in a short machine. Lower melt temperature also reduces specific energy consumption, so it improves two cost drivers at once.
Lever four: steam stripping
Metered water injection into a filled melt zone, described earlier, is the strongest process tool available for stubborn odor from ink, adhesive and fragrance residue. It requires a condenser and a water separation arrangement on the vacuum line, and it slightly increases energy consumption, but the additive-free odor reduction it delivers is difficult to match by any other means at a comparable cost level.
| Intervention | Typical VDA 270 improvement | Capital cost level | Running cost level | Applies to |
|---|---|---|---|---|
| Vacuum pump service and seal renewal | 0.3 to 0.7 grade | Low | Low | Any existing line |
| Upgrade to two-stage vacuum system | 0.5 to 1.0 grade | Medium | Low | Lines limited to minus 0.07 MPa or worse |
| Second vacuum port in series | 0.4 to 0.8 grade | Medium | Low | Machines with spare barrel length |
| Extend vented section from 3 to 5 L:D | 0.3 to 0.6 grade | Medium | None | New machine specification |
| Reduce melt temperature 10 to 15 degrees Celsius | 0.3 to 0.6 grade | None | Negative — saves energy | Any line with screw design headroom |
| Steam stripping with water injection | 0.5 to 1.0 grade | Medium | Low | Post-consumer packaging streams |
| Odor adsorbent at 0.5 parts | 0.3 to 0.5 grade | None | Medium | Final gap closing only |
| Fragrance masking | Perceived only | None | High | Not recommended |
The practical route to a grade 3.0 compound from a grade 5.0 feedstock is therefore cumulative: a two-stage vacuum system, a properly sized vented section, a disciplined melt temperature, steam stripping where the feedstock warrants it, and a modest adsorbent dosage at the end. Trying to close a two-grade gap with additives alone requires loadings at a High to Premium cost level and still tends to fail on the aldehyde fraction.
11. Screw Configuration for Recycled Compounding
Screw configuration for recycled material follows one governing principle: plasticize gently, mix thoroughly, vent generously. Recycled polymer has already absorbed one or more full heat histories, so the shear intensity that works perfectly for virgin resin actively destroys it. Kerke designs screw assemblies with computer-aided layout and a self-wiping kneading geometry precisely so that dispersion can be achieved with lower peak shear.
| Zone | Position (L:D) | Element type | Function | Design note for recycled feed |
|---|---|---|---|---|
| Feed and conveying | 0 to 6 | Long-pitch conveying elements | Intake of low bulk density regrind | Use extra-long pitch; flake bulk density can be a third of pellet bulk density |
| First melting zone | 6 to 12 | Forward kneading blocks at 45 degrees plus one 90 degree block | Controlled melting without excessive shear peak | Avoid reverse elements here; use narrow discs rather than wide ones |
| First mixing zone | 12 to 16 | Combination of 45 degree kneading and toothed mixing elements | Distributive homogenization of additives | Distributive rather than dispersive at this stage |
| Atmospheric vent | 16 to 20 | Long-pitch shallow conveying with upstream seal | Steam and light volatile release | Keep degree of fill low; heat the port jacket to avoid condensate |
| Side feeding zone | 20 to 24 | Conveying elements matched to side feeder speed | Filler, glass fiber or chain extender introduction | Never side feed into a filled zone; keep the receiving section starved |
| Second mixing zone | 24 to 32 | Kneading blocks at 45 degrees plus toothed and gear-type mixers | Filler dispersion and elastomer phase refinement | This is where dispersion happens; use narrow discs and moderate block length |
| Vacuum vent | 32 to 38 | Upstream melt seal, long-pitch vent conveying, optional stuffer | Deep devolatilization | 3 to 5 L:D of open conveying; fill below 30 percent |
| Pressure build-up | 38 to 44 | Progressively shorter pitch conveying | Melt pressure for filter and die | Step pitch down gradually to limit local shear heating |
Kneading block angle selection
| Element | Shear intensity | Mixing character | Residence time effect | Use on recycled feed |
|---|---|---|---|---|
| 30 degree forward kneading block | Low | Mainly distributive | Slight increase | Freely — safe for heat-sensitive recycled material |
| 45 degree forward kneading block | Medium | Balanced distributive and dispersive | Moderate increase | The workhorse element; use as the backbone of both mixing zones |
| 90 degree neutral kneading block | High | Strongly dispersive | Large increase | One or two only, in the first melting zone |
| Reverse kneading block | Very high | Dispersive plus melt sealing | Very large increase | Only as a short melt seal before a vent; never as a mixing strategy |
| Toothed mixing element | Low | Distributive with high surface renewal | Slight increase | Excellent for recycled work — mixing without degradation |
| Reverse conveying element | Medium to high | Sealing and residence time control | Large increase | Short sections only, before vents and side feeders |
12. Process Window Tables by Material
Process windows for recycled material are narrower than for virgin resin and sit at lower temperatures. The tables below give starting points for a 44 to 48 L:D twin-screw extruder with one atmospheric and one vacuum vent. They are starting points, not final settings; every recycled feedstock requires confirmation on a trial run.
Recycled polypropylene compound
| Parameter | Setting | Parameter | Setting |
|---|---|---|---|
| Barrel zone 1 (feed) | Water cooled, 40 to 60 degrees Celsius | Barrel zone 6 | 195 to 205 degrees Celsius |
| Barrel zone 2 | 150 to 165 degrees Celsius | Barrel zone 7 (vacuum vent) | 190 to 200 degrees Celsius |
| Barrel zone 3 | 175 to 190 degrees Celsius | Barrel zone 8 | 190 to 200 degrees Celsius |
| Barrel zone 4 | 190 to 200 degrees Celsius | Die head | 195 to 210 degrees Celsius |
| Barrel zone 5 (atmospheric vent) | 195 to 205 degrees Celsius | Actual melt temperature | 200 to 218 degrees Celsius |
| Screw speed | 350 to 500 rpm | Torque utilization | 55 to 75 percent |
| Vacuum level | Minus 0.080 to minus 0.092 MPa | Melt pressure at screen | 3 to 7 MPa |
| Specific energy consumption | 0.16 to 0.24 kWh/kg | Pelletizing | Water strand or water ring die face |
Recycled high-density polyethylene compound
| Parameter | Setting | Parameter | Setting |
|---|---|---|---|
| Barrel zone 1 (feed) | Water cooled, 40 to 60 degrees Celsius | Barrel zone 6 | 190 to 200 degrees Celsius |
| Barrel zone 2 | 145 to 160 degrees Celsius | Barrel zone 7 (vacuum vent) | 185 to 195 degrees Celsius |
| Barrel zone 3 | 170 to 185 degrees Celsius | Barrel zone 8 | 185 to 195 degrees Celsius |
| Barrel zone 4 | 185 to 195 degrees Celsius | Die head | 190 to 205 degrees Celsius |
| Barrel zone 5 (atmospheric vent) | 190 to 200 degrees Celsius | Actual melt temperature | 195 to 215 degrees Celsius |
| Screw speed | 300 to 450 rpm | Torque utilization | 60 to 80 percent |
| Vacuum level | Minus 0.080 to minus 0.090 MPa | Melt pressure at screen | 4 to 9 MPa |
| Specific energy consumption | 0.18 to 0.26 kWh/kg | Pelletizing | Water strand or underwater |
Recycled polyester compound
| Parameter | Setting | Parameter | Setting |
|---|---|---|---|
| Pre-crystallizing | 130 to 150 degrees Celsius with agitation | Drying | 160 to 170 degrees Celsius, 4 to 6 hours, dew point minus 40 degrees Celsius |
| Barrel zone 1 (feed) | Water cooled, 50 to 70 degrees Celsius | Barrel zone 6 | 265 to 275 degrees Celsius |
| Barrel zone 2 | 230 to 250 degrees Celsius | Barrel zone 7 (vacuum vent) | 260 to 272 degrees Celsius |
| Barrel zone 3 | 260 to 275 degrees Celsius | Barrel zone 8 | 260 to 272 degrees Celsius |
| Barrel zone 4 | 265 to 278 degrees Celsius | Die head | 265 to 280 degrees Celsius |
| Barrel zone 5 (atmospheric vent) | 265 to 278 degrees Celsius | Actual melt temperature | 272 to 292 degrees Celsius |
| Screw speed | 200 to 350 rpm | Torque utilization | 50 to 70 percent |
| Vacuum level | Minus 0.090 to minus 0.098 MPa | Melt pressure at screen | 3 to 6 MPa |
| Specific energy consumption | 0.20 to 0.30 kWh/kg | Pelletizing | Water strand with rapid quench, or underwater |
Mixed polyolefin compound
| Parameter | Setting | Parameter | Setting |
|---|---|---|---|
| Barrel zones 2 to 4 | 150 to 195 degrees Celsius, rising | Barrel zones 5 to 8 | 185 to 200 degrees Celsius |
| Die head | 190 to 205 degrees Celsius | Actual melt temperature | 198 to 216 degrees Celsius |
| Screw speed | 320 to 450 rpm | Torque utilization | 60 to 80 percent |
| Vacuum level | Minus 0.085 to minus 0.095 MPa | Melt pressure at screen | 4 to 8 MPa |
| Specific energy consumption | 0.18 to 0.27 kWh/kg | Filtration | Continuous or double-piston screen changer recommended |
13. Kerke KTE Series Twin Screw Extruder
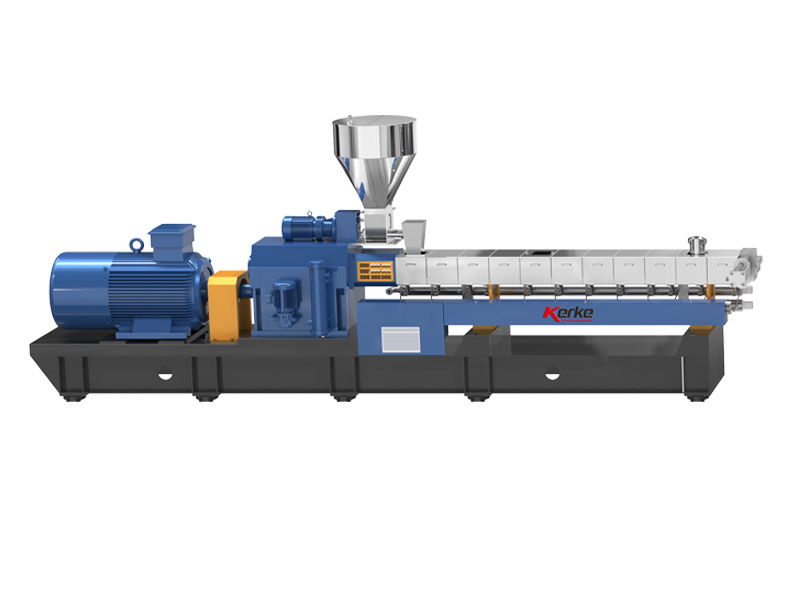
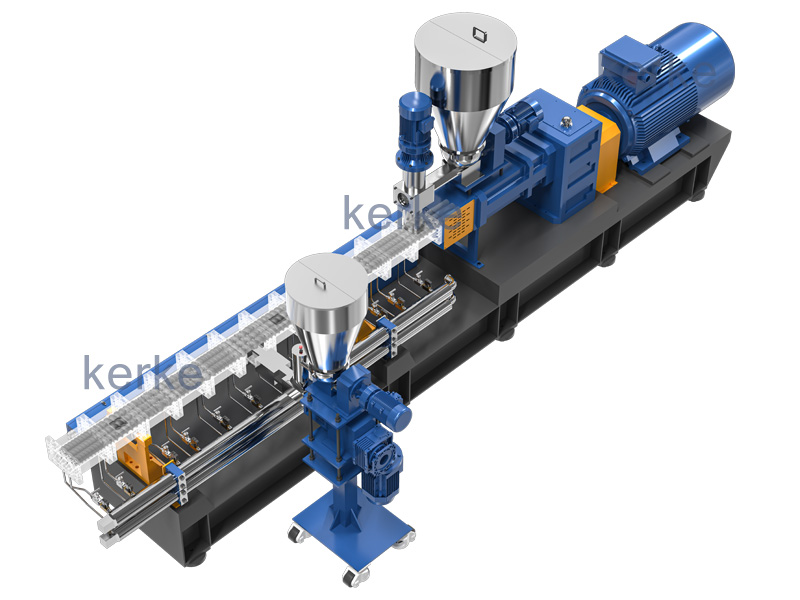
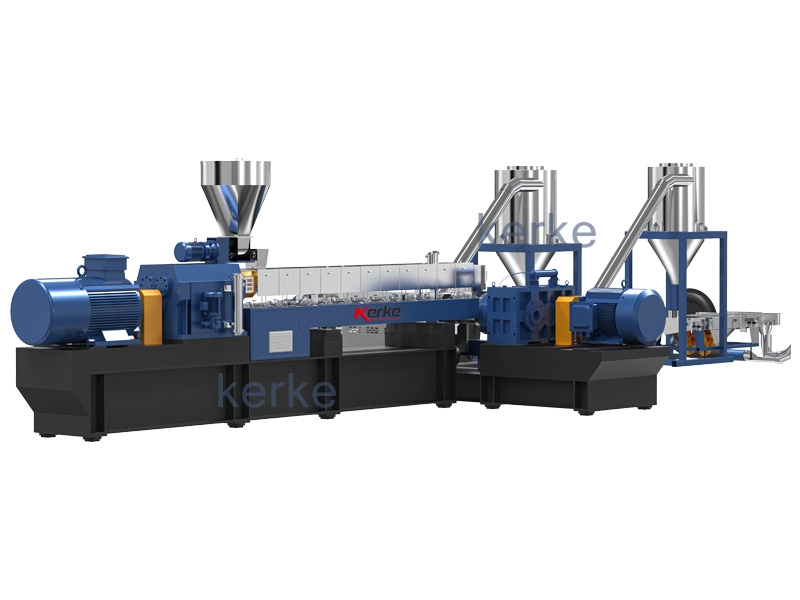
The KTE series is Kerke’s parallel co-rotating twin-screw compounding platform, spanning from the KTE-16B laboratory machine used for formula trials to the KTE-135D production machine. For recycled compounding the series is specified with a longer barrel than a standard masterbatch configuration, at least one atmospheric and one vacuum vent, and a screw assembly designed around gentle plastication rather than maximum shear.
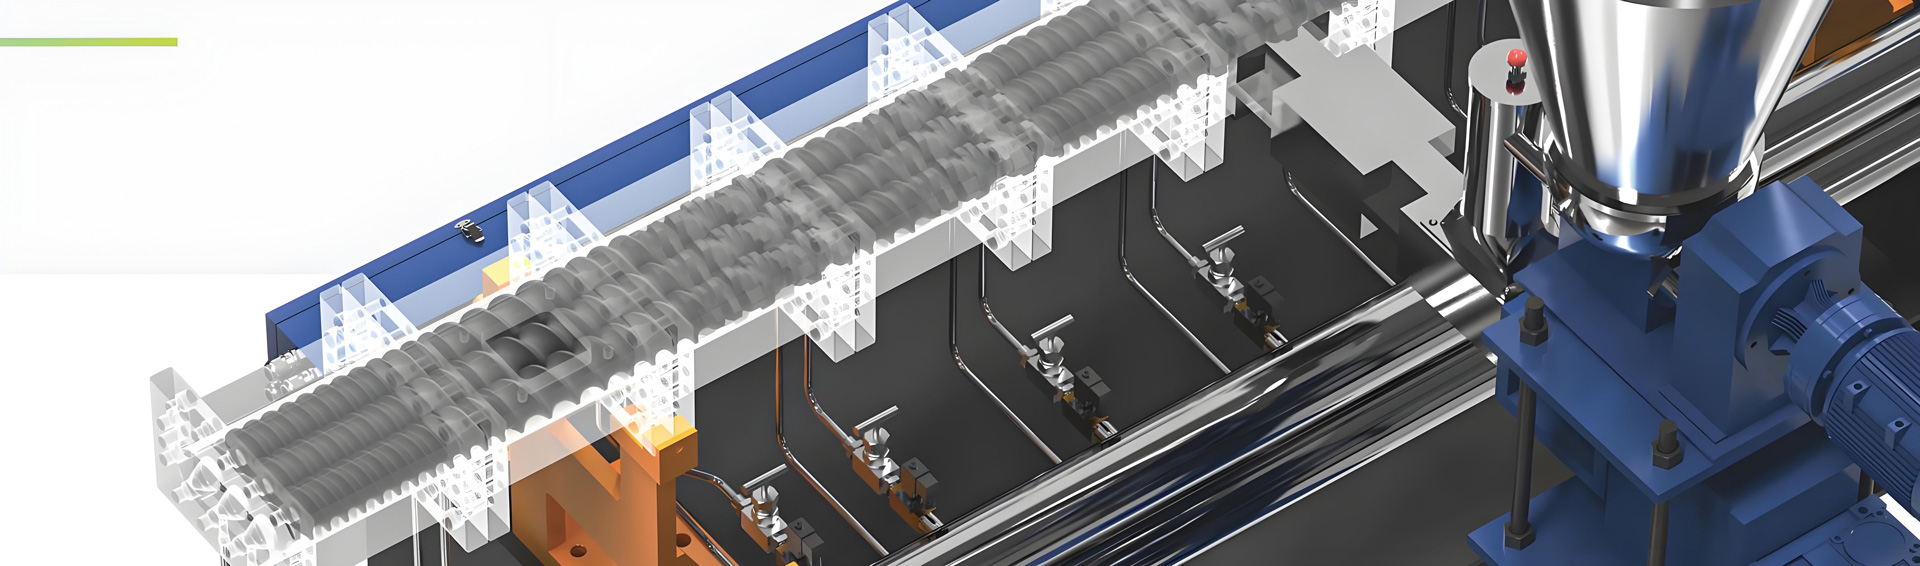
Every KTE machine is built around a modular barrel and a computer-aided designed segmented screw assembly. The kneading elements use a self-wiping co-type geometry, which matters enormously in recycled work: self-wiping surfaces leave no stagnant melt to carbonize into black specks, and segment interchangeability means a screw configured for recycled polypropylene can be reconfigured for recycled polyester by changing elements rather than buying a new shaft. The functions the assembly must deliver — material transport, plastication, shearing, dispersion, homogenization, exhaust and pressure building — are allocated deliberately across the barrel rather than left to chance.
KTE series specifications for recycled compounding
| Model | Screw diameter (mm) | Typical L:D ratio | Max screw speed (rpm) | Main motor power (kW) | Specific torque class | Output for recycled compounding (kg/h) | Vent ports |
|---|---|---|---|---|---|---|---|
| KTE-16B | 16 | 40 to 48 | 600 | 3 to 4 | Standard | 1 to 10 | 1 to 2 |
| KTE-20B | 21.7 | 40 to 48 | 600 | 4 to 7.5 | Standard | 5 to 25 | 1 to 2 |
| KTE-26B | 26 | 40 to 52 | 600 | 11 to 15 | Standard to high | 20 to 60 | 2 |
| KTE-36B | 35.6 | 40 to 52 | 600 | 22 to 37 | High | 50 to 150 | 2 |
| KTE-52B | 51.4 | 44 to 56 | 600 | 55 to 90 | High | 150 to 400 | 2 to 3 |
| KTE-65B | 62.4 | 44 to 56 | 600 | 90 to 160 | High | 300 to 700 | 2 to 3 |
| KTE-75D | 71 | 44 to 56 | 600 | 160 to 250 | High torque | 500 to 1100 | 2 to 3 |
| KTE-95D | 93 | 44 to 56 | 500 to 600 | 315 to 500 | High torque | 1000 to 2200 | 3 |
| KTE-135D | 133 | 44 to 56 | 500 | 700 to 1200 | High torque | 2500 to 6000 | 3 to 4 |
Output figures above are for recycled compounding with filler and a two-stage devolatilization configuration. Clean virgin masterbatch work on the same machines runs considerably higher; recycled feed with low bulk density flake and a long vented section deliberately trades throughput for quality, and any supplier quoting a single output number without stating the material and configuration is quoting a marketing figure rather than an engineering one.
Configuration options that matter for recycled feedstock
| Option | Standard configuration | Recycled compounding configuration | Why it matters |
|---|---|---|---|
| Barrel length | 40 to 44 L:D | 48 to 56 L:D | Room for two vents plus side feeding without shortening the mixing zones |
| Barrel liner | Nitrided | Bimetallic wear-resistant liner | Mineral filler and residual contamination are abrasive |
| Screw element material | Nitrided steel | High-alloy tool steel or powder metallurgy grade | Extends element life against filler abrasion |
| Feed opening | Standard | Enlarged with optional crammer feeder | Low bulk density flake needs help entering the barrel |
| Vent arrangement | One vent | Atmospheric plus vacuum, optional second vacuum | The foundation of odor and volatile control |
| Vacuum system | Single-stage water ring pump | Two-stage system with condenser and separator | Reaches minus 0.09 MPa and beyond reliably |
| Filtration | Manual screen changer | Double-piston or continuous screen changer | Recycled feed blinds screens far faster than virgin |
| Control system | PLC with touch screen | PLC with recipe management and data logging | Batch traceability is what wins repeat orders |
Application industries served by the KTE platform
Kerke’s KTE machines are in daily production across masterbatch and compounding sectors: color masterbatch, filler masterbatch, additive masterbatch, black masterbatch and textile masterbatch; engineering plastic compounds, biodegradable plastic compounds, cable compounding, PVC compounding, thermoplastic elastomer compounding and wood-plastic composites; plus recycled polyester flake processing, pet food processing and textured vegetable protein food processing lines. For the recycled modification work described in this article, the most common end products are automotive interior trim substrates, appliance housings and internal brackets, logistics crates and pallets, garden and outdoor furniture components, drainage and cable protection parts, industrial packaging, and non-pressure building components.
14. Kerke Feeding and Auxiliary Systems
Feeding accuracy is the most underestimated determinant of formula consistency. A recipe specified to a hundredth of a part means nothing if the antioxidant feeder drifts by five percent between shifts. On recycled lines, where the base material itself already varies, feeding precision is the only variable fully under the operator’s control — which makes it the place where consistency is won or lost.
Kerke supplies a complete feeding and downstream package alongside the KTE extruders, covering volumetric metering, loss-in-weight gravimetric feeding, twin-screw side feeders, crammer feeders for low bulk density material, liquid feeders for chain extenders and liquid additives, and a full range of pelletizing systems.
| Equipment | Capacity range | Accuracy | Applicable material | Recycled compounding role |
|---|---|---|---|---|
| Loss-in-weight feeder, single screw | 0.4 to 400 kg/h | Plus or minus 0.5 to 1 percent | Pellets, powders, additive blends | Main feed and all critical additive streams |
| Loss-in-weight feeder, twin screw | 0.2 to 250 kg/h | Plus or minus 0.5 percent | Poor-flowing powders, talc, adsorbents | Fine mineral and stabilizer dosing |
| Volumetric metering feeder | 1 to 500 kg/h | Plus or minus 2 to 3 percent | Free-flowing pellets and regrind | Non-critical bulk streams only |
| Twin-screw side feeder | 50 to 3000 kg/h | Matched to main feed rate | Mineral filler, glass fiber, high-loading additives | Downstream filler introduction after first melting |
| Crammer feeder | 20 to 1500 kg/h | Volumetric with level control | Flake, fluff, film scrap, low bulk density regrind | Forces low-density recycled feed into the barrel |
| Liquid feeder with metering pump | 0.1 to 60 kg/h | Plus or minus 1 percent | Liquid chain extenders, oils, liquid stabilizers | Precise injection of reactive liquid additives |
| Water strand pelletizing system | 50 to 3000 kg/h | Pellet length plus or minus 0.3 mm | Polyolefin and polyester compounds | Standard choice for most recycled compounds |
| Water ring die face hot cutting | 100 to 2500 kg/h | Uniform spherical pellets | Low viscosity and adhesive compounds | Good for tacky recycled polyolefin grades |
| Underwater pelletizing system | 200 to 6000 kg/h | Very uniform pellet geometry | High output polyolefin and polyester | Best pellet consistency at high throughput |
| Air-cooled die face hot cutting | 30 to 800 kg/h | Moderate uniformity | Moisture-sensitive compounds | Avoids water pickup on hygroscopic grades |
| High-speed mixer | 100 to 1000 liters | Batch homogeneity | Powder premixes and additive blends | Pre-blending stabilizer packages before dosing |
| Plastic granulator and pulverizer | 100 to 1500 kg/h | Screen-dependent particle size | Purgings, off-spec strand, rework | In-house scrap recovery back into the line |
Why gravimetric feeding pays for itself on recycled lines
Volumetric feeders meter by volume, which means their mass output changes whenever bulk density changes. Recycled flake bulk density can vary noticeably between bales, between the top and bottom of a silo, and even with ambient humidity. A loss-in-weight gravimetric feeder measures actual mass loss over time and corrects continuously, holding the recipe regardless of bulk density drift. On a filled recycled compound where the customer specification includes an ash content window, gravimetric feeding on both the main and filler streams is not optional — it is the mechanism that keeps the ash result inside the window from lot to lot.
15. Melt Filtration and Black Spot Control
Black spots are the most visible quality defect in recycled compound, and they come from three distinct sources that require three distinct remedies: carbonized stagnant melt inside the machine, degraded material at worn clearances, and unfiltered solid contamination arriving with the feedstock. Attacking only the third — by adding finer screens — while ignoring the first two is why some lines never fully solve the problem.
Source one: carbonized stagnant melt
Any dead zone in the flow path will eventually hold melt long enough for it to carbonize, and then release it as black particles. The classic locations are behind worn screw element flights, at poorly matched barrel joints, at the transition into an oversized adapter, in an oversized die manifold, and around the vent port throat. The structural answer is self-wiping screw geometry with tight, well-maintained clearances and a streamlined melt path with no cavities. Kerke’s kneading co-type elements are designed for exactly this self-cleaning behavior, and the practical maintenance rule is to measure screw element and barrel liner wear at scheduled intervals rather than waiting for spots to appear in product.
Source two: degradation at worn clearances
As barrel liners and screw elements wear, the clearance between them grows. Material trapped in an enlarged clearance circulates rather than conveying, accumulates heat history and eventually degrades. This mechanism explains why black spot complaints often begin gradually on a machine that ran cleanly for years. Wear-resistant bimetallic liners and high-alloy screw elements extend the interval substantially on abrasive filled recycled compounds.
Source three: solid contamination in the feedstock
Wood fiber, paper label residue, aluminium foil fragments, rubber, cross-linked polymer gel and unmelted higher-melting polymer all arrive with post-consumer material. Melt filtration is the barrier, and mesh selection is a balance: finer screens catch more but blind faster and raise melt pressure and shear.
| Screen mesh | Approximate opening | What it removes | Blinding rate on post-consumer feed | Typical application |
|---|---|---|---|---|
| 20 to 40 mesh | Coarse | Large solids, label fragments, wood pieces | Low | First-stage protection on heavily contaminated feed |
| 60 to 80 mesh | Medium | Medium contamination, most visible specks | Moderate | General recycled polyolefin compounding |
| 100 to 150 mesh | Fine | Fine specks, small gels | High | Technical grades and light-colored compounds |
| 200 mesh and finer | Very fine | Micro gels and fine carbonized particles | Very high | Fiber grade polyester and thin film applications only |
| Filtration technology | Continuity | Melt loss | Suitable contamination level | Capital cost level | Best fit |
|---|---|---|---|---|---|
| Manual plate screen changer | Requires line stop | Low | Very low | Low | Clean in-house scrap only |
| Hydraulic single-piston screen changer | Brief pressure interruption | Low | Low to medium | Low to Medium | Lightly contaminated regrind |
| Double-piston screen changer | Continuous, no line stop | Low | Medium | Medium | The standard choice for recycled compounding |
| Continuous belt or plate filter | Fully continuous | Medium | High | High | Heavily contaminated post-consumer streams |
| Backflush laser filter | Fully continuous with self-cleaning | Medium to high | Very high | Very High | Film and fiber recycling with paper and wood load |
16. Quality Control Plan for Recycled Compounds
A recycled compound business is a consistency business. The technical content of the formula is replicable by any competent competitor; what is not easily replicated is a supply of pellets that behaves the same way in the customer’s molding machine every week. That outcome comes from three mechanisms: continuous in-line process monitoring, a disciplined batch testing schedule, and physical homogenization of output.
In-line monitoring parameters
| Parameter | Sensor location | Normal behavior | What a deviation indicates | Alarm response |
|---|---|---|---|---|
| Melt pressure | Before screen changer and before die | Steady within plus or minus 0.3 MPa | Rising: screen blinding. Falling: feed interruption or viscosity drop | Change screen or check feeder |
| Melt temperature | Immersion probe before die | Within 6 degrees Celsius of setpoint | Rising: excessive shear or worn elements | Reduce screw speed, review screw configuration |
| Motor torque | Drive controller | Steady within plus or minus 4 percent | Fluctuating: inconsistent feed or bulk density drift | Check crammer and gravimetric feeder performance |
| Vacuum level | Vacuum line gauge | Steady at setpoint | Weakening: seal leak, warm sealing water, port fouling | Service pump, clean vent insert, cool sealing water |
| Feeder mass flow | Each loss-in-weight feeder | Within plus or minus 1 percent of setpoint | Drift: bridging, refill fault, load cell drift | Check hopper flow and recalibrate |
| Water bath temperature | Strand cooling bath | Stable within 3 degrees Celsius | Rising: cooling capacity fault, causes soft pellets | Check chiller and flow rate |
Batch testing schedule
| Test | Frequency | Sample point | Acceptance criterion | Action on failure |
|---|---|---|---|---|
| Melt flow rate | Every 2 hours and every lot change | Pellet stream after pelletizer | Within plus or minus 15 percent of grade nominal | Hold lot, adjust chain extender or feed blend |
| Ash content | Every 4 hours | Pellet stream | Within plus or minus 1.5 percentage points of target | Recalibrate filler feeder |
| Moisture | Every shift | Pellets after drying or storage | Below grade limit | Extend drying, check silo sealing |
| Pellet appearance and black spot count | Every hour, visual on a fixed sample mass | Pellet stream | Below agreed spots per unit mass | Change screen, inspect screw wear |
| Notched impact and tensile | Every lot | Injection molded test specimens | Within specification band | Hold lot, review elastomer and compatibilizer dosing |
| Odor grade | Every lot for odor-critical grades | Pellets, VDA 270 procedure | At or better than agreed grade | Raise vacuum, review melt temperature, adjust adsorbent |
| Color and yellowness index | Every lot for colored grades | Molded plaque | Within agreed color tolerance | Adjust pigment, review antioxidant package |
| Intrinsic viscosity, polyester only | Every lot | Pellets | Within plus or minus 0.02 dL/g of target | Adjust chain extender, verify drying performance |
Homogenizing silos: the cheapest consistency tool available
Even with perfect process control, output varies slowly over a production run as the feedstock bale changes. Blending several hours of production in a homogenizing silo before packing averages that variation out. A gravity-blend silo with internal blending tubes, sized to hold four to eight hours of output, typically cuts lot-to-lot melt flow rate variation by a third to a half. In terms of customer-perceived consistency per unit of capital spent, a homogenizing silo outperforms almost any additive intervention, and it is one of the first upgrades Kerke’s engineers recommend to compounders whose test results are acceptable on average but too scattered.
17. Requirement to Machine and Formula Selection Table
The table below maps common recycled compounding briefs to a recommended Kerke KTE configuration, a formula tier from the earlier sections, and the critical options that must be specified at order time rather than retrofitted later.
| Customer scenario | Recommended Kerke model | Barrel L:D | Formula tier | Critical configuration |
|---|---|---|---|---|
| 500 kg/h recycled PP injection grade with talc, appliance and crate parts | KTE-65B or KTE-75D | 48 | Standard rPP tier | Twin-screw side feeder for talc, one atmospheric plus one vacuum vent, double-piston screen changer, water strand pelletizing |
| 1000 kg/h recycled HDPE pipe and conduit grade | KTE-75D or KTE-95D | 52 | rHDPE pipe grade with chain extender | Liquid feeder for chain extender, deep vacuum two-stage system, carbon black masterbatch dosing, continuous filtration |
| Recycled PET sheet grade, intrinsic viscosity target 0.72 dL/g | KTE-75D with high-torque drive | 48 to 52 | rPET sheet and strapping formula | Crystallizing dryer with dew point minus 40 degrees Celsius, minus 0.095 MPa vacuum, high-temperature barrel package, fine filtration |
| Mixed polyolefin low-end products, crates and drainage parts, 800 kg/h | KTE-75D | 52 | Mixed polyolefin recipe | Crammer feeder for low bulk density flake, side feeder for calcium carbonate, two vacuum ports, wear-resistant bimetallic liner |
| Odor-critical automotive interior substrate from post-consumer PP | KTE-65B or KTE-75D | 56 | High-performance rPP tier | Two vacuum vents plus steam stripping water injection, condenser and separator, low-shear screw configuration, homogenizing silo |
| Formula development and small-batch trials before scale-up | KTE-16B or KTE-26B laboratory unit | 40 to 48 | All tiers, trial quantities | Segmented screw kit, both vent types, quick-change die, data logging control |
| 2500 kg/h and above, large-scale recycled polyolefin compounding | KTE-95D or KTE-135D | 52 to 56 | Economy or standard tier depending on end use | High-torque drive, three vents, continuous filtration, underwater pelletizing, homogenizing silo |
| Difficult materials that cannot be processed in one pass | Double-stage extrusion system, mother-baby configuration | Combined | Case-specific | First stage for melting and coarse devolatilization, second stage for gentle finishing and deep vacuum |
18. Common Problems and Fixes
Nearly every problem in recycled compounding traces back to one of four root causes: volatiles that were not removed, shear that was too aggressive, feeding that was not steady, or contamination that was not filtered. The troubleshooting table below is organized by symptom, with causes listed in the order they should be checked.
| Symptom | Probable causes, in check order | Corrective actions |
|---|---|---|
| Black spots in pellets | Carbonized melt in dead zones; worn screw elements or barrel liner; insufficient filtration mesh; contamination in feedstock; degraded material in the die manifold | Inspect and replace worn elements; step filtration one mesh finer; shorten screen change interval; purge and clean the die and adapter; verify self-wiping element condition; improve upstream sorting |
| Strong odor in finished pellets | Vacuum level too shallow; vented section too short; melt temperature too high; degree of fill too high under the vent; no steam stripping on a heavily contaminated feed | Service the vacuum pump and seals; cool the sealing water; extend vent conveying pitch; reduce melt temperature 10 to 15 degrees Celsius; add a second vacuum port or water injection; add adsorbent only after these steps |
| Notched impact strength drops between lots | Feedstock composition changed; elastomer feeder drifting; filler over-dosed; excessive shear degrading the matrix; compatibilizer under-dosed for the filler surface area | Run incoming characterization on every bale; switch critical streams to gravimetric feeding; verify ash content; replace 90 degree kneading blocks with 45 degree blocks; recalculate compatibilizer against filler surface area; install a homogenizing silo |
| Melt fracture and rough strand surface | Melt temperature too low at the die; die land geometry too aggressive; viscosity too high after chain extension; no processing aid; output above the die’s capability | Raise die temperature moderately; open the die land; reduce chain extender dosage; add 0.05 to 0.15 parts of processing aid; increase die hole count |
| Vacuum port flooding | Degree of fill too high under the port; melt viscosity too low; throughput surging; blocked vent insert; missing melt seal upstream | Fit longer-pitch conveying under the port; install a vent stuffer; steady the feed with gravimetric control and a crammer; clean or redesign the vent insert; add a short sealing element upstream |
| Pellet size variation | Strand diameter fluctuating from output surging; pelletizer blade wear; feed roll pressure incorrect; water bath temperature drifting; die hole partially blocked | Stabilize feeding and torque; regrind or replace pelletizer blades; reset feed roll pressure; stabilize bath temperature; clean the die plate |
| Yellowing or color drift | Antioxidant package insufficient; melt temperature too high; residence time too long; oxygen ingress at the feed throat; pigment carryover from the feedstock | Raise phosphite secondary antioxidant to 0.2 parts; reduce melt temperature; shorten high-shear zones; consider nitrogen blanketing at the feed; move the grade to a darker color |
| Torque fluctuation and unstable output | Bulk density variation in the flake; bridging in the feed hopper; crammer feeder speed mismatched; screw wear; moisture flashing in the melting zone | Use gravimetric feeding and a level-controlled crammer; fit hopper agitation; match crammer speed to intake; measure element wear; improve pre-drying |
| Gels in the compound | Cross-linked polyethylene fraction in the feed; chain extender over-dosed; localized overheating; unmelted higher-melting contaminant | Improve filtration; reduce chain extender dosage; verify barrel zone temperatures; check differential scanning calorimetry for a foreign polymer peak |
| Intrinsic viscosity below target in polyester | Drying incomplete; dew point too high; vacuum insufficient; chain extender fed at the main hopper; melt temperature too high | Verify residual moisture below 50 parts per million; confirm dew point of minus 40 degrees Celsius; raise vacuum toward minus 0.095 MPa; move chain extender to a downstream feed port; reduce barrel temperature |
19. Service and Support
A twin screw devolatilization extruder configured for recycled work is a long-service-life asset, and its economics depend as much on support as on the initial specification. Kerke, a Wanplas factory, structures its service around the Wanplas group commitments and around the specific realities of recycled compounding, where feedstock changes constantly and formulas need periodic revisiting.
Before shipment
Every machine is assembled and tested before it leaves the factory. For recycled compounding configurations, Kerke’s engineers verify screw assembly against the agreed configuration drawing, run the vacuum system to confirm it reaches the specified level, check feeder calibration across the intended dosing range, and perform a running test to confirm drive, heating, cooling and control functions. Where a customer supplies representative feedstock in advance, a trial run on the actual material is arranged so that the machine ships with a validated process window rather than a generic one.
Installation, commissioning and training
Kerke provides installation and commissioning support, either on site or through guided remote commissioning. Operator training covers screw assembly and disassembly, element identification and configuration logic, vacuum system operation and maintenance, screen changer operation, feeder calibration, recipe management in the control system, and the safety procedures for high-temperature melt and rotating equipment. For recycled work the training places particular emphasis on how to read torque, melt pressure and vacuum trends as early warnings of a feedstock change.
Spare parts and warranty
The Wanplas group spare parts policy provides USD 500 free parts per year, with free replacement of parts that fail within the warranty period. For recycled compounding lines the recommended stock list is short and specific: a set of wear-prone screw elements from the filler side feeding and second mixing zones, spare screen packs in the operating mesh range, vacuum pump seals and sealing water filters, pelletizer blades, and thermocouples. Holding these items locally converts the most common stoppages from multi-day events into one-shift events.
Remote support and factory visits
Machines specified with data-logging control systems can be supported remotely, with Kerke engineers reviewing torque, temperature, pressure and vacuum trend data to diagnose process drift without travel. The Wanplas open factory policy applies to Kerke’s 19,997 square meter manufacturing base: customers and prospective customers are welcome to visit, inspect machines under construction, and witness trial runs.
Formula development and trial runs
Formula work on recycled material is empirical. Kerke maintains laboratory twin-screw extruders — the KTE-16B and KTE-26B class machines — specifically so that a customer’s actual feedstock can be compounded at small scale before a production machine is configured. Wanplas can arrange small-batch formula verification and machine trials, so that the screw configuration, vent arrangement and additive package are proven on the real material rather than assumed from a datasheet. For a recycled compounding project, this trial step is the single most effective way to avoid specifying a machine that is one vent port or four L:D short of what the material actually needs.
20. Frequently Asked Questions
Can a twin screw devolatilization extruder remove odor from recycled plastic without additives?
To a large extent, yes. A correctly configured two-stage vent layout — an atmospheric vent after the first melting zone plus a vacuum vent at minus 0.085 to minus 0.095 MPa in the final third of the barrel — typically improves the VDA 270 odor grade by one to one and a half grades with no additive at all. Adding steam stripping can extend that to two grades on heavily contaminated post-consumer packaging streams. Adsorbent additives are then used only to close the last small gap, which is exactly the sequence that keeps a low cost recycled plastic modification formula genuinely low cost.
What is the minimum additive package for a low cost recycled PP formula?
An economy recycled polypropylene recipe needs only three things: a hindered phenol primary antioxidant at 0.10 to 0.15 parts, a phosphite secondary antioxidant at 0.10 to 0.15 parts, and a lubricant at 0.15 to 0.25 parts. Filler is added for stiffness and cost dilution, not for stabilization. Impact modifier and compatibilizer belong in the recipe only when the notched impact target exceeds what the base regrind delivers on its own, which the incoming characterization sheet will tell you before you spend anything.
How much intrinsic viscosity can a chain extender recover in recycled PET?
With correct crystallizing at 130 to 150 degrees Celsius, drying at 160 to 170 degrees Celsius for 4 to 6 hours to a dew point of minus 40 degrees Celsius, and high vacuum devolatilization at minus 0.090 to minus 0.098 MPa, an epoxy-functional styrene-acrylic oligomer chain extender at 0.3 to 0.8 parts commonly lifts intrinsic viscosity from around 0.58 dL/g to 0.70 to 0.78 dL/g. That range covers sheet, thermoformed tray, strapping and engineering compound applications. Bottle grade above 0.80 dL/g requires solid-state polycondensation and cannot be reached by extrusion chain extension alone.
Which Kerke KTE model suits 500 kg/h of recycled PP injection grade compound?
A KTE-65B covers 300 to 700 kg/h of filled recycled polypropylene and is the economical choice; a KTE-75D covers 500 to 1100 kg/h and leaves room for future growth. Either should be specified with a 48 L:D barrel, one atmospheric and one vacuum vent, a twin-screw side feeder for talc, gravimetric feeding on the main and additive streams, and a double-piston screen changer. The extra barrel length is what allows both vents and the side feeder to coexist without shortening the mixing zones.
Why do black spots appear in recycled compound pellets and how are they eliminated?
Black spots have three sources: carbonized melt sitting in dead zones inside the machine, degraded material circulating in enlarged clearances at worn screw elements or barrel liners, and solid contamination arriving with the feedstock. The remedies are correspondingly three: self-wiping screw geometry with a streamlined melt path and no cavities, scheduled wear measurement with timely element and liner replacement, and appropriately specified melt filtration with a disciplined screen change interval. Adding finer screens alone will not solve a problem whose origin is inside the barrel.
Does adding more filler always lower the cost of a recycled compound?
No, and this is the most expensive misconception in the business. Up to roughly 20 to 25 parts of talc or activated calcium carbonate, the material index falls while properties stay acceptable. Beyond about 30 parts, notched impact and weld line strength fall sharply, surface quality deteriorates, and the compound starts to fail at the customer’s molding machine. Rejection cost then rises faster than the material index falls, so the true cost per accepted kilogram increases. The optimum filler level is always the one that clears the mechanical specification with a small margin, not the maximum the melt will carry.
Should filler be added at the main hopper or through a side feeder?
Through a side feeder, downstream of the first melting zone, in essentially all cases above about 10 parts loading. Feeding mineral filler at the main hopper means the filler passes through the entire melting section, where it abrades the screw elements and barrel liner, absorbs shear energy that should be melting polymer, and disrupts the solids conveying that low bulk density recycled flake already struggles with. Side feeding into a starved zone after melting gives better dispersion at lower shear and dramatically extends component life.
How much can specific energy consumption be reduced on a recycled compounding line?
Realistically, a line running 0.24 kWh/kg on recycled polypropylene can usually be brought to 0.17 to 0.20 kWh/kg through three changes: replacing aggressive 90 degree and reverse kneading blocks with a greater number of 45 degree and toothed elements, lowering barrel setpoints by 10 to 15 degrees Celsius now that shear heating is reduced, and stabilizing feeding so the drive is not repeatedly accelerating against surges. Those same three changes reduce degradation, improve odor grade and extend screw life, which is why gentle plastication is the recurring theme of this guide.
21. Conclusion
A genuinely low cost recycled plastic modification formula for a twin screw devolatilization extruder is built in a specific order, and the order matters more than any individual ingredient. First, characterize the feedstock so that decisions are made on data rather than insurance. Second, strip the melt with a properly engineered two-stage vent system — atmospheric venting for the steam load, deep vacuum at minus 0.085 to minus 0.095 MPa for the low molecular weight residue, and steam stripping where the odor specification demands it. Third, dose the smallest additive package that clears the specification, starting with the antioxidant pair and lubricant that always pay for themselves and descending the cost-effectiveness ranking only as far as the requirement forces you. Fourth, protect consistency with gravimetric feeding, appropriate melt filtration, in-line monitoring and a homogenizing silo.
The recipes in this guide — three tiers for recycled polypropylene, three application grades for recycled high-density polyethylene, three intrinsic viscosity routes for recycled polyester, and a working mixed polyolefin formula — are starting points calibrated to real production windows. They assume a barrel long enough to hold two vents and a side feeder, a screw configured for gentle plastication rather than maximum shear, and feeding accurate enough that a formula written to a hundredth of a part actually arrives in the melt that way. Without that hardware foundation, the same recipes will underperform and the additive levels required to compensate will erase the cost advantage entirely.
Kerke, a Wanplas factory with more than twelve years of specialization in parallel co-rotating twin-screw compounding extruders, a 19,997 square meter manufacturing base, more than 2,000 machines in service across over 70 countries and a technical team of more than 100 people, configures KTE series machines from the KTE-16B laboratory unit to the KTE-135D production machine specifically for this class of work. Barrel length, vent arrangement, screw configuration, feeding accuracy and filtration technology are specified against the material and the target specification, not against a catalog default.
If you are planning a recycled compounding line or trying to lift an existing one out of a batch-consistency problem, send the details that matter: the feedstock type and its typical characterization data, the target properties and odor grade, the required output, and the end application. Kerke’s application engineers will propose a machine configuration, a screw layout and a formula tier matched to that brief, and Wanplas can arrange small-batch formula verification and a trial run on your actual material before anything is committed. Factory visits are welcome, and witnessing a trial on your own feedstock remains the most reliable way to confirm that a configuration will do what the specification says it will.