Most recycling plants that fail to reach their rated output do not fail because the twin-screw extruder is too small. They fail because the building around the extruder was drawn before anyone modeled the material flow. Contaminated waste plastic arrives wet, dirty, bulky and inconsistent, and every one of those properties translates directly into floor area, ceiling height, drainage, ventilation and traffic lanes. When a factory area layout for contaminated waste plastic twin screw extrusion is planned properly, the line runs at 85 to 92 percent utilization with two operators per shift. When it is planned badly, the same equipment set delivers 55 to 65 percent utilization, the pellet quality drifts batch to batch, and the plant spends its first three years fighting problems that a drawing could have solved in a week.
This guide is written for the person who has already decided to buy a co-rotating parallel twin-screw compounding line and now has to tell an architect how many square meters to draw, how high the roof must be, where the walls go and how the forklifts move. It gives a repeatable area calculation method organized by output tier, a contamination grading system that scales that area up or down, detailed clearance rules for the extrusion hall, and utility sizing tables that let you brief an electrical and mechanical contractor with real numbers rather than guesses. Everything below is written around the reality of dirty feedstock: soil, sand, labels, adhesive, oil residue, free water and bound moisture.
Kerke, a Wanplas factory, has spent more than 12 years designing and building parallel co-rotating twin-screw compounding extruders, with a 19,997 sqm manufacturing base, more than 2,000 machines running in over 70 countries, and a team of more than 100 people focused on one product family. That focus matters for layout work, because the questions a recycler actually asks are not about the extruder in isolation. They are about how far the buffer silo sits from the feeder, whether the crane can lift a barrel section, how much straight aisle a screw pull needs, and where the vacuum pump water goes. Kerke engineers answer those questions every week, and this article condenses the recurring answers into tables you can hand to a civil designer. For upstream washing and dewatering, Wanplas supplies matched pre-treatment lines that feed directly into Kerke twin-screw systems, so the whole chain from bale to bagged pellet can be dimensioned as one drawing rather than two disconnected projects.
Why Layout Decides Throughput in Contaminated Plastic Recycling
Layout decides throughput because contaminated plastic is a low-bulk-density, high-variance material that must be moved many times before it reaches the feed throat. Every extra meter of travel, every crossing path and every missing buffer converts directly into idle extruder minutes. In a clean virgin compounding plant, the extruder is the constraint. In a contaminated recycling plant, the constraint is almost always material handling, and material handling is a function of the floor plan.
Five layout mistakes account for the large majority of underperforming contaminated-plastic extrusion workshops. They repeat across countries, across feedstocks and across plant sizes, and each one has a specific throughput cost that can be estimated before construction starts.
Mistake One: Receiving and Finished Goods Share the Same Traffic Path
When incoming bales and outgoing pellet bags use the same door, the same apron and the same forklift lane, three things happen. Trucks queue and block each other, so receiving becomes a stop-start activity that pulls forklifts away from feeding the line. Soil and dust from bale handling settle on finished pallets, which triggers customer complaints about dirty bags even when the pellets inside are clean. And any food-contact or high-specification order becomes impossible to certify, because there is no defensible separation between dirty inbound and clean outbound material. The fix costs almost nothing at drawing stage and is very expensive later: two separate doors on opposite ends or opposite faces of the building, with a one-way internal loop.
Mistake Two: Crusher Dust Migrates Into the Extrusion Area
Crushing dry contaminated film releases a fine mixture of polymer fines, soil, paper fiber from labels and dried organic residue. If the crusher sits in the same open hall as the extruder, that dust settles on the barrel heaters, the motor cooling fins, the electrical enclosure filters and the open feed hoppers. The consequences are cumulative: heater bands overheat and fail early, drive enclosures trip on high temperature in summer, and airborne fines that fall into the feed throat produce black specks and gel defects in the pellet. There is also a combustible dust dimension, because a suspended cloud of dry polymer fines near hot surfaces is a recognized ignition scenario. Separating crushing behind a solid partition with local extraction is the single highest-value wall in the whole building.
Mistake Three: The Dewatered Material Silo Sits Too Far From the Feeder
Washed and dewatered flakes still hold 2 to 8 percent surface moisture and tend to bridge, so they are pneumatically or mechanically conveyed with more difficulty than virgin pellets. Long conveying runs increase fines generation, increase blockage frequency and add heat losses that partly undo the thermal drying step. A practical rule is to keep the horizontal distance between the buffer silo discharge and the loss-in-weight feeder inlet below 15 m for washed flakes and below 25 m for dry regrind, with no more than two 90 degree bends in a pneumatic line. Where the plot forces a longer run, switch to a mechanical belt or a screw conveyor in an enclosed trough rather than pushing air velocity higher.
Mistake Four: No Buffer Silo Between Batch Pre-treatment and Continuous Extrusion
Washing and drying are inherently semi-batch operations. Bales are opened in lots, wash tanks are drained and refilled, and dryers cycle. Twin-screw extrusion is continuous. Without a buffer, the extruder inherits every hiccup upstream, and a plant that could run 20 hours a day runs 13. Sizing the buffer for 60 to 120 minutes of extruder consumption removes most of that coupling. At 1000 kg/h and a bulk density around 0.30 to 0.35 t/m3 for washed film flakes, 60 minutes of buffer is roughly 3 m3 of usable volume, and 120 minutes is roughly 6 m3. That volume is trivial in cost terms and transformational in utilization terms, but it needs floor space and ceiling height that must be reserved in the drawing.
Mistake Five: Insufficient Maintenance Access Around the Extruder
A contaminated-feedstock line is a maintenance-heavy line. Screens are changed more often, screw elements wear faster because of mineral abrasives, and the vent ports need periodic cleaning. If the extruder is pushed against a wall to save space, every one of those routine tasks becomes a shutdown event that requires disassembling something else first. The clearance rules in the extrusion hall section below are not luxuries. They are the difference between a 40 minute screen-changer service and a four hour one.
Material Flow Model: From Bale to Pellet
A layout is only as good as the flow model behind it. Before any wall is drawn, write down every processing stage in sequence, assign each stage to a zone, and record the layout constraint that stage imposes. The table below is the reference flow for contaminated post-consumer and post-industrial plastic feeding a twin-screw compounding line with devolatilization. Not every plant needs every stage, but every plant should consciously delete a stage rather than forget it.
| Step | Stage | Function | Zone | Primary layout constraint |
|---|---|---|---|---|
| 1 | Receiving and weighing | Truck unloading, weighbridge, incoming inspection and moisture check | Dirty | Paved apron for a full trailer turn, weighbridge on the inbound side only, covered unloading bay |
| 2 | Bale storage yard | Buffer of 5 to 15 days of feedstock, segregated by grade and supplier | Dirty | Stack height and aisle width governed by fire code, drainage away from clean zones |
| 3 | Manual and mechanical sorting | Removal of metal, wood, textile, non-target polymer and oversize items | Dirty | Sorting platform 1.0 to 1.2 m above floor, reject bins directly under the belt, good lighting |
| 4 | Pre-washing and de-stoning | Trommel or pre-wash drum removes free soil, sand, grit and stones | Dirty | Sludge discharge point, sedimentation pit access, water supply and drain in the same bay |
| 5 | Crushing | Wet or dry size reduction to 20 to 60 mm flakes | Dirty | Acoustic enclosure, dust extraction hood, crane access above the rotor for knife service |
| 6 | Friction washing | High-speed mechanical scrubbing to strip adhesive, ink and residual soil | Dirty | Wastewater volume peaks here, floor slope to drain, splash containment kerbs |
| 7 | Sink-float separation | Density separation of PE and PP from PET, PVC, rubber and mineral fractions | Dirty | Long tank footprint, walkway both sides, skimmer discharge to dewatering |
| 8 | Mechanical dewatering | Centrifugal dewatering to 3 to 8 percent surface moisture | Transition | Vibration isolation, water return line, short discharge to the thermal dryer |
| 9 | Thermal drying | Hot air drying to below 1 percent surface moisture for stable feeding | Transition | Vertical space for the dryer column, hot air duct routing, thermal insulation clearance |
| 10 | Buffer silo | 60 to 120 minutes of decoupling volume between batch and continuous operation | Transition | Clear height above the feeder platform, level sensors, bridging breaker access |
| 11 | Twin-screw compounding with devolatilization | Melting, dispersive and distributive mixing, moisture and volatile removal | Clean | Screw pull-out aisle, crane coverage, vent port access, barrel section handling |
| 12 | Melt filtration | Removal of residual paper, metal, char and cross-polymer contamination | Clean | Screen changer pull space, waste screen bin, melt pressure instrumentation access |
| 13 | Pelletizing | Strand, water-ring or underwater cutting into pellets | Clean | Water channel run length, pump pit, cutter blade change clearance |
| 14 | Pellet dewatering and drying | Centrifugal drying of pellets to a dust-free, dry condition | Clean | Short pipe run from cutter, noise enclosure, water recirculation loop |
| 15 | Vibrating sieve | Removal of fines, agglomerates, tails and oversize pellets | Clean | Elevation above the homogenizing silo inlet, reject chute, isolation mounts |
| 16 | Homogenizing silo | Batch blending across production hours to level out property variation | Clean | Tallest structure in the clean zone, needs roof height or an outdoor silo pad |
| 17 | Bagging and palletizing | Big-bag or 25 kg bag filling, weighing, sealing and palletizing | Clean | Pallet staging area, scale calibration space, wrapping machine footprint |
| 18 | Finished goods warehouse | Storage of 7 to 20 days of production, segregated by grade and lot | Clean | Separate dispatch door, rack or block stacking layout, laboratory retention samples |
Two rules follow directly from this table. First, the transition zone exists physically, not just conceptually: dewatering, thermal drying and the buffer silo form a real bay with its own walls, its own floor drainage and its own air handling. Second, elevation changes should be planned as deliberately as horizontal distances. Stages 14 to 17 all rely on gravity or short lifts, and a plant that ignores vertical planning ends up with a forest of retrofit bucket elevators that consume floor area and generate fines.
Contamination Levels and How They Change the Layout
Contamination level is the single strongest driver of plant area, because it determines how many pre-treatment stages exist and how much water and air the plant must handle. Two plants with identical twin-screw extruders can differ by a factor of two and a half in total footprint purely because one runs clean industrial scrap and the other runs field-collected agricultural film. Grading feedstock into four levels makes the area calculation in the next section reproducible.
| Level | Typical feedstock | Non-polymer impurity | Required pre-treatment chain | Area coefficient | Wastewater intensity | Vent configuration | Melt filter mesh |
|---|---|---|---|---|---|---|---|
| Level A | Clean in-house industrial scrap, purge, edge trim, sprue and runner | Below 1 percent | Metal separation, crushing, dedusting; no wet process | 0.55 | Negligible | Single atmospheric vent | 100 to 150 mesh |
| Level B | Post-industrial film rolls, printed but unused packaging, clean woven bags | 1 to 3 percent | Sorting, crushing, dry cleaning or short wet rinse, dewatering | 0.75 | Low, 0.2 to 0.5 L per kg | Atmospheric vent plus one vacuum vent | 80 to 100 mesh |
| Level C | Post-consumer packaging film, bottles, household rigid containers | 3 to 8 percent | Full chain: sorting, pre-wash, crushing, friction washing, sink-float, dewatering, thermal drying | 1.00 (baseline) | Medium to high, 2 to 4 L per kg | Atmospheric vent plus two vacuum vents | 60 to 80 mesh |
| Level D | Agricultural film, greenhouse film, mulch film, heavily soiled industrial packaging | 8 to 20 percent | Extended chain: de-stoning trommel, double friction washing, two-stage sink-float, high-speed dewatering, thermal drying | 1.35 | High, 4 to 8 L per kg with heavy sludge load | Atmospheric vent plus two vacuum vents and continuous filtration | 40 to 60 mesh |
The area coefficient in the table is applied to the baseline areas given in the area calculation section. It is not a linear scaling of every zone: the extrusion hall itself barely changes between Level A and Level D at the same output, while the pre-treatment zone and the water treatment area can triple. When a plant handles mixed grades, calculate the layout for the worst grade it intends to run more than 20 percent of the time, not for the average. A plant sized for the average will bottleneck every time a dirty lot arrives, and dirty lots are exactly the lots that carry the best margin.
Moisture Load Is the Hidden Area Driver
Free water leaving the dewatering stage has to be evaporated somewhere. On Level C and Level D feedstock, the twin-screw extruder with two vacuum vent stages can absorb the last 0.5 to 1.5 percent of moisture, but it cannot economically absorb 6 percent. Trying to skip thermal drying to save floor area shifts the load onto the vent system, which then requires larger vacuum capacity, larger condensate handling and more frequent vent port cleaning, while output falls by 15 to 30 percent because vent flooding limits screw speed. The floor area saved by deleting the dryer is typically 40 to 90 sqm; the output lost is worth far more. Keep the dryer, and keep it close to the buffer silo.
Zoning Principles: Dirty, Transition and Clean
Zoning is the discipline that keeps a contaminated plastic plant from contaminating its own product. The principle is simple: material moves in one direction from dirty to clean, air moves in the opposite direction from clean to dirty, and people and vehicles cross the boundary only through controlled points. Everything else in this section is an implementation detail of those three statements.
The Three Zones Defined
The dirty zone covers receiving, bale storage, sorting, pre-washing, crushing, friction washing and sink-float separation. It is wet, dusty, noisy and odorous, and its floor carries soil, grit and sludge. The transition zone covers mechanical dewatering, thermal drying and the buffer silo. Material entering it is still damp, material leaving it is dry and ready for the feeder. The clean zone covers the twin-screw extrusion hall, melt filtration, pelletizing, pellet drying, screening, homogenizing, bagging and the finished goods warehouse. In the clean zone, product is exposed to the ambient environment at the feed throat, at the pellet dryer discharge, at the sieve and at the bagging point, so ambient air quality is a product quality parameter.
| Zone attribute | Dirty zone | Transition zone | Clean zone |
|---|---|---|---|
| Pressure regime | Slight negative pressure, minus 5 to minus 15 Pa relative to outside | Neutral to slightly negative | Neutral to slightly positive, plus 5 to plus 10 Pa |
| Air change rate | 8 to 12 changes per hour with local extraction at dust and odor sources | 6 to 8 changes per hour, higher near the dryer exhaust | 4 to 6 changes per hour, filtered make-up air |
| Floor construction | Sloped 1 to 1.5 percent to trench drains, chemical and abrasion resistant topping | Sloped to a local drain, sealed against water tracking | Flat, dust-free hardened topping, no open trenches near the feeder |
| Partition | Solid wall to underside of roof, no open transfer windows | Solid wall with airlock or strip curtain at the material pass | Solid wall, personnel doors with self-closers |
| Personnel access | Dedicated entrance from the yard, boot wash at the exit | Through the airlock only | Dedicated entrance from the office and locker area |
| Forklift traffic | Yard trucks and dirty-side forklifts only | Generally none; material moves by conveyor | Clean-side forklifts only, dedicated tires and wash-down |
| Dispatch door sharing | Never shared with finished goods | No external door required | Separate dispatch dock on the opposite face of the building |
| Typical noise level | 85 to 95 dBA at the crusher, enclosure mandatory | 75 to 85 dBA | 78 to 85 dBA at the pelletizer, hearing protection zone marked |
Pressure Gradient in Practice
The pressure gradient is what stops odor and dust from moving in the wrong direction. Achieve it by extracting more air from the dirty zone than you supply to it, and supplying more filtered air to the clean zone than you extract from it. In numerical terms, if the dirty zone extraction is 30,000 m3/h, supply about 26,000 to 27,000 m3/h of make-up air there, and let the balance leak in from the transition zone. The airlock between transition and dirty zones then always flows dirty-ward, and odors from wet organic residue never reach the bagging station. This is a cheap arrangement at design stage and nearly impossible to retrofit once ducts are installed.
One-Way Traffic and the Boot Wash Rule
Draw the forklift path as a loop, not as a shuttle. A loop means a forklift carrying bales from the yard to the sorting infeed never meets a forklift carrying pallets from bagging to dispatch. Where the plot forces a shared aisle, make it a timed corridor rather than a shared space, and mark it clearly. For personnel, place a boot wash and a compressed air blow-down station at the dirty zone exit. In plants producing pellets for demanding applications, this single station has a measurable effect on the black speck count in the finished product, because the most common carrier of soil into a clean zone is the sole of a shoe.
Area Calculation Method by Output Tier
The area calculation method below reverses the usual process: instead of drawing a building and asking what fits, it starts from the rated output in kilograms per hour and derives each zone area from empirical coefficients, then applies a contamination multiplier and a circulation allowance. The result is a defensible number you can give to a land agent or an architect on day one.
The Core Formula
Total plant footprint is calculated as the sum of the seven functional zones, each scaled by the contamination coefficient from the previous section:
A(total) = [A(yard) + A(pre-treatment) + A(drying and buffer) + A(extrusion hall) + A(pelletizing and screening) + A(finished goods) + A(utilities)] × f(contamination) × f(site)
Here f(contamination) is 0.55 for Level A, 0.75 for Level B, 1.00 for Level C and 1.35 for Level D. The factor f(site) accounts for plot geometry and is 1.00 for a rectangular plot with a favorable aspect ratio, 1.08 to 1.15 for an irregular plot that forces an L-shape or U-shape flow, and 1.20 or more where columns, existing structures or setback rules fragment the usable area. The zone areas below already include a 15 to 20 percent internal circulation allowance for aisles, operator walkways and pallet staging, so do not add circulation twice.
Baseline Area Table by Output Tier
The following table is the baseline for Level C post-consumer feedstock, single-shift capable but dimensioned for three-shift operation, with one twin-screw compounding line per tier. All figures are in square meters unless stated otherwise.
| Zone | 300 kg/h | 500 kg/h | 1000 kg/h | 2000 kg/h | Scaling logic |
|---|---|---|---|---|---|
| Raw material yard and receiving | 150 | 250 | 450 | 850 | 10 to 14 days of baled feedstock at 0.30 to 0.45 t/m3, stack height 4 m, plus truck apron |
| Pre-treatment zone (sorting, washing, crushing) | 180 | 280 | 500 | 900 | Equipment envelope plus 1.2 m walkways on both sides of each wet machine |
| Drying and buffer | 90 | 140 | 240 | 420 | Dewatering, thermal dryer column, buffer silo and feeder platform base |
| Extrusion hall | 200 | 300 | 480 | 800 | Machine footprint plus screw pull-out aisle plus crane operating envelope |
| Pelletizing and screening | 80 | 120 | 200 | 340 | Water channel, pellet dryer, vibrating sieve, homogenizing silo base |
| Finished goods warehouse | 120 | 200 | 380 | 700 | 10 to 15 days of output in big bags at 0.55 t/m3, two-high stacking, dispatch staging |
| Utilities room and workshop | 60 | 90 | 150 | 260 | Transformer room, chiller and cooling tower base, air compressor, vacuum pump room, maintenance bench |
| Total footprint (Level C) | 880 | 1380 | 2400 | 4270 | Sum of the seven zones with circulation included |
| Level A equivalent (×0.55) | 485 | 760 | 1320 | 2350 | Dry route, no washing, minimal water treatment |
| Level D equivalent (×1.35) | 1190 | 1865 | 3240 | 5765 | Extended washing chain and larger sludge and water handling |
| Minimum clear height (m) | 6.0 | 6.5 | 7.5 | 9.0 | Under the crane hook in the extrusion hall; silo bay may need 1.5 to 3 m more |
How to Use the Table Correctly
Three cautions apply. First, the yard and warehouse figures assume a 10 to 15 day inventory cycle. If your feedstock supply is seasonal, as it is for agricultural film, multiply the yard by 2 to 3 for the collection season or plan an outdoor covered stockpile with its own fire separation. Second, the extrusion hall figure covers one line. A second line does not double the hall, because the crane, aisles and control room are shared; a realistic figure for a second identical line is 70 to 80 percent of the first. Third, the utilities figure excludes an outdoor wastewater treatment plant, which for Level C at 1000 kg/h typically needs a further 150 to 300 sqm of outdoor area for tanks, a sludge press and a control cabin.
Worked Example: 1000 kg/h Post-Consumer PP
A recycler plans 1000 kg/h of washed post-consumer PP flakes compounded into a talc-filled grade for injection molding. Feedstock is Level C, the plot is rectangular with a good aspect ratio, so f(site) is 1.00. The baseline total is 2400 sqm, multiplied by 1.00 for Level C, giving 2400 sqm of process footprint. Add 250 sqm of outdoor wastewater treatment, 120 sqm of office, laboratory and locker facilities, and a 400 sqm truck maneuvering apron, and the land requirement becomes approximately 3170 sqm of developed area. Allowing for setbacks, a fire access road and a 30 percent reserve for a second line, a plot of 4800 to 5500 sqm is the correct target. That is the number to give a land agent, and it is derived, not guessed.
Extrusion Hall Detailed Layout and Clearances
The extrusion hall is where a few hundred millimeters of clearance decide whether maintenance takes 40 minutes or a full shift. The rules below are dimensional, they apply to co-rotating parallel twin-screw extruders of the KTE class, and they should be transferred directly onto the general arrangement drawing before any equipment is ordered.
Centerline Clearances
Set the extruder centerline at least 2.5 m from the nearest wall or fixed obstruction on the maintenance side, which is the side from which barrel section clamps are released, heater bands are replaced and vent ports are cleaned. On the drive side, 1.5 m is sufficient for motor and gearbox service if the crane can lift the motor vertically; increase to 2.0 m where the electrical enclosure is wall-mounted behind the machine. Leave 1.2 m minimum behind the control cabinet for rear-door access and cable pulling, and never place the cabinet where washed-flake conveying lines can drip onto it.
Screw Pull-Out Space
The most frequently violated rule in recycling plant layout is screw pull-out space. To withdraw the screw shafts for inspection, element replacement or a wear survey, you need clear straight space in front of the barrel of at least 1.2 times the working screw length. Working screw length equals screw diameter multiplied by the L/D ratio. A KTE-135D configured at 44 L/D has a working screw length of about 5.94 m, so the required clear aisle is roughly 7.1 m, and good practice is to reserve 8 to 10 m to allow a trolley and two technicians to work comfortably.
| Model | Screw diameter (mm) | L/D used for calculation | Working screw length (m) | Minimum pull-out aisle (m) | Recommended reserved aisle (m) |
|---|---|---|---|---|---|
| KTE-36B | 35.6 | 44 | 1.57 | 1.9 | 2.5 to 3.0 |
| KTE-52D | 51.4 | 44 | 2.26 | 2.7 | 3.5 to 4.0 |
| KTE-65D | 62.4 | 44 | 2.75 | 3.3 | 4.0 to 4.5 |
| KTE-75D | 71.0 | 44 | 3.12 | 3.7 | 4.5 to 5.0 |
| KTE-95D | 95.0 | 44 | 4.18 | 5.0 | 6.0 to 7.0 |
| KTE-135D | 135.0 | 44 | 5.94 | 7.1 | 8.0 to 10.0 |
Two practical notes. First, the pull-out aisle does not have to be a dead space. It can be the main hall walkway or the crane run, as long as nothing permanent is installed in it. Racks, water tanks and pallet stacks are the usual offenders. Second, if the plot genuinely cannot accommodate the full length, specify a split-shaft screw design at the ordering stage rather than discovering the problem during the first maintenance cycle.
Crane Coverage and Hook Height
An overhead traveling crane covering the whole extruder length, the screen changer and the pelletizer is not optional on lines above about 300 kg/h. Size it for the heaviest single lift, which is normally a barrel section with its heating and cooling assembly, or the gearbox. A practical capacity guide is 2 t for KTE-52D to KTE-65D lines, 3 to 5 t for KTE-75D to KTE-95D, and 5 to 10 t for KTE-135D installations. Hook height must clear the tallest fixed item on the line, typically the side feeder or the buffer silo discharge, with at least 0.8 m of slinging space above it. That is the requirement that pushes a 2000 kg/h hall to 9 m clear height.
Screen Changer, Pelletizer and Water Channel Orientation
Place the screen changer so that the hydraulic slide plate can travel its full stroke without hitting a column, and leave a 1.0 m clear zone on the discharge side for the waste screen bin and for the operator to stand clear of the purge. Behind the die, the strand pelletizing route needs a water channel of 3 to 5 m for PP and PE and up to 6 m for filled or heat-retaining compounds, followed by an air knife and the cutter. Orient this run parallel to the main aisle rather than across it, so that strand breaks can be cleared without stepping into forklift traffic. For water-ring or underwater cutting, the footprint is shorter but the pump pit, water tank and pellet dryer become a fixed cluster that needs 12 to 20 sqm and its own drain.
Control Room and Operator Sightlines
Put the operator station where it has a direct line of sight to three things: the feed throat, the die face and the pelletizer discharge. In contaminated feedstock processing, the feed throat is where surges, bridging and foreign object events first show, and a camera is a poor substitute for a direct view. A raised control room of 12 to 20 sqm with laminated glazing, positive pressure ventilation and a dedicated cable tray keeps the operator out of the noise zone while preserving those sightlines.
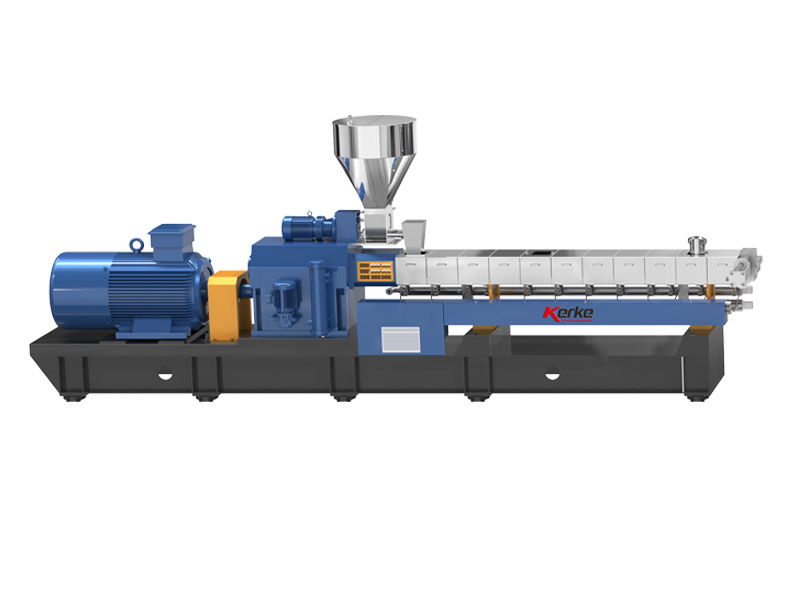
Kerke KTE Series Twin Screw Extruder
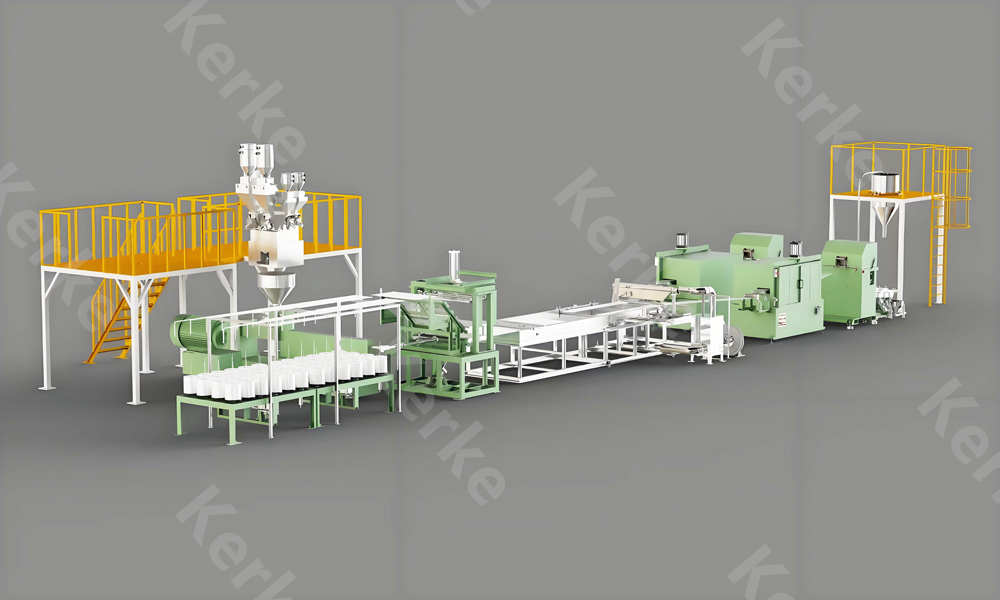
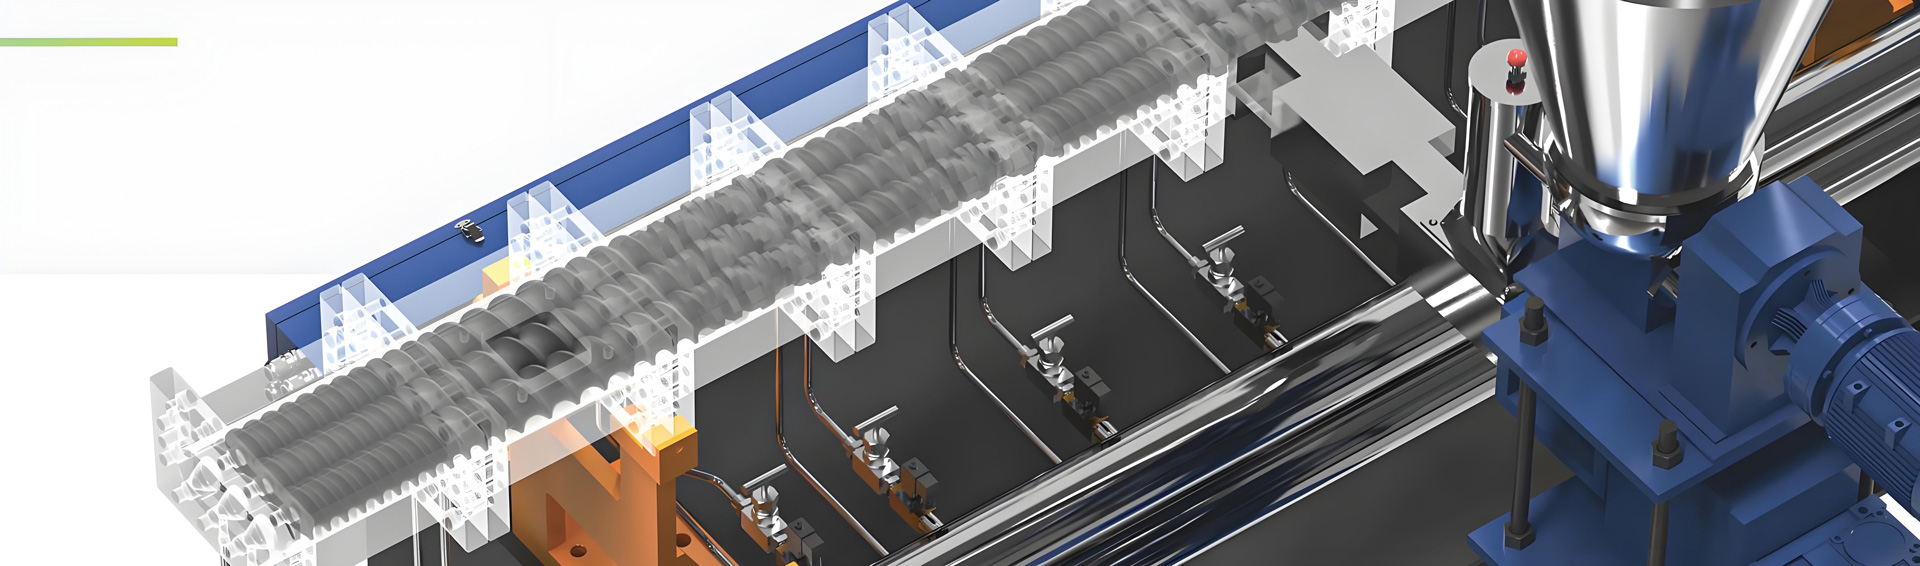
The KTE series is Kerke’s parallel co-rotating twin-screw compounding platform and the machine family around which most of the layout rules in this article are dimensioned. The range runs from the KTE-16B laboratory unit used for formula trials up to the KTE-135D production machine, and the shared design language means a plant can develop a recipe on a small machine and scale it onto a production line with the same screw geometry philosophy. Screw assemblies are computer-aided designed, use a kneading co-type geometry with strong self-cleaning behavior, and are fully interchangeable, which matters in recycling because element wear from mineral abrasives is a routine consumable cost rather than an exception.
For contaminated feedstock, the configurable elements that matter most are the aspect ratio, the barrel structure, the screw arrangement, the exhaust or vent configuration, the feeding system and the electrical control. A recycling machine is not a masterbatch machine with a different label: it usually needs a longer L/D to accommodate two vacuum vent stages, a crammer or forced side feed for low-bulk-density flakes, wear-resistant barrel liners and screw elements, and a control system tuned for feed-rate surges rather than steady-state operation.
| Model | Screw diameter (mm) | L:D ratio | Max screw speed (rpm) | Main motor power (kW) | Torque grade (N·m/cm3) | Output range (kg/h) | Machine length (m) | Machine footprint (m2) |
|---|---|---|---|---|---|---|---|---|
| KTE-16B | 15.6 | 40 to 48 | 600 | 4 | 8 to 9 | 1 to 10 | 3.0 | 6 |
| KTE-20B | 21.7 | 40 to 48 | 600 | 7.5 | 8 to 9 | 5 to 25 | 3.6 | 8 |
| KTE-26B | 25.6 | 40 to 48 | 600 | 15 | 9 to 10 | 10 to 50 | 4.5 | 11 |
| KTE-36B | 35.6 | 40 to 48 | 600 | 30 to 37 | 9 to 11 | 50 to 150 | 6.0 | 16 |
| KTE-52D | 51.4 | 40 to 48 | 600 | 55 to 75 | 10 to 12 | 150 to 350 | 8.0 | 24 |
| KTE-65D | 62.4 | 40 to 48 | 600 | 90 to 110 | 10 to 12 | 300 to 600 | 9.5 | 32 |
| KTE-75D | 71.0 | 40 to 48 | 600 | 132 to 160 | 11 to 13 | 500 to 900 | 11.0 | 42 |
| KTE-95D | 95.0 | 40 to 48 | 600 | 250 | 11 to 13 | 1000 to 1800 | 13.0 | 60 |
| KTE-135D | 135.0 | 40 to 48 | 600 | 355 | 11 to 13 | 2000 to 3500 | 16.0 | 90 |
Output ranges depend heavily on the material and the recipe. Washed post-consumer PE film with two vacuum vents and 30 percent moisture-related derating will sit at the lower end of each range, while a lightly filled post-industrial PP compound will reach the upper end. The machine footprint column covers the extruder base frame, gearbox and motor only; add the feeder platform, side feeder, screen changer and pelletizer to obtain the true equipment envelope, which is typically 2.2 to 2.8 times the extruder footprint alone.
Application Industries for the KTE Platform
Kerke’s KTE platform is used across masterbatch production, including color masterbatch, filler masterbatch, additive masterbatch, black masterbatch and textile masterbatch, and across plastic compounding, including engineering plastics, biodegradable plastics, cable compounding, PVC compounding, thermoplastic elastomers and wood-plastic composites. In recycling specifically, the platform handles R-PET flake recycling and post-consumer PP and PE compounding, and the same machine family is also applied in pet food processing and in HMMA and textured vegetable protein food processing where a co-rotating twin-screw is the standard tool. For a contaminated-feedstock plant, the practical consequence is that the machine you install for recycled PP can later be reconfigured for filled masterbatch if the market shifts, provided the layout left enough aisle and utility headroom.
Kerke SE Series Single Screw Extruder
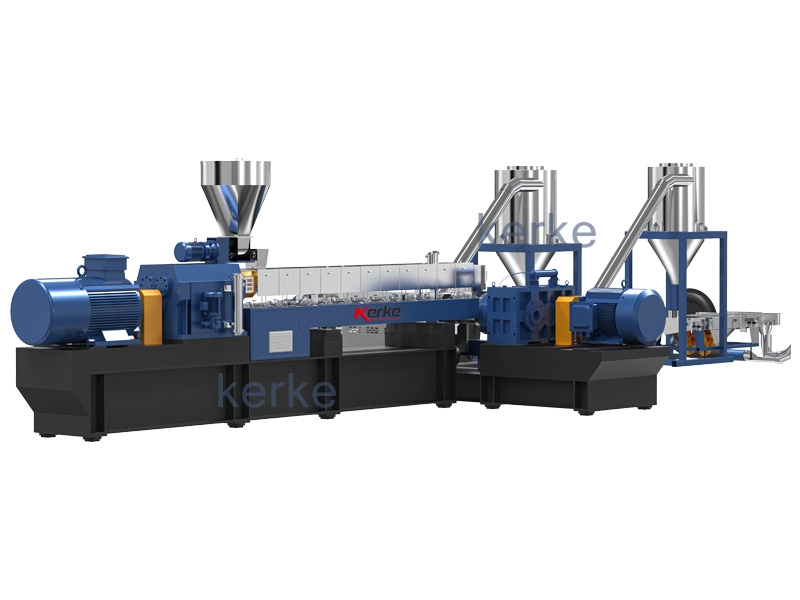
Not every stage in a recycling plant needs a twin-screw machine. The Kerke SE series single-screw extruder, with outputs from 30 kg/h to 800 kg/h, covers two distinct roles in a contaminated waste plastic layout: as the second stage of a two-stage system where the twin-screw handles compounding and devolatilization while the single-screw builds pressure for filtration and pelletizing, and as a standalone pelletizing unit for lower-specification recycled grades where dispersive mixing is not required.
The layout implications differ from the twin-screw. A single-screw machine of the same output is longer and narrower, needs less pull-out clearance relative to its length because the screw is a single shaft, and generates lower specific energy, so its cooling water demand is smaller. In a two-stage arrangement, the single-screw sits perpendicular or at a slight angle below the twin-screw discharge, which adds 3 to 5 m to the hall width but removes the pressure-building duty from the twin-screw and allows the twin-screw to run at a higher screw speed with better vent performance.
| Model | Screw diameter (mm) | L:D ratio | Motor power (kW) | Output range (kg/h) | Machine footprint (m2) |
|---|---|---|---|---|---|
| SE-65 | 65 | 30:1 | 22 | 30 to 80 | 10 |
| SE-75 | 75 | 30:1 | 30 | 60 to 120 | 12 |
| SE-90 | 90 | 30:1 | 45 | 100 to 200 | 16 |
| SE-105 | 105 | 30:1 | 55 to 75 | 180 to 300 | 20 |
| SE-120 | 120 | 30:1 | 90 | 250 to 450 | 26 |
| SE-150 | 150 | 30:1 | 132 | 400 to 650 | 34 |
| SE-180 | 180 | 30:1 | 160 to 185 | 550 to 800 | 42 |
When the Two-Stage Layout Pays for Itself
Choose the two-stage KTE plus SE arrangement when the feedstock is Level C or Level D and the target product needs both good devolatilization and fine melt filtration. The reason is mechanical: a single-stage twin-screw must simultaneously vent volatiles and build 80 to 180 bar of pressure across a fine screen pack, and those two duties fight each other. Decoupling them lets the twin-screw vent at low melt pressure and lets the single-screw build pressure steadily. The layout cost is a wider hall and one more drive to maintain. The layout benefit is that you can run 60 to 80 mesh filtration on genuinely dirty material without surging the vent ports, which on Level D feedstock can be the difference between a saleable pellet and a rejected one.
Devolatilization and Odor Control Layout
Contaminated waste plastic is never just plastic. It is plastic plus the water, the printing ink, the food residue, the detergent and the degraded low-molecular-weight fraction that came with it, and all of those leave the melt during extrusion as vapor or gas. If the building layout does not give that gas a defined path out of the plant, it will find an undefined path, usually straight into the control room or the bagging station. Devolatilization and odor control are therefore layout problems first and equipment problems second. The extruder provides the vent ports; the building provides the rooms, ducts, pumps and treatment units that make those ports work.
Atmospheric Venting as the First Stage
The first vent on a recycling twin-screw is normally an atmospheric vent placed in the early barrel zone, often around barrel position 2 or 3 depending on the screw design. Its job is to release the bulk of the entrained moisture and the lighter volatiles before the melt is sealed under pressure by the next reverse element. In layout terms this means the early barrel section sits over a vent trench or a captured hood, not over a walkway, because at start-up this port discharges a visible plume of steam and odor. Provide a local extraction canopy with a minimum face velocity of 0.5 m/s over the port, connected to the same treatment train as the vacuum vents, and never let the atmospheric vent discharge into the clean hall air.
Vacuum Vent Staging Along the Barrel
After the atmospheric vent, a recycling screw typically carries one or two vacuum vents in the later barrel zone, positioned after a set of kneading blocks where the melt has been worked and homogenized but before the final pressure-building section. The first vacuum vent removes the bulk of residual volatiles; the second, deeper vacuum vent handles the last fraction that determines the odor grade of the pellet. The geometry matters for layout: vacuum vents are tall, they need a vertical clearance above the barrel of at least 1.2 m for the vent stuffer and the sight glass, and they connect downward through a polymer trap to the vacuum line. A common error is to place an overhead crane rail or a service platform exactly where the second vacuum vent needs to stand.
| Vent position on barrel | Typical placement (L/D from feed) | Duty | Extraction air handled | Layout requirement |
|---|---|---|---|---|
| Atmospheric vent | 4 to 8 | Bulk moisture and light volatiles, atmospheric | Low, plume only | Local canopy hood plus trench drain, no walkway beneath |
| Vacuum vent 1 | 20 to 28 | Main devolatilization under first vacuum stage | Medium | Vent stuffer, polymer trap, vertical clearance 1.2 m |
| Vacuum vent 2 | 34 to 42 | Fine devolatilization and odor reduction | Medium to high | Deeper vacuum pump, separate trap, clearance above crane rail |
| Side devolatilization port | Variable | Optional for extended residence recipes | Low | Only on long L/D machines, adds one more service drop |
Vacuum Pump Room Placement
The vacuum pump room should be a dedicated, enclosed space placed on the dirty side of the building or at the perimeter wall, never inside the clean zone and never adjacent to the bagging line. The reason is twofold. First, vacuum pumps handling recycled melt vapor draw a corrosive, odorous stream that will contaminate any room it shares. Second, the pumps are a major noise source and a heat source, and enclosing them on the perimeter lets you exhaust directly to the odor treatment unit with the shortest possible duct. Size the room for the pump footprint plus 1 m on every service side, plus space for the vacuum receiver and the condensate collection drum. Route the vacuum line through a polymer trap before the pump on every line, because melted polymer reaching a vacuum pump is an expensive failure.
Odor Source Mapping
Before specifying any odor control, map where the smell is generated in the plant, because treating the wrong source wastes capital. The table below lists the usual suspects in a contaminated feedstock plant and the approximate intensity so the layout can place them correctly.
| Odor source | Generated in | Intensity at source | Layout response |
|---|---|---|---|
| Wet flake off-gassing | Pre-treatment and buffer silo | High, continuous | Enclose silo, extract to treatment, keep downwind |
| Atmospheric vent plume | Early barrel zone | High at start-up | Local canopy, treat before release |
| Vacuum vent vapor | Vacuum pump discharge | Medium to high | Route pump room exhaust to treatment unit |
| Pellet cooling water | Pellet dryer and water tank | Medium | Closed-loop water, covered tank, periodic purge |
| Sludge and rejects | Wastewater and reject bin | High if stagnant | Frequent removal, sealed container, no indoor storage |
Odor Treatment Options
Three generic technologies cover the range of recycling plants, and the choice is a layout and budget decision rather than a brand decision. Activated carbon adsorption is the simplest, fits in a small footprint beside the pump room, and is suited to low-to-medium odor loads, but it needs regular media replacement. A biological scrubber handles high, continuous loads well and is low-cost to run, but needs a water treatment tie-in and more floor area. Thermal oxidation, sometimes described loosely as an RTO-style unit, gives the highest destruction efficiency for the most demanding post-consumer streams, at the cost of fuel input and a larger plant footprint. For most Kerke twin-screw recycling lines up to 1000 kg/h, activated carbon at the vacuum pump discharge plus good housekeeping at the silo is enough; above that, a biological or thermal stage should be considered at the design stage rather than added later.
| Technology | Footprint | Operating cost | Best for | Layout note |
|---|---|---|---|---|
| Activated carbon adsorption | Small, 4 to 10 sqm | Medium, media replacement | Low to medium odor, up to 1000 kg/h | Mount beside vacuum pump room, easy duct |
| Biological scrubber | Medium, 20 to 50 sqm | Low, water and power | Continuous high load | Needs water treatment tie-in and drainage |
| Thermal oxidation unit | Large, 40 to 90 sqm | High, fuel input | Worst post-consumer streams | Place at perimeter, allow combustion air and stack |
Melt Filtration Area Planning
Every contaminated feedstock carries solids that the washing line could not remove: paper fiber, fine sand, un-melted film, crosslinked gel, rubber, wood and the occasional metal sliver. The melt filter is the last barrier before the pellet, and its layout determines whether a screen change is a routine ten-minute event or a half-shift disruption with hot polymer on the floor. For upstream washing and dewatering, Wanplas supplies matched pre-treatment lines that feed directly into Kerke twin-screw systems, so the filtration duty described here is always the final stage at the extruder die.
Screen Changer Types
Three generic screen changer classes cover recycling duty. The hydraulic slide-plate changer is the workhorse: it holds a screen pack on a plate that a hydraulic ram slides out of the flow, and it suits batch change on moderately contaminated feedstock. The continuous belt filter carries an endless screen belt through the melt, indexing forward as the exposed section blinds, and it suits steady high contamination where stopping for a change is costly. The laser filter uses a rotating disc with a fine laser-cut gap to wipe contaminants into a waste chamber and reaches the finest filtration, at the highest capital and running cost. The layout difference is real: a hydraulic changer needs a clear slide stroke and a waste screen bin on the discharge side; a continuous or laser filter needs a waste collection bin and a service aisle for the drive, and the laser filter needs a small electrical enclosure and a chilled-water tie-in for the disc.
| Filter class | Change mode | Typical contamination handled | Floor space added | Layout implication |
|---|---|---|---|---|
| Hydraulic slide-plate changer | Manual or automatic batch | Level B to C | 2 to 4 sqm for bin and stroke | Clear slide stroke, waste bin on discharge side |
| Continuous belt filter | Automatic continuous | Level C to D | 4 to 8 sqm | Waste bin plus drive aisle, tie into control system |
| Laser filter | Automatic rotating disc | Level C to D, finest grade | 6 to 12 sqm | Electrical enclosure, chilled water, disc service aisle |
Mesh Selection by Feedstock
Mesh count is the number of screen openings per linear inch and it sets both the cleanness of the pellet and the pressure drop across the pack. Too coarse and gels and specks pass; too fine and the pack blinds quickly, pressure climbs and the vent ports surge. The right mesh is a function of the contamination level from the pre-treatment line, and the table below is the starting point used when laying out a Kerke recycling line. Note that these are filtration targets at the final melt filter, after Wanplas washing has removed the bulk of the grit.
| Feedstock level | Recommended final mesh | Pressure across pack (bar) | Change frequency guide | Notes |
|---|---|---|---|---|
| Level A, clean post-industrial | 100 to 150 | 60 to 100 | Low, long runs | Fine filtration affordable, low blind rate |
| Level B | 80 to 100 | 80 to 120 | Medium | Balance cleanness against blind rate |
| Level C post-consumer | 60 to 80 | 100 to 150 | Medium to high | Two-stage KTE plus SE relieves the pressure duty |
| Level D, heavily soiled | 40 to 60 | 120 to 180 | High, prefer continuous | Continuous or laser filter strongly advised |
Waste Screen Handling and Floor Space
The displaced screen pack and the purge that comes with it are hot, odorous and a slip hazard, so the area directly in front of the screen changer must be planned, not left as spare floor. Reserve a 1.0 m clear zone on the discharge side for the waste screen bin, keep that floor free of drainage trenches that catch hot polymer, and provide a quench bin or a steel tray rather than an open pit. On lines above 500 kg/h, a dedicated small trolley for spent screen packs removes them from the operator path. The crane that serves the barrel should also be able to lift a heavy filter body for service, so check the hook reach covers the die and filter cluster, not just the barrel sections.
Feeding System Layout
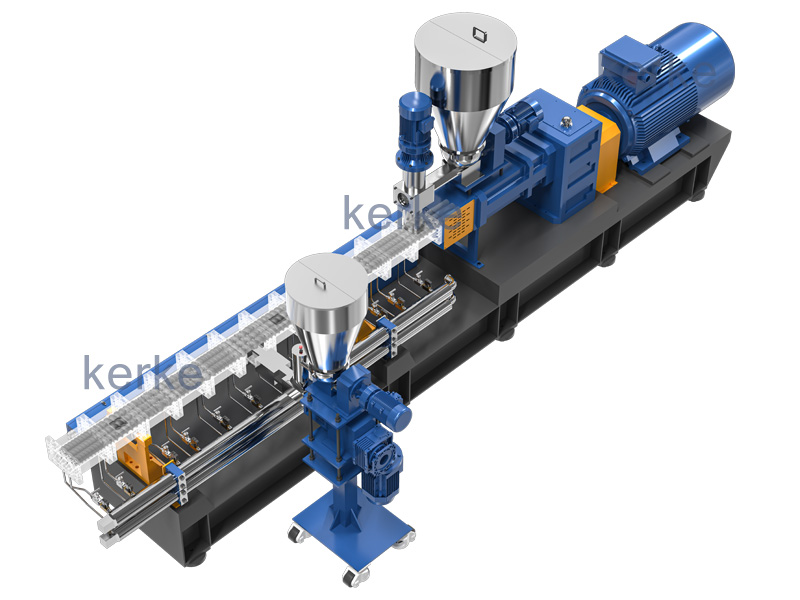
The feeder is where the dry, clean flake meets the twin-screw, and it is also where the building’s pre-treatment side and its extrusion side finally connect. Get the feeder layout wrong and you create bridging, surges and feed-throat fires; get it right and the extruder runs at steady screw speed with the vacuum vents doing their job. The feeding system for contaminated feedstock is rarely a single hopper: it is a platform, a main metering feeder, often a crammer or forced side feeder, and sometimes a second side feeder for filler.
Main Feeder Platform and Height
Because washed flake is light and fluffy, a loss-in-weight feeder mounted on a platform above the feed throat is the standard solution. The platform carries the feeder, the day bin that supplies it and the operator access, and it must be high enough that the feeder discharge drops naturally into the throat without an intermediate transfer that can bridging. A typical main feeder platform stands 2.2 to 3.0 m above the hall floor, with a stair and a guarded access gate, and the platform loading must account for a full day bin, the feeder and a maintenance load. Plan the platform as part of the extrusion hall steel structure, not as a free-standing rack, because vibration from the feeder and the screw will work a bolted rack loose over time.
| Feeder component | Role in recycling feed | Layout requirement | Typical space |
|---|---|---|---|
| Day bin | Holds 1 to 4 hours of flake above the feeder | Top of platform, filled by vacuum or screw conveyance | 1.5 to 3.0 m3 per line |
| Loss-in-weight feeder | Meters flake mass accurately into the throat | Vibration-isolated mount, load cell access beneath | 1.5 to 2.5 sqm footprint |
| Crammer feeder | Forces low-bulk-density flake into the screw | Directly above throat, vertical clearance for refill | 1.0 to 1.5 sqm |
| Side feeder for filler | Adds talc or CaCO3 downstream | Lateral mount on barrel, service aisle to one side | 1.5 to 2.0 sqm |
| Feed throat guard | Metal detection and foreign object protection | In the throat, below feeder discharge | Integrated, no extra floor |
Crammer, Forced Feed and Side Feed
A crammer feeder is a short single-screw device that stuffs flake into the throat and is essential for post-consumer film and fluffy flake that would otherwise bridge. In layout terms it sits directly above the throat and needs the same refill access as the main feeder. A side feeder for filler is mounted laterally on the barrel at a downstream port, and it needs its own small platform or a floor-standing frame with a service aisle on the open side; do not mount it where the screw pull-out aisle runs, because the side feeder occupies that wall. On Level D feedstock, a forced side feed of pre-compacted material into the first barrel zone is sometimes used to lift throughput, and that adds one more feeder footprint to the platform plan.
Conveying and Dust Control at the Feed
Moving flake from the dried buffer silo up to the day bin should be by a closed pneumatic or enclosed screw system, not by an open bucket elevator that dusts the clean hall. Closed conveying also keeps the flake dry, which matters because humid flake at the throat reduces devolatilization efficiency and loads the atmospheric vent. Place a dust collector on the conveying receive bin, sized for the conveying air volume, and route its fines back to the process or to a sealed reject container. The feed area is the single most common place for a feed-throat fire in recycling, so keep it free of loose film, provide a throat fire-suppression connection, and never store flake in open sacks on the platform.
Utilities and Infrastructure Sizing
Utilities are the part of the plant budget that surprises first-time recyclers, because the extruder is only a fraction of the connected load. The chiller, the vacuum pumps, the air compressor, the conveying blower and the wastewater treatment all draw power and all need space, cooling water and drainage. The method below reverses the output tier into a utility envelope so the electrical room, the cooling station and the compressor house can be sized before the architect draws the walls.
Installed Power and Transformer Sizing
Start from the installed motor power of the line and the auxiliaries, then apply a demand factor because not every motor runs at full load at once. A realistic demand factor for a recycling line with conveying, drying and water treatment is 0.55 to 0.65, and the transformer should then carry a 25 to 30 percent spare margin for future lines and motor starting currents. The result is a transformer kilovolt-ampere requirement that is far below the sum of nameplate powers but comfortably above the actual running load. For a 1000 kg/h line built around a KTE-95D, the connected load is roughly 320 to 360 kW; after the demand factor and margin, a 400 to 500 kVA transformer is the correct specification, not the 400-plus kW that naive summation would suggest.
| Output tier | Connected load (kW) | Demand factor applied | Transformer (kVA) | Cooling water (m3/h) | Compressed air (Nm3/min) | Wastewater area (sqm) |
|---|---|---|---|---|---|---|
| 300 kg/h | 120 to 160 | 0.60 | 150 to 200 | 8 to 12 | 1.0 to 1.5 | 80 to 150 |
| 500 kg/h | 200 to 260 | 0.60 | 250 to 320 | 14 to 20 | 1.5 to 2.5 | 120 to 220 |
| 1000 kg/h | 320 to 380 | 0.62 | 400 to 500 | 25 to 35 | 2.5 to 4.0 | 180 to 320 |
| 2000 kg/h | 560 to 680 | 0.65 | 700 to 900 | 45 to 65 | 4.0 to 6.5 | 320 to 550 |
Cooling Water Station
The barrel cooling circuit, the vacuum condensers and the pelletizer water loop all draw cooling capacity, and in most climates a closed cooling tower with a plate heat exchanger is the efficient choice. Size the station for the peak simultaneous demand from the table above, add a 15 percent margin, and place it outdoors on the perimeter with the tower on the upwind side of the odor treatment so the two never fight. The chiller or tower base, the pump skid and the buffer tank together need 15 to 40 sqm of outdoor or semi-enclosed space depending on tier, plus a drain to the wastewater system for bleed-off. Inside the hall, run the cooling supply and return in a trench or an overhead tray, never as loose hoses across the floor.
Compressed Air and Conveying
Compressed air serves instrument control, the crammer and forced feeders, the pneumatic flake conveying and the pelletizer air knife. The volumes in the table assume oil-free air for the conveying and the air knife, because oil mist in recycled flake or on the pellet surface is a quality defect. Place the compressor in the utilities room or a dedicated house, with the receiver outside the clean zone, and run a separate clean-air ring for instruments apart from the conveying ring. A receiver sized for 10 to 15 minutes of demand smooths the load and lets a single compressor serve more than one line if staged correctly.
Wastewater and Sludge
Even a Level C plant with a Wanplas washing line generates wash water carrying grit, organics and fines, and that water must be treated on site in nearly every jurisdiction. The outdoor area in the table covers the balancing tank, the treatment units, the sludge press and the control cabin, but not the building footprint. Keep the wastewater plant downwind and downstream of the clean zone, give it its own access for sludge trucks, and connect the hall floor drains, the barrel vent trench and the pelletizer water loop to it through a sealed collection network. A common layout mistake is to route clean-zone floor drains into the same network as dirty-zone wash drains; separate them so a clean-zone spill does not overload the treatment train.
Fire Safety and Plant Layout
Plastic recycling carries two distinct fire risks that a general factory layout ignores at its peril: a slow-smoldering bale fire in storage, and a fast flash fire at the feed throat from trapped volatiles or metal. Both are layout-controllable, and both are cheaper to design out than to insure around. The notes below are layout guidance, not a substitute for the local fire code, but they are the items most often missing from a first recycling plant layout.
Fire Load by Storage Zone
Baled film and flake store enormous energy per square meter, and the yard and the pre-treatment zone carry the highest fire load in the plant. The finished goods warehouse, while also plastic, is a denser, lower-surface-area product and a lower continuous load if pellets are stored in big bags rather than loose. The table gives the relative fire load so the setback and compartment rules can be applied where they matter most.
| Zone | Relative fire load | Dominant hazard | Layout control |
|---|---|---|---|
| Raw material yard | Very high | Smoldering bale fire, hard to detect | Open spacing, thermal detection, separate from buildings |
| Pre-treatment and drying | High | Hot equipment plus loose flake | Fire-rated partitions, temperature interlocks |
| Extrusion hall | Medium | Feed-throat flash, hot polymer | Throat suppression, clear evacuation, no clutter |
| Finished goods warehouse | Medium | Dense pile, slow burn if ignited | Big-bag stacking, separation from dispatch |
| Utilities room | Low to medium | Electrical and thermal | Dedicated room, fire-rated, ventilation |
Fire Compartments and Separation
Divide the building into fire compartments so a fire in the dirty zone cannot reach the clean zone through an open transfer. The dirty zone and the clean zone should be separated by a fire-rated wall with the material pass through an automatic fire shutter or an airlock, never a permanent open window. The raw material yard should sit a defined setback from the building, with a fire access road on at least two sides, and the wastewater plant should be separated from both the yard and the clean zone. Keep the extrusion hall evacuation path clear of the screw pull-out aisle clutter, because in an emergency that aisle is also the exit route.
Dust Explosion Risk Areas
Fine plastic dust from conveying, screening and grinding forms an explosible atmosphere in the right concentration, and the enclosed spaces most at risk are the conveying receive bins, the grinding and milling area, and the sieve house. Layout controls are straightforward: keep these areas separated from ignition sources, provide explosion relief venting to a safe external face, ground all equipment, and avoid dead pockets where dust settles. The extrusion hall itself is low risk because the polymer is molten, not airborne as dust, but the feeder platform and the sieve house are not, and they should be treated as classified areas in the electrical design.
Detection and Suppression Placement
Put thermal detection in the yard bales and in the pre-treatment equipment, smoke and heat detection in the clean zone and the control room, and a dedicated feed-throat suppression connection at every extruder throat. The vacuum pump room and the compressor house get their own detection because they concentrate heat and vapor. Suppression water supplies and manual call points should be reachable without crossing a compartment boundary, and the fire main should loop the building so a single valve closure does not disable a whole face.
Noise, Dust and Ventilation Hierarchy
The last layout discipline is environmental comfort, and it is also a productivity discipline, because a plant that exceeds noise limits or dust limits loses operators and fails audits. The hierarchy is the same in every recycling plant: contain the source, capture at the source, then ventilate the space. Doing it in that order is cheap; doing it backwards by burying the problem in building air changes is expensive and ineffective.
Local Dust Extraction Estimates
Dust is generated at the grinding equipment, the sieve, the conveying receive points and the bagging station, and each needs a capture hood sized to the air volume it emits. Undersized hoods simply move dust from one place to another. The table below gives the order of magnitude of extraction airflow per source so the dust collector and ductwork can be planned before the roof is drawn.
| Dust source | Canopy or hood type | Extraction airflow (m3/h) | Layout note |
|---|---|---|---|
| Wet crusher and friction washer | Enclosure with local pull | 3000 to 6000 | Part of pre-treatment enclosure, not separate |
| Vibrating sieve | Sealed hood with side draw | 1500 to 3000 | Place sieve in its own small vented room |
| Conveying receive bin | Filter vent on bin | 1000 to 2500 | Return fines to process, no open discharge |
| Bagging station | Downdraft table or booth | 2000 to 4000 | Keep in clean zone, filtered make-up air |
| Feed throat | Local extraction at throat | 800 to 1500 | Tie into throat suppression interlock |
Noise Enclosures and Buffer Zones
The crusher and the pelletizer are the loudest items, and both respond to enclosure better than to remoteness, because doubling the distance only lowers the level by a few decibels while a 30 mm acoustic enclosure can cut 15 to 20 dBA at the source. Enclose the crusher in the dirty zone as part of its housing, enclose the pelletizer in the clean zone with a removable panel for strand access, and place the air compressor and vacuum pumps in their own rooms so their noise does not add to the hall. Between the noisy dirty zone and the control room, use a buffer of storage or corridor rather than a shared thin wall, and keep the operator in the positive-pressure control room for the bulk of the shift.
Ventilation Hierarchy in Practice
Apply the pressure gradient from the zoning section here as the ventilation backbone: extract more than you supply in the dirty zone, supply filtered air to the clean zone, and let the transition zone sit between. Size the system from the air change rates already given, then add the local extraction volumes from the dust table on top, because local extraction is additional to room ventilation, not a substitute for it. Filtered make-up air to the clean zone should be at least EU class medium efficiency so the pellet surface stays clean, and the dirty-zone exhaust should pass the odor treatment described earlier before it leaves the building. A plant laid out this way meets ventilation targets with a smaller total air volume than one that tries to dilute its way out of a containment failure.
Requirement to Model and Layout Recommendation
The table below converts four common customer scenarios into a concrete Kerke machine selection plus the building area and key configuration items that go with it. It is the bridge between the area calculation method and an actual purchase order, and it is the fastest way to sanity-check a plan before detailed engineering starts.
| Customer scenario | Feedstock level | Recommended Kerke configuration | Suggested building area | Extrusion hall clear height | Key configuration items |
|---|---|---|---|---|---|
| 500 kg/h post-industrial film compounding | Level B | KTE-65D at 44 to 48 L/D, single-stage with strand pelletizing | About 1050 sqm total (1380 baseline × 0.75) | 6.5 m | Crammer feeder, one atmospheric vent plus one vacuum vent, hydraulic plate screen changer at 80 to 100 mesh, 3 t crane |
| 1000 kg/h post-consumer PP into filled injection grade | Level C | KTE-95D at 48 L/D, single-stage with water-ring die-face cutting | About 2400 sqm total plus 250 sqm outdoor water treatment | 7.5 m | Loss-in-weight main feeder, side feeder for talc, two vacuum vents with vent stuffers, continuous belt filter at 80 mesh, 5 t crane |
| 2000 kg/h agricultural film, heavily soiled | Level D | KTE-135D at 48 L/D in a two-stage arrangement with an SE-180 second stage | About 5765 sqm total plus 400 sqm outdoor water treatment | 9.0 m | Crammer plus forced feeding, two vacuum vents, rotating disc or continuous filter at 40 to 60 mesh, dedicated vacuum pump room, 10 t crane |
| Small-batch multi-grade recycled compounding and development | Level A to Level C samples | KTE-36B or KTE-52D production unit plus a KTE-20B laboratory extruder | About 700 to 900 sqm including a 60 sqm laboratory | 6.0 m | Quick-change screw elements, strand pelletizing for fast changeover, two additive feeders, small homogenizing silo bank for lot blending |
| Second-stage pelletizing only, low-specification recycled grade | Level A to Level B | SE-150 or SE-180 single-screw with a hydraulic screen changer | About 500 to 700 sqm | 6.0 m | Force feeder, single atmospheric vent, 60 to 80 mesh screens, compact water bath and cutter cluster |
Read the table as a starting point rather than a fixed prescription. Two variables move the recommendation quickly: the moisture level entering the extruder, which decides whether one vacuum vent is enough or two are needed, and the changeover frequency, which decides whether strand pelletizing with its easier cleaning is preferable to die-face cutting with its higher throughput. Kerke engineers normally ask for a feedstock sample description, a target product specification and a shift pattern before finalizing any of these choices.
Three Common Layout Templates
Most contaminated plastic extrusion plants resolve into one of three plan geometries. Choosing between them is mainly a question of plot shape, land cost and expansion ambition, and each has a predictable set of strengths and weaknesses.
I-Shape: The Straight-Line Plant
In an I-shape, material enters at one end and leaves at the other in a single straight line: yard, pre-treatment, transition, extrusion, pelletizing, warehouse, dispatch. It gives the shortest total material path, the simplest conveying and the cleanest separation between dirty and clean ends, because they are physically at opposite ends of the building. It also expands most easily, since a second line can be added as a parallel bay or the building can be extended at the clean end. The drawback is that it needs a long, narrow plot with the right orientation, and a long building costs more per square meter in structure, roof drainage and utility distribution than a compact one.
L-Shape: The Practical Compromise
The L-shape turns the flow through 90 degrees, typically at the transition zone. It fits irregular and corner plots, keeps the two arms functionally distinct, and allows the dirty arm to face the yard while the clean arm faces the dispatch road. The turn point does add a transfer, usually a bucket elevator or an inclined belt, and any transfer generates fines and creates a potential blockage. Place the turn in the transition zone rather than in the middle of the wet chain, where sticky, wet material makes transfers unreliable.
U-Shape: The Land-Efficient Layout
A U-shape brings the finished goods back alongside the receiving area, so that one dock face serves both. It has the smallest land requirement of the three and the shortest internal logistics for the forklift fleet, which is why it appeals in high land-cost locations. The risk is obvious: receiving and dispatch are close together, so contamination control and traffic scheduling become procedural rather than physical. If a U-shape is chosen, insist on a full-height partition between the two docks, separate forklift fleets, and timed slots for inbound and outbound trucks.
| Criterion | I-shape | L-shape | U-shape |
|---|---|---|---|
| Land use efficiency | Low to medium | Medium | High |
| Internal material path length | Shortest | Medium | Medium |
| Dirty and clean separation | Excellent, by distance | Good, by geometry | Requires strict procedural control |
| Number of material transfers | Fewest | One extra transfer at the corner | One or two extra transfers |
| Expansion flexibility | Highest, extend or add a parallel bay | Medium, extend one arm only | Lowest, the loop is closed |
| Structural cost per square meter | Higher, long span and long services | Medium | Lower, compact envelope |
| Suitable total area range | 1500 to 8000 sqm | 800 to 5000 sqm | 800 to 3000 sqm |
| Best fit | Greenfield sites with generous, well-oriented plots | Corner plots and staged construction | High land cost, single-grade production, disciplined operations |
Expansion Planning
Expansion planning is the difference between a plant that doubles output in six weeks and one that has to be rebuilt. The core principle is to spend a small amount of area and utility capacity now to keep future options open, because the marginal cost of reserving space at design stage is a fraction of the cost of creating it later.
Reserve the Second Line Position
Draw the second extrusion line on the first-phase general arrangement, even if it will not be ordered for three years. Reserve its floor area, its feeder platform base, its crane coverage and its aisle. In practice this means designing the extrusion hall with two bays from the beginning and using the second bay as a maintenance and staging area until it is needed. The recovered area is not wasted, and when the second line arrives, installation does not require moving the first one.
Size Utilities at 1.5 Times First-Phase Demand
Transformers, main cable routes, cooling water headers, compressed air ring mains and wastewater treatment capacity should be sized for approximately 1.5 times the first-phase requirement. The incremental cost at construction is modest because the expensive part is the civil work and the routing, not the capacity itself. Specifically, run the main cable duct bank and the cooling water header along the full length of the hall with capped branches at the future line position, and specify a transformer one standard size above the calculated need. A 1000 kg/h plant that installs an 800 kVA transformer today and reserves the pad and switchgear space for a second 800 kVA unit can double output without a utility upgrade negotiation.
Crane Rail and Structural Provisions
Extend the crane rail the full length of the planned building, including the reserved bay, at initial construction. Retrofitting a crane rail into an operating hall means shutting production down, working at height above installed equipment and often reinforcing columns that were never designed for the extra load. Similarly, design column foundations for the eventual crane capacity rather than the first-phase capacity, and leave floor slab thickened areas at the reserved machine positions so that a heavier extruder can be installed later without breaking out and recasting the slab.
Silo and Warehouse Growth
Homogenizing silo capacity and finished goods area both need to grow with output, and both are easy to under-reserve. Plan the silo bank on an outdoor pad adjacent to the bagging station, with foundations and pipe routing for two additional silos. For the warehouse, reserve a clear expansion face on one side of the building where a bay can be added without relocating the dispatch dock, and avoid placing permanent utility equipment against that face.
Service and Support
Layout planning and equipment supply are only useful if the plant can be commissioned and kept running. Kerke, as a Wanplas factory, operates on a service model built around the realities of exporting compounding lines to more than 70 countries, and several elements of that model directly affect how a plant should be laid out.
Testing Before Shipment
Every machine is assembled and tested at the Kerke factory before shipment, and customers are welcome to attend. For a contaminated feedstock project, the most valuable version of this test is a run with the customer’s own washed material rather than with virgin resin. Sending 300 to 500 kg of representative washed flake ahead of the factory test allows the screw configuration, the vent arrangement and the screen specification to be verified against the real feedstock, and it frequently changes one or two configuration decisions before the machine ever leaves China. It also produces real melt pressure and torque data that can be used to finalize the electrical load list and the utility sizing in the layout.
Installation, Commissioning and Training
Kerke engineers travel to site for installation and commissioning. The layout affects how quickly that goes: a plant that has already poured the correct foundations, run the cooling water and compressed air to the machine positions, installed the crane and left the screw pull-out aisle clear can be mechanically installed in a few days. A plant that has to improvise access loses weeks. Operator and maintenance training is delivered during commissioning and covers screw element handling, screen changing, vent port cleaning, torque and pressure interpretation, and the recipe management functions of the control system.
Spare Parts and Ongoing Support
The Wanplas group service commitments apply across all its factories, including Kerke. These cover USD 500 free parts/year, free replacement of parts that fail within the warranty period, a transportation guarantee, a production capacity guarantee and a quality standards commitment. For a recycling plant, the practical priority list for on-site spares is screw elements in the highest-wear positions, a spare screen changer seal set, heater bands, thermocouples and a spare vent stuffer paddle. Reserve a lockable spare parts store of 15 to 30 sqm inside the clean zone, with racking for screw elements laid out in order so that a rebuild can be staged before the machine is opened.
Remote Support and Factory Visits
Remote diagnostic support through the control system allows Kerke engineers to review trends in torque, melt pressure, vent vacuum and feed rate, which shortens troubleshooting on issues that would otherwise require a site visit. Kerke also maintains an open factory policy: customers are welcome to visit the 19,997 sqm manufacturing base, see machines under assembly and run trials in the test area. For layout projects specifically, Wanplas can supply English-language workshop layout drawings and equipment foundation drawings, so that the civil contractor receives dimensioned anchor bolt patterns, load points, service entry positions and drainage requirements rather than a generic outline.
Frequently Asked Questions
How much factory area do I need for a 1000 kg/h contaminated waste plastic twin-screw extrusion plant?
For Level C post-consumer feedstock at 1000 kg/h, plan on roughly 2400 sqm of total covered and paved footprint: about 450 sqm of raw material yard, 500 sqm of pre-treatment, 240 sqm of drying and buffer, 480 sqm of extrusion hall, 200 sqm of pelletizing and screening, 380 sqm of finished goods warehouse and 150 sqm of utilities. Multiply by 1.35 for heavily soiled agricultural film and by 0.55 for clean industrial scrap, then add outdoor wastewater treatment, office and laboratory space, and a truck apron.
What clear height should a contaminated plastic twin-screw extrusion hall have?
A 300 to 500 kg/h hall works at 6.0 to 6.5 m clear height under the crane hook, a 1000 kg/h hall needs about 7.5 m, and a 2000 kg/h hall with buffer silos and a two-stage vent stack needs 9.0 m or more. Clear height is driven by the feeder platform stack-up, the silo column and the crane hoist travel, not by the extruder itself. Under-specifying height is the layout mistake that cannot be corrected at any reasonable cost.
How much straight space must I leave to pull the screws out of a twin-screw extruder?
Reserve at least 1.2 times the working screw length as clear straight space in front of the barrel, where working screw length equals screw diameter multiplied by the L/D ratio. A KTE-135D at 44 L/D has a working screw length of about 5.94 m, so 8 to 10 m of unobstructed aisle should be reserved. This aisle can double as the main hall walkway, but nothing permanent may be installed in it.
Can I put the crusher and the extruder in the same open hall to save area?
It is possible for clean Level A industrial scrap with a dry, low-dust feedstock, and it is a poor decision for anything dirtier. Crushing contaminated material releases polymer fines, soil dust and label fiber that foul heaters, electrical enclosures and open feed hoppers, degrade pellet quality and create a combustible dust exposure near hot surfaces. The partition wall between crushing and extrusion typically pays for itself within the first year through reduced heater and drive failures alone.
How large should the buffer silo between drying and the extruder be?
Size the buffer for 60 to 120 minutes of extruder consumption. At 1000 kg/h and a bulk density of 0.30 to 0.35 t/m3 for washed film flakes, that is roughly 3 to 6 m3 of usable volume. The buffer decouples semi-batch washing and drying from continuous extrusion and is the cheapest single intervention available for raising plant utilization, but it needs floor space and vertical clearance that must be reserved during design.
What transformer capacity should I plan for a contaminated plastic compounding plant?
Build a nameplate load list, apply a demand factor of 0.55 to 0.65, then add 25 to 30 percent headroom for expansion. On that basis a 300 kg/h plant with about 220 kW installed uses a 315 kVA transformer, a 1000 kg/h plant with about 650 kW installed uses 800 kVA, and a 2000 kg/h plant with about 1150 kW installed uses 1600 kVA. Barrel heating inflates the connected load but runs at only 20 to 35 percent duty in steady state, which is why the demand factor is well below 1.
Where should the vacuum pump room be placed?
Place it adjacent to the extrusion hall, within 8 to 12 m of pipe run from the vent ports, in a separately ventilated enclosure with a floor drain routed to process wastewater and a sealed collection pit for pump service water. Long vacuum lines lose capacity through pressure drop and trap condensate that can slug back toward the barrel, while an in-hall installation spreads noise, heat and odor across the entire workshop.
Which layout template should I choose for a 2000 sqm plot?
At 2000 sqm, an L-shape is usually the best compromise, because it fits an ordinary rectangular or corner plot while keeping the dirty and clean arms functionally distinct. A U-shape uses the land most efficiently but forces receiving and dispatch close together, which demands strict traffic and contamination procedures. Reserve an I-shape for larger, well-oriented greenfield plots where expansion by adding parallel bays is part of the plan from the beginning.
Conclusion
A factory area layout for contaminated waste plastic twin screw extrusion is a technical calculation, not an architectural preference. Start from the rated output, apply the zone coefficients, scale by the contamination level of the feedstock you actually intend to run, and only then draw walls. A 1000 kg/h Level C plant needs about 2400 sqm of process footprint, 7.5 m of clear height in the extrusion hall, an 800 kVA transformer, 70 m3/h of cooling water circulation and a screw pull-out aisle that nobody is allowed to block. Those numbers are derivable on day one, and every one of them is expensive to change on day one thousand.
The layout principles that matter most are consistent across plant sizes and across feedstocks. Separate dirty, transition and clean zones with real walls and a real pressure gradient. Give material a one-way path and give forklifts a loop rather than a shuttle. Put a buffer silo between semi-batch pre-treatment and continuous extrusion. Keep the dryer, because trying to remove 6 percent moisture in the vent section costs far more output than the dryer costs in floor area. Reserve the screw pull-out aisle, the crane coverage and the vacuum pump room. Size utilities at 1.5 times first-phase demand and draw the second line before the first one is ordered. Plants that follow these rules reach rated output in months; plants that skip them spend years discovering why they cannot.
On the equipment side, the Kerke KTE series of parallel co-rotating twin-screw extruders covers the full range from the KTE-16B laboratory unit to the KTE-135D production machine, with configurable aspect ratio, barrel structure, screw arrangement, vent configuration, feeding system and control, which is exactly the flexibility that contaminated feedstock demands. The SE series single-screw extruders from 30 kg/h to 800 kg/h complete the picture as second-stage pressure builders or standalone pelletizing units for lower-specification recycled grades. Behind both sits the Wanplas group service framework: factory testing before shipment, on-site installation and commissioning, operator training, remote diagnostic support, USD 500 free parts/year and an open factory policy for customers who want to see the machines being built.
If you are planning a contaminated plastic recycling and compounding workshop in 2026, send Kerke your feedstock description, target output, product specification and plot dimensions. The engineering team will return a recommended machine configuration, a dimensioned workshop layout, an equipment foundation drawing and a utility list you can hand directly to your civil and electrical contractors. Bring a sample of your washed material and run it on a production machine at the factory before you commit to a configuration. You are welcome to visit the factory, watch the trial and take the resulting data home as the basis for your building design.