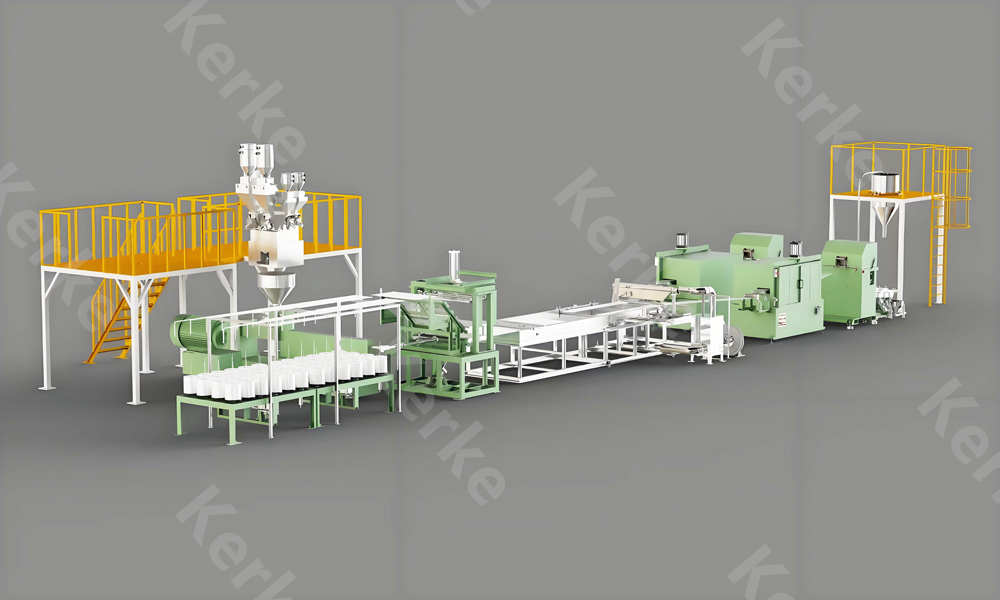
Recycled plastic compound pelletizing on a co-rotating twin-screw extruder is a margin business, not a volume business. The machine can run for years, yet the difference between a profitable line and a struggling one is decided by a handful of numbers that fit on a single sheet: feedstock cost, energy per ton, wear-part life, yield, and the price grade the final pellet can command. This article builds a complete per-ton net profit model for a recycled compound pellet operation, expressed entirely in index points so the logic stays valid regardless of the local currency, resin price, or plant location. Kerke, a Wanplas factory with more than 12 years of twin-screw compounding experience and over 2,000 machines running in 70-plus countries, uses exactly this kind of model when helping compounders size and configure a line. By the end you will be able to construct your own profit cascade, run a sensitivity matrix, and see precisely how screw configuration, vacuum venting, gravimetric feeding, and melt-pressure stabilization transmit into the bottom line.
The Per-Ton Net Profit Model for Recycled Compound Pelletizing
A net profit calculation is only useful when every cost line is normalized to the same denominator. For a recycled compound pellet line the cleanest denominator is the selling price of one metric ton of good pellet, set equal to 100 index points. Every revenue and cost line is then written as a share of that 100, which means the final net profit figure is itself an index that can be compared between a PCR general-grade plant in one region and a glass-fiber engineering-grade plant in another. The model follows a standard cascade: Revenue becomes Variable Cost, then Contribution Margin, then Fixed Cost, then EBITDA, then Depreciation, then EBIT, and finally Net Profit after tax.
The cascade is intentionally transparent so that an operator can isolate which lever moves the result. Contribution Margin is the first verdict: it tells you whether the plant survives its own variable cost. EBITDA tells you whether the operation covers cash fixed cost. EBIT tells you the pre-tax operating result after depreciation. Net Profit is what the owner actually keeps. In the index-point convention the net profit number is also the net margin percentage, because revenue is normalized to 100.
Base case cascade for an automotive-grade recycled PP/PE compound
The table below presents a representative base case: a mid-grade recycled polypropylene and polyethylene compound pellet sold into automotive interior applications, running at roughly 80 percent capacity utilization with a 93 percent good-yield. The selling price is the 100-point reference. Feedstock is set at 54 index points, which sits inside the 52 to 62 index-point band that recycled streams typically occupy. Additives, energy, labor, wear parts, packaging, logistics, and waste loss complete the variable side. Fixed cash cost and depreciation complete the fixed side. An effective tax rate near 25 percent is applied to reach net profit.
| P&L line (per ton) | Index points | % of revenue | Comment |
|---|---|---|---|
| Revenue (selling price) | 100.0 | 100.0% | Reference price per ton = 100 index points |
| Feedstock (yield-adjusted) | 54.0 | 54.0% | Sorted PP/PE hard scrap, 93% yield |
| Additives & modifiers | 5.0 | 5.0% | Antioxidant, compatibilizer, filler |
| Energy | 5.0 | 5.0% | Specific energy consumption based |
| Labor | 3.0 | 3.0% | Man-hour per ton based |
| Wear parts | 3.0 | 3.0% | Screw, barrel, screen, cutter |
| Packaging & inland logistics | 3.0 | 3.0% | Bags, labels, local freight |
| Waste & start-up loss | 3.0 | 3.0% | Off-spec, screen dump, purge |
| Variable cost total | 76.0 | 76.0% | All volume-driven cost |
| Contribution margin | 24.0 | 24.0% | Revenue minus variable cost |
| Fixed cash cost | 7.0 | 7.0% | Mgmt, sales, cert, finance, env |
| EBITDA | 17.0 | 17.0% | Contribution minus cash fixed |
| Depreciation | 3.0 | 3.0% | 8 to 10 year straight line |
| EBIT | 14.0 | 14.0% | Pre-tax operating result |
| Tax (effective ~25%) | 3.5 | 3.5% | Jurisdiction dependent |
| Net profit | 10.5 | 10.5% | Net margin index points |
In this base case the line keeps 10.5 index points of net profit, which means a 10.5 percent net margin on every ton sold. That figure sits inside the 9 to 16 index-point band that well-run recycled compound plants realistically achieve. The band is wide because the same machine can be pointed at a thin-margin PCR general grade or a thick-margin engineering modified grade, and because process discipline changes the variable side by several points. Everything that follows explains how to move within and beyond that band on purpose rather than by luck.
Revenue Side Variables: The Grade Pricing Ladder
Revenue is not a single number. A recycled compound pellet is priced by grade, and the grade ladder is the single biggest revenue lever on the line. The model recognizes four main grade tiers: PCR general grade, automotive grade, food-contact grade, and engineering modified grade. Each tier commands a different price index relative to the base, and each tier carries different cost and certification requirements. Understanding the ladder is the first step to choosing which grade to target, because chasing a premium grade only pays off if the line can actually meet its consistency and certification bar.
Price index gradient by grade
The table below shows the relative price level of each grade expressed as a multiplier of the PCR general base price. A food-contact grade sells at roughly 1.16 times the PCR base, while an engineering glass-fiber modified grade reaches about 1.30 times. These are relative price levels, not currency amounts. The reason the premium exists is traceability, consistency, and a performance envelope the buyer can certify.
| Grade tier | Relative price index | Color & odor tolerance | MFR consistency | Key certification | Net margin band (idx) |
|---|---|---|---|---|---|
| PCR general grade | 1.00x (base) | Wide | MFR ±10% | Basic QC | 9.0 |
| Automotive grade | 1.08x | Medium | MFR ±6% | ISO 9001, GRS | 10.5 |
| Food-contact grade | 1.16x | Tight | MFR ±4% | EU 10/2011, FDA 21 CFR 177 | 12.5 |
| Engineering modified grade | 1.30x | Tight, filled | MFR ±3% | ISO 9001, GRS, performance spec | 15.5 |
Color and odor are quiet profit killers. A pellet that looks grey or carries a detectable smell is downgraded one or two tiers even if its mechanical properties are fine, because the converter cannot risk it in a visible or closed application. Vacuum venting quality, which is covered later, is what keeps the odor grade high. Melt flow rate consistency is the other silent lever: a buyer who specifies MFR at a tight tolerance will pay the premium only if the supplier can hold it. A line that drifts at ±10 percent is locked into the PCR general band; a line that holds ±3 percent can quote the engineering band. The certification row is the gatekeeper, and maintaining those certifications is a fixed cost that the higher grades must absorb.
How certification lifts the achievable price index
Certifications do not change the pellet, but they change what the buyer is allowed to do with it. A GRS recycled-content claim lets a brand report recycled content in its sustainability accounting. An ISO 9001 quality system lets an automotive tier supplier qualify the material. Food-contact compliance such as EU 10/2011 or FDA 21 CFR 177 opens the packaging and consumer-goods channel. Each certification adds a maintenance cost on the fixed side, but the price index it unlocks more than offsets that cost when volume is sufficient. The net margin band in the table already includes a representative certification maintenance load, which is why food-contact and engineering grades show higher net margin despite higher cost.
Variable Cost Breakdown by Cost Center
Variable cost is where most of the profit fight is won or lost, because it scales with every ton produced. The model splits variable cost into seven centers: feedstock, additives and modifiers, energy, labor, wear parts, packaging and inland logistics, and waste plus start-up loss. Each center is expressed both in index points and in physical units so the operator can connect the number to a meter on the factory floor. Kilowatt-hour per ton, kilogram per ton, and man-hour per ton are the units that make the index points auditable.
Feedstock by material family
Feedstock is the heaviest line and the most volatile. The table below maps the main recycled resin families to their typical feedstock index and their processing yield, which is the ratio of good pellet output to clean flake or regrind input. Yield matters because the feedstock index is already yield-adjusted: it shows cost per ton of good output, not per ton of input. PET and ABS or PC streams cost more per ton of input but also often sell into higher grades, while PP and PE hard scrap is cheaper and sits at the low end of the 52 to 62 index-point band.
| Material family | Feedstock index (pts) | Processing yield | Typical volatiles | Abrasion level |
|---|---|---|---|---|
| PP / PE hard scrap | 52 to 56 | 92 to 96% | Low | Low |
| PET bottle flakes | 55 to 60 | 88 to 93% | Medium (moisture, acetaldehyde) | Medium |
| ABS / PC stream | 58 to 62 | 85 to 91% | Medium to high | Medium |
| PA engineering stream | 58 to 62 | 86 to 92% | High (hygroscopy) | Medium |
Additives and modifiers
The additive line looks small in index points but is the most controllable. A recycled compound typically carries a hindered-phenol plus phosphite antioxidant blend at 0.1 to 0.3 percent to survive the heat history of reprocessing. A compatibilizer such as PP-g-MAH at 2 to 5 percent is used when polyolefin and polar fractions must bond. PET grades use a chain extender at 0.3 to 0.8 percent to recover molecular weight lost during previous melt cycles. Color masterbatch or pigment, calcium carbonate filler, glass fiber at 10 to 30 percent, and a POE toughener at 5 to 15 percent are the modifiers that define the grade. Each percentage point of additive is a direct cost, so the dispersion quality of the screw determines how little additive you can get away with and still meet spec.
| Additive / modifier | Dosage range | Index points (approx) | Purpose |
|---|---|---|---|
| Antioxidant blend | 0.1 to 0.3% | 0.5 to 1.5 | Thermal stability on re-extrusion |
| Compatibilizer (PP-g-MAH) | 2 to 5% | 2 to 4 | Phase bonding of mixed streams |
| Chain extender (PET) | 0.3 to 0.8% | 1 to 2 | IV recovery for PET |
| CaCO3 filler | 5 to 30% | 1 to 4 | Cost dilution, stiffness |
| Glass fiber (GF) | 10 to 30% | 4 to 9 | Strength, stiffness, wear up |
| POE toughener | 5 to 15% | 2 to 5 | Impact improvement |
Energy, labor, and wear parts in physical units
Energy is expressed through specific energy consumption, the kilowatt-hour per kilogram of pellet. A co-rotating twin-screw pelletizing line typically runs at 0.18 to 0.35 kWh/kg depending on material and screw load. Drying and crystallizing of PET or PA add a separate energy step before the extruder. Water circulation and compressed air are small but continuous loads. Labor is expressed as man-hour per ton and falls sharply with automation: a semi-automatic line may need 0.08 to 0.15 man-hour per ton, while a fully automated line with automatic bagging and central control needs 0.03 to 0.06 man-hour per ton. Wear parts are the stealth cost on abrasive streams: screw elements and barrel liners last 8000 to 20000 hours on clean polyolefin but collapse to 3000 to 6000 hours when glass fiber is present, and screen packs, cutter blades, and die plates wear in proportion.
| Cost center | Physical unit | Typical range | Index points |
|---|---|---|---|
| Energy (extrusion) | kWh/kg | 0.18 to 0.35 | 4 to 7 |
| Energy (dry / crystallize) | kWh/kg | 0.05 to 0.15 | 1 to 3 |
| Labor (semi-auto) | man-hour/ton | 0.08 to 0.15 | 3 to 5 |
| Labor (full auto) | man-hour/ton | 0.03 to 0.06 | 1.5 to 3 |
| Wear (clean polyolefin) | hours | 8000 to 20000 | 2 to 4 |
| Wear (glass-filled) | hours | 3000 to 6000 | 4 to 7 |
| Packaging & logistics | kg/ton | fixed | 3 |
| Waste & start-up loss | % of input | 2 to 5% | 2 to 4 |
The packaging and inland logistics line is often forgotten in a profit model but is real: bags, inner liners, pallets, labels, and the local freight to the converter or port all add up to a steady 2 to 4 index points. Waste and start-up loss covers material lost during screen pack dumps, purge blocks, and off-spec transition runs between grades. On a line that changes grade frequently, this line can creep toward 5 index points, which is why quick changeover and a clean screw design that needs little purge material protect margin directly.
Fixed Cost Structure and Depreciation
Fixed cost does not scale with volume, which means its per-ton impact shrinks as utilization rises. This is the second most important profit lever after feedstock, because a line running at 90 percent utilization carries roughly half the fixed cost per ton of a line running at 60 percent. The fixed side has five centers: depreciation of the plant and equipment, management and sales, certification maintenance, finance, and environmental and emission control.
Depreciation and the fixed cost table
Equipment depreciation is modeled on an 8 to 10 year straight-line basis, which is the common accounting life for a twin-screw compounding line treated as a production asset. The building and auxiliary systems are depreciated on a similar or longer schedule. Management and sales cover administration, commercial staff, and marketing. Certification maintenance covers the recurring audit and documentation cost of ISO 9001, GRS, and food-contact dossiers. Finance covers interest on borrowed capital and working capital tied up in feedstock inventory. Environmental and emission control covers dust collection, odor treatment, wastewater, and permit compliance.
| Fixed center | Index points (at 80% util) | Nature | Lever |
|---|---|---|---|
| Depreciation (equipment) | 3.0 | 8 to 10 yr straight line | Utilization, asset life |
| Management & sales | 3.0 | Headcount based | Scale with volume |
| Certification maintenance | 1.0 | Audit, documentation | Shared across grades |
| Finance | 2.0 | Interest, working capital | Leverage, inventory |
| Environmental & emission | 1.5 | Dust, odor, water | Process sealing |
| Total fixed | 10.5 | Cash + depreciation | Utilization driven |
Notice that total fixed cost in this table is 10.5 index points at 80 percent utilization, but in the base-case cascade the fixed cash plus depreciation was 10.0. The small difference reflects that the base case assumes a slightly leaner overhead; the point is that fixed cost per ton is not a constant. At 60 percent utilization the same 10.5 index points of absolute annual fixed cost spreads over fewer tons and becomes about 14.0 index points per ton, while at 90 percent it drops to about 9.3. This single effect can move net profit by 4 to 5 index points without any change in the machine or the formula.
Sensitivity Analysis Matrix
A single base case is comforting but dangerous. The whole point of an index-point model is that you can flex the inputs and watch the bottom line move. The two dominant risks are feedstock cost and capacity utilization. Feedstock moves the variable side directly; utilization moves the fixed side per ton. The three-dimensional matrix below crosses feedstock at minus 15 percent, base, and plus 15 percent against utilization at 60, 75, and 90 percent, and reports the resulting net profit index points.
Feedstock x utilization net profit matrix
| Feedstock scenario | Util 60% | Util 75% | Util 90% |
|---|---|---|---|
| Feedstock -15% | 14.1 | 16.1 | 17.4 |
| Feedstock base | 8.0 | 10.0 | 11.3 |
| Feedstock +15% | 1.9 | 3.9 | 5.3 |
The matrix tells a clear story. At base feedstock and a healthy 90 percent utilization the line nets 11.3 index points, comfortably inside the 9 to 16 band. Push feedstock up 15 percent while utilization slips to 60 percent and net profit collapses to 1.9, a marginal operation that barely covers tax and risk. Pull feedstock down 15 percent with 90 percent utilization and the line reaches 17.4, above the normal band, which is exactly the windfall a compounder enjoys when recycled flake is cheap and orders are full. The lesson is that feedstock procurement and order-book fullness are not back-office concerns; they are the two largest drivers of net profit.
Single-variable yield sensitivity
Yield is the third major driver and deserves its own table because it is directly controlled by process quality. Yield here means the ratio of good pellet to clean input. A higher yield means less feedstock per ton of saleable output and less waste loss. The table holds every other input at base and varies only the good-yield between 88, 93, and 97 percent.
| Good-yield | Feedstock idx | Waste idx | Contribution idx | Net profit idx |
|---|---|---|---|---|
| 88% | 57.1 | 3.2 | 17.8 | 5.8 |
| 93% (base) | 54.0 | 3.0 | 24.0 | 10.5 |
| 97% | 51.8 | 2.9 | 26.3 | 12.3 |
Moving yield from 88 to 97 percent lifts net profit by 6.5 index points. That is a larger swing than many operators expect, and it is almost entirely free once the line is tuned, because it comes from less scrap rather than from buying anything. The next section explains the process parameters that actually deliver that yield and that contribution margin, which is the part where machine selection stops being generic and starts being specific.
How Process Parameters Rewrite Profit
This is the section that separates a commodity twin-screw line from a profit engine. Every parameter below is a physical setting on the extruder, and each one transmits into the index-point model through a measurable channel. The unifying idea is that better dispersion, cleaner venting, tighter feeding, stable pressure, fewer stops, and less thermal damage each remove cost or protect price. The table at the end of the section summarizes the transmission into net profit index points.
Screw configuration and the filler headroom it creates
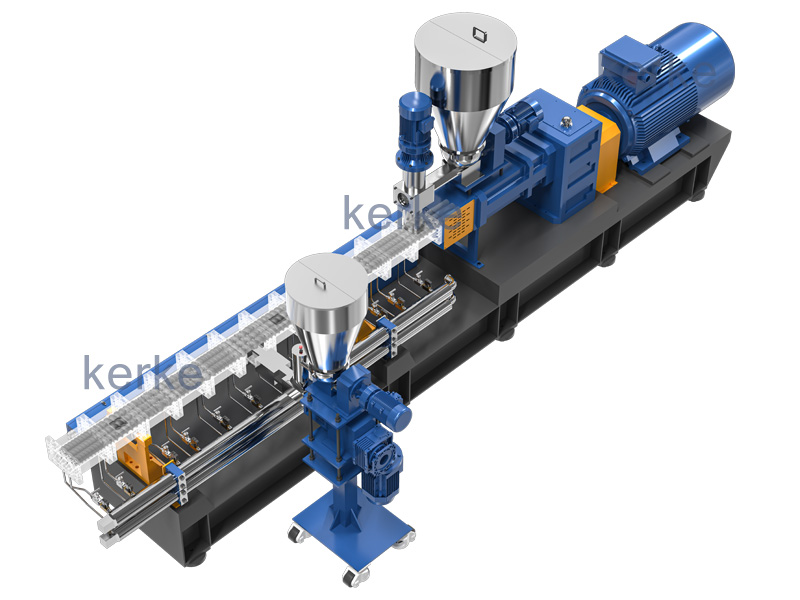
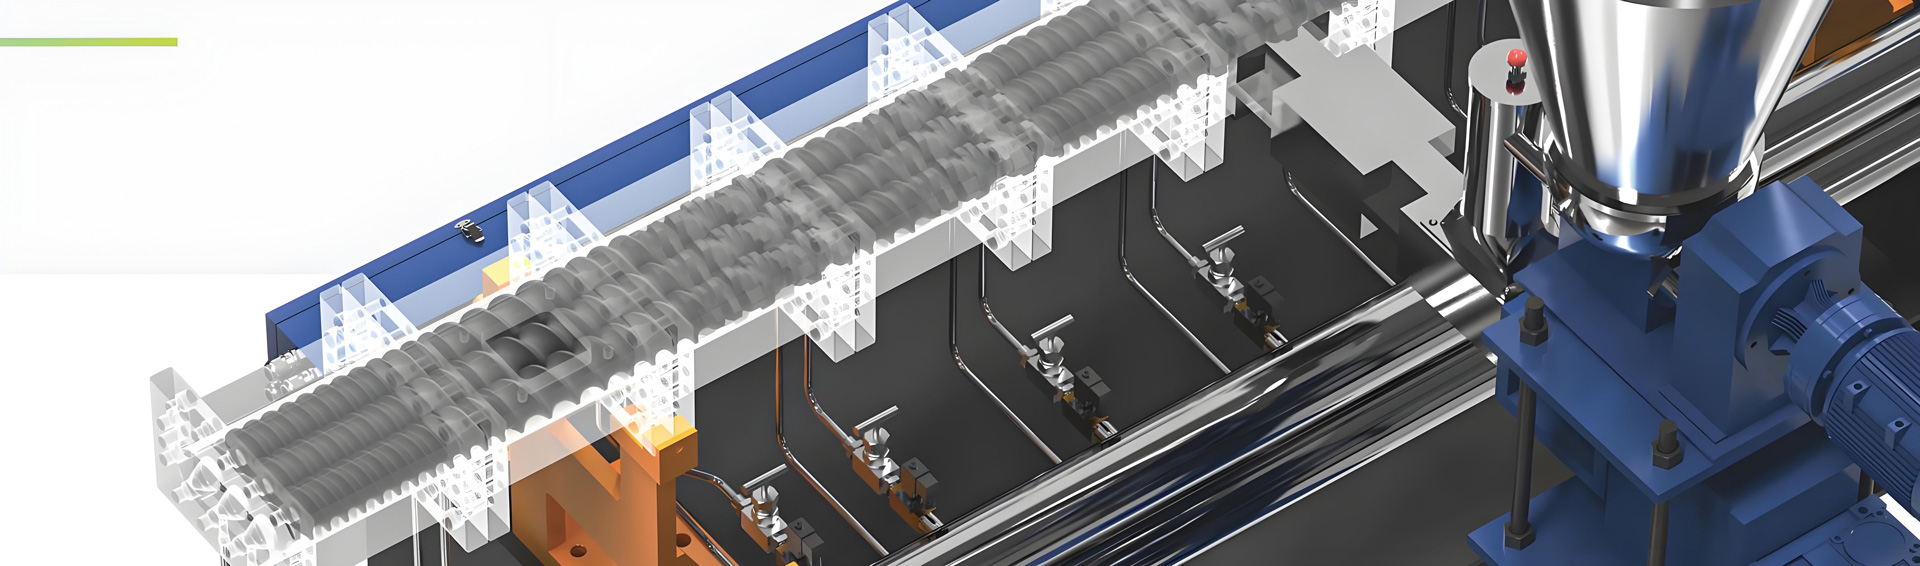
The screw is a modular assembly of conveying, kneading, and reversing elements. The ratio of 45-degree to 90-degree kneading blocks and the position of the high-shear zone decide how finely the filler, pigment, and glass fiber are dispersed. Better dispersion means the same visual and mechanical quality is reached with less additive: a well-optimized screw can often cut calcium carbonate or pigment dose by 1 to 3 index points while holding appearance, directly lifting net profit. The reversing elements also build pressure and improve mixing without raising melt temperature, which protects the heat-sensitive recycled fraction. Kerke screw assemblies are computer-aided designed for transport, plasticization, shearing, dispersion, homogenization, venting, and pressure building in one sequence, which is what makes this headroom available in the first place.
Vacuum venting and the odor-grade defense
Volatiles such as moisture, monomers, and low-molecular fractions determine odor and, for PET, acetaldehyde level. Multi-stage vacuum venting with barrels pulled to between minus 0.08 and minus 0.095 MPa strips these volatiles before the melt reaches the die. The financial channel is twofold: lower odor protects the price grade (avoiding a one-to-two tier downgrade), and lower volatile content reduces the reject and screening loss. The transmission is typically 0.5 to 2.0 index points of net profit, and it is the difference between selling into automotive or food-contact channels versus being stuck in the PCR general band.
Loss-in-weight feeding accuracy
A loss-in-weight feeder measures the actual mass flow of each ingredient by weighing the hopper, not by guessing volume. At plus or minus 0.5 percent accuracy it eliminates the chronic over-addition that volumetric feeders cause when bulk density shifts between feedstock lots. Over-addition of expensive compatibilizer, chain extender, or glass fiber is pure lost margin. Gravimetric control typically recovers 0.3 to 0.8 index points and, just as importantly, tightens batch-to-batch consistency so the MFR stays inside the tight tolerance the premium grades require.
Melt pump stabilization and pellet size uniformity
A gear-type melt pump placed after the barrel stabilizes die pressure against screw speed ripple and feed fluctuation. Stable pressure lowers the coefficient of variation of pellet size, which lowers the fraction of off-size pellet removed at the screen or classifier. The channel is small but real: 0.2 to 1.0 index point, plus the downstream benefit of a more uniform product that converters prefer. It also lets the line run the screw at its most efficient speed without sacrificing pressure stability.
Screen changer form and changeover stops
A hydraulic screen changer needs a stop or a brief flow disturbance to swap the screen pack; a continuous belt screen changer swaps filter media without halting the line. On abrasive or contaminated recycled feed, screen packs clog often, so the number of changeover stops per day directly sets overall equipment effectiveness. Moving from hydraulic to continuous form typically raises OEE by 2 to 5 percent, which on the fixed-cost side alone is worth 0.5 to 2.0 index points of net profit, before counting the saved purge material at each stop.
Temperature profile, residence time, and melt flow drift
The barrel temperature curve and the residence time distribution decide thermal degradation. Over-long residence or hot spots scorch the melt, drop molecular weight, and widen MFR drift, which forces a price discount because the buyer cannot certify the lot. A tight temperature profile with controlled shear keeps MFR drift within plus or minus 3 percent, holding the engineering-grade price. The transmission into net profit is 1 to 3 index points when it keeps the line in the premium band rather than the general band.
| Process parameter | Improvement range | Profit channel | Net profit idx gain |
|---|---|---|---|
| Screw config (kneading ratio) | Filler dose -1 to -3 idx | Less additive, same quality | +1.0 to +3.0 |
| Vacuum venting (-0.08 to -0.095 MPa) | Odor grade up, downgrade -0.5 to -1.5 idx | Price grade protection | +0.5 to +2.0 |
| Loss-in-weight feeder (±0.5%) | Over-add -0.3 to -0.8 idx | Recipe accuracy | +0.3 to +1.0 |
| Melt pump | Pellet CV down | Screening loss down | +0.2 to +1.0 |
| Continuous screen changer | OEE +2 to +5% | Fixed cost per ton down | +0.5 to +2.0 |
| Temp profile & residence | MFR drift ±3% | Grade retention | +1.0 to +3.0 |
Stack the upside and the line can move from the 10.5 base case toward the 16 index-point ceiling of the engineering band purely through process discipline, with no change in feedstock cost or selling market. That is the core message of this article: net profit on a recycled compound pellet line is an engineered outcome, not a market gift.
Kerke KTE-75D Twin-Screw Compounding Line
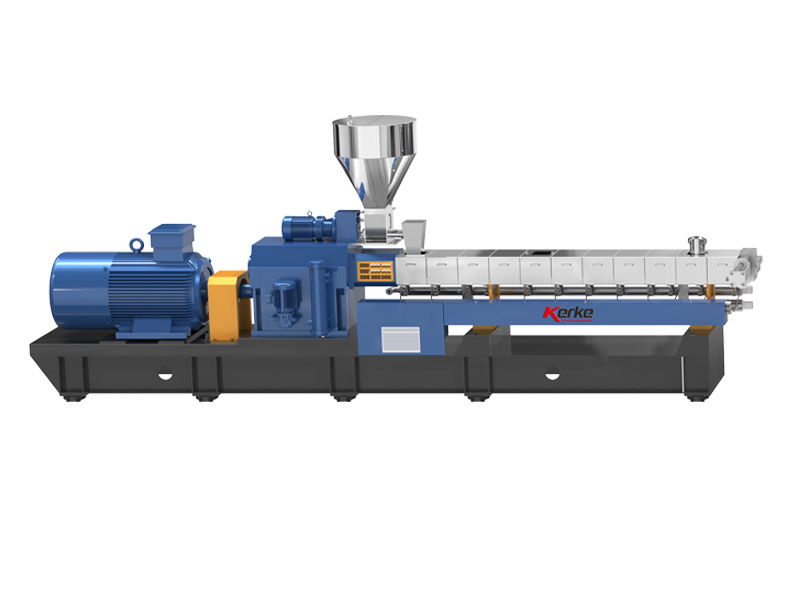
When the profit model says a mid-capacity recycled compound line is the right size, the Kerke KTE-75D is the workhorse. Kerke, a Wanplas factory, builds the KTE series as co-rotating parallel twin-screw extruders from the KTE-16B laboratory unit through the KTE-135D production line, and the KTE-75D sits in the sweet spot for compounders running 300 to 900 kg/h of recycled PP, PE, or PET compound. Its modular barrel and screw system lets the venting and shear configuration be matched to the volatility and abrasion of the specific recycled stream.
| Specification | KTE-75D value |
|---|---|
| Screw diameter | 75 mm |
| L/D ratio | 40:1 (36 to 48 configurable) |
| Main motor power | 160 kW (132 to 250 kW range) |
| Max screw speed | 600 rpm |
| Torque grade (Ma/D3) | 11 Nm/cm3 |
| Output range | 300 to 900 kg/h (material dependent) |
| Vacuum sections | 2 venting barrels |
| Barrel sections | 10 to 12 |
| Pelletizing method | Strand, air-cooled, or underwater option |
The KTE-75D is the right choice when the model points to a base or automotive grade at moderate volume, because its two venting barrels and configurable L/D give the vacuum and shear control the profit bridge depends on, while the 11 Nm/cm3 torque grade handles filled and mildly glass-loaded compounds without overloading. For formula development and scale-up, Kerke also supplies the KTE-16B laboratory twin-screw extruder, which lets a compounder validate the exact screw configuration and additive dose that the profit model assumes before committing to full production.
Kerke KTE-135D High-Capacity Compounding Line
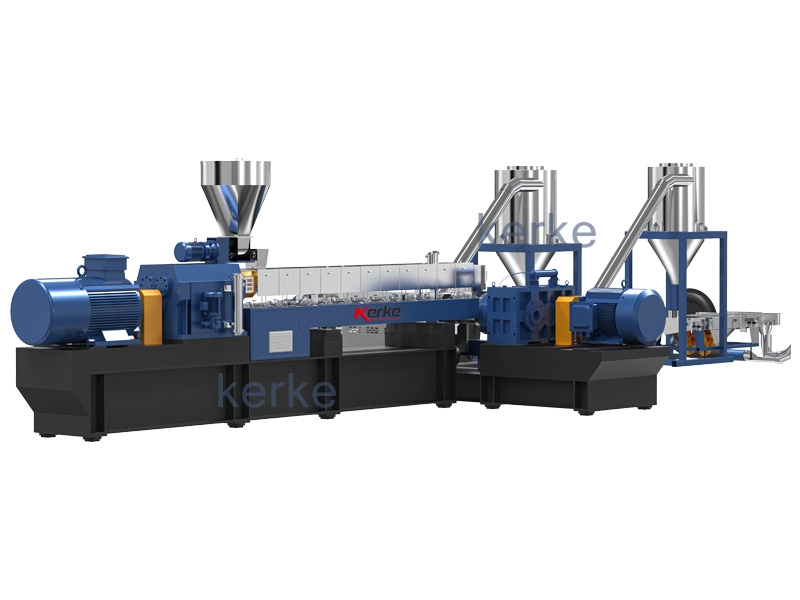
When the sensitivity matrix shows that utilization above 85 percent is achievable and the order book supports it, scale becomes the profit multiplier because fixed cost per ton falls. The Kerke KTE-135D is the production flagship of the KTE series, built for 2500 to 6000 kg/h of recycled compound. With three vacuum sections and a longer barrel stack, it is suited to the volatile-rich and abrasive streams that define recycled feedstock, and its side-feeding option handles high glass-fiber or mineral loading without starving the main feed.
| Specification | KTE-135D value |
|---|---|
| Screw diameter | 135 mm |
| L/D ratio | 40:1 (36 to 48 configurable) |
| Main motor power | 900 kW (710 to 1200 kW range) |
| Max screw speed | 500 rpm |
| Torque grade (Ma/D3) | 10 Nm/cm3 |
| Output range | 2500 to 6000 kg/h (material dependent) |
| Vacuum sections | 3 venting barrels |
| Barrel sections | 12 to 14 |
| Pelletizing method | Underwater or die-face hot cutting |
The KTE-135D earns its place in the profit model through utilization. At 90 percent utilization its fixed cost per ton is the lowest in the KTE range, which is exactly the cell in the sensitivity matrix that reaches 17.4 index points of net profit. For recycled streams that are abrasive, the longer barrel life strategy and the optional continuous screen changer keep OEE high, protecting the wear-parts line that otherwise climbs on glass-filled grades. Where a project needs washing and sorting upstream of pelletizing, Wanplas supplies matched washing and recycling systems that integrate with the Kerke twin-screw line so the whole train runs as one controlled process.
Requirement to Model Selection Guide
The profit model and the machine spec only pay off when the line is sized to the actual requirement. The table below maps a customer requirement, expressed as material system, target output, and quality positioning, to a recommended Kerke model and configuration. The aim is to avoid both under-sizing, which caps utilization and traps the line in the high fixed-cost-per-ton corner of the matrix, and over-sizing, which leaves utilization too low to amortize depreciation.
| Material system | Target output | Quality position | Recommended model | Key configuration |
|---|---|---|---|---|
| PCR PP/PE general | < 800 kg/h | General | KTE-75D | Single stage, 2 vents |
| Auto-grade PP/PE | 800 to 2000 kg/h | Medium | KTE-95D | 2 vents, side feeder option |
| Food-contact PET | 1500 to 3000 kg/h | Tight | KTE-110D | 3 vents, chain extender dosing |
| Engineering GF modified | 2500 to 6000 kg/h | Premium | KTE-135D | 3 vents, side feeder, continuous screen |
| LAB / R&D trial | 2 to 10 kg/h | Any | KTE-16B | Modular screw, same geometry |
The selection logic is driven by the profit model. A general-grade line below 800 kg/h does not need the KTE-135D, because the fixed cost would sit on too few tons and push utilization below the profitable threshold. A food-contact PET line needs the third vent and accurate chain-extender dosing to hold the grade that justifies the 1.16 price index. An engineering glass-filled line needs the side feeder so glass enters downstream of the melting zone, protecting fiber length and thus the mechanical property that the premium price pays for. Wanplas, as the parent brand, backs all of these with shared quality standards and the same service policy across the group.
OEE and Production Ramp-Up Curve
Net profit in the model is a steady-state number. A real plant does not start at steady state. The first months are dominated by commissioning, operator training, and grade stabilization, during which utilization and yield are both low and net profit can be near zero or negative before tax. The ramp-up table below shows a typical trajectory from trial production through ramp-up to steady operation, with the corresponding capacity utilization, good-yield, and net profit index points. It is the bridge between the model and the bank account.
| Phase | Period | Capacity utilization | Good-yield | Net profit idx |
|---|---|---|---|---|
| Trial production | Month 1 to 2 | 45% | 85% | 3.0 |
| Ramp-up | Month 3 to 6 | 70% | 92% | 8.0 |
| Steady operation | Month 7 onward | 88% | 96% | 12.0 |
The ramp matters for two reasons. First, it sets the payback clock: the recovery period in months is measured from the first commercial ton, and a slow ramp pushes the break-even point several months later. Second, it exposes whether the assumed yield is real; if good-yield stalls at 88 percent instead of reaching 96 percent, the steady-state net profit falls from 12.0 to roughly 5.8 index points, which is the single-variable yield table playing out in real life. A disciplined commissioning plan, good operator training, and a screw configuration validated on the KTE-16B laboratory line are what compress the ramp and protect the modeled margin.
Service, Support, and How to Start
A profit model is only as good as the machine that executes it day after day. Kerke, a Wanplas factory, supports every KTE line with a service package designed to keep OEE high and the ramp short. Each line is run through factory acceptance testing, including continuous operation checks, before shipment, so the commissioning phase starts from a known-good machine rather than a surprise. Engineers travel for on-site installation and commissioning, and operator training is built into the handover so the good-yield curve climbs fast.
The Wanplas group service promise includes USD 500 free parts every year, free replacement of damaged parts within warranty, and an open-factory policy that welcomes customers to audit the build and the process before they buy. Remote monitoring lets the Kerke engineering team read PLC and process data from the China headquarters, catch abnormal trends early, and advise corrections before a downgrade lot is made. For projects that need more than pelletizing, Wanplas supplies matched upstream washing, sorting, and recycling systems and downstream ancillary equipment such as high-speed mixers, granulators, pulverizers, and water chillers, so the customer gets one accountable process train rather than a chain of unrelated vendors.
If you are building or upgrading a recycled plastic compound pellet line and want to turn the index-point model in this article into a number tailored to your feedstock, grade target, and utilization plan, send Kerke your material specification and required output. The engineering team will propose a KTE configuration with the venting, feeding, and pelletizing setup that protects your margin, and invite you to the factory for a verification run on real material. A short sample trial on your own recycled stream is the fastest way to replace assumptions with measured yield, energy, and wear data, and to confirm the net profit index your business plan should carry.
Frequently Asked Questions
What does net profit per ton mean for recycled compound pelletizing?
Net profit per ton is the residual value after every variable and fixed cost, including depreciation and tax, is subtracted from the selling price of one metric ton of good pellets. In the index-point model used here, the selling price is normalized to 100 index points and every cost line is expressed as a share of that base, so the net profit figure is directly comparable across grades, plants, and years.
How large a share of revenue does feedstock normally consume?
Feedstock is the dominant cost center and typically consumes 52 to 62 index points of the 100-point selling price, depending on the resin family. Sorted PP and PE hard scrap sits at the low end, PET flakes and ABS or PC engineering streams sit at the high end. Because it is the largest single line, a 15 percent move in feedstock cost can swing net profit by more than 6 index points.
Which process parameter most directly improves net margin?
Vacuum venting and barrel temperature control have the most direct financial leverage. Strong multi-stage vacuum removes volatiles and odor, which protects the price grade and cuts downgrade loss, while a stable temperature profile avoids thermal degradation that widens melt flow rate drift and forces a price discount. Together these levers can add 2 to 5 index points of net profit without any change in throughput.
How does glass fiber loading change the cost model?
Glass fiber raises both the additive index and the wear-parts index. A 10 to 30 percent glass loading lifts the additive line by roughly 4 to 9 index points and shortens screw and barrel life to 3000 to 6000 hours, lifting the wear index by 1 to 2 points. It also earns a higher price grade, so the net effect is usually positive when the glass-filled grade is sold into engineering applications rather than as a commodity.
What capacity utilization is needed to stay profitable?
At base feedstock cost, the line stays clearly profitable above roughly 65 percent capacity utilization. Below 60 percent, fixed cost per ton balloons and net profit can fall under 3 index points or turn marginal, so a steady order book and fast changeover discipline matter as much as the machine specification itself.
How do certifications affect the selling price index?
Certifications that a buyer can audit and trace raise the achievable price grade. A GRS recycled-content claim, ISO 9001 quality system, and food-contact compliance such as EU 10/2011 or FDA 21 CFR 177 let a compound pellet move from the general PCR band into the food-contact or engineering band, lifting the realized price index by 12 to 30 points relative to the base grade.
How long is the payback period for a twin-screw compounding line?
Payback is driven by net margin index, annual throughput, and the installed equipment value expressed as an index. For a mid-grade recycled compound running at 80 to 90 percent utilization with a 10 to 13 index-point net margin, the recovery period commonly lands in the 24 to 48 month band; higher grades and higher utilization compress that toward the lower end of the range.
Why choose Kerke twin-screw extruders for recycled compounding?
Kerke, a Wanplas factory, builds co-rotating parallel twin-screw extruders from the KTE-16B laboratory unit through the KTE-135D production line, with computer-aided screw assemblies, multiple venting barrels, and side-feeding options suited to abrasive and volatile-rich recycled streams. The design emphasizes self-cleaning, dispersion control, and stable output, which is exactly what protects margin on recycled feedstock.
Conclusion
The net profit of a recycled plastic compound pellet line is not a mystery and it is not luck. It is a cascade that any operator can write on one sheet: revenue of 100 index points, a variable side led by feedstock at 52 to 62 points, a fixed side that thins as utilization rises, and a net result that lands in the 9 to 16 index-point band for well-run plants. The model shows that feedstock procurement and order-book fullness set the outer boundaries, while process discipline, screw configuration, vacuum venting, gravimetric feeding, melt-pressure stabilization, and quick changeover capture the margin in between. Kerke, a Wanplas factory with more than 12 years of twin-screw compounding experience, 2,000-plus machines in the field, and coverage across 70-plus countries, builds the KTE series precisely so that this margin is reachable: from the KTE-16B laboratory line that validates your formula, through the KTE-75D workhorse, to the KTE-135D high-capacity flagship. Send your material and output target, and the Kerke team will configure a line and run a sample on your own recycled stream so your profit model is built on measured data, not assumptions.