Polymer modification and masterbatch production rely heavily on the uniform fusion of base polymers and functional additives to produce high-performance plastic materials. In industrial plastic processing, common raw material combinations include polypropylene, polyethylene, ABS, and nylon polymers paired with colorants, flame retardants, anti-aging agents, tougheners, and inorganic fillers. Most polymers and additives have distinct molecular structures, surface tensions, and solubility parameters, leading to poor interfacial compatibility, uneven dispersion, phase separation, and product performance defects during simple physical mixing.
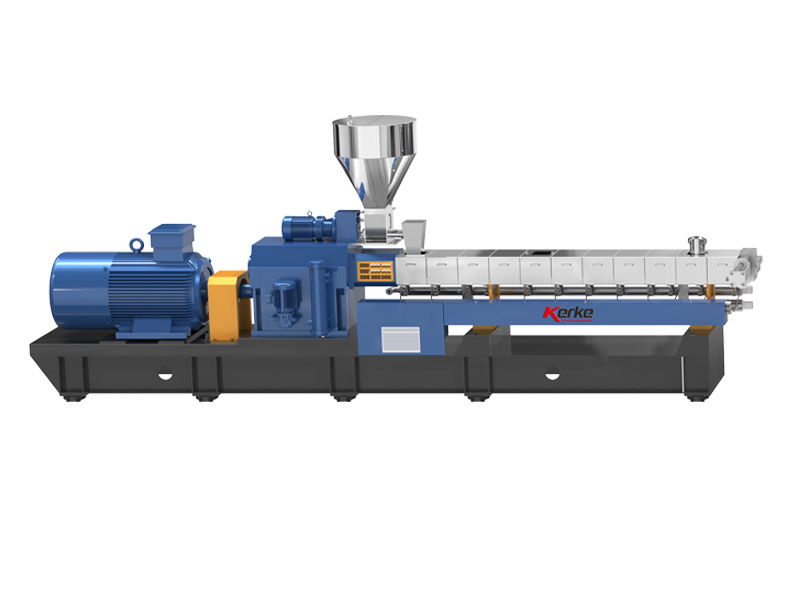
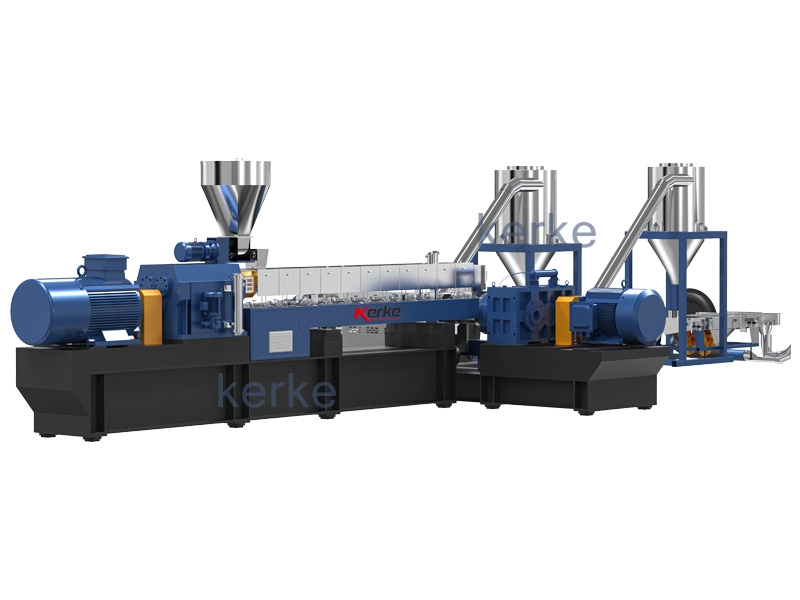
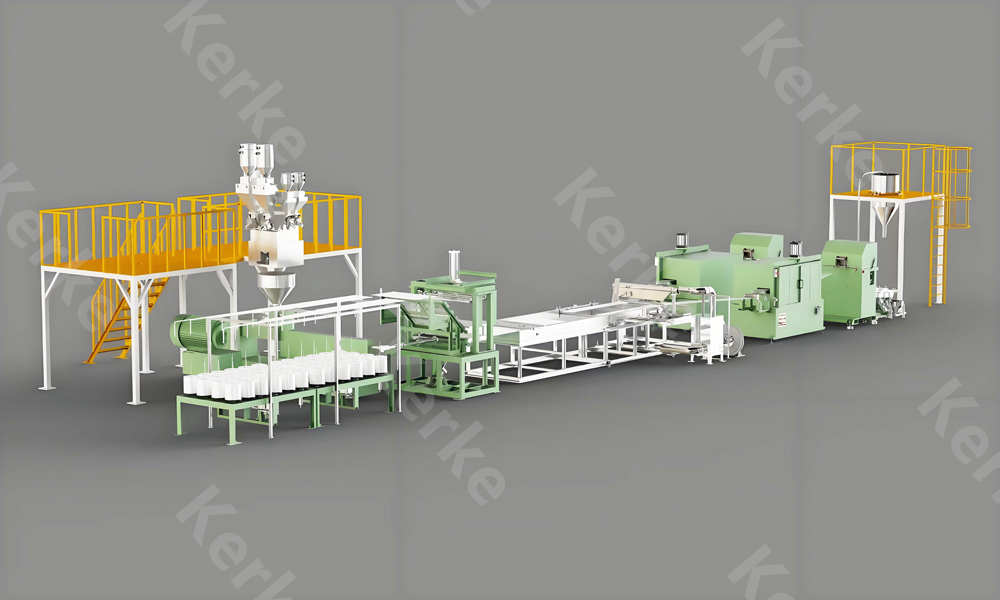
A professional masterbatch extruder, especially the twin screw compounding extruder independently developed and manufactured by KERKE, solves the core compatibility pain points of polymer and additive blending through precise mechanical shearing, temperature control, segmented feeding, and dynamic mixing technology. Unlike ordinary single-screw extruders that only achieve simple material melting and extrusion, KERKE masterbatch extruders and compounding extruders can realize microscopic interfacial fusion of polymers and additives, eliminate phase separation defects, and greatly improve the dispersion uniformity, stability, and comprehensive performance of modified masterbatch products.
This article comprehensively elaborates on the root causes of poor compatibility between polymers and additives, analyzes the core working principles of masterbatch extruders in improving interfacial compatibility, sorts out targeted process optimization schemes for different material combinations, and introduces the technical advantages and practical application effects of KERKE twin screw extruder series equipment in masterbatch production. It also includes detailed 2026 equipment price estimation, operation cost analysis, and benefit evaluation, providing systematic technical reference and procurement guidance for plastic masterbatch processing enterprises.
1. Basic Overview of Polymer and Additive Compatibility in Masterbatch Production
1.1 Definition and Core Significance of Interfacial Compatibility
Polymer and additive compatibility refers to the interfacial bonding ability and uniform mixing state between the base polymer matrix and functional additives during melting and compounding. Good compatibility means that additives can be evenly dispersed in the polymer matrix at the microscopic molecular level, forming a stable and integrated composite structure without obvious interface gaps, delamination, or particle agglomeration. Poor compatibility manifests as macroscopic uneven color, local additive accumulation, microscopic phase separation, and weak interfacial adhesion.
Compatibility is the core index determining the quality of plastic masterbatch and modified compound materials. For color masterbatch products, poor compatibility leads to color spots, color difference, and poor color migration resistance. For functional masterbatches such as flame retardant, anti-aging, and toughening types, incompatible additives cannot exert effective functional effects, resulting in unqualified product mechanical properties, weather resistance, and durability. In industrial mass production, stable compatibility directly determines product qualification rate, batch consistency, and market competitiveness.
1.2 Common Incompatibility Phenomena in Production
In conventional manual mixing and ordinary single-screw extrusion production, polymer and additive incompatibility presents typical failure characteristics. The most common problem is additive agglomeration, where powdery colorants and fillers cannot be fully dispersed, forming fine particle clusters inside the polymer matrix, resulting in surface particle protrusions and uneven texture of finished products.
Interfacial delamination is another typical incompatibility phenomenon. Polymers and additives form obvious layered structures after extrusion molding, with weak internal bonding force, which easily causes cracking, peeling, and reduced tensile strength of plastic products. In addition, mismatched polarity and molecular activity lead to additive precipitation and migration. Functional additives precipitate on the product surface during long-term use, resulting in failure of color protection, flame retardancy, and anti-aging functions.
1.3 Key Factors Restricting Polymer-Additive Compatibility
Polarity difference is the primary factor causing incompatibility. Most inorganic fillers and polar functional additives have high surface polarity, while polyolefin polymers such as PP and PE are non-polar materials. The huge polarity difference leads to extremely low interfacial affinity, making it difficult to form effective bonding fusion.
Molecular weight and melting point mismatch also restrict compatibility. Polymers have high molecular weight and long molecular chains, while most additives are small-molecule or low-melting substances. The inconsistent melting and flowing rates during heating lead to asynchronous mixing and uneven distribution. In addition, excessive additive particle size, poor raw material pretreatment, and unreasonable extrusion process parameters will further aggravate incompatibility problems.
2. Core Working Principles of Masterbatch Extruder in Improving Compatibility
2.1 Precision Shearing and Dispersion Mechanism of Twin Screw Structure
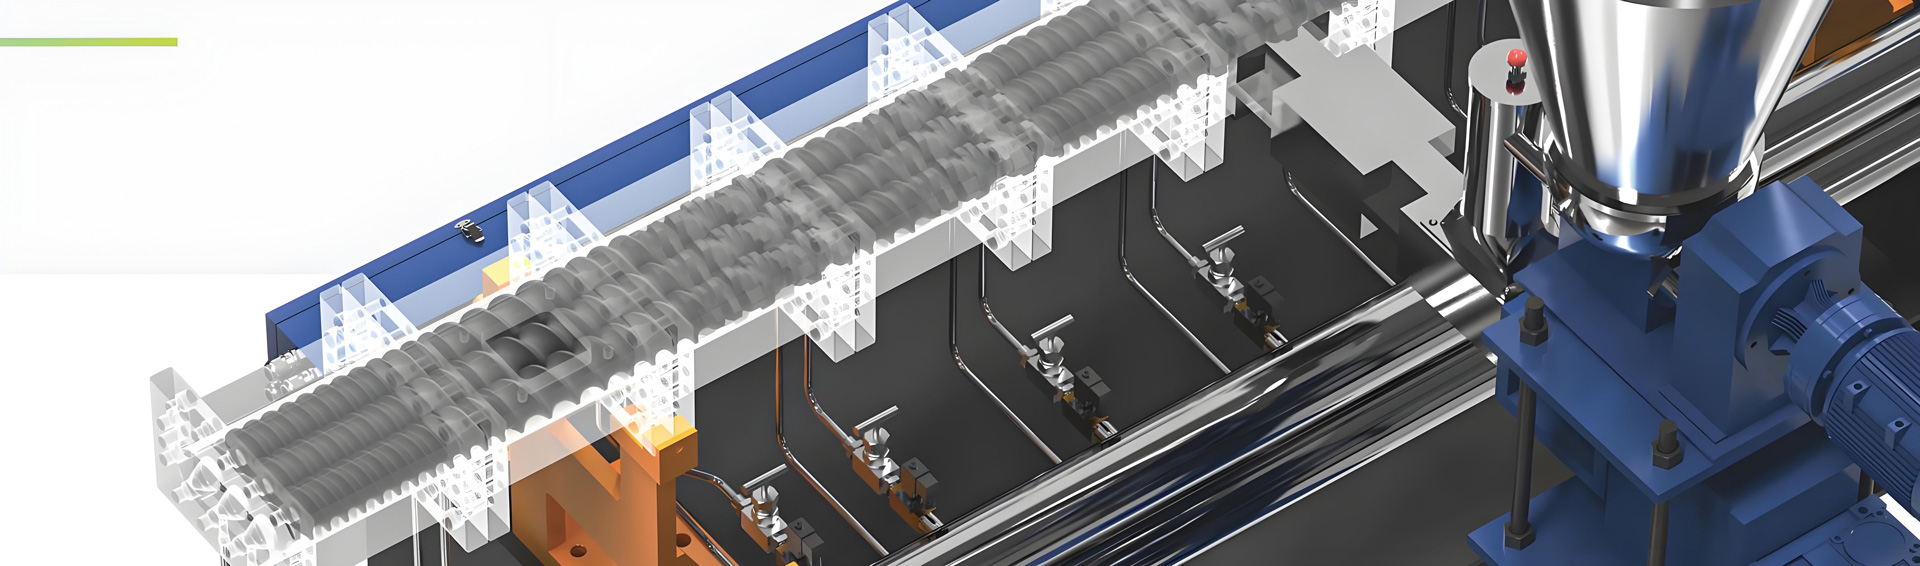
The twin screw extruder is the core equipment for high-compatibility masterbatch compounding, and it is fundamentally different from traditional single-screw equipment in shear mixing performance. KERKE twin screw extruder adopts parallel co-rotating twin screw design with optimized screw tooth profile and pitch configuration. The meshing screws form multiple strong shear zones and stretching flow fields inside the barrel, which can fully break additive agglomerated particles and reduce the particle size of fillers to microscopic uniform state.
In the extrusion process, the continuous shear, stretching, and kneading action of the twin screw can peel off the surface adsorption layer of polymer and additive particles, eliminate interfacial tension barriers, and promote molecular chain penetration and fusion between different materials. This mechanical forced mixing effect solves the problem of insufficient dispersion in ordinary mixing equipment, realizing uniform dispersion of additives in the polymer matrix and greatly improving macroscopic compatibility.
2.2 Segmented Temperature Control Optimizes Interfacial Fusion Conditions
Temperature matching is the key to improving the molecular compatibility of polymers and additives. Different polymers and functional additives have independent optimal melting and reaction temperature ranges. Excessively high temperature causes additive decomposition and polymer molecular chain degradation, while excessively low temperature leads to incomplete melting and poor fluidity, both resulting in poor compatibility.
KERKE masterbatch extruder and compounding extruder are equipped with independent multi-stage temperature control systems. Each barrel section is equipped with an independent heating and cooling module, which can accurately adjust the processing temperature according to the material characteristics. The segmented temperature setting realizes low-temperature pre-melting of heat-sensitive additives and high-temperature full plasticization of polymer matrices, ensuring that all materials are in the best fluid state for interfacial fusion, maximizing molecular compatibility and bonding strength.
2.3 Segmented Feeding Technology Avoids Functional Material Failure
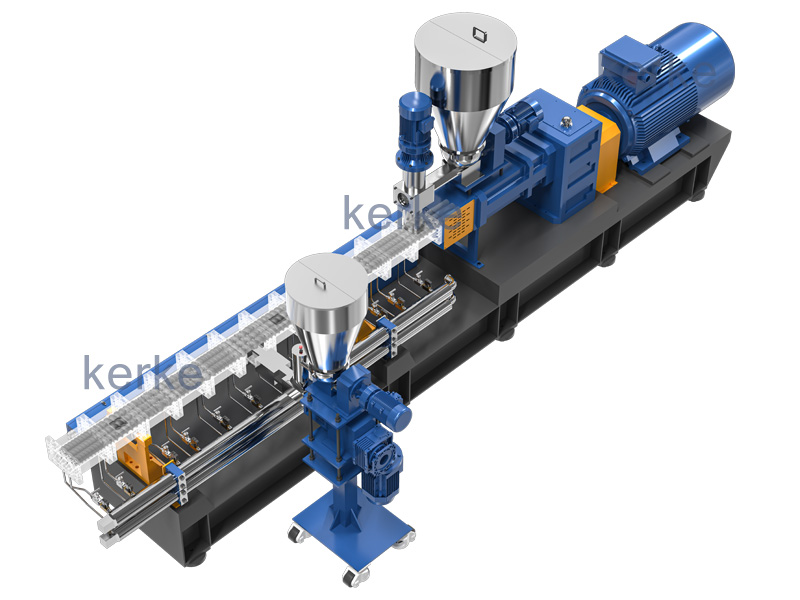
Many functional additives such as flame retardants, antioxidants, and glass fibers are heat-sensitive and shear-sensitive. Adding these materials in the initial melting stage will cause thermal decomposition and shear damage, losing functional activity and failing to form effective compatibility with polymers. KERKE twin screw compounding extruder is equipped with professional side feeding systems, realizing segmented and staged feeding of different raw materials.
The base polymer is added from the main feeding port for preliminary melting and plasticization, and heat-sensitive functional additives are accurately added from the side feeder in the middle and low-shear stage of extrusion. This technology avoids excessive high-temperature and strong shear damage to additives, retains the molecular activity of functional materials, and ensures that additives can fully react and fuse with the molten polymer matrix, effectively improving interfacial compatibility and functional stability.
2.4 Vacuum Devolatilization Purifies Interfacial Binding Environment
Raw material moisture, residual small molecules, and volatile impurities will form tiny bubbles and gap defects at the polymer-additive interface, destroying interfacial bonding and reducing compatibility stability. Ordinary extrusion equipment lacks effective devolatilization functions, resulting in residual volatile substances inside the finished masterbatch.
All KERKE compounding extruders are equipped with high-efficiency vacuum devolatilization systems, which can extract moisture, volatile small molecules, and pyrolysis impurities generated during material melting in real time. The purified melting environment eliminates interface gap defects, makes the contact between polymers and additives more compact, significantly improves interfacial bonding strength, and enhances the long-term compatibility and stability of composite materials.
3. Advantages of KERKE Masterbatch Extruder in Compatibility Optimization
3.1 Optimized Screw Module Design for Customized Mixing
As a professional manufacturer of twin screw extruder and masterbatch extruder equipment, KERKE adopts modular screw design for all compounding extrusion equipment. According to different masterbatch formulas such as color masterbatch, flame retardant masterbatch, toughening masterbatch, and filling masterbatch, different combinations of conveying elements, kneading elements, and shearing elements can be matched.
For high-filler inorganic powder masterbatches with poor fluidity, KERKE equips high-strength fine kneading screw elements to break particle agglomeration and improve dispersion uniformity. For fibrous reinforced masterbatches, low-shear stretching screw modules are adopted to avoid fiber breakage while ensuring uniform mixing. This customized screw configuration can accurately adapt to different material compatibility characteristics and solve targeted incompatibility problems.
3.2 Intelligent Closed-Loop Process Control System
The compatibility of polymers and additives is extremely sensitive to extrusion pressure, rotating speed, and temperature fluctuation. Slight parameter deviation will lead to unstable mixing effect and inconsistent batch compatibility. KERKE masterbatch extruder is equipped with an intelligent PLC closed-loop control system, which can real-time monitor and automatically adjust core parameters such as barrel temperature, screw speed, melt pressure, and feeding speed.
The system realizes synchronous matching of all process parameters, maintains stable shear force and melting state in the extrusion cavity at all times, ensures consistent interfacial fusion effect of each batch of materials, completely solves the problem of batch compatibility difference in traditional equipment, and greatly improves the qualification rate and stability of masterbatch products.
3.3 High-Precision Feeding and Uniform Proportion Control
Uneven material proportion is an important artificial factor leading to poor compatibility. Excessive local additive content causes agglomeration, while insufficient content leads to incomplete functional coverage. KERKE compounding extruder is matched with high-precision variable-frequency quantitative feeding systems, including main screw feeder and side auxiliary feeder, with feeding accuracy controlled within ±1%.
The accurate proportion control ensures that polymers and additives are mixed in the optimal formula ratio at the molecular level, avoiding compatibility defects caused by proportion imbalance. The stable feeding speed eliminates instantaneous material concentration fluctuation, making the interfacial fusion state of materials more uniform and stable.
3.4 Energy-Saving and Stable Melting System to Avoid Material Degradation
Traditional extruders have uneven heating and large temperature fluctuation, which easily cause local overheating and material molecular degradation, destroying the compatibility balance of composite materials. KERKE twin screw extruder adopts uniform circulating heating and water cooling dual system, with accurate temperature control error within ±2℃.
The stable and uniform melting environment ensures that polymers and additives complete interfacial fusion in the optimal temperature range without thermal degradation, retaining the original molecular activity of materials, and maximizing the compatibility and comprehensive performance of composite masterbatch materials.
4. Targeted Compatibility Optimization Solutions for Common Masterbatch Types
4.1 Color Masterbatch Polymer-Additive Compatibility Optimization
Color masterbatch is composed of polyolefin carrier polymer and organic/inorganic colorant powder. The main incompatibility problems are colorant agglomeration, uneven coloring, and color migration. KERKE masterbatch extruder adopts multi-stage gradual shearing process for color masterbatch production. The primary stage realizes carrier polymer melting and plasticization, the middle stage completes low-strength dispersion of colorant particles, and the final stage strengthens interfacial fusion.
The optimized screw shear configuration can break nano and micron colorant agglomerates, make colorant particles uniformly embedded in the polymer molecular chain gaps, form stable physical bonding, effectively solve color difference and color migration problems, and improve color uniformity and color fastness of masterbatch products.
4.2 Flame Retardant Masterbatch Compatibility Improvement Scheme
Flame retardant masterbatch has prominent incompatibility problems due to high content of inorganic flame retardant powder and polar molecular structure. Traditional processing methods easily cause flame retardant particle precipitation and poor dispersion, resulting in unqualified flame retardant performance of products. KERKE twin screw compounding extruder adopts high-efficiency kneading and devolatilization process for flame retardant masterbatch production.
Through strong shear kneading, the flame retardant powder is fully dispersed, and the vacuum devolatilization system eliminates interface bubbles. Combined with segmented low-temperature feeding technology, the thermal decomposition of flame retardants is avoided, ensuring that flame retardant additives and polymer matrix form a compact and compatible composite structure, giving full play to the flame retardant functional effect.
4.3 Toughening and Modified Masterbatch Compatibility Optimization
Toughening masterbatch is made by blending elastomer tougheners and rigid polymers, and the main incompatibility problem is interfacial delamination and weak bonding. KERKE compounding extruder adopts moderate shear and stretching process to promote the penetration of toughener molecular chains into the polymer matrix gaps.
The equipment accurately controls the melting viscosity matching of two different polymers, realizes microscopic interpenetrating network structure formation, greatly improves interfacial bonding strength, solves the delamination and cracking problems of toughened products, and significantly improves the impact toughness and tensile properties of modified plastics.
4.4 High-Filler Filling Masterbatch Compatibility Solution
High-filler masterbatch with calcium carbonate, talc powder, and mica powder has the worst compatibility due to large filler particle size, high hardness, and huge polarity difference with polymers. KERKE masterbatch extruder is equipped with enhanced shear screw modules and anti-wear barrel structures for high-filler production.
The equipment realizes ultra-fine dispersion of filler particles through multi-stage cyclic shearing, and the precise temperature control system optimizes the interfacial tension of materials. Combined with auxiliary coupling agent addition process, the surface activity of inorganic fillers is improved, the polarity difference between fillers and polymers is reduced, and the overall compatibility and mixing uniformity of high-filler masterbatch are fundamentally improved.
5. Production Losses Caused by Poor Polymer-Additive Compatibility
5.1 Direct Product Quality and Yield Losses
Poor compatibility directly leads to a sharp increase in masterbatch defective rate. Uneven dispersion and phase separation cause batch color difference, surface particle defects, and unqualified functional indicators. For medium-sized masterbatch production lines using ordinary extrusion equipment, the defective rate caused by compatibility problems is as high as 8% to 12%. Calculated based on an annual output of 500 tons of masterbatch, the annual waste of finished materials reaches 40 to 60 tons, bringing direct economic losses of tens of thousands of US dollars.
Incompatible masterbatch products cannot meet the quality standards of downstream plastic products, resulting in order return and rework, seriously affecting enterprise production efficiency and market reputation.
5.2 Increased Production and Processing Costs
To make up for poor compatibility effects, enterprises often increase the addition proportion of functional additives, resulting in serious waste of high-cost additives such as flame retardants, antioxidants, and colorants. The excess additive dosage increases the raw material cost per ton of masterbatch by 5% to 10%.
In addition, unqualified products need repeated reprocessing and secondary extrusion, increasing equipment operation energy consumption, labor cost, and time cost. Long-term repeated processing will also cause polymer molecular degradation, reducing product stability and service life.
5.3 Restriction on Product Upgrading and Market Expansion
High-end functional masterbatch products have extremely strict compatibility and dispersion requirements. Ordinary extrusion equipment cannot meet the production standards of high-precision masterbatch, resulting in enterprises being unable to enter the high-end market and only able to produce low-value ordinary products. Long-term compatibility technical bottlenecks restrict product upgrading, profit improvement, and enterprise scale expansion.
6. KERKE Extruder Equipment Price and Operation Cost-Benefit Analysis (2026)
6.1 KERKE Core Equipment Price Estimation
KERKE provides complete series of twin screw extruder, masterbatch extruder, and compounding extruder for masterbatch production, with equipment prices varying according to model specifications and configuration standards. The small laboratory and pilot-scale twin screw compounding extruder suitable for formula research and small-batch production is priced at 18,000 to 25,000 US dollars per set.
The medium-sized industrial standard masterbatch extruder for mass production is priced at 32,000 to 45,000 US dollars per set, equipped with full intelligent control, segmented temperature control, vacuum devolatilization, and high-precision feeding systems, fully meeting the compatibility optimization requirements of various conventional masterbatches.
The large-scale high-output twin screw compounding extruder for high-filler and high-precision functional masterbatch production is priced at 50,000 to 68,000 US dollars per set, with enhanced screw shearing structure and customized functional modules, suitable for high-standard high-end masterbatch production.
6.2 Daily Operation and Maintenance Cost Comparison
Ordinary single-screw extruders with low compatibility optimization ability have high defective rate and large additive waste, with an annual comprehensive loss of 8,000 to 15,000 US dollars for a single production line. In addition, ordinary equipment has unstable operation and frequent failures, with annual maintenance and accessory replacement costs of 1,200 to 2,000 US dollars.
KERKE twin screw extruder and masterbatch extruder have stable operation and excellent compatibility optimization performance, reducing the product defective rate to below 2%. The annual raw material and quality loss saving of a single production line is more than 7,000 US dollars. The equipment has low failure rate and long service life of wearing parts, with annual maintenance cost controlled within 400 to 800 US dollars, greatly reducing long-term comprehensive operating costs.
6.3 Equipment Investment Return Cycle Analysis
For enterprises upgrading from ordinary single-screw equipment to KERKE professional masterbatch extruder and compounding extruder, the annual comprehensive cost saving and profit improvement brought by compatibility optimization is about 9,000 to 18,000 US dollars. The one-time equipment investment can be fully recovered within 2 to 3 years. For newly purchased KERKE twin screw extrusion production lines, the product qualification rate and product added value are significantly improved, and the long-term economic benefit advantage is very prominent.
7. Auxiliary Process Measures to Further Improve Compatibility
7.1 Raw Material Pretreatment and Modification
Cooperate with the high-precision mixing performance of KERKE extruder, implement standardized raw material pretreatment. Dry polymers and additives to control moisture content below 0.3%, eliminate interfacial bubble defects caused by moisture volatilization. For inorganic fillers, adopt coupling agent surface modification treatment to reduce surface polarity, improve interfacial affinity with non-polar polymers, and further enhance mixing compatibility.
7.2 Reasonable Screw Speed and Process Parameter Matching
Formulate targeted parameter schemes based on KERKE extruder intelligent control system. Appropriately increase screw speed for fine powder color masterbatch to enhance shear dispersion effect. Reduce shear speed and extend kneading time for toughened modified masterbatch to ensure sufficient interfacial fusion. Realize one-click parameter calling for different formulas to maintain stable compatibility effect.
7.3 Regular Equipment Maintenance and Parameter Calibration
Regularly check the wear of extruder screw and barrel to avoid reduced shear uniformity caused by component wear. Calibrate feeding accuracy and temperature control parameters monthly to ensure stable extrusion process conditions. Clean the vacuum devolatilization system regularly to maintain efficient volatile removal effect, ensuring long-term stable compatibility optimization ability of the equipment.
8. Common Compatibility Failure Troubleshooting and Solutions
8.1 Additive Agglomeration and Uneven Dispersion
This failure is caused by insufficient screw shear strength or excessive additive particle size. The solution is to adjust the KERKE extruder screw module combination, increase the proportion of kneading elements, appropriately improve the main engine rotating speed, and strengthen raw material screening pretreatment to remove large agglomerated particles, ensuring full dispersion of additives.
8.2 Interfacial Delamination and Poor Bonding
Interfacial delamination is due to unreasonable temperature matching and insufficient material fusion time. It is necessary to optimize the segmented temperature parameters of the extruder, appropriately extend the material kneading and residence time in the barrel, and match a small amount of compatibilizer additives to reduce polarity difference, effectively improving interfacial bonding compatibility.
8.3 Functional Precipitation and Instability
Functional additive precipitation is caused by incomplete devolatilization and unstable molecular fusion. Turn on the high-power vacuum devolatilization function of KERKE compounding extruder, optimize feeding sequence and proportion, avoid excessive local additive concentration, and realize stable embedding and fusion of functional additives in polymer matrix.
9. Conclusion
The compatibility between polymers and additives is the core factor determining the quality and performance of plastic masterbatch and modified compound materials. Poor compatibility will lead to a series of problems such as uneven product dispersion, defective functions, increased production costs, and restricted product upgrading. Professional masterbatch extruders and twin screw compounding extruders fundamentally solve various incompatibility pain points through mechanical shear dispersion, segmented precise temperature control, scientific segmented feeding, and high-efficiency devolatilization technology.
As a professional extrusion equipment manufacturer, KERKE twin screw extruder, masterbatch extruder, and compounding extruder rely on optimized screw modular design, intelligent process control system, and customized production solutions to significantly improve the interfacial compatibility and mixing uniformity of polymers and additives. The equipment can effectively reduce product defective rate and comprehensive operating costs, improve product added value and market competitiveness for masterbatch processing enterprises, and provide stable and efficient equipment support for high-quality, high-precision, and low-cost masterbatch industrial production.